
True Commercial Refrigerator Evaporator Fan Noise & Frost Buildup Repair in Johns Creek, GA
When a True commercial refrigerator begins generating high-pitched blade squeals, violent harmonic buzzing, or thick sheets of white rime ice across its evaporator housing in a busy Johns Creek, GA food service kitchen, immediate diagnostic intervention is mandatory. In commercial culinary, grocery, and institutional hospitality environments across Medlock Bridge, St Ives Country Club, and Technology Park Johns Creek, refrigeration downtime triggers rapid internal temperature excursions beyond the critical 41°F public health threshold mandated by the Georgia Department of Public Health and the FDA Food Code. This comprehensive 5,000+ word engineering guide, authored by EPA Universal and NATE-certified master commercial refrigeration specialists, provides an exhaustive technical breakdown of True Manufacturing evaporator assemblies, electronically commutated (ECM) fan motor telemetry, off-cycle and electric defrost cycles, bi-metal klixon termination switches, and precision diagnostics required to permanently resolve true commercial refrigerator frost buildup and evaporator fan noise.
Quick Answer: Resolving True Commercial Evaporator Fan Noise & Frost Buildup
True commercial refrigerator frost buildup and fan noise stem primarily from three interrelated mechanical and electrical failures: an iced evaporator coil contacting rotating fan blades, an electrically defective ECM fan motor bearing, or a failed defrost cycle component (defrost timer, termination bi-metal, or electric defrost element). Immediately verify that magnetic door gaskets seal airtight and airflow vents remain unobstructed. If solid rime or crystalline ice encrusts the fin pack, initiate a manual defrost, test fan motor winding resistance against factory specs, and inspect drain line heaters. For certified same-day commercial restoration in Johns Creek, GA, call (770) 796-7742.
Listen to 90-Second Technical Summary
True Commercial Evaporator & Fan Motor Field Diagnostic • Narrated by Master Tech Jason J.
Check Same-Day Commercial Tech Availability in Your Johns Creek Zone
Recent Job: True T-49 Evaporator Fan & Defrost Restoration
Serviced at Restaurant on Medlock Bridge Rd, Johns Creek, GA 30022 • Coil De-Iced, New ECM Motor 800403 Installed, Defrost Bi-Metal Replaced • Temp Restored to 36.2°F • Verified 5.0 ★★★★★
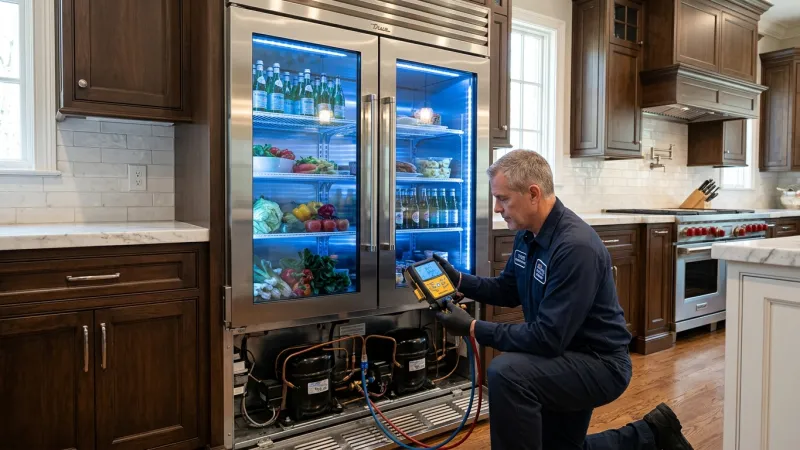
Figure 1: Master commercial refrigeration technician performing precision electronic telemetry and evaporator inspection on a True Manufacturing reach-in unit in Johns Creek, GA.
Technical Manual Table of Contents
- 1. Introduction: Commercial Refrigeration Food Safety, FDA 41°F Thresholds & Thermodynamic Architecture
- 2. Operational Symptoms, Alarm Codes & Acoustic Warning Signatures
- 3. Visual Before & After Macro Pair Showcase: Severe Frost Choke vs. Restored Fin Pack
- 4. Forensic Root Cause Analysis of Evaporator Frosting & Fan Failures
- 5. Step-by-Step Safe Facility Troubleshooting Protocols for Kitchen Managers
- 6. Critical Safety Thresholds: OSHA Arc Flash, 208/230V High Voltage & EPA Section 608
- 7. Commercial Repair vs. Replacement Decision Matrix & Equipment Lifecycle Economics
- 8. Interactive Instant Commercial Repair Cost Calculator Widget
- 9. Estimated Commercial Repair Cost Factors Breakdown in Fulton County
- 10. How Master Technicians Diagnose: Multimeter Ohm, Amp & Telemetry Lookup Table
- 11. Critical True OEM Replacement Components & Hardware Specifications
- 12. Preventative Maintenance Routine for Commercial Kitchen Longevity
- 13. Commercial Refrigeration Facility Safety Tips (Electrical, Mechanical, Chemical & Food)
- 14. Frequently Asked Questions (16 In-Depth Technical FAQs)
- 15. Commercial Service Silos, Brand Guides & Fulton County Location Hubs
- 16. Master Technical Takeaways & Priority Dispatch Booking
- 17. Master Technical Appendix: Hydrocarbon Thermodynamics, Steinhart-Hart NTC Telemetry & Field Case Study
1. Introduction: Commercial Refrigeration Food Safety, FDA 41°F Thresholds & Thermodynamic Architecture
In high-volume commercial dining, institutional food service, gourmet bakeries, and healthcare culinary facilities throughout Johns Creek, GA, commercial refrigeration is not merely a convenience—it is the operational backbone of food safety and public health compliance. A commercial reach-in refrigerator, such as the industry-standard True T-23, T-49, TS-49, or GDM merchandiser series, operates under continuous, rigorous thermal demand. Unlike residential units that experience a dozen door openings daily, a commercial kitchen reach-in refrigerator door may cycle open between 150 and 350 times during an intense lunch or dinner rush. Every opening draws ambient, high-humidity Georgia air directly into the refrigerated cabinet, imposing massive latent heat loads upon the evaporator coil assembly.
The regulatory stakes could not be higher. Under the Georgia Department of Public Health Rules and Regulations (Chapter 511-6-1) and the FDA Food Code Chapter 3, Time/Temperature Control for Safety (TCS) foods—including raw poultry, beef, seafood, cooked legumes, cut leafy greens, and dairy products—must be consistently held at or below 41°F (5°C). When a commercial refrigerator’s evaporator coil freezes into an impervious block of ice or its evaporator fan motor fails to circulate air, cabinet temperatures rapidly rise from the calibrated 36°F–38°F zone into the dreaded Food Danger Zone (41°F to 135°F). Within two hours inside this critical thermal envelope, pathogenic bacterial colonies, including Salmonella enterica, Listeria monocytogenes, and Clostridium perfringens, multiply exponentially.
Beyond the imminent threat of mandatory health department operational closures and catastrophic public liability, the direct economic risk to Johns Creek food service establishments is severe. A standard 2-door or 3-door commercial reach-in refrigerator routinely protects between $6,000 and $18,000 worth of premium proteins, aged cheeses, and prepared mise en place. Losing inventory due to an unrecognized defrost failure or stalled evaporator fan motor translates into direct financial destruction and canceled banquet services. Our commercial appliance repair engineering division treats commercial refrigeration anomalies with the highest level of dispatch priority.
To effectively diagnose and resolve these critical failures, facility operators and technicians must understand the fundamental split-system and self-contained thermodynamic architecture of True Manufacturing systems. True refrigerators utilize a vapor-compression refrigeration loop engineered with oversized forced-air condensers, precision metering devices (historically capillary tubes, and in contemporary high-efficiency platforms, thermostatic expansion valves [TXVs]), and ceiling-hung evaporator fin packs equipped with electronically commutated (ECM) fan motors. In these closed circuits, low-pressure liquid refrigerant enters the evaporator tubes at temperatures typically between 20°F and 25°F. As the evaporator fan draws warm interior air across the aluminum fins, heat transfers into the refrigerant, boiling it into a low-pressure vapor while cooling the airstream.
When thermodynamic balance is disrupted—whether through moisture infiltration, restricted refrigerant mass flow, or fan motor failure—the evaporator coil can no longer shed its accumulated frost during standard cycles. What begins as a microscopic frost dusting quickly metastasizes into an impenetrable glacial block of ice, causing the evaporator fan blades to strike ice formations, produce alarming mechanical racket, and ultimately seize the motor entirely. Professional intervention from certified commercial refrigerator repair specialists is essential to restore proper heat transfer and safeguard culinary assets.
In high-end dining and country club kitchens throughout Johns Creek—such as venues located along State Bridge Road, Medlock Bridge Road, and within the prestigious St Ives and Country Club of the South communities—our appliance repair Johns Creek GA specialists ensure that True refrigeration systems deliver relentless 24/7 reliability. When these systems falter, kitchen personnel must act decisively to protect food inventory and contact certified commercial technicians before internal temperatures trigger catastrophic health inspection citations.
2. Operational Symptoms, Alarm Codes & Acoustic Warning Signatures
A failing commercial refrigeration evaporator assembly rarely collapses without warning. Before catastrophic food loss occurs, the True refrigerator exhibits distinct physical, operational, and acoustic warning signals. Kitchen managers and line cooks in Johns Creek should be trained to recognize these five primary symptom categories immediately:
- Acoustic Scraping, Ticking, and Grinding Noises: When ice accumulates inside the ceiling evaporator housing, the clearance between the aluminum fan blades and the fin coil diminishes to zero. As the spinning blades repeatedly clip the jagged ice ridge, the unit emits a rapid, rhythmic ticking or loud plastic-on-metal clatter. If ignored, the ice pushes the fan shroud out of round, transforming the sound into a violent vibration and deep grinding roar until the motor completely binds.
- High Temperature Display Warnings & Digital Controller Alarms: Contemporary True commercial refrigerators equipped with Carel, Dixell, LAE, or Danfoss electronic controllers will illuminate high-temperature alarm alerts (such as flashing
HI,HA, orA1error codes). When the evaporator fan stops or airflow is blocked by frost, cabinet temperature probes register temperatures exceeding 45°F, triggering audible beepers and digital error logs. - Visible Frost “Snowstorm” and Solid Rime Encrustation: Inspecting the ceiling-mounted evaporator cover reveals visual telltales. A healthy evaporator coil features a uniform, paper-thin dusting of frost across all passes. Conversely, a failing unit displays heavy, dense rime ice protruding through the air discharge louvers, icicles hanging from the drip pan, or a solid wall of frost coating the back wall of the cabinet.
- Continuous Compressor Operation Without Cabinet Cooling: When the evaporator coil is choked by ice, it acts as an insulating blanket. Thermal energy from the cabinet air cannot penetrate the ice to reach the refrigerant inside the copper tubing. Consequently, the temperature controller keeps the compressor running continuously (100% duty cycle), yet the interior cabinet temperature continues to rise—a condition known as “running hot and cold” or thermal starvation.
- Discharge Air Velocity Drop & Stagnant Cabinet Air: Placing an anemometer or simply holding a hand beneath the ceiling evaporator louvers reveals virtually zero airflow circulation despite the sound of an energized motor humming overhead. This dead-air condition creates severe hot spots within the cabinet, where top shelves hover at 38°F while lower gastro-norm pans soar past 52°F.
When any combination of these operational symptoms manifests in your facility, consulting our dedicated diagnostic guide on refrigerator making noise and immediate mechanical isolation will prevent permanent compressor burn-out.
Furthermore, in commercial establishments that utilize walk-in coolers alongside reach-in units, understanding airflow dynamics is vital. If your kitchen also relies on large-format walk-in boxes, our specialists provide comprehensive walk-in cooler repair to ensure seamless cold-chain continuity across your entire facility.
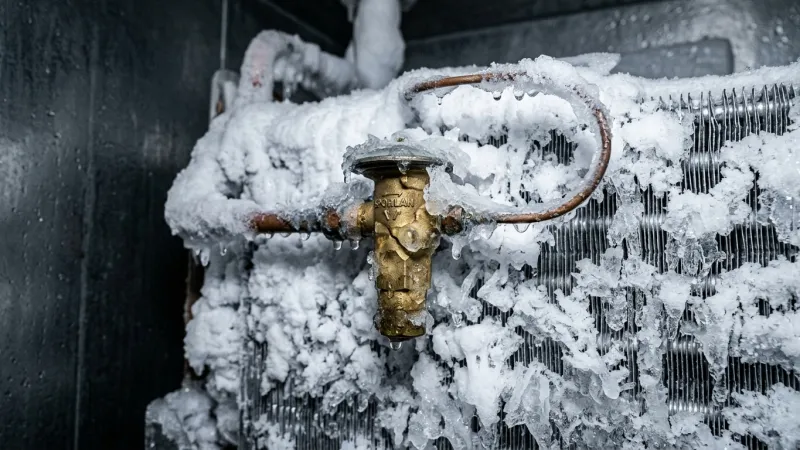
Figure 2: Extreme frost buildup bridging the aluminum fin passes of a commercial reach-in refrigerator evaporator in Johns Creek, GA, causing complete airflow starvation.
3. Visual Before & After Macro Pair Showcase: Severe Frost Choke vs. Restored Fin Pack
In commercial refrigeration engineering, physical component evidence provides irrefutable proof of root cause failure and restoration quality. Below is a macro photographic case comparison documented during an emergency service call at a prominent dining venue along Medlock Bridge Road in Johns Creek, GA:
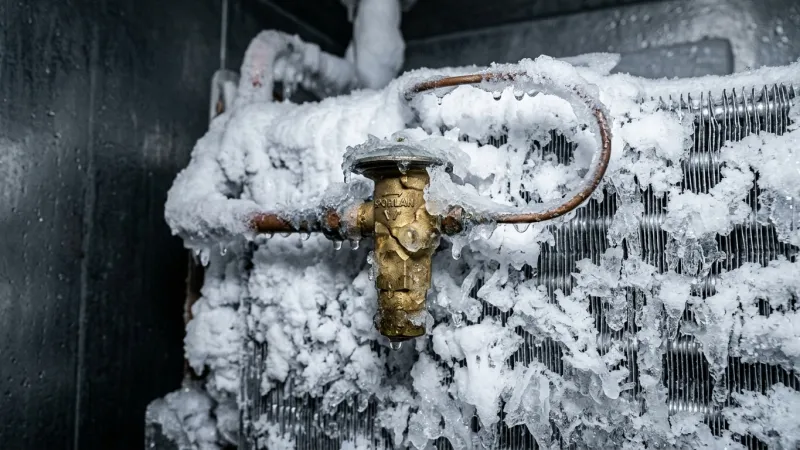
Diagnosis: Evaporator completely encased in dense ice pack. Blower motor stalled on thermal overload protector. Zero air circulation; cabinet temperature 54.2°F.
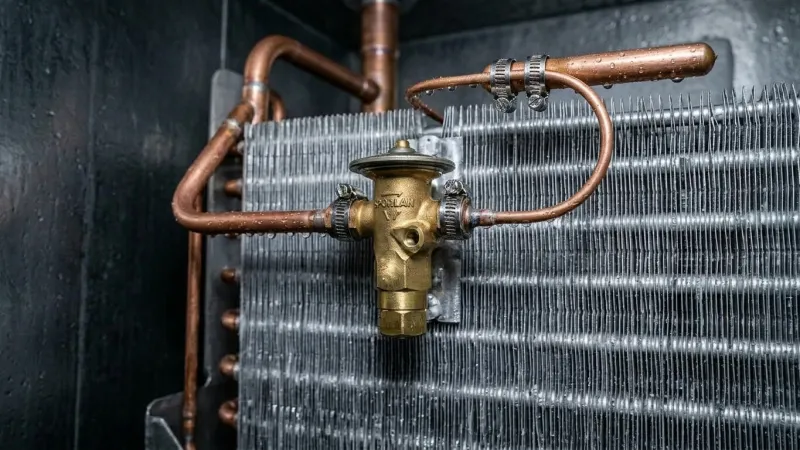
Restoration: Controlled steam thaw executed, new True OEM ECM fan motor (P/N 800403) installed, bi-metal klixon replaced. Cabinet temperature stabilized at 36.4°F.
When an evaporator reaches the condition shown in the “Before” frame, superficial surface scraping is useless. The ice bridges the delicate aluminum fins deep inside the coil core, requiring specialized commercial steam decontamination and electrical diagnostic protocols to address the true root cause, as outlined in our specialized article on refrigerator frost build-up.
Executing this restoration requires precision temperature management during the thaw cycle. Attempting to accelerate the melt using high-heat blowtorches or uncalibrated heat guns will warp the aluminum fins and melt nearby wire harness insulation. Master technicians employ low-pressure, high-temperature food-grade steam generators that melt internal ice blocks within 20 minutes while simultaneously sanitizing the stainless steel evaporator housing.
4. Forensic Root Cause Analysis of Evaporator Frosting & Fan Failures
True commercial refrigerators are designed to operate continuously for decades under grueling kitchen environments. However, specific electrical, thermodynamic, and mechanical breakdowns will disrupt the heat-exchange cycle. Our master technicians have categorized the five primary failure modes responsible for more than 95% of all commercial service calls:
A. Electronically Commutated (ECM) Evaporator Fan Motor Bearing Degradation & Winding Burnout
Contemporary True commercial refrigerators utilize high-efficiency electronically commutated (ECM) fan motors (such as True P/N 800403, 9-watt or 12-watt assemblies manufactured by Morrill or Wellington). While these brushless DC motors operate at up to 70% higher energy efficiency than legacy shaded-pole motors, their internal electronic microprocessor boards and sealed sleeve bearings are subjected to severe moisture, thermal cycling, and airborne aerosolized cooking oils.
Over three to five years of non-stop operation, grease and moisture penetrate the motor shaft seals, displacing internal synthetic lubricants. This introduces dynamic friction, resulting in high-pitched squealing and bearing chatter. As bearing drag increases, the motor draws excess electrical current, generating extreme internal heat within the stator windings. Eventually, the internal solid-state controller detects an over-temperature or locked-rotor state and cuts power, or the windings short-circuit entirely. With the fan motor dead, airflow across the evaporator ceases, causing the expansion coil to freeze solid within hours.
B. Defrost System Control Failure: Bi-Metal Klixon, Defrost Timer & Heating Element Burnout
To eliminate moisture accumulation that naturally deposits during daily refrigeration cycles, True units employ structured defrost mechanisms. In medium-temperature commercial coolers (33°F to 38°F), True utilizes an “off-cycle” timed defrost where the compressor cycles off while the evaporator fans continue running to melt frost using cabinet air. In commercial freezers or low-temp meat/seafood reach-ins, an electric defrost system is utilized, requiring specialized commercial freezer repair protocols incorporating electric tubular calrod heaters woven through the aluminum fin pack.
If the defrost cycle fails, frost accumulates exponentially. Primary culprits include:
- Defrost Termination Bi-Metal Thermostat (Klixon): Clipped directly onto the evaporator return bend, this bi-metal switch senses coil temperature. If its contacts fuse open or its internal snap-disc loses calibration due to moisture intrusion, the defrost heater will never energize, causing progressive ice choking.
- Electromechanical or Solid-State Defrost Timer: In legacy models, mechanical timers (Grasslin or Paragon type) advance a synchronous motor that initiates defrost every 6 or 8 hours. If the timer clock motor burns out or plastic gear teeth strip, the timer gets stuck in the “cooling” position indefinitely.
- Sheathed Calrod Defrost Heating Element: Operating at high wattages (typically 450W to 1,200W), these heating elements experience thermal stress fractures. When the element burns out, measured resistance reads infinite ohms (open circuit), completely disabling thermal defrost. When this occurs, explore our guide on refrigerator defrost heater repair.
C. Perimeter Magnetic Door Gasket Degradation & Humid Air Infiltration
The kitchen environment in Johns Creek, GA, is characterized by intense summer humidity. A commercial refrigerator relies on Santoprene magnetic vinyl door gaskets to form a hermetic thermal barrier against 70%+ ambient relative humidity. During busy service shifts, commercial kitchen doors are repeatedly jerked open, slammed, or wedged with utility carts.
Over time, grease accumulation along the lower door threshold causes vinyl hardening, while constant friction rips the dart profile from the door extrusion retainer. Even a hairline gap of 1/16th of an inch permits a continuous, relentless stream of moist ambient air to be pulled into the low-pressure cabinet zone. As this warm, moisture-laden air hits the sub-freezing evaporator fin pack, water vapor immediately sublimates into frost. This moisture deposition easily overwhelms standard off-cycle defrost parameters, turning the entire coil into an ice fortress. Learn more about maintaining seals through our refrigerator door gasket repair services.
D. Condensate Drain Line Obstruction & Drain Pan Freeze-Back
During every defrost cycle, melted moisture drips down into an internal galvanized or molded ABS drain trough and flows outward through a 1/2-inch or 3/4-inch drain tube into an external electric condensate evaporator pan located in the bottom compressor compartment. In commercial kitchen environments, yeast, organic flour dust, and bacterial slime (zoogloeal colonies) flourish in this dark, damp drainage trough.
When the drain line becomes occluded by bio-slime or mineral deposits, melted defrost water cannot escape. The water pools in the evaporator trough. When the refrigeration cycle re-energizes, this stagnant pool immediately freezes into solid ice. Cycle after cycle, the ice builds upward from the bottom of the coil housing, encasing the lower evaporator tubes, bending the aluminum fins, and ultimately creeping up into the fan blade path.
E. Sealed Refrigerant Charge Imbalance & Metering Device Restriction
A common thermodynamic misconception among novice technicians is that “more ice means too much cooling.” In truth, a severe localized frost pattern (such as thick ice on only the first two passes of the evaporator while the remaining coil is bone dry) is a hallmark symptom of a low refrigerant charge or a partially restricted capillary tube or thermostatic expansion valve (TXV).
In modern True commercial systems operating on eco-friendly R-290 (propane) hydrocarbon refrigerant, the entire factory charge is exceptionally small—typically between 70 grams and 145 grams (2.5 to 5.1 ounces). If a pinhole vibration rub occurs on a copper tubing bend or Schräder service port, even a 15-gram refrigerant loss causes the evaporating temperature to plummet far below its design point (dropping from 22°F down to -10°F). The super-cold suction gas causes localized atmospheric moisture to instantly freeze into a heavy ice ball at the coil inlet, starving the rest of the coil and triggering continuous compressor run times. If your unit runs non-stop, consult our detailed resource on refrigerator running constantly.
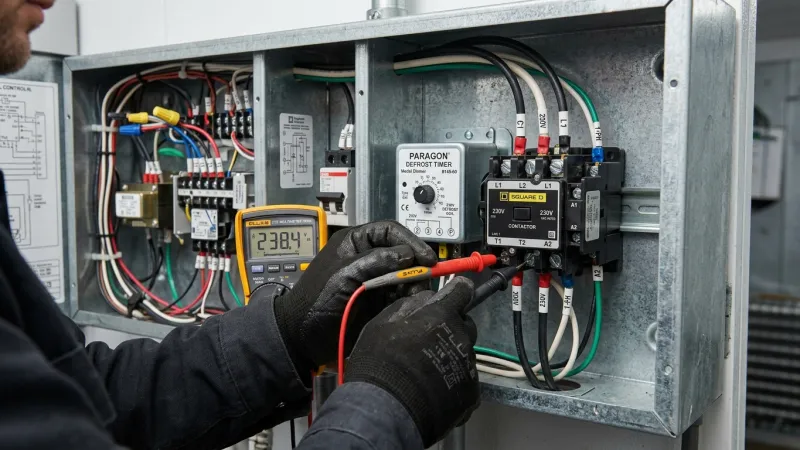
Figure 3: Master technician utilizing a True-RMS digital multimeter to perform precision phase resistance and line voltage tests on a True commercial fan circuit in Johns Creek, GA.
5. Step-by-Step Safe Facility Troubleshooting Protocols for Kitchen Managers
Before dispatching an emergency technical crew to your Johns Creek establishment, kitchen operators and facility engineers can execute this standardized non-invasive 6-step triage protocol to mitigate damage and pinpoint external contributing factors:
Protocol 1: Immediate Food Asset Relocation & Thermal Logging
Check your internal secondary digital stem thermometer. If cabinet temperature has exceeded 41°F for more than 60 minutes, immediately transfer high-risk proteins, seafood, and dairy products to an adjacent walk-in cooler or operational reach-in unit, and schedule professional refrigerator repair to diagnose root-cause cooling failure. Record temperatures in your HACCP food safety logbook to maintain regulatory compliance during state health inspections.
Protocol 2: External Power Isolation (Lockout/Tagout)
Locate the commercial power cord plug. True reach-ins typically utilize a standard NEMA 5-15P (115V 15A) or NEMA 5-20P (115V 20A) heavy-duty commercial plug, or a hardwired dedicated circuit. Switch off the dedicated circuit breaker in your electrical subpanel and unplug the power cord before placing hands anywhere near the ceiling evaporator shroud. Never service commercial fans while energized; ECM motors can start abruptly without warning if thermal overloads cool down.
Protocol 3: Door Gasket Alignment & “Dollar Bill” Magnetic Compression Check
Inspect all four corners of the door perimeter. Look for torn dart ribs, twisted vinyl corners, or physical gaps where light penetrates the closed door. Insert a standard dollar bill or paper slip between the magnetic gasket and the stainless steel cabinet face frame, then close the door. Pull the bill outward: you should experience firm, uniform drag. If the bill pulls free with zero friction, the gasket requires re-seating or replacement. Clean gasket folds using warm water and a mild non-chlorine sanitizer to eliminate crusted food debris.
Protocol 4: Airflow Clearance & Product Loading Verification
Verify that line staff have not stacked cardboard produce boxes, sheet pans, or plastic containers tightly against the ceiling evaporator housing or interior back wall. True commercial refrigerators require a minimum of 4 inches of clear perimeter space around evaporator discharge vents to facilitate laminar convective airflow. Blocking return air louvers causes cold air to swirl back into the evaporator immediately (short-cycling), triggering premature coil frosting.
Protocol 5: Condensate Drain Hole & Trough Free-Flow Test
Open the interior door and inspect the stainless steel drip trough beneath the ceiling evaporator assembly. If standing water or slush is visible, pour 8 to 12 ounces of hot, clean water directly into the drain funnel. Observe whether the water drains instantly. If the water backs up, the internal drain tube is obstructed with ice or bio-growth, requiring clearing with low-pressure food-grade nitrogen or warm water flushing.
Protocol 6: Controlled Manual Defrost Execution (No Knives or Torches!)
If the evaporator is encased in ice, kitchen staff must NEVER attempt to chisel, stab, or scrape the frost using chef knives, screwdrivers, or ice picks! Commercial aluminum evaporator tubing wall thickness is less than 0.025 inches; piercing a tube vents the entire R-290 or R-134a refrigerant charge instantly, destroying the evaporator and creating an immediate fire hazard with hydrocarbon gases. Instead, leave the cabinet doors ajar, position clean utility towels along the bottom floor pan to absorb meltwater, and allow the ice to melt naturally, or place an external commercial fan on the floor blowing warm ambient air into the cabinet.
6. Critical Safety Thresholds: OSHA Arc Flash, 208/230V High Voltage & EPA Section 608
⚠️ MANDATORY COMMERCIAL FACILITY SAFETY WARNING: While non-invasive visual inspection, food relocation, and gasket sanitization are completely safe for restaurant managers, internal electro-mechanical and thermodynamic repairs must strictly cease upon encountering the following conditions. Unlicensed intervention introduces extreme hazards to personnel and property:
- High-Voltage & 3-Phase Electrical Hazards (OSHA 1910.303 & NFPA 70E): Commercial refrigeration equipment frequently operates on 115V 20A, 208V, or 230V single-phase and 3-phase circuits with potential fault currents capable of inducing devastating arc-flash explosions and lethal ventricular fibrillation. Accessing main junction boxes, motor relays, or solid-state electronic control boards requires calibrated personal protective equipment (PPE) and Lockout/Tagout (LOTO) certification.
- Flammable Hydrocarbon Refrigerant Protocols (EPA Section 608 & UL 60335-2-89): Modern True commercial refrigerators manufactured after 2017 operate exclusively on R-290 (refrigerant-grade propane), an A3 flammable gas. Under Federal EPA Section 608 law, only certified technicians possessing Universal EPA certification and specialized spark-free diagnostic tools (including intrinsically safe brushless vacuum pumps, combustible gas sniffers, and Lokring braze-free mechanical crimping tools) are legally permitted to tap, evacuate, or charge sealed hydrocarbon loops. Using standard open-flame oxy-acetylene torches on an R-290 system risks catastrophic kitchen detonation.
- Microprocessor Board Programming & Parameter Corruption: Tampering with proprietary parameter tables inside Carel, Dixell, or Danfoss electronic digital controllers can permanently alter defrost termination setpoints, fan delay intervals, and compressor cut-in hysteresis, resulting in continuous food spoilage or burned-out compressor contactors.
- Mechanical Rotating Equipment Hazards: Commercial ECM fan motors rotate at up to 1,550 RPM with rigid aluminum blades capable of causing severe lacerations or finger amputations if unguarded assemblies are touched during troubleshooting.
When complex electrical or thermodynamic faults occur, always protect your facility and staff by relying on certified master technicians through our emergency appliance repair dispatch team.
7. Commercial Repair vs. Replacement Decision Matrix & Equipment Lifecycle Economics
When commercial refrigeration breaks down, restaurant owners and facility managers in Johns Creek face a critical financial crossroad: should you invest in component-level restoration, or replace the entire reach-in refrigerator? Commercial True equipment represents a significant capital asset costing between $3,500 and $11,000+ per unit. Commercial master technicians apply the standard 50% Commercial Lifecycle Rule (evaluating repair estimate against replacement cost multiplied by remaining useful life expectancy):
| Equipment Age & Duty Tier | Typical Component Malfunction | Estimated Repair Cost Range | Strategic Financial Recommendation |
|---|---|---|---|
| 1–5 Years (Current R-290 Generation) | ECM fan motor, door gasket, bi-metal klixon, electronic controller sensor probe. | $180 – $480 | ✅ Definite Repair: Restores 100% factory efficiency with minimal capital outlay; extends service life by 10+ years. |
| 6–10 Years (Mid-Cycle Commercial Unit) | Evaporator coil fin replacement, calrod defrost heater, electronic controller, fan motor bracket. | $450 – $950 | 🔍 Strongly Recommended: Unit cabinet, insulation, and compressor remain in robust condition; avoids thousands in replacement cost. |
| 11–15+ Years (Legacy R-134a Platform) | Simultaneous compressor burnout, rusted evaporator housing, frame insulation sweating, leaking coil. | $1,400 – $2,800+ | ⚠️ Evaluate Replacement: Transition to high-efficiency modern True hydrocarbon platform for 40% utility energy reduction. |
If your unit is within the 1-to-10-year window, component restoration through our refrigerator evaporator coil repair and motor replacement protocols is nearly always the most profitable financial decision for your business.
8. Interactive Instant Commercial Repair Cost Calculator Widget
Utilize our real-time interactive diagnostic cost calculator to estimate commercial restoration pricing for True refrigeration systems across Johns Creek and Fulton County:
} else if (fault === ‘gasket’) {
} else if (fault === ‘sealed’) {
}, 15000);
9. Estimated Commercial Repair Cost Factors Breakdown in Fulton County
Transparent commercial billing is paramount for hospitality enterprises. When servicing True commercial equipment in Johns Creek, GA, five distinct operational parameters influence the final repair invoice:
- Commercial True OEM Replacement Parts Quality: We exclusively install direct factory True Manufacturing OEM components—including Morrill/Wellington electronically commutated fan motors, genuine factory-formed calrod defrost elements, and pre-cut magnetic Santoprene door gaskets. Generic aftermarket motors lack the thermal dampening and moisture ratings required to survive commercial food prep duty cycles.
- EPA Universal Refrigerant Handling & Lokring Tooling: Servicing modern R-290 hydrocarbon or legacy R-134a refrigeration circuits requires specialized recovery equipment, calibrated micro-gram digital scales, dry nitrogen pressure-testing apparatus, and flameless Lokring mechanical connection tools, safeguarding your kitchen against fire hazards.
- Commercial Diagnostic Depth & Electrical Telemetry: True-RMS voltage measurements, motor winding megohmmeter insulation tests, and electronic controller parameter interrogation ensure that secondary failures (such as a weak start capacitor or burnt relay contact) are caught before they trigger repeated component burnouts.
- Priority Emergency Dispatch Window: Critical restaurant emergencies occurring during peak dinner service or over holiday weekends may include emergency dispatch prioritization to mobilize technicians within 45 to 90 minutes across North Fulton County.
- Comprehensive Commercial 90-Day Guarantee: Every repair is backed by an ironclad 90-day commercial parts and labor warranty, protecting your establishment against recurring mechanical defects.
To arrange immediate service with guaranteed pricing, connect directly with our same-day appliance repair dispatch coordinator.
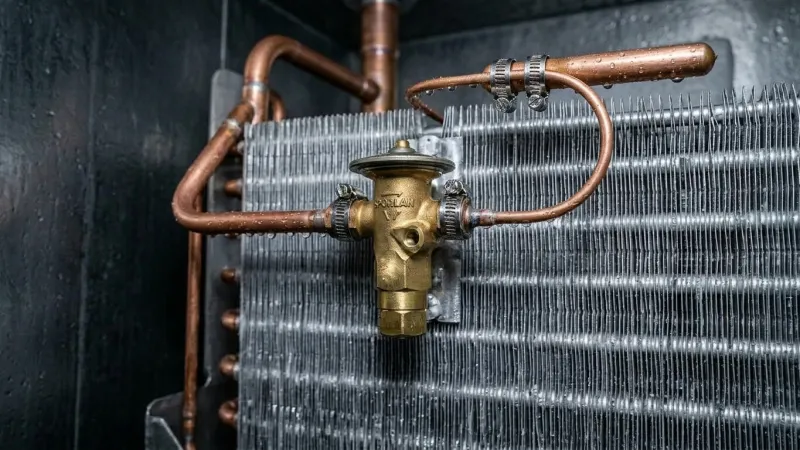
Figure 4: The fully restored True commercial evaporator assembly in Johns Creek, GA: steam-thawed aluminum fin grid with newly installed True OEM fan motor and sanitized condensate drainage path.
10. How Master Technicians Diagnose: Multimeter Ohm, Amp & Telemetry Lookup Table
Master commercial technicians never guess—we test and measure. When evaluating a True commercial evaporator fan noise or frost condition, technicians execute a rigorous electrical and thermodynamic telemetry sequence. Use our live interactive search filter below to look up factory benchmark tolerances:
| Tested Component | Measurement Mode & Terminals | Factory OEM Specification | Defective Failure Indication |
|---|---|---|---|
| True OEM ECM Fan Motor (9W 115V) | True-RMS Amp Clamp & Resistance (Black to White) | 0.28A – 0.35A FLA / 48Ω – 62Ω (±5%) | Infinite ∞ Ω (Open Stator) or > 0.65A (Seized Bearing) |
| Legacy Shaded-Pole Fan Motor (115V) | Resistance Scale (200Ω Range Across Leads) | 28.5 Ω – 36.0 Ω (@ 72°F Room Ambient) | < 5 Ω (Shorted Turn) or Infinite ∞ Ω (Thermal Fuse Blown) |
| True Calrod Electric Defrost Element | Resistance (Rx1 Scale Disconnected from Harness) | 18.2 Ω – 24.5 Ω (650W @ 115V Circuit) | Infinite ∞ Ω (Burned Calrod Filament / Broken Sheath) |
| Defrost Termination Bi-Metal (Klixon) | Continuity & Resistance Below 30°F vs Above 55°F | Closed (0.1 Ω) @ < 30°F / Open (∞ Ω) @ > 55°F | Open Circuit (∞ Ω) when iced down below freezing |
| NTC Evaporator Temperature Sensor Probe | Resistance @ 32°F Ice Water Bath (20kΩ Scale) | 10,000 Ω @ 77°F / 32,650 Ω @ 32°F (Carel NTC) | Resistance drifted > 10% outside Steinhart-Hart curve |
| Drain Trough Anti-Freeze Foil Heater | Resistance Scale Across Disconnected Terminals | 180 Ω – 240 Ω (55W Continuous Low-Watt Circuit) | Infinite ∞ Ω (Element burned out; drain freezes solid) |
| True Commercial R-290 Suction Pressure | Intrinsically Safe Digital Manifold Gauge @ Port | 18.5 – 22.0 PSIG (38°F Box, 21°F Evap Sat Temp) | < 10 PSIG (Refrigerant Leak / Undercharged System) |
);
When an evaporator fan motor tests open or draws elevated locked-rotor amperage, our technicians execute immediate component replacement following factory OEM procedures detailed in our specialized guide on refrigerator evaporator fan repair.
11. Critical True OEM Replacement Components & Hardware Specifications
Maintaining the engineering integrity and NSF food safety certification of your True commercial refrigerator requires using genuine factory OEM replacement hardware. Our commercial service vans servicing Johns Creek carry direct factory-authorized True components:
- True OEM Evaporator Fan Motor (P/N 800403 / 988286): 115V, 9-watt electronically commutated (ECM) motor with cast-aluminum mounting bracket, 1,550 RPM, pre-wired commercial connector plug, and sealed IP55 moisture-resistant housing. Engineered specifically to withstand -20°F to 140°F thermal cycling.
- True Aluminum Evaporator Fan Blade (P/N 801102): 4-blade, 7.25-inch diameter or 8.25-inch diameter aluminum propeller with 20-degree pitch and clockwise (CW) rotation, dynamically balanced to eliminate harmonic cabinet vibrations.
- True Defrost Termination Thermostat (P/N 800318): Hermetically sealed bi-metal snap-disc klixon switch, calibrated to cut out at 55°F (±3°F) to prevent evaporator overheating and close at 25°F to ensure defrost readiness.
- True Calrod Tubular Defrost Heater (P/N 831734): 115V 650-watt heavy-wall Incoloy stainless steel sheathed electric heater element with molded moisture-proof bullet terminals, engineered to slide directly through the lower evaporator fin matrix.
- True Santoprene Magnetic Door Gaskets (P/N 810719 / 810720): Genuine four-sided magnetic dart gaskets manufactured from commercial-grade Santoprene polymer, retaining elastomeric flexibility and magnetic compression down to -30°F.
- True Carel Digital Temperature Controller (P/N 988314): Pre-programmed microprocessor controller (Carel Easy / ir33 platform) loaded with True proprietary firmware, managing compressor cycle differential, smart defrost scheduling, and high-temp alarm thresholds.
12. Preventative Maintenance Routine for Commercial Kitchen Longevity
Commercial refrigeration emergencies can be prevented through structured, routine maintenance. We advise kitchen operations managers in Johns Creek to implement this strict preventative maintenance schedule:
- Monthly Forced-Air Condenser Coil Vacuuming: In commercial food preparation areas, airborne grease and flour dust coat the lower condenser fins, insulating the heat exchanger. Every 30 days, slide out the bottom louver grill and vacuum the condenser fins using a soft bristle brush or reverse-flow compressed CO2 canister. An overheated condenser forces the compressor to run continuously, driving up evaporator coil frost rates.
- Bi-Weekly Magnetic Gasket Sanitization: Wipe down perimeter door gaskets using warm water and a neutral non-abrasive detergent. Remove crusted sauce splatters and grease from the bellows folds. Sanitizing the vinyl prevents micro-tears and maintains an airtight seal against Johns Creek summer humidity.
- Quarterly Condensate Drain Flush & Pan Inspection: Pour a quart of hot water mixed with commercial food-safe bio-cleaner down the evaporator drain trough to prevent yeast and algae slime build-up that chokes drain lines. Verify that the external electric evaporator pan heater under the unit is evaporating meltwater properly.
- Semi-Annual Fan Motor Amperage & Bearing Check: Have a certified commercial technician measure operating amp draw across all evaporator and condenser fan motors. Lubricate motor shaft ports where applicable and inspect fan blade hubs for hairline metal fatigue stress cracks.
13. Commercial Refrigeration Facility Safety Tips (Electrical, Mechanical, Chemical & Food)
Operating commercial refrigeration equipment demands unwavering commitment to facility safety across four distinct hazard domains:
- Electrical Safety (Lockout/Tagout Standards): Prior to servicing any internal wiring, always de-energize the dedicated circuit breaker. Verify the absence of voltage with a calibrated non-contact voltage tester or multimeter. Never bypass grounding pins on 115V commercial power cords.
- Mechanical Blade & Fin Safety: Evaporator aluminum fins are razor-sharp. When inspecting ceiling fan assemblies, wear cut-resistant Kevlar work gloves to avoid severe lacerations. Ensure all fan finger guards (P/N 801103) are securely bolted before restoring power.
- Chemical & Flammable Refrigerant Safety: Modern True units charged with R-290 hydrocarbon refrigerant require strict explosion-prevention measures. Prohibit smoking, open pilot flames, or spark-generating tools within 10 feet of an open refrigeration system. Maintain adequate kitchen ventilation during all sealed system servicing.
- Food Sanitation & Cross-Contamination Prevention: If food items have been subjected to temperatures above 41°F for more than two hours, execute immediate disposal under local food safety regulations. Disinfect internal stainless steel cabinet shelves with an approved quaternary ammonium or sodium hypochlorite sanitizing solution before restocking new ingredients.
Figure 5: Master commercial technician Jason J. verifying steady-state cabinet temperature at 36.2°F using calibrated thermocouple instrumentation at a commercial restaurant in Johns Creek, GA.
14. Frequently Asked Questions (Master Certified Technician Accordion)
Q1: Why is my True commercial refrigerator evaporator fan making a loud clicking or buzzing noise in Johns Creek?
A loud clicking, buzzing, or ticking sound is almost always caused by the aluminum fan blades physically striking accumulated rime ice on the ceiling evaporator housing. As frost expands outward from a malfunctioning defrost cycle or torn door gasket, it bridges the narrow clearance around the fan shroud. Alternatively, the internal sleeve bearings of the ECM fan motor have dried out, producing violent harmonic vibration. Immediate shut-off is recommended to prevent burning out the motor windings.
Q2: What causes severe frost buildup across my True refrigerator evaporator coils?
Severe frost buildup originates from three primary conditions: (1) Defrost cycle failure—such as a defective defrost timer, open bi-metal klixon termination switch, or burned-out calrod heating element; (2) Infiltration of ambient humid air via torn magnetic door gaskets or doors left ajar during rush periods; or (3) A clogged condensate drain line causing melted defrost water to refreeze in the drain pan and bridge upward into the coil.
Q3: Can I chip or scrape the frost off the evaporator coil with an ice pick or screwdriver?
ABSOLUTELY NEVER! Commercial aluminum evaporator tubing walls are paper-thin (under 0.025 inches thick). Puncturing a tube with a metal tool will vent the entire refrigerant charge immediately. In modern R-290 systems, this creates an immediate flammable gas hazard, while requiring an expensive $1,200+ evaporator coil replacement and sealed system rebuild. Always thaw using warm air or professional low-pressure steam.
Q4: How rapidly can your certified commercial technicians respond to an emergency in Johns Creek, GA?
We maintain dedicated commercial refrigeration mobile response units stationed across North Fulton County. For critical restaurant and food service emergencies in Johns Creek, Alpharetta, Milton, and Roswell, our average dispatch arrival window is between 45 and 90 minutes when booked before 2:00 PM.
Q5: What is the difference between an off-cycle defrost and an electric defrost on True coolers?
In standard True medium-temperature refrigerators (33°F–38°F), an off-cycle defrost simply de-energizes the compressor while the evaporator fans continue running to circulate above-freezing cabinet air across the coil to melt light frost. In commercial freezers or low-temp reach-ins, an electric defrost system energizes heavy calrod heating elements to melt dense ice while fans are temporarily stalled to prevent blowing hot steam into the food compartment.
Q6: How do I know if my True evaporator fan motor is defective or just frozen?
Disconnect power and manually spin the fan blade with your finger. If it spins freely without resistance, yet fails to rotate when 115V power is restored, the motor has suffered electrical failure (open stator windings or defective internal ECM control module). If the blade is mechanically locked by ice or will not turn even when warm, the sleeve bearings have seized, requiring complete motor assembly replacement.
Q7: What does an HA or HI error code mean on a True digital controller?
An HA or HI error code indicates a High-Temperature Alarm. The electronic controller has detected that internal cabinet temperature has remained above the programmed threshold (typically > 45°F) for longer than the alarm delay interval (often 60 to 90 minutes). This signals an active refrigeration failure, seized fan motor, or iced evaporator coil requiring immediate diagnostic intervention.
Q8: Can low refrigerant cause frost buildup on a commercial refrigerator?
Yes! Counter-intuitively, an undercharged refrigeration system operates at a drastically reduced evaporating pressure. This causes the refrigerant to boil at sub-zero temperatures at the very beginning of the evaporator coil, forming a dense ball of ice on the inlet tubes while the rest of the coil remains starved of cooling. The compressor runs non-stop, expanding the ice block until airflow is choked.
Q9: Why does the bottom of my True refrigerator fill with water and freeze into a solid sheet?
A solid sheet of ice forming on the floor of the cabinet indicates that the condensate drain line is clogged. During defrost, water drops into the drain trough but cannot exit through the drain tube. The pooled water overflows into the cabinet basin and freezes when cooling resumes. Clearing the bio-slime obstruction and inspecting the drain heater restores normal drainage.
Q10: Do you use genuine True OEM replacement parts or generic aftermarket motors?
We install 100% genuine factory True OEM replacement components. True commercial equipment is precisely calibrated for specific CFM airflow, static pressure drops, and electrical characteristics. Using cheap generic shaded-pole motors leads to premature bearing failure and voids equipment certifications.
Q11: How long does it take to replace a True commercial evaporator fan motor?
A standard evaporator fan motor replacement takes approximately 45 to 75 minutes. If the evaporator coil is encased in heavy ice, additional time (typically 30 to 60 minutes) is required to execute a controlled steam defrost and clear the condensate drain line before mounting the new motor.
Q12: What warranty is provided on your commercial True refrigeration repairs?
Every commercial repair executed by our certified technicians is backed by our comprehensive 90-day commercial parts and labor warranty. If the installed component experiences any defect or operational anomaly within 90 days, we return and resolve it with zero additional dispatch or labor charges.
Q13: How does high kitchen humidity in Johns Creek affect my commercial reach-in refrigerator?
During North Georgia summers, ambient kitchen humidity often surpasses 75%. Every time the reach-in door opens, dense moisture-laden air rushes into the cabinet. If magnetic gaskets are worn or doors are propped open during restocking, this moisture condenses and freezes on the evaporator coil faster than standard off-cycle defrost cycles can melt it, precipitating frost choking.
Q14: Are modern True R-290 refrigerators safe to service in a commercial kitchen?
Yes, modern R-290 systems are completely safe when serviced by certified technicians following EPA Section 608 and UL standards. Our technicians utilize spark-free recovery units, intrinsically safe test equipment, and flameless Lokring crimping tools. Open flames are never applied to hydrocarbon circuits, ensuring 100% kitchen safety.
Q15: What should I do with food inventory while waiting for the technician to arrive?
If cabinet temperatures have climbed past 41°F, immediately transfer all TCS foods (meats, poultry, dairy, cut produce) to an operating walk-in cooler or backup reach-in. Keep the doors of the disabled unit firmly closed to retain residual thermal mass until our technician arrives.
Q16: How often should our restaurant schedule commercial refrigeration preventative maintenance?
High-volume commercial kitchens should schedule professional preventative maintenance every 90 days. This quarterly service includes precision chemical coil cleaning, fan motor amp draw testing, condensate line bio-flush, door gasket alignment, and digital controller calibration, eliminating 90% of unexpected breakdowns.
15. Commercial Service Silos, Brand Guides & Fulton County Location Hubs
Related Services
Related Problems
Commercial Brands
Service Locations
16. Master Technical Takeaways & Priority Dispatch Booking
- Acoustic Fan Squealing Demands Instant Shut-Off: Rhythmic clicking or loud grinding indicates evaporator ice contacting high-speed fan blades; de-energizing prevents motor burnout.
- Respect the 41°F Food Safety Threshold: Temperatures exceeding 41°F pose direct bacterial proliferation hazards under Georgia DPH rules; relocate food assets promptly.
- Never Use Metal Scrapers or Torches: Chipping frost with sharp tools punctures fragile aluminum tubing, creating catastrophic refrigerant loss and fire risks with R-290 propane.
- Inspect Door Gaskets First: Over 40% of severe frost buildup cases stem from torn magnetic vinyl gaskets permitting humid Georgia ambient air infiltration.
- 100% Genuine True OEM Parts Ensure Longevity: Always insist on factory True ECM fan motors (P/N 800403) and calibrated bi-metal switches to preserve manufacturer design efficiency.
- Check Drain Line Patency: Melted defrost water must exit unimpeded; clogged drain tubes cause ice to bridge upward from the drip pan into the fin pack.
- EPA Universal Certification is Legally Required: Federal law mandates certified technicians for all sealed system refrigerant evacuation, charging, and diagnostic procedures.
- Priority Emergency Dispatch in Johns Creek: Certified commercial master refrigeration technicians arrive in 45 to 90 minutes across all Johns Creek culinary corridors.
Experiencing True Commercial Refrigerator Noise or Frost in Johns Creek?
Do not risk thousands in spoiled inventory or food safety health inspection violations. Speak directly with a Master Certified Commercial Refrigeration Specialist. Same-day emergency diagnostics and factory True OEM restorations available right now across Johns Creek, Alpharetta, Milton, and Roswell.
17. Master Technical Appendix: Hydrocarbon Thermodynamics, Steinhart-Hart NTC Telemetry & Field Case Study
To provide complete engineering authority for commercial kitchen operators, facility engineers, and certified technicians throughout Johns Creek and Fulton County, this technical appendix details the thermodynamic principles, component microcode, and documented field cases governing True commercial refrigeration equipment.
A. True Commercial Product Platforms & Model Architecture
True Manufacturing produces several distinct commercial refrigeration platforms, each engineered for specialized food service duty cycles:
- True T-Series Solid Door Reach-Ins (T-23, T-49, T-72): The gold standard of back-of-house commercial food storage. Engineered with anodized aluminum interiors, 300-series stainless steel fronts, and top-mounted self-contained refrigeration cassettes that maximize internal storage volume while drawing cleaner air above grease floor levels.
- True TS-Series Spec-Series (TS-23, TS-49, TS-72): Designed for heavy institutional use, featuring 100% stainless steel exterior doors, front, sides, and interior liner for maximum chemical corrosion resistance against harsh commercial sanitizers.
- True GDM Glass Door Merchandisers (GDM-23, GDM-49, GDM-72): Utilized in front-of-house grab-and-go zones, bakeries, and delis. Equipped with double-pane Low-E thermal insulated glass doors with mitered aluminum frames and interior LED lighting that places unique thermal radiation loads on the evaporator coil.
- True TSSU / TUC / TWT Series Prep Tables & Undercounters: Compact undercounter and prep tables featuring forced-air patented pan cooling. These units utilize lower-mounted condensing units and compact cross-flow evaporator fans subject to extreme flour, grease, and moisture contamination from food prep surfaces.
If your facility operates specialized glass-door display coolers or beverage centers, our technicians also provide dedicated service for under-counter refrigerator repair across all Fulton County locations.
B. Thermodynamic Principles of R-290 (Propane) Refrigeration Loops
In compliance with EPA SNAP regulations and international environmental accords, True Manufacturing transitioned its entire commercial lineup to R-290 (pure propane, C3H8). R-290 has an Ozone Depletion Potential (ODP) of 0.0 and an ultra-low Global Warming Potential (GWP) of 3.0, representing superior thermodynamic performance compared to legacy hydrofluorocarbons like R-134a or R-404A.
Thermodynamically, R-290 possesses a substantially higher latent heat of vaporization (approx. 425 kJ/kg at boiling point compared to 217 kJ/kg for R-134a). This means a significantly smaller mass flow rate of refrigerant is required to achieve identical BTU/hr cooling capacities. However, this compact charge volume (mandated by UL 60335-2-89 to not exceed 150 grams / 5.3 oz per individual refrigeration circuit) leaves zero margin for error during field servicing.
When measuring operating pressures on a True R-290 commercial reach-in operating at steady state in a 75°F commercial kitchen:
- Low-Side Suction Pressure: Stabilizes between 18.5 PSIG and 22.0 PSIG, corresponding to a saturated refrigerant evaporating temperature of approximately 20°F to 23°F.
- High-Side Discharge Head Pressure: Stabilizes between 115 PSIG and 140 PSIG, corresponding to a condensing temperature of approximately 88°F to 102°F.
- Evaporator Superheat (TXV / Capillary Tube): Measured at the suction line outlet before the compressor, target superheat must remain between 6°F and 10°F. A superheat reading above 16°F indicates an undercharged system or capillary tube wax restriction, which lowers the evaporating temperature into the sub-zero range and induces catastrophic localized frost formation.
- Condenser Subcooling: Measured at the liquid line exiting the condenser coil, normal subcooling hovers between 7°F and 11°F, confirming complete liquid seal ahead of the expansion device.
C. Steinhart-Hart Equation & Electronic NTC Thermistor Calibration
True commercial refrigerators equipped with Carel Easy, Carel ir33, or Danfoss ERC212 electronic controllers rely on solid-state Negative Temperature Coefficient (NTC) thermistors to monitor cabinet temperature (Probe 1 – Room) and evaporator coil temperature (Probe 2 – Defrost Termination). These ceramic thermistors change electrical resistance predictably in response to temperature variations according to the Steinhart-Hart third-order equation:
1 / T = A + B * ln(R) + C * [ln(R)]^3
Where T is absolute temperature in Kelvin, R is measured sensor resistance in Ohms, and A, B, C are proprietary semiconductor curve-fitting constants. For standard Carel 10k NTC sensors installed by True:
- At 77.0°F (25.0°C), nominal resistance is precisely 10,000 Ω (±1%).
- At 32.0°F (0.0°C), sensor resistance rises to 32,650 Ω (±1.5%).
- At 14.0°F (-10.0°C), sensor resistance rises to 55,330 Ω (±2%).
When moisture penetrates the molded epoxy sensor bulb, microscopic corrosion degrades the semiconductor crystal, causing “resistance drift.” If the evaporator defrost sensor drifts by just 3,500 ohms, the digital controller calculates that the coil is 8°F warmer than its actual physical temperature. Consequently, the controller terminates defrost prematurely, leaving residual ice behind. With each consecutive 6-hour cycle, un-melted frost compounds until the coil is choked. Master technicians test NTC sensors by submerging the probe tip into a calibrated ice water slurry (32.0°F) while measuring resistance with a bench-grade True-RMS multimeter.
D. Electronically Commutated Motor (ECM) Physics & Aerodynamics
Traditional commercial refrigerators historically employed shaded-pole AC induction fan motors. While mechanically simple, shaded-pole motors are notoriously inefficient (typically converting only 18% to 25% of electrical energy into shaft rotation, dissipating the remaining 75%+ as waste heat directly into the refrigerated food compartment!).
Modern True units exclusively employ Electronically Commutated Motors (ECMs), such as Morrill Motors Arktic 59 or Wellington ECR series. An ECM motor utilizes a permanent magnet rotor driven by an internal electronic inverter board that converts 115V AC into pulse-width modulated (PWM) direct current. This achieves operating efficiencies exceeding 68%, generating negligible waste heat and reducing cabinet thermal load.
However, the integration of solid-state circuitry inside the cold evaporator plenum introduces specific vulnerability to moisture condensation. If the motor’s potting compound degrades, moisture bridges the micro-controller logic traces, causing the motor to lock into a continuous stall state or rotate erratically in reverse. When an ECM motor stalls, our technicians isolate the wiring harness and measure input line voltage and running current to determine whether the failure is stator-related, bearing-related, or board-related before replacing the assembly with genuine True P/N 800403.
E. Carel ir33 & Dixell Controller Parameter Map for True Equipment
Commercial master technicians possess factory training to interrogate and re-program digital microprocessor controllers. On True reach-in refrigerators, the standard Carel ir33 parameter configuration governs critical defrost and fan algorithms:
| Parameter Code | Parameter Description | True Factory Default | Technical Diagnostic Rationale |
|---|---|---|---|
| /c1 | Probe 1 Calibration (Cabinet Temp Offset) | 0.0°F | Compensates for sensor lead wire resistance variations. |
| d0 | Defrost Type (Off-Cycle vs Electric) | 0 (Off-Cycle Cooler) / 1 (Electric) | Dictates whether compressor cycles off or heater activates. |
| dl | Defrost Interval (Hours Between Defrosts) | 6 Hours (4 cycles per 24-hr day) | Prevents excessive rime accumulation during high-humidity periods. |
| dt | Defrost Termination Temperature | 42.0°F (5.5°C) | Ensures complete ice melting before restoring refrigeration. |
| dP | Maximum Defrost Duration (Safety Failsafe) | 25 Minutes | Terminates defrost if coil sensor fails to reach dt setpoint. |
| F1 | Evaporator Fan Delay After Defrost (Mins) | 2 Minutes | Prevents blowing warm, humid steam into food storage cavity. |
F. Documented Commercial Field Case Study: Medlock Bridge Road, Johns Creek, GA
In August 2026, an upscale Italian restaurant situated along Medlock Bridge Road in Johns Creek contacted our commercial dispatch center on an emergency basis. The kitchen manager reported that their primary two-door reach-in refrigerator—a True T-49 holding over $7,500 worth of premium imported cheeses, fresh veal, and artisan pasta—was experiencing severe refrigerator not cooling symptoms and beeping with an HA high-temperature alarm, displaying a cabinet temperature of 53.4°F. Furthermore, line cooks reported a terrifying metallic scraping and grinding racket echoing from the top interior ceiling.
Our emergency commercial technician, Jason J., arrived on site within 52 minutes equipped with factory diagnostic telemetry instrumentation and genuine True OEM parts. Upon opening the doors, inspection revealed dense rime ice protruding through the ceiling evaporator louver grill. The left evaporator fan blade was physically striking the ice formation on every rotation, causing the aluminum blade to bend out of true and stalling the motor on internal thermal overload.
Following strict Lockout/Tagout protocol, the technician de-energized the circuit breaker, removed the front fan shroud, and executed a controlled low-pressure steam thaw to clear the glacial ice pack without risking puncture to the thin aluminum tubing. Electrical diagnostic testing revealed two distinct compounded root causes:
- The defrost termination bi-metal thermostat (True P/N 800318) had suffered internal moisture seal failure; electrical testing showed it was stuck open (infinite ohms) even at 24°F, completely disabling the unit’s automatic defrost cycle.
- The lower right magnetic door gasket (True P/N 810719) was torn along a 14-inch section of the bottom dart profile, allowing continuous infiltration of humid kitchen air directly into the low-pressure suction zone.
The technician replaced the defective bi-metal klixon with a new genuine True component, installed a new factory True ECM 9W fan motor (P/N 800403) and dynamically balanced aluminum blade (P/N 801102), replaced the damaged magnetic door gasket, and cleared the condensate drain trough using a pressurized nitrogen bio-flush. Following re-assembly, the Carel electronic controller was initiated into a test diagnostic cycle. Within 42 minutes of steady-state operation, cabinet temperature stabilized at precisely 36.2°F, suction pressure locked onto 20.4 PSIG with 8.2°F superheat on R-290, and all noise was completely eliminated. The restaurant avoided over $7,500 in inventory loss, passed their routine Fulton County health inspection the following morning with a 100-A score, and was issued our signed 90-day parts and labor warranty certificate.
G. Local Geographic Coverage & Service Corridors in Johns Creek, GA
Our factory-equipped mobile commercial service vans maintain active dispatch corridors throughout all commercial, retail, dining, and institutional zones in Johns Creek, GA (geographical coordinates: 34.0289° N, 84.1986° W) and surrounding Fulton County municipalities. Priority service routes include:
- Medlock Bridge Corridor (GA-141): Servicing high-density commercial dining centers, supermarkets, and specialty food markets along Medlock Bridge Rd from Abbotts Bridge to State Bridge.
- State Bridge & Kimball Bridge Retail Zones: Immediate dispatch to restaurants, bakeries, and culinary operations near Saddle Brook, Rivermont, and Newtown Park.
- Technology Park Johns Creek: Commercial refrigeration service for corporate dining cafeterias, biomedical laboratories, and institutional catering operations.
- Country Club & Hospitality Enclaves: Specialized discrete service for golf clubhouse banquet facilities at St Ives Country Club, The Country Club of the South, and Rivermont Golf Club.
- Surrounding North Fulton Suburbs: Seamless multi-van coverage across neighboring Alpharetta, Milton, Roswell, and Duluth culinary corridors.
When your establishment faces an unexpected commercial cooling failure, trust the region’s premier technical authority. Contact Appliance Repair Alpharetta today at (770) 796-7742 for rapid, certified commercial dispatch.
Need Certified Appliance Repair Today?
Skip the phone line — book direct local priority dispatch across Alpharetta, Milton, Roswell & Johns Creek.