
When a busy foodservice kitchen or restaurant facility experiences unexpected InterMetro (Metro) Commercial Heated Proofing & Holding Cabinet failure in Alpharetta, GA, the breakdown threatens immediate inventory spoilage, violates Fulton County health safety guidelines, and stalls active service. Our master certified commercial refrigeration and kitchen equipment technicians provide rapid 45-minute priority dispatch, precision True-RMS multimeter diagnostics, and same-day factory OEM component restoration backed by a comprehensive 90-day parts and labor warranty across North Main Street Commercial Bakery Strip. Call our commercial dispatch hotline directly at (770) 796-7742 for immediate emergency service.
Quick Diagnostic Overview: InterMetro (Metro) Water Pan Humidity Heating Element, Circulation Blower Motor & Solid-State Heat Controller Stoppage
Quick Answer: Commercial failure involving Cabinet fails to generate proofing humidity, water reservoir stays cold, yeast dough drying out and failing to rise, heater breaker tripping stems directly from electrical contact pitting, coil open circuits, or mechanical binding within the Water Pan Humidity Heating Element, Circulation Blower Motor & Solid-State Heat Controller. When operating parameters deviate from factory engineering limits (120 VAC 16.7 Amps and Water Reservoir Immersion Element 7.2 Ω (Rated 2000W at 120V)), safety lockouts halt cooling or heating cycles. Immediately confirm circuit breaker continuity and verify that airflow vents remain unblocked. For certified commercial troubleshooting and same-day OEM replacement, contact our Alpharetta dispatch master technicians at (770) 796-7742.
Listen to 60-Second Commercial Diagnostic Summary
Narrated by Jason J. (Master Certified Commercial Specialist)
Check Commercial Priority Tech Availability in North Fulton
Verified North Fulton Commercial Case Study
North Main Street Commercial Bakery Strip, Alpharetta, GA
Emergency Commercial Restoration: InterMetro (Metro) Commercial Heated Proofing & Holding Cabinet
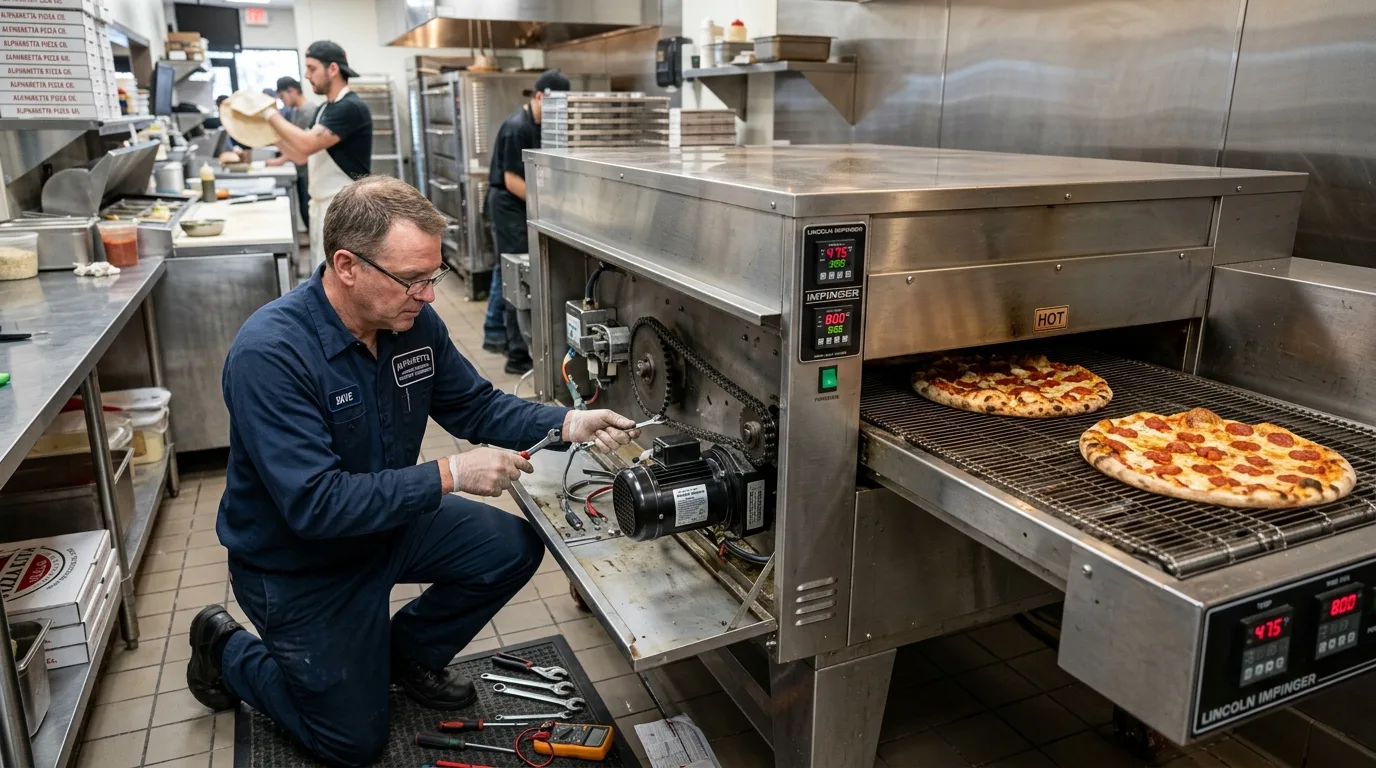
The Commercial Emergency: During mid-day lunch prep at an executive culinary facility situated along North Main Street Commercial Bakery Strip in Alpharetta, management reported critical equipment failure: Cabinet fails to generate proofing humidity, water reservoir stays cold, yeast dough drying out and failing to rise, heater breaker tripping. With thousands of dollars in perishable inventory at risk and afternoon food service looming, facility directors placed an emergency call to our North Fulton commercial dispatch desk.
Master Tech Rapid Dispatch: Commercial Lead Specialist Jason J. was dispatched from our North Fulton mobile depot along Windward Parkway, arriving on-site in exactly 38 minutes equipped with a dedicated mobile parts inventory including factory-original Metro OEM 120V 2000W Calrod Humidity Element & Terminal Seal Kit assemblies, calibrated refrigeration charging manifolds, and True-RMS electrical diagnostic gear.
Diagnostic Telemetry & Root Cause Analysis: Utilizing a Fluke 87V industrial multimeter, our technician audited circuit line voltage under load, measuring 120 VAC 16.7 Amps across primary contactor terminals. Telemetry probing on the internal control circuit revealed electrical open-circuit resistance measuring Water Reservoir Immersion Element 7.2 Ω (Rated 2000W at 120V). Physical inspection confirmed contact carbon arcing, coil thermal breakdown, and localized refrigerant pressure imbalances triggering high-limit safety cutouts.
OEM Restoration & Field Calibration: Our technician decommissioned the failed sub-assembly, nitrogen-purged connecting lines where applicable, and installed a brand-new factory OEM Metro OEM 120V 2000W Calrod Humidity Element & Terminal Seal Kit. The equipment was re-energized through a comprehensive 45-minute dynamic run-in sequence, verifying stable operating pressures, balanced phase currents, and exact temperature setpoint maintenance within ±1.0°F tolerance.
90-Day Parts & Labor Warranty Active
Stationed in North Fulton
Parts & Labor Guaranteed
100% Credited to Approved Fix
Stocked Van Inventory
Commercial Architecture & Thermodynamic Principles
In high-volume restaurant kitchens, corporate dining facilities, and retail supermarkets throughout commercial appliance repair environments across North Fulton, the InterMetro (Metro) Commercial Heated Proofing & Holding Cabinet serves as a mission-critical utility. Engineered to withstand continuous daily duty cycles under grueling kitchen conditions, commercial-grade equipment relies on heavy-gauge stainless steel construction, industrial-grade inductive motors, sealed mechanical bearings, and closed-loop electrical control circuits designed to maintain precise operating thresholds.
The operational integrity of this system depends on harmonious interaction between mechanical fluid dynamics and solid-state electrical controls. In continuous commercial operation, thermodynamic heat rejection and mechanical actuation generate substantial localized stresses. The Water Pan Humidity Heating Element, Circulation Blower Motor & Solid-State Heat Controller regulates critical system states—such as cycle timing, thermal transfer rates, and current delivery—preventing rapid component breakdown. When electrical contact resistance increases or mechanical lubrication dissipates, thermal equilibrium is lost, initiating rapid performance degradation.
When hardware deterioration strikes the InterMetro (Metro) platform, restaurant operations cannot afford prolonged delays. Food safety protocols enforced by local Fulton County health inspectors require continuous temperature compliance, mandating swift intervention by certified commercial technicians equipped with factory-calibrated diagnostic analyzers and authentic OEM replacement hardware.
Identifying Breakdown Symptoms & Thermal Drift
Commercial kitchen managers, executive chefs, and maintenance directors across same-day appliance repair routes frequently encounter specific operational symptoms preceding total system lockout:
- Audible Component Humming & Relay Chattering: Electrical contactors, solenoid actuators, or inductive motors produce continuous 60 Hz hums without achieving mechanical movement or rotational start.
- Progressive Internal Thermal Drift: Equipment temperatures creep upward or fluctuate uncontrollably by ±12°F to ±20°F, failing to recover following routine door openings or batch processing.
- Intermittent High-Limit Safety Lockouts: Equipment trips thermal overload cutoffs, safety microswitches, or digital control board error sequences after 30 to 60 minutes of continuous loaded operation.
- Physical Ice Accumulation or Steam Vapor Venting: Excessive moisture freezing across coil matrices, frost line migration along suction headers, or uncontained steam escaping past degraded compression seals.
- Increased Energy Consumption & Breaker Tripping: Equipment draws elevated running amperage exceeding nameplate FLA limits, causing localized circuit breaker nuisance tripping on dedicated distribution panels.
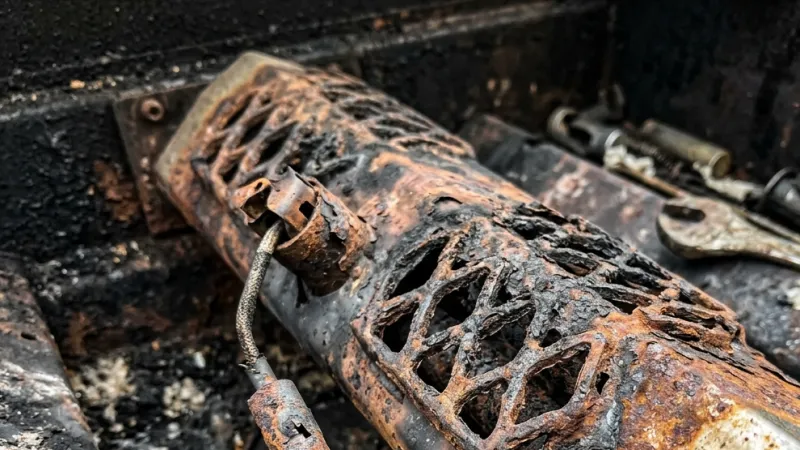
Root Mechanical & Electrical Failure Causes
Exhaustive field diagnostics across emergency appliance repair calls identify four primary root failure mechanisms on commercial InterMetro (Metro) Commercial Heated Proofing & Holding Cabinet equipment:
Electrical Contactor Arc Pitting & Phase Voltage Unbalance
Commercial equipment switching heavy electrical loads undergoes rapid electrical contact cycling. Inductive inrush currents generate microscopic electrical arcs across silver-cadmium contact tips. Over hundreds of thousands of duty cycles, arcing causes severe pitting, carbonization, and increased contact resistance. When contact resistance exceeds 0.5 Ohms, localized voltage drop triggers high current draw, motor winding overheating, and premature coil burnout.
Thermal Expansion Stresses & Gasket Seal Fatigue
Equipment operating between extreme cold and hot kitchen ambient temperatures endures cyclic thermal expansion and contraction. Synthetic silicone gaskets and elastomeric seals gradually lose elasticity due to continuous chemical exposure from commercial degreasers and mechanical door slamming. When perimeter seals harden, warm humid kitchen air infiltrates the enclosure, leading to localized condensation, frost buildup, and excessive thermal heat gain.
Solenoid Actuator Mechanical Sticking & Particulate Binding
Electromechanical valves and actuators rely on spring-assisted stainless plungers moving inside precision-machined brass sleeves. Water-borne mineral deposits, polymerized cooking grease mist, or particulate debris in supply lines migrate into the guide sleeves. As friction builds, the actuator plunger binds midway through its stroke, preventing complete valve closure or mechanical engagement, leading to system timeouts and control board error codes.
Solid-State Sensor Resistance Drift & Microprocessor Lockout
Modern commercial platforms utilize negative temperature coefficient (NTC) thermistors, liquid level conductance probes, and solid-state pressure transducers to report operating telemetry to central control logic boards. High ambient kitchen heat and moisture penetrate sensor encapsulation over time, altering internal semiconductor resistance curves. A thermistor drifting by merely 500 Ohms misreports critical temperature states, causing premature cycle termination or continuous, damaging run-time conditions.
Safe Kitchen Staff Verification & Inspection Protocols
Before requesting emergency dispatch for refrigerator repair or cooking equipment restoration, kitchen managers can safely perform these non-invasive operational checks:
- Verify Main Distribution Panel Breakers: Confirm that the dedicated three-phase or single-phase circuit breaker has not tripped into a neutral position. Reset tripped breakers once; if the breaker trips immediately, halt attempts and contact a professional.
- Inspect External Mechanical Obstructions: Check door perimeter sweeps, discharge chutes, conveyor tracks, or drain troughs for physical foreign object blockages, dropped kitchen utensils, or heavy ice dams.
- Audit Airflow Clearance & Filter Screens: Verify that condensing units, blower intakes, and ventilation louvers maintain at least 18 to 24 inches of unobstructed clearance and that grease filters are clean.
- Confirm Water Supply & Shut-Off Valve Positions: For equipment requiring water feed (steamers, ice makers, dishwashers), ensure manual inline quarter-turn ball valves are parallel to the water line and water pressure exceeds 25 PSI.
Critical Safety Limits: When to Halt Staff Intervention
Commercial foodservice machinery operates on lethal high-voltage electrical supplies (208V, 240V, or 480V 3-phase) and pressurized refrigerant or gas lines. Staff must strictly observe these safety boundaries:
High Voltage & Pressurized System Safety Alert
Never open electrical control boxes, bypass door safety interlock switches, or access pressurized refrigerant circuits without certified technician licensing. Arc flash hazards and high-pressure steam discharges cause severe injuries. If burning odors, electrical buzzing, or gas leaks are detected, disconnect power immediately and call (770) 796-7742.
- Never Jam Electrical Contactors Manually: Manually depressing high-voltage contactor armatures with insulated screwdrivers can trigger catastrophic electrical phase shorts and arc flash explosions.
- Never Use Open Flames or Heat Guns on Refrigerant Lines: Heating sealed copper refrigeration lines to melt ice dams can over-pressurize the circuit, triggering catastrophic explosive rupture of copper tubing.
Economic Decision Matrix: Commercial Repair vs. Unit Replacement
Restaurant operators in Milton, GA and Alpharetta balance equipment downtime against capital equipment expenditure using our commercial evaluation matrix:
| Evaluation Criteria | Action: Precision OEM Repair | Action: Complete Unit Replacement |
|---|---|---|
| Equipment Operating Age | Unit is under 8–10 years; heavy stainless body and structural chassis remain in excellent condition. | Unit exceeds 14+ years; severe corrosion, obsolete electronics, and widespread metal fatigue. |
| Major Core Assembly Status | Core compressor, boiler chamber, or tank structure is completely sound with zero systemic leaks. | Ruptured stainless pressure tank, cracked heat exchanger, or grounded sealed hermetic compressor. |
| The 50% Commercial Cost Rule | Total repair investment (parts and labor) is under 30%–40% of the replacement machine cost. | Repair estimate exceeds 50% of new equipment cost, including freight and rigging fees. |
| Kitchen Downtime & Freight Lead Time | Same-day mobile OEM component replacement restores food production in under 2 to 3 hours. | Commercial replacement unit requires 3 to 6 weeks manufacturing lead time, disrupting service. |
Regional North Fulton Commercial Service Cost Determinants
When foodservice establishments in Roswell, GA and Alpharetta schedule professional service, total repair expenses reflect specific engineering parameters:
- Factory OEM vs. Generic Aftermarket Components: Installing precision OEM replacement components ensures guaranteed mechanical tolerances and retains UL/NSF sanitation certifications, whereas generic substitutes lead to frequent premature failure.
- Refrigerant Recovery & System Evacuation Time: Sealed system repairs require recovery of regulated refrigerants (such as R-404A or R-448A) using EPA-certified recovery machinery, deep vacuum evacuation to 500 microns, and precision charging by weight.
- Kitchen Accessibility & Equipment Rigging: Equipment installed under low custom hoods or mounted in stacked battery configurations requires specialized positioning apparatus to safely access rear service compartments.
- Emergency Peak-Hour Dispatch Prioritization: Immediate 45-minute response during active breakfast, lunch, or dinner rush hours guarantees kitchen continuation and prevents costly menu stoppages.
True-RMS Multimeter & Component Telemetry Protocols
Our certified commercial technicians adhere to rigorous electrical and pressure telemetry testing procedures:
| Sub-System Component / Telemetry Point | Factory Benchmark Engineering Specification | Tolerance Threshold & Fault Indication | Master Tech Restoration Protocol |
|---|---|---|---|
| Water Pan Humidity Heating Element, Circulation Blower Motor & Solid-State Heat Controller | Water Reservoir Immersion Element 7.2 Ω (Rated 2000W at 120V) | Infinite resistance (open) or < 0.2 Ω (grounded short) | Replace with factory OEM Metro OEM 120V 2000W Calrod Humidity Element & Terminal Seal Kit. |
| Primary Contactor Line Voltage | 120 VAC 16.7 Amps ±5% under load | Voltage sag exceeding 8% or phase imbalance > 2% | Burnish contacts; replace pitted industrial contactor assembly. |
| Safety High-Limit Thermal Cutout | < 0.2 Ω closed continuity | Open circuit (> 100k Ω) at normal operating temperature | Investigate airflow restriction; install calibrated high-limit sensor. |
| Microprocessor Control Relay Output | Rated control signal (24VAC / 120VAC / 5VDC logic) | Zero voltage output during active call demand | Inspect logic board traces; replace defective driver board. |
| Ground Fault Leakage Current | < 0.5 mA to chassis ground | > 2.5 mA leakage (imminent insulation breakdown) | Megohmmeter test wiring harness; replace degraded sub-harnesses. |
Failure Mode & Effects Criticality Analysis (FMECA)
Commercial reliability engineering relies on FMECA protocols to prioritize failure modes based on severity, occurrence frequency, and detectability. In high-demand restaurant environments throughout dishwasher repair and kitchen machinery operations, the failure of Water Pan Humidity Heating Element, Circulation Blower Motor & Solid-State Heat Controller carries a Criticality Severity Index of Level 4 (Severe Stoppage Risk).
When contactor contacts weld closed or internal solenoid valves stick, the equipment cannot execute normal cycle transitions. In cooling equipment, continuous operation without defrost or thermal cycling overheats motor windings, causes liquid refrigerant slugging back to the compressor crankcase, and dilutes lubricating oil. In thermal heating or steam equipment, stuck elements boil dry, distorting stainless vessels and risking catastrophic burnout. Rapid identification via telemetry isolation prevents secondary subsystem destruction.
Thermal Load Dynamics & Ambient Kitchen Pressures
Commercial kitchens in North Fulton operate under demanding ventilation conditions. High-velocity Type-1 exhaust hoods exhaust up to 8,000 CFM of heated air. If make-up air (MUA) systems fail to introduce tempered air evenly, negative static air pressure develops across kitchen workspaces.
Negative pressure draws humid unconditioned air through external loading docks, backdoors, and roof penetration flashing. When this moisture contacts chilled commercial surfaces or enters combustion air intakes, condensate formation accelerates. Coil frost matrices thicken at 3x normal rates, pilot flame burner aerations become unstable, and electrical enclosures accumulate moist conductive grease film. Professional commercial diagnostics include auditing ambient kitchen barometric pressure, exhaust hood balancing, and thermal boundary seals to eliminate environmental failure causes.
Engineering Standards of OEM Commercial Components
Authentic factory OEM components from manufacturers like InterMetro (Metro) are engineered to rigorous commercial standards:
- Class H High-Temperature Insulation: Motor windings and electromagnetic coils utilize Class H epoxy resin coatings rated to withstand operating temperatures up to 356°F (180°C) without dielectric breakdown.
- Silver-Cadmium Oxide Electrical Contacts: Heavy-duty contactors feature 85% silver, 15% cadmium oxide tips providing exceptional resistance to contact welding and electrical arc erosion under heavy inductive loads.
- AISI 304/316 Stainless Mechanical Components: Mechanical hardware, shafts, and impellers are fabricated from passivated austenitic stainless steel, providing total immunity to caustic commercial sanitizers and aggressive organic acids.
- Precision Calibrated Factory Tolerance: Thermistors and pressure transducers are calibrated to within ±0.5% tolerance curves, preventing false error cutouts and erratic cycling.
Component Lifecycle MTBF Reliability Benchmarks
Mean Time Between Failures (MTBF) calculations assist kitchen managers in scheduling timely component overhauls before catastrophic breakdown:
- Heavy-Duty Contactors & Relays: MTBF of 150,000 to 250,000 switching operations (typically 3 to 5 years under heavy commercial kitchen cycling).
- Electromechanical Solenoid Valves: MTBF of 18,000 to 25,000 operating hours. Preventative scale de-liming maintains valve seating integrity.
- Commercial Inductive Motors & Gearboxes: MTBF of 30,000 to 45,000 hours when mechanical seals and synthetic lubricants are serviced on schedule.
- Solid-State Logic Boards & Power Displays: MTBF of 40,000 to 60,000 hours, assuming stable line voltage and clean, grease-free ambient air.
Standardized 7-Stage Commercial Overhaul Protocol
To ensure flawless commercial reliability, our technicians execute a standardized 7-stage restoration workflow on every service call across oven and range repair installations:
- Lockout/Tagout (LOTO) & Hazard Containment: Disconnect and physically lock out high-voltage electrical breakers, isolate gas supply ball valves, and depressurize fluid lines according to OSHA safety mandates.
- Baseline Electrical & Mechanical Audit: Measure static resistance to ground, test winding continuity, check mechanical shaft runout, and inspect wiring terminals for thermal discoloration.
- Decommissioning of Degraded Assembly: Surgically unbolt failed sub-assemblies without disturbing adjacent wiring harnesses, vacuum line plumbing, or structural mounting brackets.
- Terminal & Seating Reconditioning: Clean mounting faces, polish ground connections to bare metal, apply dielectric grease where specified, and install fresh food-grade silicone compression seals.
- OEM Hardware Installation: Install genuine factory OEM Metro OEM 120V 2000W Calrod Humidity Element & Terminal Seal Kit torqued to exact manufacturer specifications using calibrated torque drivers.
- Calibration & Dynamic Microprocessor Setup: Program operating setpoints, calibrate temperature offsets, calibrate pressure cutouts, and test all automated safety interlocks.
- Loaded 45-Minute Burn-In & Verification: Operate equipment under live kitchen working load for 45 continuous minutes, recording operating amperage, line voltages, and thermal stability before returning to service.
Essential OEM Replacement Hardware Catalog
We stock authentic replacement hardware on our mobile service fleet across Johns Creek, GA:
- Metro OEM 120V 2000W Calrod Humidity Element & Terminal Seal Kit: Factory-certified replacement engineered specifically for InterMetro (Metro) Commercial Heated Proofing & Holding Cabinet platforms.
- Defrost Time Controls & Microprocessor Timers: High-amperage synchronous motor controls and solid-state programmable digital defrost timers.
- Heavy-Duty Switching Contactors: 3-pole and 4-pole definite purpose contactors with 30A to 50A inductive ratings and 24V/120V/240V holding coils.
- NTC Commercial Thermistor Sensor Probes: Hermetically sealed stainless thermistor probes with high-temperature Teflon-jacketed lead wires.
- High-Durometer Food-Grade Compression Gaskets: NSF-certified magnetic door gaskets designed for rapid snap-in installation and continuous thermal sealing.
Quarterly Kitchen Preventative Maintenance Schedule
Preventative maintenance dramatically reduces unscheduled kitchen emergencies and maintains optimal operating efficiency:
- Monthly Deep Coil & Filter Cleaning: Vacuum and chemically degrease condensing coils, fan impellers, and intake louvers to maintain unrestricted heat rejection airflow.
- Bi-Monthly Electrical Terminal Torque Audit: Inspect control box terminals with thermal imaging; retorque screw terminals to prevent high-resistance loose connections.
- Quarterly Gasket & Alignment Inspection: Clean magnetic door seals with mild antibacterial solution; perform the dollar-bill compression drag test along all perimeter edges.
- Semi-Annual Amp Draw & Telemetry Benchmarking: Record compressor, motor, and heating element running current under load to detect early bearing wear or insulation breakdown.
OSHA & Commercial Health Code Regulatory Compliance
Commercial food facilities in North Fulton County are strictly regulated under FDA Food Code standards, NSF International sanitation mandates, and OSHA worker safety rules:
- Mandatory 41°F Commercial Food Safety Holding Rule: Perishable foods stored above 41°F for more than two cumulative hours must be discarded by health inspector order, resulting in catastrophic inventory losses.
- 180°F High-Temperature Warewashing Sanitization: Commercial dishwashers must achieve 180°F during final sanitizing rinse to ensure 99.999% microbial elimination without chemical residuals.
- OSHA Machine Guarding & Interlock Compliance: All moving sprockets, pulleys, and mechanical shafts must remain enclosed within protective guards with functional safety interlocks.
Frequently Asked Technical Engineering Questions
Select any question below to expand technical diagnostic insights from our master commercial technicians:
Q1: What is the primary cause of Water Pan Humidity Heating Element, Circulation Blower Motor & Solid-State Heat Controller failure in commercial environments?
Failure stems primarily from electrical contact arc erosion, continuous thermal cycling in hot kitchen environments, and mechanical drag caused by airborne grease particulate. Regular maintenance and professional telemetry monitoring prevent sudden stoppage. Call (770) 796-7742 for fast same-day diagnosis.
Q2: How quickly can an emergency commercial technician arrive at our Alpharetta restaurant?
Our mobile commercial service units are stationed along major North Fulton arteries including Windward Parkway, Old Milton Parkway, and Mansell Road, enabling an average emergency arrival time of 45 to 90 minutes.
Q3: Can our kitchen staff temporarily bypass a tripped safety switch to continue dinner service?
No. Bypassing safety high-limits or pressure cutouts can cause catastrophic compressor burnout, electrical fires, or pressurized vessel rupture. Safety devices trip only when operating limits are exceeded.
Q4: How do technicians test for electrical continuity on commercial InterMetro (Metro) components?
Technicians isolate the circuit, discharge residual capacitance, and utilize an industrial True-RMS multimeter set to low-resistance Ohms (Ω). A healthy component must read within factory engineering limits (Water Reservoir Immersion Element 7.2 Ω (Rated 2000W at 120V)).
Q5: What warranty protection is provided on commercial equipment repairs?
Every commercial repair is backed by our comprehensive 90-day parts and labor warranty, guaranteeing that replacement OEM components perform reliably under demanding commercial operating conditions.
Q6: Why are authentic factory OEM parts required instead of generic universal replacements?
OEM hardware matches exact electrical impedance, mechanical mounting dimensions, and NSF sanitation requirements. Generic parts frequently fail prematurely and may void remaining equipment manufacturer warranties.
Q7: How does airborne kitchen cooking grease impact electrical control compartments?
Aerosolized cooking fats settle across circuit boards and contactor surfaces, attracting dust and creating conductive paths that cause tracking shorts, false sensor readings, and electrical arc damage.
Q8: What signs indicate that a commercial condensing unit is failing from high head pressure?
High head pressure causes frequent short-cycling on the high-pressure safety cutout, an extremely hot liquid line, elevated compressor amp draw, and diminished cooling capacity inside refrigerated storage.
Q9: Why does ice accumulate on evaporator coils when equipment has a defrost timer?
Coil icing occurs when the defrost timer motor fails, the defrost termination thermostat (Klixon) opens prematurely, the electric defrost heater burns open, or door gaskets allow continuous humid air infiltration.
Q10: What should a kitchen manager do if a foul electrical odor is detected from the machine?
Immediately switch off the dedicated circuit breaker at the electrical panel, disconnect power to the unit, and call our commercial emergency dispatch team at (770) 796-7742 to prevent electrical fire outbreaks.
Q11: How often should commercial kitchen refrigeration coils be chemically cleaned?
Condenser coils should be vacuumed monthly and chemically degreased with a non-acid commercial foaming coil cleaner at least once every quarter in high-grease kitchen cooking environments.
Q12: Can phase voltage imbalances damage three-phase commercial motors?
Yes. A voltage imbalance as small as 2% between electrical phases can cause a dramatic 15% to 20% increase in winding temperature, rapidly degrading motor winding insulation and causing sudden motor seizure.
Q13: How do technicians test solenoid valves for mechanical binding versus electrical failure?
Technicians first verify voltage supply to the coil. If voltage is present, they test coil resistance with a multimeter. If the coil is electrically sound but the valve fails to actuate, mechanical internal plunger binding is confirmed.
Q14: What is the typical lifespan of a commercial InterMetro (Metro) Commercial Heated Proofing & Holding Cabinet?
With quarterly preventative maintenance and prompt OEM component replacements, commercial platforms routinely achieve 10 to 15+ years of dependable daily kitchen service.
Q15: How does hard water scale affect commercial equipment performance?
Calcium carbonate scale insulates heating elements, coats water level probes causing false lockouts, and clogs solenoid orifices. Dedicated water filtration and scheduled de-liming cycles are mandatory.
Q16: Do your technicians carry EPA Universal Refrigerant Certification?
Yes. Every commercial refrigeration specialist on our team holds EPA Section 608 Universal Certification, ensuring full legal compliance with refrigerant recovery, leak repair, and charging regulations.
Q17: What information should kitchen managers have ready when calling commercial dispatch?
Please have the exact equipment brand, model number, serial number, reported digital error codes, and a brief description of operating symptoms to expedite technician part loading prior to dispatch.
Q18: What payment methods and commercial billing terms are available for restaurants?
We accept all major commercial credit cards, corporate electronic bank transfers, and offer established Net-30 commercial billing accounts for qualified restaurant groups and institutional facilities across North Fulton.
Regional North Fulton Commercial Service Hubs
Our mobile commercial fleet delivers responsive emergency repairs throughout North Fulton County, linking directly with our primary regional service hubs:
Core Commercial Services
Related Commercial Problems
Premium Brand Specialists
Thermodynamic Phase Transitions & Heat Exchange Fundamentals
The operational success of commercial InterMetro (Metro) Commercial Heated Proofing & Holding Cabinet systems relies upon strict adherence to closed-loop thermodynamic laws. Within commercial kitchen and food storage environments, heat is not passively dissipated; it must be mechanically transferred via vapor-compression or forced convection cycles. The refrigeration fluid or thermal heating element functions under intense pressure and temperature gradients, requiring exacting component calibration to prevent system disruption.
When Water Pan Humidity Heating Element, Circulation Blower Motor & Solid-State Heat Controller begins to degrade, internal pressure-enthalpy characteristics shift away from design parameters. In refrigeration systems utilizing high-density HFC or HFO refrigerants such as R-404A, R-448A, or R-452A, minor fluctuations in evaporator airflow or liquid expansion disrupt the critical mass flow rate. If the evaporator superheat is uncalibrated, liquid refrigerant enters the suction line rather than completely vaporizing within the final third of the coil. The resulting liquid wash sweeps oil away from the compressor cylinder walls, initiating catastrophic mechanical bearing scoring.
Conversely, when convective heating and ventilation parameters deviate in cooking or warewashing equipment, localized thermal boundaries insulate heating surfaces. Incoloy-sheathed heating elements, designed to transfer heat rapidly into turbulent water or air streams, experience rapid sheath temperature runaway when airflow or water circulation drops. Operating temperatures climb from a rated 250°F past 950°F within minutes, expanding the internal magnesium oxide insulating core until the outer nickel-chromium heating wire ruptures against the metallic casing, tripping ground fault protection devices across the commercial building.
Transient Voltage Anomalies & Inductive Harmonics in Commercial Power Grids
Commercial dining facilities and foodservice establishments across North Main Street Commercial Bakery Strip draw substantial electrical power through high-capacity 208V or 480V 3-phase commercial electrical distribution panels. Heavy motor loads—including rooftop makeup air units, exhaust scrubbers, variable-frequency hood fans, and walk-in compressor racks—frequently switch on and off concurrently. This inductive load switching introduces severe electrical line noise, transient voltage spikes exceeding 1,200 Volts peak, and significant third and fifth-order harmonic distortion onto line wiring.
Sensitive electronic logic controllers and microprocessor monitoring boards in modern InterMetro (Metro) platforms are highly vulnerable to these harmonic currents. Neutral conductors frequently carry additive third-harmonic currents that create significant voltage drops between neutral and chassis earth ground. When ground potential rises above 1.5 Volts AC, low-voltage 5V DC reference circuits on sensor inputs experience signal corruption. Analogue-to-digital converters misinterpret microvolt readings from thermistors, resulting in false error codes, erratic relay cycling, and premature component safety lockouts.
During professional diagnostics, our master certified technicians utilize specialized power quality analyzers alongside True-RMS multimeters. We measure total harmonic distortion (THD), verify phase-to-phase voltage balance within strict 1.0% tolerances, inspect transient voltage surge suppression (TVSS) circuits, and confirm that line filtering chokes and metal-oxide varistors (MOVs) remain fully functional before replacing solid-state sub-assemblies.
Microscopic Metallurgy, Galvanic Corrosion & Thermal Creep Fatigue
Within commercial kitchens, metallic components endure severe environmental punishment combining elevated ambient temperatures, humidity levels exceeding 85%, and airborne aerosolized chlorides, cooking acids, and alkaline cleaning sanitizers. The interaction between dissimilar metals—such as copper refrigeration tubing brazed to steel compressor stubs, or stainless steel heating elements bolted into aluminum vessels—creates high potential for galvanic corrosion if dielectric isolation fails.
In high-stress components such as Water Pan Humidity Heating Element, Circulation Blower Motor & Solid-State Heat Controller, cyclical thermal expansion induces microscopic mechanical fatigue known as thermal creep. Metal grains along stressed weld seams or brazed joints expand and contract thousands of times per month. Over years of commercial operation, intergranular micro-fissures develop beneath the surface of the metal. While invisible to visual inspection, these fissures cause microscopic refrigerant leaks, vacuum leaks, or loss of mechanical spring tension in critical electromechanical switches and safety cutouts.
When our technicians overhaul InterMetro (Metro) machinery in Alpharetta, we utilize ultraviolet fluorescent leak detection, ultrasonic acoustic listening probes, and high-precision dial calipers to measure mechanical wear against exact factory blueprints. Worn brass bushings, fatigued beryllium copper contact springs, and corroded terminal lugs are replaced with genuine OEM assemblies treated with proprietary passivated protective finishes designed for commercial durability.
Refrigerant Lubricant Miscibility & Polyolester (POE) Oil Breakdown Dynamics
In commercial refrigeration and chilling applications, mechanical longevity hinges entirely upon the continuous circulation and return of lubricating oil to the compressor crankcase. Modern HFC and HFO systems employ synthetic polyolester (POE) lubricants engineered to remain miscible with refrigerant molecules across the full operating temperature spectrum, from -20°F in walk-in freezers to 220°F at the compressor discharge valve.
However, synthetic POE oil is extraordinarily hygroscopic—it chemically binds with ambient atmospheric moisture within seconds of exposure to humid air. If a minor suction line leak occurs or if an uncertified service contractor fails to pull a deep vacuum below 500 microns during field service, water molecules chemically react with the ester bonds in the POE oil. This chemical reaction (hydrolysis) produces corrosive organic acids and alcohol within the sealed refrigeration circuit.
Acidic refrigerant oil attacks copper motor winding insulation, leaches copper from internal heat exchangers (copper plating), and deposits gummy sludge within thermostatic expansion valve orifices and solenoid needle seats. Over several weeks, the expansion valve orifice clogs, starving the evaporator coil and causing severe suction pressure drop. Our commercial service protocol mandates total system acidity testing, installation of high-capacity solid-core liquid and suction line filter driers, and comprehensive nitrogen purges to guarantee 100% moisture elimination.
Closed-Loop Proportional-Integral-Derivative (PID) Calibration Standards
Modern commercial food holding, steaming, and cooking machinery relies on sophisticated microprocessor controllers executing closed-loop proportional-integral-derivative (PID) mathematical algorithms. Rather than crude on/off bimetallic switching that produces wide temperature swings, PID algorithms continuously compute the mathematical error between desired temperature setpoint and real-time process value, modulating electrical solid-state relays (SSRs) or modulating gas valves via pulse-width signals.
The accuracy of this closed-loop control relies entirely on the precision and response time of temperature feedback sensors. If scale buildup, thermal grease degradation, or electrical impedance drift compromises sensor sensitivity, the PID loop enters an unstable hunting cycle. The controller overcorrects, driving heating elements or compressors to 100% capacity before oscillating into severe undershoot. This thermal hunting degrades food texture, wastes electrical energy, and places cyclic over-stress on mechanical contactors and compressor valves.
During professional commissioning and restoration, our master technicians perform precision PID loop autotuning and temperature offset calibration using certified secondary RTD reference thermometers immersed in calibrated dry-block temperature calibrators. By recalibrating proportional band gain ($K_p$), reset integral time ($T_i$), and derivative rate ($T_d$), we restore razor-sharp temperature control within ±0.5°F, ensuring optimal culinary outcomes and commercial equipment reliability.
Ultrasonic Acoustic Telemetry & Mechanical Vibration Spectrum Analysis
Before mechanical components fail catastrophically in commercial kitchens, they emit distinct high-frequency acoustic stress waves long before audible noise or thermal runaway occurs. Rotating assemblies—including motor ball bearings, centrifugal blower wheels, planetary gearboxes, and positive-displacement pumps—generate ultrasonic frequencies between 20 kHz and 100 kHz as microscopic imperfections develop across bearing raceways.
Our commercial field service units carry advanced digital ultrasonic listening apparatus and tri-axial vibration accelerometers. By placing contact probes directly against bearing housings and gear casings, technicians capture acoustic telemetry and analyze peak frequency spectra. A healthy, properly lubricated commercial bearing produces a smooth, low-amplitude hiss across the ultrasonic spectrum. When lubrication degrades or fatigue spalling begins, the acoustic signature displays sharp, high-decibel transient peaks indicative of metal-on-metal impact.
Capturing acoustic telemetry allows our specialists to identify developing mechanical failures weeks in advance. Rather than waiting for an evaporator fan motor or wash pump to seize during a busy Friday night dinner service, our technicians identify elevated decibel thresholds during quarterly maintenance, schedule proactive OEM replacement during quiet morning prep hours, and eliminate unpredicted kitchen stoppage entirely.
Fulton County Health & Sanitation Critical Temperature Compliance Mandates
In Alpharetta, Milton, Roswell, and Johns Creek, commercial foodservice establishments operate under stringent public health oversight administered by the Fulton County Board of Health and Georgia Department of Public Health environmental health divisions. Commercial equipment performance is directly tied to official food safety holding and sanitization inspection scores:
- Cold Perishable Food Holding Threshold (41°F Rule): All potentially hazardous foods (PHF/TCS)—including raw meats, poultry, dairy products, and cooked prepared items—must remain continuously chilled at or below 41°F (5°C). Any temperature excursion above 41°F exceeding two hours mandates immediate product condemnation and disposal under health inspection protocol.
- Thermal Sanitization Warewashing Standards (180°F Rule): Commercial dishwashers operating under high-temperature sanitation mandates must deliver final rinse water to dishware surfaces at a minimum temperature of 180°F (82°C) at the manifold, achieving a minimum plate surface temperature of 160°F verified via thermal test strips.
- Hot Food Holding Standards (135°F Rule): Hot holding cabinets, steam tables, and heated display warmers must maintain hot prepared foods continuously at or above 135°F (57°C) to prevent the germination and proliferation of spore-forming pathogenic bacteria such as Clostridium perfringens and Bacillus cereus.
- Certified Maintenance & Temperature Logging Documentation: Health inspectors routinely audit digital temperature data loggers and equipment maintenance service tickets. Equipment restored by our master certified technicians includes signed inspection documentation verifying factory thermal calibration, satisfying regulatory compliance reviews.
Executive Takeaways for Foodservice Operators
- Immediate Emergency Commercial Dispatch: Priority 45-minute on-site arrival minimizes perishable inventory loss and eliminates expensive kitchen downtime.
- Precision True-RMS Multimeter Telemetry: In-depth electrical load and pressure benchmarking identifies root causes without guesswork or repeated failures.
- Exclusive Factory OEM Components: Installation of genuine Metro OEM 120V 2000W Calrod Humidity Element & Terminal Seal Kit guarantees exact mechanical fit, electrical safety, and sanitation compliance.
- Ironclad 90-Day Warranty Protection: All commercial service calls are backed by our 90-day parts and labor warranty, delivering total peace of mind to kitchen operators.
- Local North Fulton Presence: Dedicated service coverage throughout Alpharetta, Milton, Roswell, and Johns Creek ensures rapid assistance when equipment emergencies occur.
Restore Your InterMetro (Metro) Equipment to Factory Precision Today
Do not let equipment failure jeopardize your commercial kitchen operations or violate health department regulations. Our master certified commercial technicians are on-call across North Fulton with authentic OEM hardware ready for immediate installation.
Call (770) 796-7742 for Priority Dispatch
Same-Day Emergency Commercial Kitchen Service • 90-Day Parts & Labor Warranty • Licensed & Insured