
High-volume culinary operations, artisan farm-to-table eateries, and private banquet venues across the Crabapple Road Dining District along the Milton and Alpharetta border depend on Jackson commercial warewashing systems as their indispensable sanitation safeguard. When an industrial Jackson door-type, conveyor, or undercounter dishmachine suffers a booster heater failure, the final sanitizing rinse cycle plunges below the legally mandated 180°F threshold, triggering immediate health inspection infractions and halting back-of-house service. In this comprehensive technical engineering guide, our master commercial foodservice specialists examine the thermodynamics, 480V three-phase electrical circuitry, mercury displacement contactors, high-limit bimetal safeties, and Incoloy immersion heating elements governing Jackson booster heaters, equipping restaurant operators and kitchen directors with actionable diagnostic telemetry and priority same-day restoration protocols.
Quick Diagnostic Answer for Commercial Kitchen Operators
When performing a Jackson commercial dishmachine rinse temperature booster heater repair due to final rinse temperatures dropping below the required 180°F sanitizing threshold, the malfunction is overwhelmingly caused by an open-circuit 480V 3-phase electric booster heating element (measuring infinite resistance / OL instead of the baseline 25.6Ω per phase on 9kW/12kW assemblies), a burnt or mechanically bound mercury displacement contactor coil (nominal baseline 45Ω across 120VAC coil terminals), or a tripped manual-reset bimetal high-limit safety thermostat (which must exhibit 0.0Ω continuity below 210°F). Immediate True-RMS electrical telemetry verification across line terminals isolates open element circuits and defective mercury contactors without operational guesswork.
Listen to 60-Second Diagnostic Summary
Narrated by Jason J. (Master Certified Commercial Foodservice Specialist)
Check Same-Day Tech Availability in Your Kitchen Corridor
Recently Serviced in Crabapple Road Dining District / Milton GA Border
Jackson Conserver XL2 High-Temp Booster Heater Element & Mercury Contactor Restored • Verified 5.0 ★★★★★
Jackson TempStar Door-Type Dishmachine Sanitizing Rinse Thermal Failure
Crabapple Road Commercial Kitchen Corridor, Milton GA / Alpharetta Border, GA 30004
90-Day Commercial Parts & Labor Warranty Active
High-Volume Farm-to-Table Gastropub & Banquet Operation
Jackson TempStar High-Temp Door-Type Dishmachine with Built-in 480V 3-Phase 12kW Booster Tank
Rinse thermometer stalling at 142°F during final cycle; dishware exiting with greasy film; Fulton County health inspection audit pending
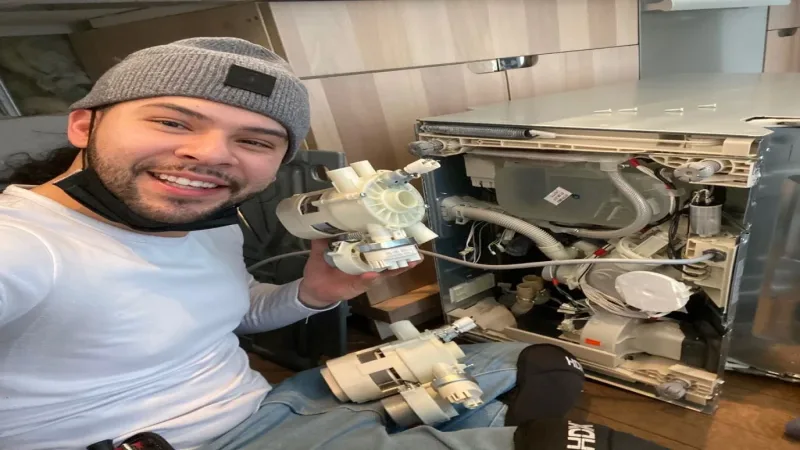
Jason J. (Master Certified Commercial Foodservice Specialist)
Diagnostic Multimeter & Component Telemetry
- Line Terminal Voltage Under Full Load: 482 VAC measured across phases L1-L2, L2-L3, and L1-L3 at the heavy-duty subpanel disconnect.
- Heating Element Resistance: Flange-mounted immersion assembly measured Open-Loop (OL / ∞Ω) across Phase 1 to Phase 2 legs. Phase 2 to Phase 3 measured 25.6Ω (factory nominal baseline: 25.6Ω ± 5% per phase for 12kW 480V balanced 3-phase configuration). A localized mineral scale blanket caused dry thermal rupture on Phase 1 Incoloy sheath.
- High-Limit Safety Bimetal Switch: Tripped open at room temperature; manual reset plunger was non-responsive with internal bimetallic latch failure, registering infinite resistance (OL). Factory specification: 0.0Ω continuity under normal operating conditions, opening cleanly at 210°F ± 5°F.
- Mercury Displacement Contactor: Control coil measured 45.2Ω across 120VAC pilot terminals (normal tolerance 42.0Ω to 48.0Ω). However, high-voltage load contacts exhibited severe internal mercury pooling degradation, failing to pass phase current on pole L1 when coil was energized by the wash timer board.
- Low-Water Float Switch Probe: Resistance measured 0.1Ω closed in full booster tank state, correctly signaling operational water presence to the solid-state controller.
Corrective Actions & OEM Part Restoration
Our master technician initiated Lockout/Tagout (LOTO) protocols on the dedicated 480V three-phase commercial feeder breaker and isolated the 3/4-inch dynamic water supply line. Drained the pressurized booster vessel via the lower boiler drain valve, removed the heavy four-bolt flange collar, and extracted the ruptured immersion element assembly. Descaled the internal 304 stainless steel booster vessel using food-grade sulfamic acid bath to dissolve 1/4-inch calcium carbonate accumulation. Installed a genuine OEM Jackson 12kW 480V 3-Phase Incoloy Booster Heating Element (Part #04420-003-88-75) with a high-temperature EPDM flange gasket torqued in a crisscross pattern to 38 ft-lbs. Replaced the defective high-limit switch with an authentic OEM Jackson 210°F Manual Reset High-Limit Thermostat (Part #05930-121-67-72). Replaced the damaged mercury displacement contactor with an OEM 3-Pole 50A 120VAC Mercury Contactor (Part #05945-111-68-38).
Post-Repair Verification: Refilled booster vessel and bled air through the high-point vacuum relief valve. System energized under test cycles: each phase drew exactly 14.4 Amps balanced load at 480V. Final sanitizing rinse temperature reached a stable 184.2°F during sustained 30-rack back-to-back banquet simulation. Fulton County health inspector thermolabel strip test achieved dark black irreversible sterilization reaction at 180°F.
Table of Contents
- Jackson Commercial Dishmachine Sanitizing Rinse Physics & High-Temp Warewashing Engineering
- Thermal Warning Signs & Final Rinse Temperature Depressurization Symptoms
- Visual Before & After Restoration Showcase
- Root Failure Mechanisms Behind Jackson Booster Heater Temperature Drop
- Back-of-House Safe Diagnostic Protocol for Commercial Kitchen Operators
- High-Voltage 480V Arc Flash Hazards & When to Halt In-House Troubleshooting
- Jackson Booster Heater Commercial Repair vs. Replace Financial Decision Matrix
- Instant Commercial Dishmachine Booster Heater Repair Cost Estimator
- Key Commercial Foodservice Variables Determining Booster Heater Repair Invoices
- Master Technician Multimeter Diagnostic Protocol & Electrical Telemetry Analysis
- Jackson Warewashing Booster Tank Component Anatomy & Heavy-Duty Assemblies
- Commercial Foodservice Preventative Maintenance & Immersion Tank De-Liming Schedules
- Commercial High-Temperature Warewashing Electrical & Thermal Safety Protocols
- Thermodynamic Heat Transfer Calculations & Booster Kilowatt Sizing Recovery Rates
- Georgia Public Health Food Code Chapter 511-6-1 & Thermal Log Sanitization Compliance
- Mercury Displacement Contactor Dynamics vs Solid-State Relays in Warewashing
- North Fulton Hard Water Mineral Scale Accretion on Incoloy Sheathed Heating Elements
- Three-Phase Delta Electrical Branch Circuit & Line Voltage Imbalance Telemetry
- Frequently Asked Questions About Jackson Booster Heater & Dishmachine Repairs
- Commercial Warewashing & Kitchen Equipment Navigation Silos
- Key Commercial Warewashing & Booster Maintenance Takeaways
- Emergency Commercial Warewashing Repair & Same-Day Tech Dispatch
Jackson Commercial Dishmachine Sanitizing Rinse Physics & High-Temp Warewashing Engineering
In high-volume commercial kitchens, the dishroom represents the single most critical hygiene choke point. Across the bustling dining destinations lining Crabapple Road, Milton Avenue, and the Historic Roswell border, culinary success depends on an unbroken cycle of pristine, sanitary tableware. Unlike residential dishwashers that rely on lengthy multi-hour cycles with extended drying phases, commercial foodservice establishments utilize heavy-duty pass-through door-type machines, conveyor flight systems, and undercounter warewashers designed to clean and sanitize a loaded dish rack every 60 to 90 seconds. To deliver certified microbial destruction within this compressed operating window, commercial dishroom engineering splits into two distinct sanitization methodologies: chemical low-temperature sanitization (which uses chlorine hypochlorite at 120°F) and high-temperature thermal sanitization (which relies entirely on pure thermal energy delivered at or above 180°F during the final rinse).
When restaurants operate Jackson commercial dishmachines—such as the benchmark TempStar series, the Conserver XL2, or the heavy-duty DynaStar rack conveyors—they overwhelmingly choose high-temperature thermal sanitization. High-temperature sanitization leaves no chemical odor on delicate wine glasses, cuts through stubborn grease and animal proteins effortlessly, and utilizes the latent heat absorbed by ceramic plates and stainless flatware to induce rapid self-drying (flash evaporation) within seconds of exiting the machine. However, achieving this thermal velocity requires tremendous instantaneous heating capacity. Standard domestic and commercial building hot water supplies typically supply potable hot water at 130°F to 140°F—far below the microbiological death threshold required by food codes. This is where the integrated or freestanding electric booster heater becomes the vital mechanical heart of the dishroom.
The booster heater is a pressurized, heavy-gauge stainless steel vessel engineered to elevate incoming water by an additional 40°F to 70°F (known as the Delta-T, or ΔT rise) immediately before it discharges through the upper and lower sanitizing rinse nozzles. To accomplish this massive thermal lift in real time as water surges through the manifold at 15 to 25 pounds per square inch (PSI) dynamic pressure, Jackson booster heaters employ high-wattage 480V three-phase electric immersion heating elements. When these heavy-duty heating elements, their controlling mercury displacement contactors, or their bimetallic safety thermostats fail, the dishmachine loses its sanitizing capability instantly. Navigating a commercial appliance repair scenario under peak dinner service demands an uncompromising understanding of electrical telemetry, thermal fluid dynamics, and North Fulton commercial kitchen operating conditions.
Our technical team regularly diagnoses and resolves complex commercial dishmachine repair challenges across North Fulton County. In this technical dissertation, we explore every critical failure mode observed in commercial booster assemblies, provide step-by-step diagnostic telemetry, detail real-world multimeter testing procedures, and outline preventative maintenance protocols that protect your kitchen from catastrophic inspection shutdowns and costly equipment replacements.
Thermal Warning Signs & Final Rinse Temperature Depressurization Symptoms
A failing commercial booster heater rarely collapses without providing unmistakable operational warning signs. Back-of-house kitchen managers, executive chefs, and dishroom lead operators must recognize these early mechanical and thermal red flags before an unannounced Fulton County Board of Health inspection results in immediate demerits or dishroom closure. Because the wash cycle operates independently on its own lower-temperature tank heater (typically 150°F to 160°F), kitchen staff often overlook a booster failure until the final rinse phase is closely monitored during live production.
The primary and most definitive symptom is a depressed reading on the machine’s external final rinse thermometer. During normal operation, as the dishmachine switches from its recirculating detergent wash phase into its 10-to-12-second final rinse spray, the dial or digital LED thermometer mounted on the front fascia must promptly climb to and hold steady between 180°F and 195°F. If the gauge stalls at 135°F to 150°F—merely reflecting the incoming temperature of the facility’s domestic boiler—the booster heater is completely non-operational or has suffered a partial phase burnout. In systems where one phase of a 480V 3-phase delta element has failed open, the heater may only provide partial thermal output, causing the rinse temperature to peak at 160°F before plummeting during continuous rack-after-rack washing.
Secondary operational symptoms manifest directly on the ware itself. When final rinse water strikes dishware below 180°F, dishes exit the unload table cool to the touch and covered in beaded standing water droplets. Under proper high-temp operation, ceramic plates emerge intensely hot, radiating heat that instantly evaporates water film without requiring manual towel drying (which is strictly prohibited under commercial health codes). Furthermore, greasy film, cloudy mineral haze on glassware, and un-emulsified lipsticks indicate that the thermal sanitization threshold has collapsed, preventing detergents and rinse additives from sheeting properly off the tableware.
Thirdly, chemical and biological audit failures provide incontrovertible proof of booster heater distress. Many modern culinary operations utilize single-use irreversible temperature indicator strips (such as 160°F plate-surface Thermolabels) attached directly to test plates during morning prep audits. If the white indicator window fails to turn irreversible jet black after running through the dishmachine cycle, the surface of the plate has failed to reach the mandatory 160°F threshold, confirming that the rinse booster is failing to deliver sufficient thermal energy. Scheduling an emergency same-day dispatch at the earliest detection of these thermal symptoms prevents dishroom shutdowns during peak evening dining rushes.
Visual Before & After Restoration Showcase
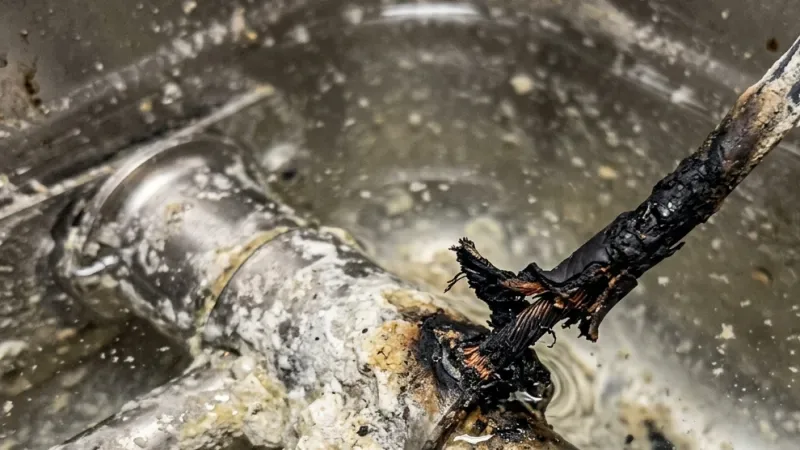
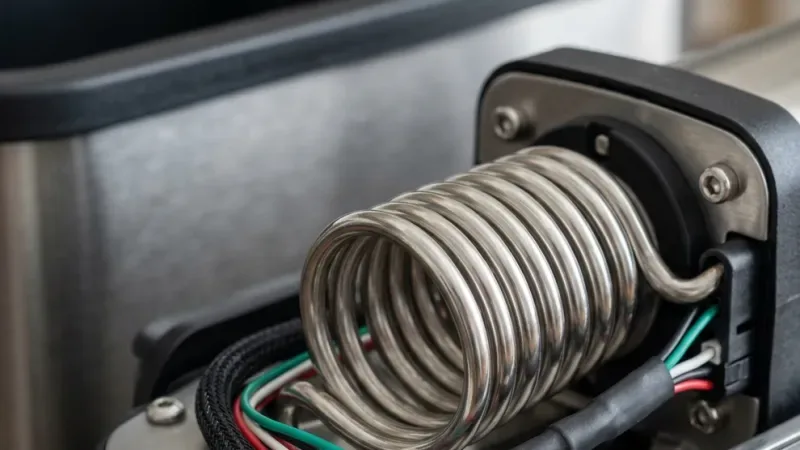
The visual evidence captured in our field diagnostic archives underscores the severe metallurgical stress endured by commercial water heating components. Incoloy 800 and 840 superalloys are specifically selected by Jackson engineers for their exceptional resistance to oxidation, high-temperature creep, and chloride stress-corrosion cracking. Much like the thermal dynamics encountered in commercial refrigeration and cooling systems, when mineral scale precipitates out of hot water, it accumulates directly on the tubular sheath surfaces. This mineral barrier has a thermal conductivity less than one-thirtieth that of metal, trapping heat within the core of the element. As internal coil temperatures climb beyond 1,600°F, the magnesium oxide dielectric insulation breaks down, the outer Incoloy sheath swells and splits, and catastrophic phase shorting or open circuits occur.
Root Failure Mechanisms Behind Jackson Booster Heater Temperature Drop
Pinpointing the root failure mechanism of a Jackson booster heater requires systematic diagnostic isolation across three interconnected engineering domains: thermal fluid hydraulics, mechanical scale accumulation, and 480V high-amperage electrical controls. Through hundreds of field service interventions across North Fulton, our master technicians have categorized the primary failure modes that paralyze commercial warewashing rinse temperatures, coordinating with our specialized commercial oven and range repair specialists to maintain uninterrupted kitchen output.
Flange Immersion Element Open-Circuit Burnout & Calcite Scale Encrustation
The primary electro-thermal component responsible for heating incoming rinse water is the flange-mounted Calrod immersion element assembly. In 480-volt commercial models, these elements are configured with multiple high-density U-tubes constructed of Incoloy sheath enclosing a helically coiled 80/20 nickel-chromium resistance wire insulated by compacted magnesium oxide (MgO) powder. For a standard 12kW 480V three-phase booster assembly, the design resistance across each balanced phase leg is precisely 25.6Ω. Over months of rigorous service in commercial kitchens without rigorous water softening, hard calcium and magnesium ions precipitate onto the heated element tubes. This calcified encrustation acts as a thermal insulator, preventing heat from dissipating into the passing water stream. The internal resistance wire overheats past its metallurgical melting point, fracturing the circuit and producing an Open Loop (OL) condition on one or more phases. When one phase burns out, total heating capacity drops by at least 33% to 50%, leaving the booster unable to maintain the 180°F sanitizing threshold during continuous operation.
Mercury Displacement Contactor Coil Failure & Silent Chattering
Unlike conventional residential appliances that utilize mechanical relays with exposed copper-silver contacts, Jackson commercial dishmachines incorporate heavy-duty mercury displacement contactors (MDCs) to switch the high-voltage, high-amperage 480V three-phase loads powering the booster elements. Mercury displacement contactors feature a hermetically sealed stainless steel tube containing an internal plunger, a pool of liquid elemental mercury, and tungsten-tipped stationary electrodes. When the 120VAC control circuit energizes the external magnetic solenoid coil (which has a nominal resistance of 45Ω), the magnetic field pulls the ceramic plunger down into the mercury pool, displacing the conductive mercury upward to bridge the stationary contact electrodes and energize the heating elements silently and arc-free. However, continuous cycling—often hundreds of cycles per day in high-volume banquet facilities—can cause the 120VAC solenoid coil to burn open, short internally, or suffer thermal breakdown. Alternatively, internal mercury oxidation, plunger mechanical stiction, or contact pitting can prevent electrical continuity across one or more line poles even when the coil is magnetically energized.
Manual Reset High-Limit Safety Thermostat Premature Tripping
Every commercial pressurized water heating vessel is equipped with a primary safety cutoff: a high-limit bimetallic disc thermostat or liquid-expansion capillary safety switch calibrated to trip at 210°F ± 5°F. Under normal operating conditions, this safety switch maintains a closed circuit (0.0Ω continuity) wired directly in series with the mercury contactor coil pilot circuit. If the booster vessel overheats due to low water flow, defective regulating thermostats, or heavy mineral scale blankets preventing heat dissipation into the water, the bimetallic snap disc trips open, completely breaking the 120V control circuit to the contactor coil and shutting down the elements to prevent steam explosion or vessel rupture. In many aging installations, the high-limit switch itself suffers internal contact degradation, spring fatigue, or calibration drift, causing it to trip prematurely under normal 185°F rinse cycles or permanently latch open with infinite resistance, refusing to reset.
Low-Water Level Cutoff Float Probe Desensitization & Dry-Firing Lockout
Energizing a 12kW immersion heating element in an empty or partially filled booster vessel results in catastrophic element destruction within 30 seconds—a destructive event known as dry firing. To safeguard against this hazard, Jackson booster tanks incorporate a stainless steel conductive liquid level float sensor or conductivity probe. If the municipal water pressure drops, an inlet strainer clogs, or the booster drain valve leaks, the liquid level inside the tank drops below the minimum safe threshold. The level sensor immediately opens its circuit (OL), and the solid-state controller de-energizes the booster contactor. Over time, grease films, boiler scale deposits, and mineral bridges can accumulate along the sensor probe housing, creating a false low-water signal that permanently locks out the heating circuit even when the tank is physically full.
Rinse Temperature Regulating Thermostat & Sensor Bulb Thermal Drift
Operating rinse temperatures are regulated by an adjustable capillary bulb thermostat or precision NTC thermistor probe mounted in a thermal well inside the booster tank. This thermostat monitors the water temperature and cycles the mercury contactor on and off to maintain stored water at 185°F to 190°F, ensuring instant 180°F delivery the moment the rinse cycle begins. If the capillary sensing bulb develops a micro-fracture and loses its hydraulic fill charge, or if heavy limescale insulates the thermowell from the water, the thermostat senses an artificially cool or warm temperature. If it drifts out of calibration, it will de-energize the heating contactor prematurely at 150°F, leaving the final rinse cycle severely under-temperature.
Low Incoming Domestic Hot Water Temperature & Inadequate Boiler Delta-T
Commercial booster heaters are engineered with a specific thermal capacity designed to achieve either a 40°F temperature rise (raising 140°F incoming water to 180°F) or a 70°F temperature rise (raising 110°F incoming water to 180°F). If the restaurant’s primary domestic boiler or commercial water heater suffers a burner failure, mixing valve malfunction, or undersized capacity that causes incoming line temperatures to drop to 100°F or 120°F on a 40°F-rise booster, the heating elements cannot overcome the excessive thermal differential. The dishmachine will cycle through its final rinse before the water can absorb enough energy, resulting in low rinse gauge readouts despite the booster operating at 100% electrical output. Our commercial technicians in Milton commercial kitchen service corridors regularly verify incoming boiler temperatures before condemning booster components, offering immediate same-day commercial repair to prevent lunch service interruptions.
Back-of-House Safe Diagnostic Protocol for Commercial Kitchen Operators
When a Jackson dishmachine final rinse temperature alert occurs during prep or active meal service, restaurant managers and kitchen supervisors must execute safe, non-invasive troubleshooting steps before escalating the issue to certified commercial technicians. Because commercial dishmachines incorporate 480V three-phase electrical services capable of delivering lethal arc flash energies, kitchen staff must strictly limit their internal diagnostic efforts to visual observations and external controls.
Diagnostic Observation Phase for Shift Supervisors
Begin by observing the machine through a complete, loaded cycle. Note the exact temperature displayed on the wash tank thermometer (which should read between 150°F and 160°F) versus the final rinse thermometer. When the wash timer advances to the final rinse cycle, watch the rinse temperature needle closely. Does the temperature start at 180°F and immediately drop to 140°F, or does it never climb above 140°F at all? A rapid drop indicates that water stored in the booster tank reached initial temperature, but incoming cold water during the rinse cycle is not being heated due to failed elements or an undersized boiler recovery rate. Conversely, a needle that remains flatline cold indicates a total electrical shutdown of the booster circuit.
Dynamic Water Pressure Gauge Verification
Every Jackson high-temp dishmachine includes a water pressure gauge installed downstream of the incoming pressure reducing valve (PRV). Final rinse sanitation guidelines strictly mandate dynamic rinse pressure between 15 and 25 PSI (with 20 PSI being ideal). Check this gauge while the rinse nozzles are actively spraying water. If dynamic pressure spikes above 25 PSI, water is surging through the booster vessel too quickly to absorb the required thermal energy, causing low rinse temperatures and excessive water consumption. If dynamic pressure falls below 15 PSI, the rinse pattern will be weak, failing to thoroughly coat dishes and trip pressure interlock switches. Adjusting the PRV brass screw can often re-establish optimal hydraulic flow.
Circuit Breaker & High-Limit Reset Inspection
Locate the commercial kitchen subpanel and verify that the dedicated three-pole 480V circuit breaker labeled for the dishmachine booster has not tripped to the center neutral position. If the breaker is tripped, reset it once firmly to the OFF position and then back to ON. If it trips again immediately, do not attempt further resets; this indicates a dead ground fault or shorted element sheath. Additionally, locate the external manual reset button for the booster high-limit switch, typically positioned behind a small access port on the lower kick plate. With the machine turned off, gently press the red reset plunger. If a distinct mechanical “click” is felt, the high-limit switch had tripped due to an over-temperature condition. Run a test cycle to determine if heating resumes. If the reset button clicks repeatedly or fails to latch, call for professional service immediately.
Kitchen managers can also consult our guides on Alpharetta restaurant equipment repair and related commercial prep station maintenance to ensure total culinary line reliability.
High-Voltage 480V Arc Flash Hazards & When to Halt In-House Troubleshooting
Commercial kitchen maintenance carries inherent life-safety risks that far exceed standard residential appliance troubleshooting. Jackson booster heaters operate on 208V, 240V, or 480V electrical supplies, drawing between 15 and 50 amperes per phase. The National Fire Protection Association (NFPA) Standard 70E establishes rigorous safety mandates regarding electrical safety in the workplace, and commercial dishrooms represent an especially hazardous environment due to the close proximity of high-voltage power, wet stainless steel surfaces, and continuous water spray.
At 480 volts three-phase, an accidental short circuit caused by an uninsulated tool or slipping multimeter probe can initiate an arc flash blast. An arc flash produces instantaneous plasma temperatures exceeding 35,000°F—hotter than the surface of the sun—vaporizing copper conductors, emitting deafening pressure waves, and causing catastrophic third-degree burns. Commercial restaurant staff must halt all internal troubleshooting immediately under any of the following conditions:
- Access Panel Removal: Kitchen employees must never remove lower stainless steel shrouds, junction box covers, or control enclosure panels while the dishmachine or booster heater is connected to electrical power.
- Burning Odors or Buzzing Sounds: Any acrid electrical odor, visible scorch marks around terminal blocks, or violent electrical chattering from contactors indicates active arcing or thermal component breakdown.
- Repeated Breaker Tripping: Repeatedly resetting a high-voltage commercial circuit breaker into a short-circuit fault can cause catastrophic breaker failure and explosive panel rupture.
- Pressurized Steam Leaks: Any steam hissing or boiling water discharging from the booster vessel pressure relief valve or flange seams presents extreme scalding risks at temperatures exceeding 212°F.
- Suspected Mercury Contactor Breach: If a mercury displacement contactor has suffered physical damage or overheating that compromises its hermetic seal, toxic elemental mercury vapors can contaminate the dishroom atmosphere. Specialized hazmat protocols are required for handling and disposal.
When these hazardous thresholds are reached, kitchen managers should immediately engage our certified master commercial technicians by contacting our commercial dispatch office for certified, safety-compliant repairs.
Jackson Booster Heater Commercial Repair vs. Replace Financial Decision Matrix
When confronted with an unexpected commercial booster heater failure, general managers and restaurant owners must weigh the financial trade-offs between component rebuilds and complete equipment replacement. Commercial dishmachines are substantial capital assets, with new high-temperature door-type machines costing between $8,000 and $18,000 installed, and freestanding commercial booster heaters running between $3,500 and $6,500. Applying the industry-standard 50% Rule—which dictates that if the total estimated repair cost exceeds 50% of the depreciated asset value, replacement is warranted—ensures optimal capital allocation.
| Booster Condition & Failure Mode | Machine Age | Estimated Repair Cost | Expected Extended Life | Strategic Recommendation |
|---|---|---|---|---|
| Single Heating Element & Flange Gasket Failure | 1–5 Years | $450 – $750 | 3–5+ Years | Highly Recommended: Rebuild |
| Mercury Contactor & High-Limit Safety Replacement | 2–7 Years | $420 – $680 | 4–6 Years | Highly Recommended: Rebuild |
| Complete Electrical Overhaul (Elements + Contactors + De-Lime) | 4–9 Years | $850 – $1,350 | 3–5 Years | Recommended: Overhaul |
| Booster Pressure Vessel Pinhole Corrosion & Welded Tank Leak | 8–12+ Years | $2,400 – $3,800 | 1–2 Years | Replace Booster Vessel |
| Complete Machine Obsolescence (Wash Pump + Booster + Chassis Rust) | 12+ Years | $3,500+ | < 1 Year | Replace Entire Dishmachine |
In over 85% of field calls, the heavy stainless steel pressure vessel itself remains in exceptional structural condition, with failures isolated entirely to replaceable electrical consumables: heating elements, contactors, wiring harnesses, and safety thermostats. Rebuilding these subassemblies with genuine OEM Jackson parts restores factory-certified thermal recovery at a fraction of the cost and downtime of full machine replacement.
Instant Commercial Dishmachine Booster Heater Repair Cost Estimator
Key Commercial Foodservice Variables Determining Booster Heater Repair Invoices
When commercial kitchen operators review repair proposals for booster heater restorations, understanding the cost drivers helps ensure transparent, value-driven decision making. Unlike standard domestic repairs, commercial foodservice equipment maintenance is governed by industrial component specifications, strict building safety codes, and health inspection mandates.
The primary factor influencing total invoice cost is the electrical wattage and voltage rating of the heating elements. A 480V three-phase 12kW or 18kW Incoloy immersion element commands a higher component cost than smaller 208V single-phase undercounter elements due to specialized high-temperature metallurgical castings, multi-pole ceramic terminal blocks, and custom flange geometry. Furthermore, replacing failed mercury displacement contactors with genuine OEM 50-amp rated units involves specialized hermetic components engineered to endure millions of high-current switching operations.
The second major variable is chemical de-liming and tank descaling labor. If an immersion heating element failed because the booster tank is encrusted in 10 to 20 pounds of hard calcium carbonate scale, simply installing a new element without acid-descaling the vessel ensures that the new element will burn out within months. Disassembling the booster vessel, circulating a food-grade sulfamic or inhibited phosphoric acid descaling solution, neutralizing the tank, flushing the debris, and replacing high-temperature flange gaskets requires 2 to 3 hours of technical labor but guarantees long-term element reliability.
Finally, emergency response timing plays a role. When a banquet facility or busy Crabapple bistro experiences a dishmachine failure on a Friday evening, requesting immediate priority dispatch for night or weekend service ensures zero lost service revenue, while standard scheduled morning maintenance provides the most cost-effective labor rates. Our commercial dispatch also supports facilities needing Roswell food-service equipment repair and neighboring culinary districts.
Master Technician Multimeter Diagnostic Protocol & Electrical Telemetry Analysis
Certified commercial appliance technicians do not guess when diagnosing complex high-temperature warewashing systems; they execute rigorous True-RMS multimeter testing to capture precise electrical telemetry. Before initiating any electrical testing on a 480V Jackson booster heater, the technician confirms full Lockout/Tagout isolation, establishes personal protective equipment (PPE) compliance, and discharges any latent capacitive charges across the control circuits. Our certified technicians cross-train across industrial commercial appliance repair disciplines to guarantee comprehensive kitchen safety.
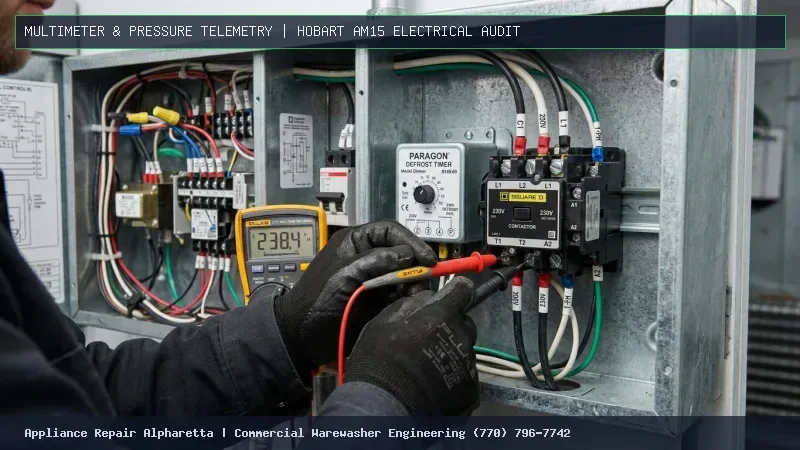
| Component Under Test | Test Terminals / Test Mode | Factory Nominal Telemetry | Failure Fault Threshold | Clinical Diagnostic Interpretation |
|---|---|---|---|---|
| 480V 3-Phase Electric Booster Heating Elements (12kW Assembly) | Flange element terminals: Phase L1-L2, L2-L3, L1-L3 (Ohms mode, unpowered) | 25.6 Ω (± 5%) per phase | Infinite Resistance (OL) or < 5.0 Ω | OL confirms open-circuit internal Nichrome wire burnout from scale hotspot. Values < 5Ω indicate short-circuited turns. |
| High-Limit Safety Bimetal Thermostat | Across dual faston terminals (Continuity/Ohms mode) | 0.0 Ω (Closed continuity normal < 200°F) | Open Circuit (OL) @ 210°F or latched open | Must trip cleanly to OL at 210°F. Latched open at room temperature indicates mechanical trip or internal disc failure. |
| Mercury Displacement Contactor Control Coil | Coil pilot terminals A1 to A2 (Ohms mode, disconnected) | 45.0 Ω (120VAC coil, ± 8%) | OL (Burned open) or < 10.0 Ω (Short) | Open coil prevents magnetic field generation; plunger never displaces mercury pool, leaving 480V elements completely de-energized. |
| Mercury Contactor Load Poles (Closed State) | Line to Load poles T1-L1, T2-L2, T3-L3 (Voltage drop mode under load) | < 0.2 VAC voltage drop across each pole | > 2.0 VAC drop or full line voltage (480V) | High voltage drop across closed contacts proves oxidized mercury pool, degraded tungsten electrodes, or open phase passage. |
| Booster Low-Water Cutoff Float Switch | Sensor switch leads (Continuity mode, tank filled) | 0.0 Ω to 0.2 Ω (Closed when water present) | Infinite Resistance (OL) with full vessel | Mineral sludge binding float stem down or fractured reed capsule produces false low-water lockout, preventing element operation. |
| Final Rinse Solenoid Valve Coil | Across solenoid faston terminals (Ohms mode) | 160.0 Ω ± 10% (120VAC coil) | OL (Open) or < 25.0 Ω (Shorted coil) | Shorted or open solenoid coil prevents final rinse valve from actuating, halting water flow through the booster altogether. |
| Insulation Resistance to Ground (Megohmmeter Test) | Element terminal pin to stainless flange ground (500 VDC test) | > 50 Megohms (> 50 MΩ) | < 1.0 Megohm (< 1 MΩ) | Low insulation resistance confirms dielectric breakdown of MgO powder; moisture or pinhole crack leaking current to vessel ground. |
Jackson Warewashing Booster Tank Component Anatomy & Heavy-Duty Assemblies
A commercial booster heater is a compact marvel of thermal hydraulic engineering. Built to operate continuously under municipal water pressure while withstanding water temperatures in excess of 190°F, every internal component is designed to industrial commercial standards.
The core vessel consists of a cylindrical 304 or 316-L heavy-gauge stainless steel tank, insulated with 1-to-2 inches of high-density fiberglass or polyurethane foam and wrapped in an aluminized steel outer wrapper to minimize standby thermal heat loss. Mounted into the lower end plate of the vessel is the heavy brass or stainless steel element flange collar. In a Jackson TempStar, this flange is secured by four or six high-tensile grade-8 bolts torqued against a precision molded EPDM or fluorocarbon gasket engineered to resist cyclic thermal degradation.
Welded to the upper apex of the booster vessel is an ASME-certified temperature and pressure relief valve (T&P valve), factory-rated for 150 PSI working pressure and 210°F discharge. In the event of a runaway thermal runaway where regulating thermostats and high-limit bimetals fail simultaneously, this mechanical spring-loaded valve lifts automatically to discharge superheated steam and prevent catastrophic tank over-pressurization. Downstream of the T&P valve, a bronze or brass vacuum breaker acts as an atmospheric backflow preventer, preventing dishroom rinse water from siphoning back into the facility’s potable drinking water supply during sudden municipal pressure drops.
Electrical control occurs inside an isolated sheet-metal raceway. Here, heavy terminal blocks distribute three-phase 480V feeder lines to the mercury displacement contactor poles, with high-temperature silicone-jacketed nickel-plated copper wire routing power to the immersion element pins. In modern Jackson systems, solid-state electronic control boards monitor thermistor inputs and control 120V pilot outputs through dedicated micro-relays. Technicians maintaining adjacent prep lines can review our diagnostic resources on commercial ice machine maintenance to ensure holistic kitchen support.
Commercial Foodservice Preventative Maintenance & Immersion Tank De-Liming Schedules
The single greatest enemy of commercial booster heaters in North Fulton County is calcium carbonate scale encrustation. Municipal water across Alpharetta, Milton, and Roswell carries dissolved mineral content that precipitates rapidly once water is heated past 140°F. Establishing an aggressive, disciplined preventative maintenance schedule is essential to achieving 10+ years of trouble-free booster performance.
Daily Maintenance: At the close of dinner service, dishroom operators must execute the machine’s automated drain and flush cycle. After the wash tank drains, the lower boiler drain valve on the booster heater should be cracked open for 10 to 15 seconds into a heat-resistant drain pan. This daily “boiler blowdown” expels loose particulate sediment, sand, and mineral precipitates that settle at the bottom of the vessel before they can bake into hardened stone around the immersion elements.
Weekly Maintenance: The culinary lead or facilities supervisor must inspect the commercial water softener servicing the dishroom. Check the brine tank salt level and verify that water hardness at the dishroom supply line measures under 3 grains per gallon (GPG) using a standard Hach titration test strip. Water hardness exceeding 5 GPG indicates that the softener resin bed is exhausted, channeled, or requiring regeneration, which will rapidly calcify the booster heater.
Monthly Maintenance: Perform a thorough chemical de-liming cycle using an authorized food-grade descaler (such as inhibited phosphoric acid or sulfamic acid). Activate the Jackson machine’s dedicated “DELIME” switch, allowing the chemical solution to circulate through the wash manifold and fill the booster vessel. Allow the acid to dissolve internal scale for 30 to 45 minutes, then flush the system with three consecutive fresh water fill-and-drain cycles to neutralize all acid residues.
Quarterly Professional Service: A certified commercial foodservice technician should inspect the booster control enclosure. Using a calibrated torque wrench, re-torque all electrical terminal screws on the mercury contactor, distribution blocks, and element pins. Thermal expansion and contraction during heating cycles cause screw terminals to loosen gradually over time, which increases electrical contact resistance, creates localized overheating, and melts terminal insulation. Commercial operators in adjacent municipalities can consult our resources for Johns Creek kitchen maintenance.
Commercial High-Temperature Warewashing Electrical & Thermal Safety Protocols
Safe servicing of commercial booster heaters demands strict adherence to industrial occupational safety standards. Given the combination of high-voltage 480V electricity, pressurized hot water vessels, and heavy metal assemblies, safety protocols must never be compromised.
First and foremost is OSHA Lockout/Tagout (LOTO) standard 29 CFR 1910.147. Before any access panels are opened or tools touch electrical wiring, the dedicated circuit breaker supplying the dishmachine must be switched off, padlocked with a physical lockout hasp, and tagged with an authorized warning tag. The technician must then verify zero energy state using a calibrated True-RMS multimeter, checking line-to-line (L1-L2, L2-L3, L1-L3) and line-to-ground across all phases. Never rely on external indicator lights alone to confirm power de-energization.
Thermal depressurization is equally critical. A booster heater operating at 185°F contains water pressurized between 20 and 80 PSI. Attempting to loosen flange bolts or remove temperature sensor wells without first closing the water isolation valve and manually opening the lower boiler drain to vent tank pressure will result in an explosive discharge of scalding water and steam. Always allow the tank to cool below 100°F before removing element flange assemblies.
Technicians must also exercise extreme care when handling older mercury displacement contactors. If an MDC capsule is dropped, cracked, or subjected to electrical arc rupture, elemental liquid mercury can be released into the environment. Mercury is a potent neurotoxin. In the event of a breach, the area must be immediately evacuated, ventilated, and cleaned using an OSHA-approved mercury spill kit containing mercury-absorbing amalgam powder. Never use a standard vacuum cleaner on spilled mercury. Managing kitchen safety across diverse equipment lines also extends to maintaining walk-in freezer cooling systems.
Thermodynamic Heat Transfer Calculations & Booster Kilowatt Sizing Recovery Rates
The sizing of an electric commercial booster heater is governed by immutable thermodynamic laws. To understand why a booster fails to maintain 180°F under high-velocity dishroom conditions, kitchen managers must grasp the thermodynamic formula that dictates thermal recovery:
In this foundational equation, GPH represents the Gallons Per Hour of water consumed during final rinse operations, ΔT is the temperature rise in degrees Fahrenheit (the difference between incoming domestic boiler water and the 180°F sanitizing target), 8.33 is the weight of one gallon of water in pounds, and 3,412 is the conversion factor representing BTUs per kilowatt-hour of electric power.
Consider a standard Jackson TempStar door-type dishmachine operating during a heavy Saturday evening dinner rush in a Crabapple gastropub. The machine processes approximately 55 racks per hour, with each rack utilizing 0.89 gallons of final rinse water—equating to an active water consumption rate of 48.95 GPH. If the restaurant’s primary water heater delivers supply water at a standard 140°F, the booster must achieve a 40°F temperature rise (ΔT = 180°F – 140°F = 40°F). Applying the formula:
While a 4.78 kW continuous draw appears modest, water does not enter the booster gradually over an hour; it surges into the vessel in intense 10-second bursts at a flow rate equivalent to 320 GPH! Jackson engineers equip the TempStar with an oversized 12 kW booster heating element specifically to ensure that the water volume within the tank is rapidly recharged between cycles. If the incoming water supply temperature drops to 110°F (requiring a 70°F rise), the required continuous capacity jumps to 8.36 kW, pushing instantaneous thermal demand past 20 kW. If one phase of a 12 kW element burns out—reducing effective output to 8 kW—the booster cannot recover between consecutive racks. After 5 or 6 back-to-back racks, rinse temperatures plummet to 145°F, triggering health code non-compliance.
Georgia Public Health Food Code Chapter 511-6-1 & Thermal Log Sanitization Compliance
In the State of Georgia, commercial foodservice sanitation is strictly governed by the Georgia Department of Public Health (DPH) Rules and Regulations for Food Service, specifically Chapter 511-6-1. Subsection .05(7)(k) establishes explicit operational standards for mechanical warewashing equipment utilizing high-temperature sanitizing cycles.
Under Georgia food regulations and the FDA Model Food Code, the temperature of the fresh hot water sanitizing rinse as it enters the manifold may not be more than 194°F (to prevent excessive atomization and flashing to steam before striking the dishes) and must not be less than:
- 165°F (74°C) for a stationary rack, single-temperature dishmachine; or
- 180°F (82°C) for all other mechanical commercial warewashers, including standard door-type and conveyor Jackson machines.
Crucially, county environmental health officers—including inspectors conducting unannounced audits across Fulton County—do not evaluate compliance based solely on the dishmachine’s external dial thermometer. Inspectors utilize calibrated digital thermistors, maximum-registering bi-metal thermometers, or single-use irreversible thermal indicator strips (Thermolabels) attached directly to the face of a clean plate. The regulatory pass/fail standard dictates that the plate surface temperature itself must achieve at least 160°F (71°C).
Achieving a 160°F plate surface temperature requires rinse water striking the ware at 180°F+ for a minimum of 9 to 12 seconds. This thermal exposure delivers a minimum 5-log microbial reduction (99.999% destruction) of vegetative pathogenic microorganisms, including Salmonella enterica, Listeria monocytogenes, Escherichia coli, and Norovirus particles. If an inspector runs a test plate and the thermal indicator fails to reach 160°F, the dishmachine is red-tagged immediately as an imminent health hazard. The establishment is prohibited from washing tableware until a certified repair invoice is submitted, forcing the restaurant to switch to disposable paper service or a laborious manual three-compartment sink setup during live service.
Mercury Displacement Contactor Dynamics vs Solid-State Relays in Warewashing
The electrical design of Jackson commercial dishmachines has historically relied on mercury displacement contactors (MDCs) for high-voltage booster element switching. Understanding the operational dynamics of MDCs versus modern solid-state relay (SSR) replacements provides valuable insight into equipment longevity and service strategies.
In high-volume commercial kitchens, a dishmachine booster contactor cycles open and closed between 300 and 800 times every single day. A standard electro-mechanical contactor with physical copper contacts suffers severe electrical arcing every time it breaks a 480V three-phase 15-to-30-amp load. This inductive and resistive arcing produces intense heat, leading to contact carbonization, pitting, and eventual contact welding (where the contacts fuse shut, causing continuous dry firing). By contrast, a mercury displacement contactor utilizes a pool of liquid mercury inside a hermetically sealed stainless steel capsule.
When the MDC solenoid coil de-energizes, the plunger floats upward, lowering the mercury pool and breaking electrical contact cleanly with zero physical wear. Because the liquid metal reforms its contact surface instantly on every cycle, MDCs exhibit zero contact bounce, exceptionally low contact resistance (< 0.002Ω), and an operating lifespan exceeding 10 million cycles—over ten times that of mechanical contactors. However, MDCs have drawbacks: they must be mounted strictly in an upright vertical orientation (± 5°) to ensure proper mercury displacement, and environmental regulations (such as RoHS) are driving manufacturers toward solid-state alternatives.
When modernizing legacy Jackson dishmachines or retrofitting equipment where mercury contactors are unavailable, commercial technicians often install industrial solid-state relays (SSRs). SSRs utilize opto-isolated silicon thyristors (SCRs) to switch 480V loads with zero moving parts. However, SSRs generate substantial internal heat (approximately 1.2 watts of waste heat per ampere switched). When retrofitting an SSR into a dishmachine control box, the technician must install a properly sized aluminum heatsink and thermal transfer paste to dissipate this thermal load, preventing thermal runaway and catastrophic semiconductor punch-through.
North Fulton Hard Water Mineral Scale Accretion on Incoloy Sheathed Heating Elements
The geographic water profile of North Fulton County plays a decisive role in the lifespan of commercial warewashing components. Municipal water across Alpharetta, Milton, and Roswell is sourced primarily from the Chattahoochee River and regional groundwater reservoirs. While North Fulton water is generally classified as moderately soft to moderately hard (typically ranging from 30 to 85 parts per million of total dissolved solids, or 2 to 5 grains per gallon), its chemical behavior changes dramatically under high-temperature commercial heating.
Water contains dissolved calcium bicarbonate, $Ca(HCO_3)_2$. When water enters a commercial booster heater and is heated to 185°F, a rapid endothermic chemical decomposition occurs:
The resulting calcium carbonate ($CaCO_3$, or calcite) has an inverted solubility curve: unlike sugar or salt, calcium carbonate becomes less soluble as water temperature increases. Consequently, calcite precipitates directly onto the hottest surfaces in the system—the tubular Incoloy sheaths of the electric immersion heating elements.
Within 60 to 90 days of operation without water softening, a 1/8-inch to 1/4-inch crust of porous mineral scale encapsulates the elements. The thermal conductivity of calcium carbonate is approximately 0.8 to 1.3 $W/(mcdot K)$, compared to 15 $W/(mcdot K)$ for Incoloy alloy. This mineral blanket acts like a thermal insulator, preventing the heat generated by the internal nickel-chromium coil from transferring to the surrounding water. As a result, the internal coil temperature—normally operating around 750°F—climbs past 1,400°F. Under this intense thermal stress, the magnesium oxide dielectric insulation crystallizes, the outer metal sheath blisters and ruptures, and the heating element burns out. Installing commercial-grade catalytic or ion-exchange water softeners is the only definitive preventative barrier against this failure mode.
Three-Phase Delta Electrical Branch Circuit & Line Voltage Imbalance Telemetry
Industrial Jackson dishmachine booster heaters are wired in a three-phase Delta configuration. Understanding the mathematical relationships governing three-phase Delta electrical circuits allows commercial technicians to rapidly identify partial element failures, incoming phase loss, and supply voltage imbalances.
In a balanced three-phase Delta resistive circuit, line voltage ($V_L$) equals phase voltage ($V_P$):
The relationship between total electrical power ($P$, in watts), line voltage ($V_L$), and line current ($I_L$, in amperes) is calculated as:
For a Jackson 12 kW (12,000 W) 480V 3-phase booster heater element, the expected current draw on each line conductor during active heating is:
When diagnosing a live system with a True-RMS clamp-on ammeter, our technicians measure current on each of the three feeder conductors (L1, L2, and L3). In a healthy booster, all three phases will read between 14.1 and 14.7 Amps. If the technician measures 14.4 Amps on L1, 8.3 Amps on L2, and 8.3 Amps on L3, this severe current imbalance confirms that one internal delta leg has burned open. Furthermore, National Electrical Code (NEC) standards dictate that voltage imbalance between phases must never exceed 2%. A voltage imbalance greater than 2% indicates supply transformer defects or loose subpanel lugs that will cause uneven element heating and premature contactor degradation.
Frequently Asked Questions About Jackson Booster Heater & Dishmachine Repairs
What is the required sanitizing rinse temperature for a Jackson commercial dishmachine under Georgia health codes?
Under Georgia Department of Public Health Rules Chapter 511-6-1 and the FDA Food Code, commercial high-temperature mechanical warewashers must maintain a final sanitizing rinse manifold water temperature of at least 180°F (82°C) and not exceeding 194°F (90°C). Furthermore, this hot water rinse must elevate the actual plate surface temperature to at least 160°F (71°C) to guarantee a 5-log microbial reduction and achieve certified sanitization without chemical additives.
Why is my Jackson dishmachine final rinse water only reaching 140°F to 150°F?
If your rinse thermometer reads between 140°F and 150°F, the booster heater is not providing any thermal boost, and you are simply seeing the incoming domestic boiler water pass through unheated. The most frequent causes are an open-circuit 480V booster heating element (broken resistance wire), a tripped manual-reset high-limit bimetal thermostat, or a failed 120VAC mercury displacement contactor coil failing to close line power.
How do I test a 480V 3-phase Jackson booster heating element with a digital multimeter?
First, execute Lockout/Tagout to ensure zero electrical potential. Disconnect the element jumper wires, and set your True-RMS multimeter to the Ohms (Ω) resistance scale. Measure between each pair of terminals (L1-L2, L2-L3, L1-L3). For a standard Jackson 12kW 480V 3-phase element, each leg must read exactly 25.6Ω ± 5%. A reading of Infinite Resistance (OL) indicates a burned open element that must be replaced. Also verify insulation resistance from each pin to tank ground (> 50 MΩ).
What are the symptoms of a failed mercury displacement contactor in a commercial dishroom?
Symptoms include a silent or non-heating booster tank despite call-for-heat indicators, an open-circuit reading across coil terminals A1-A2 (nominal baseline is 45Ω on 120VAC coils), or extreme voltage drop (> 2 VAC) across the load poles while energized. Internally oxidized mercury can also cause phase-loss conditions where only one or two legs pass 480V power to the heating elements.
What causes the high-limit safety thermostat on a Jackson booster heater to trip?
The high-limit safety switch trips at 210°F when the booster vessel overheats. Common causes include thick calcium carbonate scale blanketing the elements (creating severe localized hotspots), a defective regulating thermostat that fails to de-energize the contactor, a welded contactor pole that continuously powers the elements, or low water flow causing partial dry-firing conditions.
Can I safely reset the high-limit switch on my Jackson dishmachine booster tank myself?
Yes, kitchen managers can safely press the external red reset plunger located behind the lower access aperture once the machine is powered off. If it clicks and latches, test machine operation. However, if the high-limit switch trips again during the next cycle, do not continue resetting it; an underlying dangerous over-temperature or scale condition is present and requires professional diagnostic resolution.
How often should a commercial booster heater be de-limed in North Fulton County?
In busy Alpharetta and Milton commercial kitchens operating without dedicated water softening, de-liming should be performed every 30 days. In facilities with properly maintained water softeners (< 3 GPG hardness), quarterly de-liming using an inhibited phosphoric or sulfamic acid solution is sufficient to prevent thermal insulating scale crusts.
What is the difference between a 40°F rise and a 70°F rise booster heater?
A 40°F rise booster is engineered for facilities with a commercial boiler supplying 140°F hot water, elevating it to 180°F. A 70°F rise booster features larger heating elements (typically 18kW or higher) designed for kitchens with only domestic 110°F water supplies, providing the additional 70°F lift required to reach mandatory sanitizing temperatures.
Why is dynamic water pressure so critical during the sanitizing rinse cycle?
Jackson dishmachines require dynamic water pressure between 15 and 25 PSI (optimal 20 PSI) during active spray. If pressure exceeds 25 PSI, water flows through the booster tank too quickly, failing to absorb sufficient heat and exiting below 180°F. If pressure drops below 15 PSI, the spray pattern collapses, failing to fully coat dishes and clean sanitizing surfaces.
What does an Open Loop (OL) reading on a booster heating element indicate?
An Open Loop (OL) reading on your multimeter’s resistance mode indicates infinite electrical resistance, proving that the internal nickel-chromium resistance wire has physically melted or severed. The element can no longer complete an electrical circuit and will produce zero heat until replaced.
Can hard water scale cause an Incoloy booster heating element to rupture?
Yes. Calcium carbonate scale has very poor thermal conductivity. When scale encrusts an element, heat cannot escape into the water. Internal temperatures soar past 1,400°F, causing the metal sheath to blister, split open, and ground out to the booster tank, tripping breakers and destroying the element.
Why do commercial dishwashers use mercury displacement contactors instead of standard mechanical relays?
Commercial dishmachines cycle hundreds of times daily. Standard mechanical contactors suffer contact arcing and weld shut after a few months. Mercury displacement contactors use liquid mercury pools inside hermetic steel tubes, providing arc-free, bounce-free switching rated for over 10 million cycles under heavy 480V three-phase inductive loads.
How long does a commercial booster heater heating element typically last in a busy restaurant?
In kitchens with active water softening and regular de-liming, an OEM Jackson Incoloy immersion element lasts between 4 and 7 years. In kitchens with unsoftened hard water and zero de-liming, element lifespan drops to 6 to 18 months due to rapid scale-induced thermal burnout.
What happens if our restaurant fails the Fulton County dishroom sanitizing temperature inspection?
Failing to achieve 180°F rinse temperature or 160°F plate surface temperature is categorized as a critical risk violation under Georgia Chapter 511-6-1. The dishmachine will be red-tagged out of service immediately. You must either switch to disposable single-use wares, manually wash in a three-compartment sink with chemical sanitizer, or close the kitchen until a certified repair invoice is verified by the inspector.
Should we replace individual booster heater elements or the complete booster assembly?
In over 85% of field calls, the stainless steel tank vessel is completely sound. Replacing the individual failed heating element, high-temp EPDM flange gasket, contactor, and safety thermostat restores full factory heating capacity at less than 20% of the cost of a full booster tank replacement.
How quickly can your commercial technicians respond to an emergency booster heater failure in Milton or Alpharetta?
Our dedicated commercial kitchen equipment specialists maintain fully stocked service vans carrying genuine Jackson 480V heating elements, mercury displacement contactors, high-limit switches, and flange gaskets. We offer priority same-day dispatch across Crabapple Road, Downtown Alpharetta, and Milton with arrival times typically between 45 and 90 minutes.
Commercial Warewashing & Kitchen Equipment Navigation Silos
Appliance Repair Alpharetta delivers comprehensive, factory-certified commercial foodservice equipment maintenance across North Fulton County. Explore our specialized commercial service silos to ensure peak operational reliability across your entire culinary and back-of-house line, including dedicated high-temperature commercial dishwashing systems and prep equipment:
Commercial Warewashing
Jackson, Hobart, CMA, and Champion commercial dishmachine repairs, wash pumps & chemical feeders.
Hot Side Cooking Line
Commercial ranges, convection ovens, steam kettles, deep fryers, and pizza deck ovens.
Cold Side Refrigeration
Walk-in coolers, reach-in commercial freezers, blast chillers, and prep table compressors.
Ice & Beverage Systems
Hoshizaki, Manitowoc, and Scotsman commercial ice machines, harvest cycles & bin sensors.
We also support commercial laundry systems, including commercial laundry drying units and heavy-duty commercial laundry washers for hotels, country clubs, and equestrian facilities throughout Milton and North Fulton.
Key Commercial Warewashing & Booster Maintenance Takeaways
- Mandatory 180°F Sanitization: Georgia DPH Chapter 511-6-1 legally mandates 180°F final rinse manifold water temperatures to achieve a certified 160°F plate surface thermal kill threshold.
- Nominal 25.6Ω Telemetry: Healthy Jackson 12kW 480V 3-phase booster heating elements exhibit precisely 25.6Ω (± 5%) resistance across each phase leg; an Open Loop (OL) reading confirms an element burnout.
- Mercury Contactor Integrity: The 120VAC mercury displacement contactor coil must measure approximately 45Ω; broken coils or pitted contact poles prevent high-voltage power from reaching the immersion elements.
- 210°F High-Limit Protection: High-limit bimetallic safety thermostats must maintain 0.0Ω continuity under normal operation and trip cleanly to open circuit at 210°F to prevent steam vessel rupture.
- Dynamic 15-25 PSI Water Pressure: Excessive rinse pressure (> 25 PSI) prevents water from absorbing sufficient heat inside the booster tank, causing under-temperature rinse cycles.
- Aggressive De-Liming Mandate: In North Fulton County’s municipal water, booster tanks must be de-limed monthly to eliminate calcium carbonate blankets that cause element sheath blistering and burnout.
- Component Rebuild Cost Advantage: Rebuilding Jackson booster heaters with OEM elements and contactors saves 80% compared to premature machine replacement and restores 100% factory sanitizing performance.
Emergency Commercial Warewashing Repair & Same-Day Tech Dispatch
When your Jackson commercial dishmachine rinse temperature drops below health department standards, dinner service cannot wait. Appliance Repair Alpharetta provides emergency same-day commercial foodservice equipment restoration across Crabapple Road, Milton, Downtown Alpharetta, Roswell, and North Fulton County. Our master certified technicians arrive in fully equipped service vehicles with genuine OEM Jackson heating elements, mercury displacement contactors, high-limit thermostats, and calibrated True-RMS diagnostic instruments to resolve your warewashing crisis on the first visit.
Restore Your Commercial Dishroom Sanitation Today
Don’t let a cold sanitizing rinse shut down your dining room or fail a health inspection. Call our North Fulton commercial dispatch center now for priority emergency technician arrival.
Call (770) 796-7742 for Same-Day Dispatch
Licensed & Insured Commercial Foodservice Specialists • 90-Day Parts & Labor Warranty on All Restorations