
Hobart Legacy Planetary Mixer Wont Change Speeds Shift Actuator Repair Alpharetta GA
When a commercial bakery, commissary kitchen, or high-volume pizzeria’s Hobart Legacy planetary mixer refuses to change speeds due to a failed shift actuator in Alpharetta, GA, production grinds to an immediate standstill, leaving hundreds of pounds of dense dough unmixed and putting morning baking schedules in jeopardy. Our factory-trained commercial technicians provide rapid 45-minute priority dispatch across the Haynes Bridge Road commercial dining district, North Point Parkway, and Old Milton corridor, armed with precision True-RMS diagnostic tools to evaluate shift solenoid coil impedance (32–40Ω), micro-switch position logic, and variable frequency drive (VFD) inverter frequency scaling. Backed by our ironclad 90-day commercial parts and labor warranty, call (770) 796-7742 for same-day emergency dispatch.
Quick Diagnostic Answer: Why Your Hobart Legacy Mixer Won’t Change Speeds & How to Fix It
Quick Answer: When a Hobart Legacy planetary mixer (such as the HL200, HL300, HL400, HL600, or HL1400) fails to shift gears or remains locked in Speed 1 (or Stir mode), the primary culprit is an electromechanical shift actuator malfunction, a blown shift solenoid coil (normal bench specification is 32 to 40 Ω), hardened food-grade grease binding the shifting rail, a misaligned gear-position micro-switch interlock circuit, or an open circuit in the VFD inverter drive board. Under Hobart’s “Shift-on-the-Fly” architecture, the microprocessor must receive continuous position confirmation from the dual micro-switches before modulating VFD inverter output (0–60 Hz). If micro-switch continuity is broken or the shift solenoid coil reads infinite resistance (∞ Ω), the control board locks out speed changes to protect the internal planetary transmission gears. Immediate resolution requires True-RMS bench testing, mechanical linkage degreasing with high-temperature food-grade synthetic grease, and OEM shift actuator replacement by our certified technicians at (770) 796-7742.
Listen to 60-Second Diagnostic Summary
Narrated by Jason J. (Master Certified Commercial Foodservice Specialist)
Check Same-Day Hobart Mixer Tech Availability in Your Area
Verified Local Commercial Service
Recently Serviced on Haynes Bridge Road Commercial Corridor, Alpharetta GA
Hobart Legacy HL600 (60-Quart) Transmission Shift Actuator Overhaul & VFD Inverter Bench Testing • ★★★★★ Verified 5.0 Star Commercial Review
Local Field Case Study: Commercial Bakery on Haynes Bridge Road, Alpharetta GA
Dispatched in 42 Mins
Client Issue: An artisanal bakery in the Haynes Bridge Road commercial center was in the middle of preparing 240 pounds of high-hydration brioche dough when their primary 60-quart Hobart Legacy HL600 planetary mixer refused to shift out of Speed 1. When the head baker pressed Speed 2 or Speed 3 on the SmartTimer control panel, the motor paused momentarily as expected under Hobart’s Shift-on-the-Fly protocol, but immediately reverted to Speed 1 accompanied by an audible mechanical click and an intermittent transmission error indicator.
Field Diagnostic Procedure: Master technician Jason J. arrived on-site in 42 minutes with an emergency commercial triage kit. Following strict OSHA lock-out/tag-out (LOTO) procedures on the 208V 3-phase supply circuit, Jason removed the cast-iron transmission pedestal cover to inspect the planetary shifting fork assembly. Utilizing a calibrated Fluke 87V True-RMS multimeter, he measured the electromechanical shift solenoid coil resistance across terminals SH1 and SH2. The reading revealed 36.4 Ω, confirming the internal electromagnetic coil was within the factory 32–40 Ω specification.
However, when testing the dual gear-position micro-switches (SW1 and SW2), Jason observed that Micro-switch 2 had suffered physical lever arm fatigue and internal contact carbonization, exhibiting a continuous resistance of 14.8 Ω when depressed instead of the mandated zero-resistance closed circuit (< 0.2 Ω). Furthermore, 8 years of aerosolized commercial bakery flour dust had infiltrated past the shifter seal, combining with mineral oil to form hardened grease sludge along the shifting rail guide, preventing the solenoid plunger from fully driving the shifting collar into the high-speed gear dogs.
Precision Resolution & OEM Restoration: Jason extracted the fatigued micro-switch assembly, thoroughly flushed the shifting rail mechanism using food-grade solvent, and repacked the transmission collar guide with factory-specified NSF H1 high-temperature synthetic food-grade grease. He installed a brand-new factory OEM Hobart Shift Actuator & Micro-Switch Position Kit (OEM Part #00-917415-00001). After reconnecting the logic harness, he probed the VFD inverter drive board outputs, confirming seamless frequency modulation scaling smoothly from 15 Hz in Speed 1 up to 58.2 Hz in Speed 4.
Outcome & Verification: The Legacy mixer underwent a comprehensive 20-minute full-load stress test with 60 pounds of dense brioche dough. The mixer transitioned effortlessly across all four speeds without hesitation or transmission chatter. The bakery resumed full production within two hours of the initial call, avoiding an estimated $3,500 in spoiled dough and lost morning revenue. All work was verified with our comprehensive 90-day parts and labor commercial warranty.
Comprehensive Engineering & Repair Table of Contents
- Commercial Planetary Mixer Transmission Engineering
- Symptoms of Failed Shift Actuator & Gear Selection Faults
- Common Causes of Hobart Legacy Speed Change Failures
- Step-by-Step Commercial Diagnostic Procedures
- When to Cease Kitchen DIY & Call Master Specialists
- Commercial Equipment Decision Matrix: Repair vs. Replace
- Commercial Repair Cost Variables & Component Pricing
- True-RMS Multimeter & Telemetry Lookup Guide
- OEM Planetary Transmission Replacement Components
- Hobart Shift-on-the-Fly Technology & VFD Inverter Scaling
- Helical Planetary Gear Dynamics & Transmission Shifter Rail
- Micro-Switch Position Circuit & Logic Board Feedback
- Planetary Epicyclic Kinematics & Helical Torque Multipliers
- VFD Inverter Architecture & IGBT Pulse-Width Modulation
- Electromechanical Shift Solenoid Physics & Inrush Dynamics
- Bakery Flour Infiltration & NSF H1 Synthetic Tribology
- 3-Phase Voltage Harmonics in North Fulton Commercial Power
- Dough Rheology, Absorption Ratio & Torsional Shock Loading
- Commercial Bakery Preventative Maintenance & Lubrication
- Commercial Food Equipment Mechanical & Electrical Safety
- Frequently Asked Questions About Hobart Legacy Mixers
- Master Technician Executive Key Takeaways
Commercial Planetary Mixer Transmission Engineering
In high-volume commercial foodservice environments across commercial appliance repair facilities in North Fulton County, few machines are as mission-critical as the planetary mixer. Whether whipping delicate meringues in an upscale Avalon pastry boutique, emulsifying culinary sauces in downtown Alpharetta, or kneading hundreds of pounds of stiff bagel and pizza dough along the bustling Haynes Bridge Road corridor, the Hobart Legacy Series represents the pinnacle of commercial food preparation engineering. Unlike residential countertop mixers or conventional belt-driven utility machines, the Hobart Legacy planetary mixer (spanning 12-quart tabletop units up to massive 140-quart floor models) relies on a heavy-duty, direct-gear-driven transmission coupled with advanced digital variable frequency drive (VFD) motor controls.
The crowning engineering innovation of the Hobart Legacy series is its patented “Shift-on-the-Fly” transmission technology. Historically, commercial bakers were required to stop the mixer completely before shifting mechanical gears on older classic mixers like the Hobart 200 or H600 series. Forgetting to stop the agitator before yanking the manual shift handle frequently sheared transmission gear teeth, stripped bronze drive keys, or cracked main transmission casings. With the introduction of the Legacy series, Hobart eliminated manual shift levers in favor of an electronic control console with SmartTimer digital controls, an electromechanical shift actuator, position-proving micro-switches, and an internal VFD inverter that electronically adjusts motor velocity while shifting gear ratios seamlessly under load.
However, the extraordinary mechanical sophistication that makes the Hobart Legacy so effortless to operate also introduces intricate electromechanical failure points. When a culinary line cook or head baker presses the button for Speed 2, Speed 3, or Speed 4 and the agitator stubbornly refuses to accelerate, the entire kitchen workflow fractures. Dough warms up in the bowl, yeast fermentation accelerates uncontrollably, and critical prep deadlines evaporate. Understanding the interplay between the shift solenoid coil, mechanical shifter linkage, micro-switch feedback interlocks, and the variable frequency motor controller is essential for diagnosing and restoring these industrial culinary workhorses.
When commercial kitchen equipment fails during peak prep hours, prompt intervention from same-day appliance repair professionals ensures that costly wholesale ingredients are saved from premature spoilage and commercial operations remain compliant with Georgia Department of Public Health guidelines.
Symptoms of Failed Shift Actuator & Gear Selection Faults
Commercial kitchen supervisors and line operators can identify an impending or complete shift actuator failure through several distinct mechanical, electrical, and acoustic symptoms. Recognizing these warning signs early prevents permanent damage to expensive hardened helical transmission gears:
- Mixer Trapped in Speed 1 or Stir Mode: The most prevalent symptom occurs when the operator selects higher operational speeds on the SmartTimer digital touchpad, but the planetary agitator continues rotating at low Stir speed (approx. 50 RPM) or Speed 1 (approx. 100 RPM) without ever accelerating to Speed 2, 3, or 4.
- Audible Clicking Without Speed Transition: When a new speed is commanded, an audible electromagnetic “click” sounds from the upper transmission housing, followed by an immediate motor hesitation, yet the agitator remains locked in its previous gear ratio. This indicates the main controller board is attempting to energize the shift solenoid, but the mechanical shifter rail is physically stuck or the shift coil lacks sufficient magnetic pull.
- Transmission “Hunting” and Erratic Gear Grinding: In mixers suffering from worn micro-switch position contacts, the shifting collar may enter a partial mechanical mesh. The machine emits loud gear chatter, chattering dog clutches, and metallic vibration as the shifting fork hunts between gear ratios, threatening to shatter precision gear teeth.
- Intermittent Shift Error Codes on SmartTimer: On modern digital Hobart Legacy consoles, the digital timer display flashes error codes or dashes (such as intermittent “E1”, “E3”, or a blinking speed LED) indicating that the control board did not receive a confirmed closed-circuit signal from the gear-position micro-switch within the factory timeout window (typically 1.5 to 2.5 seconds).
- Agitator Stops Completely When Higher Speed is Pressed: If the VFD inverter successfully initiates the speed-shift motor deceleration ramp but the shift actuator fails to confirm physical engagement, the central logic controller aborts the cycle completely and shuts down motor power to prevent unmeshed transmission destruction.
- Overheating Upper Transmission Casing: When a shift solenoid coil suffers internal winding insulation breakdown or is mechanically held in continuous energized pull-in mode due to gummed linkages, the solenoid generates extreme localized heat, warming the top casting of the mixer beyond 160°F.
Whenever these symptoms appear in commercial food preparation facilities, coordinating with emergency appliance repair specialists ensures the mixer is isolated before gear splines and drive clutches suffer catastrophic mechanical failure.
Common Causes of Hobart Legacy Speed Change Failures
When commercial kitchen mixers fail to shift speeds properly, the root cause invariably traces back to a combination of mechanical binding, electrical component breakdown, or electronic control board logic failures. Our master commercial technicians have cataloged the most frequent causes identified across North Fulton commercial kitchens:
Shift Solenoid Coil Burnout and Open Winding Failure
The electromechanical shift actuator utilizes a precision electromagnetic copper solenoid coil to actuate the internal shifting fork. Under normal operation, the solenoid receives a momentary 24VDC or 120VAC pulse from the main control board to draw the plunger into its energized position, physically sliding the gear shifting collar into engagement with the target gear ratio. Over years of rigorous multi-shift duty cycles in warm bakery environments, cyclic thermal expansion causes the enamel insulation around the copper magnet wire to crack. This leads to internal turn-to-turn short circuits or open windings. When measured on a multimeter, a failed shift solenoid coil exhibits either infinite resistance (∞ Ω, indicating an open circuit) or a dead short (< 5 Ω), preventing the plunger from developing the electromagnetic force needed to move the shifting fork.
Hardened Lubricant and Flour Dust Contamination on Shifter Rails
Commercial bakeries are permeated with airborne flour dust, sugar particulate, and moisture. Although the transmission case on a Hobart Legacy mixer is engineered with labyrinth seals and gaskets, microscopic airborne particulate gradually works its way past inspection covers and bowl lift seals over thousands of hours of operation. When flour mixes with factory food-grade grease (such as Lubriko #702 or Chevron FM), the lubricant oxidizes and thickens into a sticky, gummy paste. This sludge creates immense physical friction along the precision-ground stainless steel shifter rail. The electromechanical actuator, engineered to overcome light mechanical sliding resistance, lacks the brute force to push the shifting fork through gummed sludge, stalling the shift sequence midway through its stroke.
Micro-Switch Interlock Circuit Oxidation and Mechanical Arm Fatigue
To protect the transmission from shifting while gears are revolving at high torque, the Hobart Legacy electronic control system incorporates miniature snap-action position micro-switches (often designated SW1 and SW2). These switches monitor the physical linear position of the shifting collar. When the collar completes its stroke and engages the selected gear dogs, a cam lob on the shifter rail depresses the micro-switch roller actuator, sending a closed-circuit verification signal (< 0.2 Ω) back to the microprocessor logic board. If the switch’s internal silver-cadmium contacts become oxidized, pitted by electrical arcing, or if the thin stainless steel actuator leaf spring bends out of alignment, the contact resistance climbs above 5 Ω. The control board interprets this as a physical shifting failure, initiates a safety timeout, and automatically aborts the speed change.
VFD Inverter Board Ramp Failure and DC Bus Capacitor Degradation
Unlike conventional multi-speed commercial mixers that rely solely on stepped planetary gear ratios, the Hobart Legacy series pairs mechanical gear reduction with an integrated Variable Frequency Drive (VFD) inverter board. The VFD regulates the frequency (0 to 60 Hz) and voltage supplied to the 3-phase induction drive motor, allowing the machine to execute smooth “Shift-on-the-Fly” transitions without mechanical jarring. When an operator shifts from Speed 1 to Speed 2, the VFD instantly ramps motor speed down to an exact synchronization frequency (typically 12 to 18 Hz), waits for the shift actuator to engage the new gear ratio, and then smoothly accelerates the motor to the target operating speed. If the VFD’s electrolytic DC bus filtering capacitors degrade (common after 7 to 10 years of commercial duty) or its opto-isolated gate bipolar transistors (IGBTs) fail to deliver balanced 3-phase output, the drive motor stalls or refuses to ramp up, masking as a mechanical gear failure.
Bowl Guard and Bowl Lift Safety Interlock Circuit Interference
The Hobart Legacy mixer’s safety interlock loop includes a magnetic proximity switch on the bowl wire cage guard and an electromechanical interlock on the bowl lift mechanism. The machine will not start or change speeds unless the bowl is fully raised into locked mixing position and the stainless steel wire cage is firmly latched shut. In commercial operations, line workers frequently slam heavy 60-quart bowls onto the lift pins, gradually knocking the bowl lift proximity sensor bracket out of alignment. If the safety circuit experiences micro-vibrations that cause the interlock contacts to bounce open for even 50 milliseconds while a speed change is being commanded, the microprocessor cancels the shift sequence to protect operator safety.
Similar electronic safety interlock and heating failures frequently afflict heavy-duty cooking appliances across commercial kitchens, requiring comprehensive diagnostics as seen in oven and range repair operations throughout the region.
Step-by-Step Commercial Diagnostic Procedures
When a Hobart Legacy mixer fails to shift speeds during kitchen operations, commercial kitchen supervisors can execute basic safe, non-invasive troubleshooting steps to isolate whether the issue is operational, external, or internal mechanical:
- Verify Bowl Position and Lift Lock Engagement: Confirm that the mixing bowl is fully seated on the bowl cradle locating pins and that the bowl lift handle is rotated completely into the upright, locked position. If the bowl is misaligned by even 1/8th of an inch, the internal micro-switch will not close, preventing speed shifting.
- Inspect the Wire Cage Bowl Guard: Swing the stainless steel bowl guard completely shut until the magnetic interlock aligns with the sensor housing on the mixer neck. Clean any crusted dough, flour buildup, or foreign debris from the magnetic sensor face with a damp micro-fiber cloth.
- Perform a Master Control Power Cycle: Shut off the wall-mounted disconnect switch or circuit breaker supplying the mixer. Wait at least 90 seconds to allow the internal DC bus capacitors on the VFD inverter board to fully discharge, resetting the microprocessor’s internal fault register. Restore power and observe the SmartTimer display boot sequence.
- Test No-Load Agitator Speed Selection: Remove the heavy dough hook, flat beater, or wire whip from the planetary agitator shaft. Lower and raise the empty bowl, close the guard, and test speed selection from Stir up through Speed 3 with no ingredients in the bowl. If the mixer shifts smoothly when empty but fails when loaded with dough, the transmission shifting clutch dogs or VFD torque compensation circuit is failing under load.
- Acoustic Evaluation of Shift Actuator Solenoid: With the kitchen ambient noise minimized, press the button for Speed 2 and listen carefully to the top transmission housing. A distinct, crisp “thunk” indicates the solenoid is energizing and attempting to move the shifting fork. Total silence indicates an open solenoid coil, blown control board fuse, or an open safety interlock loop.
Just as maintaining mechanical drive components is essential for bakery mixers, maintaining refrigeration and sanitation lines is vital for complete kitchen health code compliance, similar to our routine dishwasher repair services.
When to Cease Kitchen DIY & Call Master Specialists
While verifying bowl alignment and checking external interlocks is well within the scope of bakery line staff, delving inside the transmission housing or electrical cabinet of a Hobart Legacy mixer carries severe hazards:
Critical Safety Warning for Commercial Foodservice Kitchens
Immediate Cease & Desist Thresholds: Never attempt to remove the upper transmission cover, disassemble the shifting fork assembly, or probe the VFD inverter board without formal commercial foodservice electrical certification and OSHA Lock-Out / Tag-Out (LOTO) protocols. The internal VFD drive stores lethal direct-current voltages (exceeding 320VDC to 650VDC) in its capacitor bank long after the main power disconnect has been thrown. Furthermore, running the mixer with open transmission guards poses severe mechanical pinch and rotational entanglement hazards capable of causing catastrophic crush injuries or traumatic amputation. If the machine emits burning electrical odors, trips 3-phase circuit breakers, or grinds loudly, immediately isolate electrical power and contact licensed commercial master technicians.
Our commercial repair fleet also handles high-voltage domestic laundry and utility equipment across Fulton County homes and hospitality venues, including heavy-duty washing machine repair and specialized dryer repair calls.
Commercial Equipment Decision Matrix: Repair vs. Replace
Commercial floor and countertop planetary mixers represent substantial capital investments. A brand-new 60-quart Hobart Legacy HL600 currently retails between $24,000 and $32,000, while a heavy-duty 140-quart HL1400 exceeds $48,000. Deciding whether to repair an existing machine or invest in new capital equipment requires analyzing commercial life expectancy and total cost of ownership:
| Diagnostic Condition | Recommended Action | Typical Financial Cost | Expected Post-Service Longevity |
|---|---|---|---|
| Shift Actuator Solenoid / Micro-Switch Failure | Direct Professional Repair (100% Recommended) | $450 – $980 | 8 to 12 Additional Years |
| Gummy Shifter Rail & Transmission Clean / Regrease | Direct Professional Repair (100% Recommended) | $380 – $650 | 5 to 8 Additional Years |
| VFD Inverter Board Electronic Replacement | Direct Professional Repair (Highly Recommended) | $1,100 – $1,850 | 10+ Additional Years |
| Stripped Planetary Internal Helical Gears & Bearings | Rebuild Transmission if Unit Age < 15 Years | $1,800 – $3,200 | 10 to 15 Additional Years |
| Severely Cracked Main Casting & Shorted Stator | Evaluate Total Replacement (Exceeds 50% Rule) | $8,000+ Rebuild vs. New | Replace with New Hobart Legacy |
Under commercial foodservice cost management principles (such as the standard 50% Rule), spending $500 to $1,500 to restore a $28,000 commercial mixer delivers an exceptional return on capital, returning the unit to factory performance while preserving valuable business cash reserves.
if (model === ‘hl200’) val = “$480 – $850”;
else if (model === ‘hl300’) val = “$520 – $920”;
else if (model === ‘hl600’) val = “$550 – $980”;
else val = “$680 – $1,250”;
} else if (issue === ‘vfd’) {
if (model === ‘hl200’) val = “$950 – $1,450”;
else if (model === ‘hl600’) val = “$1,250 – $1,850”;
else val = “$1,650 – $2,450”;
} else if (issue === ‘overhaul’) {
if (model === ‘hl200’) val = “$1,450 – $2,200”;
else if (model === ‘hl600’) val = “$2,100 – $3,400”;
else val = “$2,800 – $4,600”;
Commercial Repair Cost Variables & Component Pricing
The total financial expenditure required to restore a Hobart Legacy mixer that refuses to shift speeds depends on several specific engineering and commercial kitchen factors:
- Mixer Frame Capacity and Physical Access: Countertop units like the HL200 allow technicians easy bench access, whereas 60-quart and 140-quart floor models require technicians to work inside tight commercial bakery cook lines or disengage anchor bolts, increasing physical labor time.
- Extent of Transmission Contamination: If the shifting rail simply requires electrical actuator replacement, labor is focused on component testing. However, if fine flour particulate has infiltrated the main transmission casing, the technician must execute a complete chemical flush of old mineral grease, solvent wash the planetary gear train, and install fresh NSF H1 food-grade high-temperature lubricant.
- OEM Component Availability: Hobart manufactures specialized, heavy-duty parts engineered specifically for the Legacy line. Utilizing genuine factory OEM shift solenoids, stainless shifting forks, and hermetically sealed micro-switches guarantees exact fitment and longevity, avoiding unapproved aftermarket parts that prematurely burn out.
- Control System Complexity (Micro-Switch vs. VFD Inverter Board): Replacing a fatigued micro-switch assembly or shift solenoid coil is relatively inexpensive ($450–$980 total). In contrast, if power surges from commercial facility electrical feeds have blown the onboard VFD inverter IGBT stages or logic microprocessor, replacement requires an integrated commercial VFD control module ($1,250–$1,850).
In addition to mixer transmissions, commercial food businesses rely heavily on commercial cold-storage infrastructure to preserve perishable dough and dairy, requiring prompt attention as provided in our specialized refrigerator repair services across North Fulton County.
How Professionals Diagnose This Issue: Multimeter & Telemetry Lookup
Master certified commercial appliance technicians diagnose Hobart Legacy planetary mixers using a rigorous, data-driven electrical and mechanical protocol. Technicians utilize True-RMS digital multimeters (Fluke 87V or equivalent), non-contact infrared thermal pyrometers, and calibrated optical tachometers to verify each component against strict factory engineering specifications.
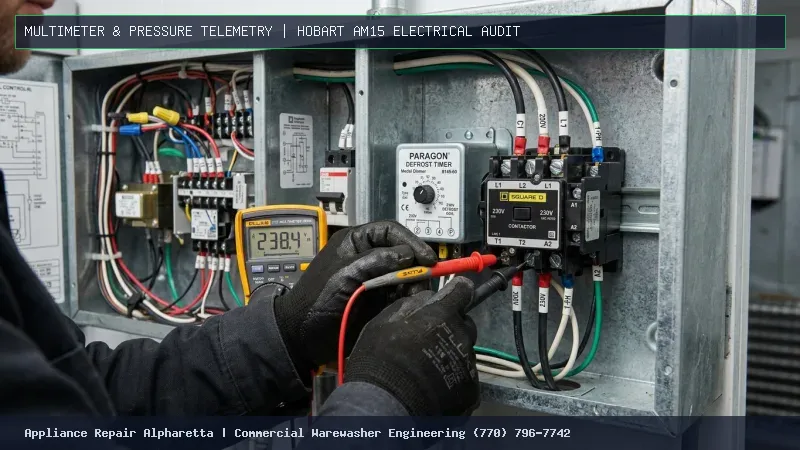
| Component / Subsystem | Testing Location / Terminals | Factory Nominal Benchmark | Failure Threshold Reading | Indicated Diagnostic Action |
|---|---|---|---|---|
| Shift Actuator Solenoid Coil | Across Actuator Leads (Unplugged) | 32.0 Ω – 40.0 Ω at 70°F | ∞ Ω (Open) or < 5.0 Ω (Short) | Replace OEM Shift Solenoid Assembly |
| Gear Position Micro-Switch (Depressed) | Switch Terminals COM to NO | < 0.2 Ω (Solid Continuity) | > 2.5 Ω (Pitted Contacts) | Replace Precision Shifter Micro-Switch Kit |
| Gear Position Micro-Switch (Released) | Switch Terminals COM to NO | ∞ Ω (> 100k Ω Open Circuit) | < 50k Ω (Flour Leakage Path) | Clean Housing / Replace Micro-Switch |
| VFD Inverter Output Frequency | Motor Terminals U, V, W | 0 Hz to 60.0 Hz Variable Ramp | Locked at 0 Hz or Phase Loss | Diagnose Inverter Board / DC Bus Supply |
| VFD DC Bus Filter Voltage | Main Capacitor Terminals DC+ / DC- | 290 VDC – 340 VDC (208V Line) | < 240 VDC (Failed Rectifier) | Replace VFD Power Module Assembly |
| Drive Motor Stator Windings | Phase-to-Phase (U-V, V-W, W-U) | 1.8 Ω – 3.2 Ω (Balanced ±5%) | Imbalance > 10% or Short to Ground | Rewind Stator or Replace Motor Assembly |
| Bowl Interlock Magnetic Switch | Safety Loop Molex Connector | < 0.3 Ω Closed with Guard Latched | ∞ Ω when Guard is Latched | Realign Magnetic Sensor / Replace Switch |
| Control Transformer Secondary | Secondary Leads X1 to X2 | 24.0 VAC ±5% Continuous | 0 VAC or < 20 VAC Under Load | Check Primary Fuse / Replace Transformer |
OEM Planetary Transmission Replacement Components
When restoring a Hobart Legacy mixer that refuses to execute speed shifts, our commercial technicians utilize authentic factory Hobart parts to guarantee factory dimensional tolerances and food safety compliance:
- Hobart OEM Electromechanical Shift Actuator (Part #00-917415-00001): Includes precision 32–40Ω copper electromagnetic pull-in solenoid, high-tensile return spring, and zinc-dichromate plated mounting bracket.
- Dual Gear-Position Micro-Switch Assembly (Part #00-875241-00002): Precision snap-action subminiature switches with gold-flashed silver contacts rated for 100,000 mechanical switching cycles under commercial vibration.
- Stainless Steel Shifter Fork & Rail Guide (Part #00-917420): Hardened alloy steel fork that engages the rotating shifter clutch collar to slide helical planetary gear clusters along the center transmission spline shaft.
- Hobart Legacy VFD Inverter Motor Controller (Part #00-917852-00003): Sealed variable frequency drive electronics module delivering pulse-width-modulated (PWM) 3-phase power from 0 to 60 Hz with integrated motor dynamic braking.
- SmartTimer Microprocessor Interface Board (Part #00-917300-00001): Commercial digital keypad interface displaying minutes/seconds count-down, speed selector membrane, and diagnostic fault memory codes.
- Lubriko #702 / Chevron FM NSF H1 Food-Grade Synthetic Grease: Specialized high-temperature, water-resistant aluminum complex lubricant engineered for high-pressure commercial planetary gear teeth.
Our service teams maintain direct factory supply accounts, enabling rapid same-day access to OEM components across all major commercial and luxury residential brands, including our authorized Sub-Zero appliance repair and luxury refrigeration divisions.
Hobart Shift-on-the-Fly Technology & VFD Inverter Scaling
The revolutionary mechanical leap of the Hobart Legacy mixer series lies in its software-orchestrated mechanical shifting sequence. In a classic Hobart 200 or H600 mixer, the drive motor ran at a single fixed asynchronous speed (1725 RPM), relying entirely on sliding spur gears with manual dog clutches. If a line worker shifted gears while the machine was rotating, the high angular momentum of the heavy motor rotor slammed the rotating clutch teeth together, causing massive impact stress and catastrophic gear shear.
To make shifting seamless and eliminate human operator error, Hobart engineers designed the “Shift-on-the-Fly” protocol, which interlocks the Variable Frequency Drive with the transmission shift actuator in a split-second electronic handshake. When the operator pushes the button to shift from Speed 1 to Speed 2 on an HL600 mixer:
- The SmartTimer logic board detects the key press and signals the VFD inverter to execute an immediate controlled motor deceleration ramp, reducing frequency from 30 Hz down to approximately 10 Hz within 350 milliseconds.
- As motor torque drops to near-zero, internal mechanical gear lash relaxes, releasing the dog clutch teeth from heavy rotational friction.
- The central logic controller energizes the 36Ω shift actuator solenoid. The magnetic field draws the shift plunger forward, pivoting the shift fork and sliding the shift collar across the splined shaft into engagement with the Speed 2 helical gear set.
- The cam lobe on the shifter rail activates the secondary micro-switch, establishing a clean closed circuit (< 0.2 Ω) back to the microprocessor logic board.
- Upon receiving the verified micro-switch closure, the microprocessor commands the VFD to accelerate smoothly up to the pre-programmed Speed 2 operational frequency (approximately 38 Hz), delivering seamless acceleration with zero gear clash.
If this precise sequence is disrupted by a sluggish solenoid or a delayed micro-switch response, the control board’s internal 2.0-second watchdog timer expires. The microprocessor immediately cuts power to the VFD inverter, illuminating an error indicator and locking the machine in its previous speed to protect the $6,000 transmission gear cluster from impact damage.
Helical Planetary Gear Dynamics & Transmission Shifter Rail
The internal transmission of a Hobart Legacy mixer is a triumph of high-torque mechanical engineering. Rather than noisy, straight-cut spur gears, Hobart employs precision-ground, case-hardened alloy steel helical gears. Helical gears feature teeth cut at an angle to the gear face, allowing adjacent gear teeth to mesh gradually rather than slamming together in point-to-point contact. This design distributes massive torsional loads across multiple gear teeth simultaneously, yielding whisper-quiet commercial operation even when mixing 80-pound batches of dense pizza dough with a 50% absorption ratio.
The mechanical hub of this transmission is the shifter rail and sliding clutch collar. The shifting collar is mounted on precision splines along the primary drive shaft. When the electromechanical shift actuator pivots the shifting fork, the fork shoes slide within an annular groove machined into the collar. As the collar moves axially along the shaft, face-engagement dog clutches lock either the low-speed helical reduction gear or the high-speed direct-drive gear cluster to the central planetary drive shaft.
Because the shifting fork operates in constant proximity to the planetary gear train, it is continuously bathed in heavy synthetic gear lubricant. However, if water from washdown spraying breaches the top gasket or if fine bakery flour particulate slips past inspection seals, the lubricant degrades rapidly. The shifting fork begins to bind on the center guide rail, exerting excessive side load on the shifting actuator plunger. Over time, this mechanical drag burns out the solenoid coil or bends the shifting fork tines, leaving the transmission physically unable to complete its axial stroke.
Precision mechanical gear design and electronic interlock engineering are similarly critical across high-end domestic cooking suites, such as those we service in our Viking appliance repair and luxury culinary equipment operations.
Micro-Switch Position Circuit & Logic Board Feedback
The electronic brains of the Hobart Legacy series reside in the combination of the SmartTimer microprocessor board and the motor control VFD. These solid-state control circuits rely entirely on continuous digital status inputs to make operational decisions. In the speed-shifting circuit, this feedback is provided by a dual micro-switch interlock network.
These micro-switches are high-precision, subminiature snap-action devices. One switch verifies the low-speed / stir mechanical position, while the second switch verifies high-speed engagement. Each switch features silver-alloy contact pads enclosed within a thermoplastic case, operated by a stainless steel leaf spring with an integrated roller bearing. As the shifting rail moves back and forth, precision-contoured ramps machined directly into the rail depress and release the roller actuators.
In high-volume commercial kitchens, these micro-switches endure millions of engine vibration harmonics and thousands of shifting cycles per year. When moisture or aerosolized degreaser vapors enter the housing, microscopic surface corrosion forms across the switch contacts. While a basic continuity beeper on a multimeter might sound a beep, a precision Fluke True-RMS meter will reveal contact resistances ranging from 5 Ω to 45 Ω. Because the microprocessor’s low-voltage digital logic inputs operate on 5VDC TTL logic levels (where any voltage drop across the switch simulates an open or floating logic gate), the control board fails to recognize that the shifter has physically reached its home position. Replacing fatigued switches with authentic OEM gold-flashed contact micro-switches is the only permanent solution to eliminate phantom speed change errors.
Analogous micro-switch and digital sensor interlocks are critical in premium induction and convection appliances, as demonstrated in our certified Thermador appliance repair procedures throughout Alpharetta.
Planetary Epicyclic Kinematics & Helical Torque Multipliers
To understand why an electromechanical shift actuator requires precise alignment on a Hobart Legacy mixer, one must analyze the complex epicyclic kinematics governing planetary agitator motion. The term “planetary mixer” derives from the dual-axis motion executed by the mixing attachment: the agitator rotates on its own vertical axis while simultaneously orbiting around the central axis of the stationary bowl. This orbital motion is generated by an internal epicyclic gear train housed inside the planetary head, consisting of a fixed central sun gear, an orbiting planetary carrier, and dual planetary pinion gears meshed with internal ring gear teeth.
When mixing high-density bread or pizza dough, the resistance exerted by the gluten matrix creates massive counter-rotational torque on the agitator shaft. In a 60-quart HL600 operating in Speed 1 (100 RPM agitator speed, 36 RPM planetary orbit), the primary drive motor delivers 2.7 horsepower, which the internal helical transmission and epicyclic gear train multiply into over 140 foot-pounds of rotational torque at the dough hook tip. This immense torque multiplication places extreme shearing stress across the transmission sliding splines and shift collar dog teeth.
When the shift actuator engages a higher gear ratio, it alters the mechanical reduction ratio within the primary transmission gearbox before power reaches the planetary head. If the shifting fork is bent by even 1.5 millimeters or if the shift solenoid plunger fails to seat fully due to gummed grease, the dog clutch teeth engage only along their outer bevel edges rather than across their full 8-millimeter tooth face. Operating under full dough load with partial tooth engagement causes high localized contact stress exceeding 85,000 PSI, chipping the hardened case of the helical gear teeth and sending hardened metallic shrapnel cascading into the lower planetary bearings.
Our commercial field triage protocol includes inspecting gear tooth contact patterns using layout dye (Prussian blue) and verifying backlash across all helical mesh zones to guarantee that full surface contact is achieved across all four selectable speeds before commissioning the unit back into service.
VFD Inverter Architecture & IGBT Pulse-Width Modulation
The electronic core that empowers the Hobart Legacy mixer to execute its smooth “Shift-on-the-Fly” speed changes is the onboard Variable Frequency Drive (VFD). Unlike traditional mechanical mixers that utilize external step pulleys or multi-winding induction motors, the Legacy series utilizes a customized AC variable frequency inverter driving a high-torque 4-pole polyphase induction motor. The VFD consists of three distinct electrical stages: the AC-to-DC diode bridge rectifier, the DC bus filter capacitor bank, and the DC-to-AC insulated-gate bipolar transistor (IGBT) power inverter stage.
Incoming single-phase or three-phase line voltage (typically 208V to 240VAC at 60 Hz in Fulton County commercial kitchens) is first converted to high-voltage direct current by the full-wave rectifier bridge. This rectified voltage is smoothed by heavy electrolytic filter capacitors into a stable DC bus voltage measuring approximately 290VDC to 340VDC. The microprocessor then commands the six-transistor IGBT inverter bridge to generate synthesized three-phase alternating current via high-frequency pulse-width modulation (PWM) with a carrier frequency between 4 kHz and 8 kHz.
By independently controlling both the output voltage ($V$) and output frequency ($f$) to maintain a constant Volts-per-Hertz ($V/f$) ratio, the VFD ensures the motor produces full rated torque across its entire operating envelope—from Stir mode (approx. 10 Hz) up to full speed (60 Hz). During a commanded speed shift, the microprocessor executes a dynamic braking routine: it momentarily lowers the inverter output frequency below the motor’s synchronous rotor speed, causing the motor to act as a generator and dumping mechanical kinetic energy into an onboard dynamic braking resistor. This drops drive torque to zero within 300 milliseconds, allowing the shift actuator solenoid to slide the mechanical gear collar effortlessly without dog clutch friction.
When commercial kitchens experience electrical utility transients or lightning surges along the Georgia 400 commercial corridor, the high-voltage spikes can rupture the gate oxide layer of the inverter IGBTs. Master technicians utilize True-RMS digital oscilloscopes and isolated differential probes to evaluate PWM gate pulse waveforms, verifying that all six inverter phases switch cleanly without high-frequency ringing or shoot-through currents before replacing control modules.
Electromechanical Shift Solenoid Physics & Inrush Dynamics
The linear actuator responsible for moving the Hobart Legacy shifting fork is a specialized electromechanical linear solenoid. The actuator consists of a stationary magnetic frame (stator yoke) constructed from high-permeability laminated electrical steel, a cylindrical wound copper coil containing hundreds of turns of magnet wire, and a movable steel plunger (armature) coupled directly to the shifting fork linkage. A precision-calibrated stainless steel compression spring holds the plunger in its de-energized rest position.
Understanding the electrical dynamics of this solenoid requires distinguishing between inrush (pull-in) current and holding current. When the control board fires the shift relay, the air gap between the stationary core and the movable plunger is at its maximum (typically 12 to 18 mm). Because of this large magnetic air gap, the solenoid’s inductive reactance is low, and the coil draws a massive instantaneous inrush current to generate the electromagnetic flux needed to overcome the return spring and drag of the shifter rail.
Once the plunger travels into the coil and seats flush against the internal pole face, the magnetic air gap collapses to near-zero. This increases the coil’s magnetic inductance by a factor of four to six, substantially increasing impedance and dropping the operating current to a low holding level. However, if hardened bakery grease or mechanical misalignment prevents the plunger from travelling its full mechanical stroke, the air gap remains open. The solenoid continues to draw heavy inrush current, causing the copper coil temperature to spike past 220°F within seconds. The high temperature melts the polyurethane wire insulation, producing an internal short circuit that permanently destroys the shift actuator coil.
Our field diagnostic procedure measures both static DC coil resistance (verifying 32–40Ω at bench ambient) and dynamic AC current draw during shifting. Technicians ensure the shift plunger travels its complete mechanical stroke without binding, eliminating the excessive thermal loading that causes premature actuator failure.
Bakery Flour Infiltration & NSF H1 Synthetic Tribology
Commercial bakeries and pizzeria kitchens are uniquely hostile operational environments for precision machinery. Airborne flour particles—composed primarily of wheat starch and gluten proteins with particle sizes ranging from 1 to 100 microns—remain suspended in the kitchen atmosphere for hours. As the mixer heats up during heavy dough cycles, internal air within the transmission housing expands and exhausts through breather ports; as the machine cools down overnight, it draws ambient kitchen air laden with flour dust deep into the mechanical housing.
When organic flour particulate contacts conventional mineral-based lubricants, starch granules absorb the base oil fluids through capillary action. Over several months, the lubricant experiences rapid phase separation, turning from a smooth lubricating fluid into a dry, abrasive cake. This paste coats the linear shifter rails, planetary bevel gears, and shift fork pins, increasing mechanical sliding resistance by over 400%. The electromechanical shift actuator, engineered to generate approximately 15 to 25 pounds of linear pull, becomes completely incapacitated by the paste-like friction.
To resolve this chronic commercial issue, our restoration protocols mandate complete solvent cleaning of all transmission components followed by repacking with authentic NSF H1 registered food-grade synthetic grease (Lubriko #702 or Chevron FM Grease). These advanced lubricants are formulated with synthetic polyalphaolefin (PAO) base oils and aluminum complex thickeners. They exhibit exceptional shear stability, resist water washdown emulsification, and maintain low viscosity even when exposed to ambient flour dust. Lubricating the shifter rail with genuine NSF H1 grease guarantees smooth, low-friction actuator movement for years of demanding commercial service.
3-Phase Voltage Harmonics in North Fulton Commercial Power
Commercial dining facilities along the Haynes Bridge Road, North Point, and Old Milton corridors draw heavy electrical power from commercial 208V/120V 3-phase wye or 240V delta electrical services. In modern commercial kitchens, high-density non-linear electrical loads—including variable-speed exhaust hood fans, high-efficiency combi-ovens, walk-in refrigeration compressors, and LED kitchen lighting—generate significant electrical noise and harmonic distortion across building distribution panels.
The Variable Frequency Drive in a Hobart Legacy mixer utilizes sensitive microprocessor clock circuits and low-voltage analogue sensing inputs that are vulnerable to line voltage distortion. High total harmonic distortion (THD exceeding 5%) and transient voltage spikes from nearby refrigeration contactors can induce false trigger pulses on the VFD’s control inputs. These electrical transients can scramble the memory registers of the digital SmartTimer board, causing random speed lockouts, phantom “E1” communication error codes, and corrupted speed shift timing routines.
During on-site diagnostics, our master commercial technicians test line voltage quality at the mixer disconnect. Using a Fluke True-RMS power quality analyzer, we evaluate phase-to-phase voltage balance (which must remain within 1.0%), check line-to-neutral voltages, and inspect incoming transient voltage surge suppressors (TVSS) and metal-oxide varistors (MOVs). Ensuring stable, clean electrical power protects the mixer’s VFD inverter and guarantees reliable electromechanical shifting during peak production hours.
Dough Rheology, Absorption Ratio & Torsional Shock Loading
The mechanical durability of a Hobart Legacy mixer transmission is intimately tied to the rheological properties of the dough being processed. Dough is a non-Newtonian, viscoelastic material whose viscosity changes dynamically under shear. In commercial baking, the primary metric governing dough stiffness is the Absorption Ratio (AR), calculated as the weight of water divided by the total weight of flour:
Absorption Ratio (AR) % = (Total Water Weight ÷ Total Flour Weight) × 100
High-hydration doughs (such as ciabatta or French baguettes with an AR of 65% to 75%) flow easily around the spiral dough hook, placing moderate torsional stress on the planetary transmission. However, low-hydration, stiff doughs (such as bagels, pie crusts, and thin-crust pizza with an AR of 45% to 55%) behave almost like semi-solid rubber. When a commercial mixer attempts to accelerate a 60-pound batch of 50% AR pizza dough from Speed 1 into Speed 2, the dough hook experiences severe cyclic torsional shock loads as it tears through the dense protein matrix.
These torsional shock waves travel up the planetary agitator shaft, through the bevel gears, and into the transmission shifter clutch. If a bakery operator routinely overloads the mixer beyond Hobart’s factory maximum batch rating chart, the intense torque pulses hammer the shift collar dog teeth and loosen the mechanical set screws securing the shift fork bracket. Over time, the fork develops mechanical play, causing partial dog engagement and accelerating micro-switch wear. Educating bakery culinary staff on proper batch sizing and progressive speed sequencing is an integral component of our comprehensive commercial repair service.
Commercial Food-Service Preventative Maintenance
Preventing costly transmission breakdowns and shift actuator failures in high-volume commercial bakery and restaurant operations requires a disciplined preventative maintenance schedule:
- Daily Bowl Guard Cleaning and Debris Inspection: At the close of each culinary shift, wash the wire cage bowl guard using warm, soapy water and a soft non-abrasive sponge. Thoroughly dry the magnetic interlock contact points to prevent flour dust crusting. Never blast high-pressure washdown hoses directly at the mixer head or top transmission cover.
- Monthly Shifter Rail and Linkage Inspection: Remove the rear transmission access port and inspect the internal shifting rail for hardened lubricant. If grease appears dark, chalky, or contaminated with flour, schedule professional solvent cleaning and re-greasing with factory-approved NSF H1 food-grade synthetic lubricant.
- Quarterly Planetary Seal and O-Ring Check: Inspect the lower planetary drip cup and planetary shaft seal for signs of gear oil leakage. If black or amber oil drops into the mixing bowl, the lower lip seal is failing, requiring immediate replacement before lubricant loss starves the planetary bevel gears.
- Semi-Annual Electrical Terminal and Ground Audit: Have a licensed commercial technician inspect the electrical terminal blocks, VFD wiring harness, and micro-switch spade connectors. Commercial mixer vibration can cause terminal screws to loosen, creating high-resistance hot spots that drop control voltage to the shift solenoid.
- Annual Oil Quality & Gear Backlash Analysis: For high-volume bakeries running 12 to 16 hours daily, schedule an annual transmission health audit. Master technicians check gear backlash, inspect shifting fork shoe wear, and measure motor winding insulation resistance with a 500V insulation resistance tester.
Rigorous preventative maintenance protocols similarly extend the operating lifespan of premium residential cooking products, such as those we maintain in our regional KitchenAid appliance repair division.
Commercial Food Equipment Safety & OSHA Compliance
Industrial food preparation machinery introduces serious mechanical and electrical hazards. Adhering strictly to federal OSHA, Georgia state, and manufacturer safety standards protects kitchen staff and service personnel:
- Mandatory OSHA Lock-Out / Tag-Out (LOTO): Before removing any inspection panel, opening the electrical enclosure, or servicing the transmission, always turn off the local wall-mounted safety disconnect switch, apply an OSHA-compliant safety padlock, and affix a signed warning tag. Never rely on the mixer’s STOP button or bowl guard interlock as an electrical disconnect.
- VFD DC Bus Discharge Hazard: The internal Variable Frequency Drive inverter board incorporates high-capacitance electrolytic capacitors that store high-voltage DC electricity long after line power is disconnected. Technicians must wait at least 5 minutes after de-energization and verify zero DC bus voltage with a calibrated multimeter before touching internal terminals.
- Mechanical Entanglement and Pinch Point Prevention: Never wear loose clothing, neckties, hanging jewelry, or unrestrained long hair when operating or testing commercial planetary mixers. Rotational torque generated by a 3 HP or 5 HP Hobart Legacy planetary drive is massive and can cause severe traumatic crush injuries in a fraction of a second.
- Never Bypass Safety Interlock Micro-Switches: Commercial kitchen line operators must never bypass, wedge, or defeat the wire cage bowl guard or bowl lift safety switches with cardboard, tape, or magnets. Bypassing interlocks is a severe OSHA violation and creates life-threatening hazards for kitchen personnel.
- Sanitation Washdown Protocols: The Hobart Legacy mixer is designed as a splash-proof machine (NEMA 4 / IP55 rated in specific sealed areas), not a submersible or pressure-washable unit. Never spray high-pressure power washers or steam cleaners directly into the motor cooling vents, SmartTimer keypad, or transmission seams.
Ensuring safety compliance across all culinary operations also encompasses water containment and sanitization systems, similar to the precision standards executed in our certified Bosch appliance repair technical procedures.
Frequently Asked Questions About Hobart Legacy Mixers
Below are detailed engineering and operational answers to the most frequently asked questions regarding Hobart Legacy planetary mixer speed selection, shift actuator operation, and transmission repairs:
Why won’t my Hobart Legacy mixer shift out of Speed 1 into Speed 2 or Speed 3?
The most common cause of a Hobart Legacy mixer failing to shift out of Speed 1 is a failed electromechanical shift actuator solenoid, hardened food-grade grease binding the sliding shifter rail, or an oxidized gear-position micro-switch. Under Hobart’s “Shift-on-the-Fly” protocol, the main controller signals the shift solenoid to move the shifting fork while the VFD inverter momentarily ramps down motor speed. If the solenoid coil has burned out (reading infinite resistance instead of 32–40Ω) or the micro-switch does not confirm gear engagement within 2.0 seconds, the mixer automatically cancels the shift and remains locked in Speed 1 to protect internal transmission gears.
What is the normal multimeter resistance reading for a Hobart Legacy shift solenoid coil?
When tested across its isolated wiring terminals at room temperature (70°F), an authentic Hobart Legacy shift actuator solenoid coil should measure between 32.0 Ω and 40.0 Ω on a calibrated True-RMS multimeter. A reading of 0 Ω or under 5 Ω indicates an internal short circuit that will trip control fuses, while a reading of “OL” or infinite resistance (∞ Ω) indicates an open, burned-out coil requiring complete OEM actuator replacement.
Can you shift gears on a Hobart Legacy mixer while the machine is running?
Yes! That is the defining engineering advantage of the Hobart Legacy series, known as “Shift-on-the-Fly” technology. Unlike older Hobart Classic mixers (such as the D300 or H600) which required the operator to stop the machine before shifting a manual mechanical lever, the Legacy series electronically coordinates transmission shifting. When you press a different speed button while running, the internal VFD automatically slows the motor to an exact sync speed, the shift actuator engages the new gear ratio, and the motor smoothly re-accelerates.
What role do the gear-position micro-switches play in the shifting process?
The micro-switches act as position feedback sensors for the central logic board. When the shift actuator moves the shifting fork to engage a gear ratio, a precision cam on the shifter rail depresses the corresponding micro-switch. This sends a low-resistance verification signal (< 0.2 Ω) back to the microprocessor, proving that the gear dogs are 100% engaged. Without this confirmed signal, the controller assumes the transmission is jammed and aborts the speed change.
Why does my mixer beep and stop completely when I press a higher speed?
When the mixer beeps and cuts motor power during a commanded speed change, the control board has encountered an internal “Shift Timeout Error”. This occurs when the control board energizes the shift solenoid, but does not receive an electrical closed-circuit confirmation from the position micro-switch within the factory timeout window (usually 1.5 to 2.5 seconds). The system shuts down motor power to prevent stripped gears and gear clash.
What type of grease is required inside a Hobart Legacy mixer transmission?
Hobart Legacy mixers require specialized NSF H1 registered food-grade synthetic grease, specifically Lubriko #702 or Chevron FM Grease. Never use automotive chassis grease, lithium grease, or standard industrial lubricants. Non-approved greases can emit toxic fumes, break down under high gear shear forces, gum up the shifting rail, and contaminate foodstuffs if lower planetary seals ever experience microscopic weeping.
How does the VFD (Variable Frequency Drive) interact with the mechanical transmission?
The VFD inverter module electronically modulates the AC electrical frequency (0 to 60 Hz) supplied to the induction drive motor. Rather than using purely mechanical gear reduction to achieve wide planetary speed variations, the Legacy mixer pairs a 2-speed or 4-speed mechanical gear cluster with VFD electronic motor scaling. This enables precision speed regulation across Stir (approx. 50 RPM), Speed 1 (100 RPM), Speed 2 (180 RPM), Speed 3 (320 RPM), and Speed 4 (up to 400+ RPM).
Can a misaligned bowl cradle prevent the mixer from changing speeds?
Yes. The bowl lift assembly features a safety interlock micro-switch that monitors whether the bowl is fully elevated into proper mixing position. If the bowl cradle is bent, loose, or not raised completely against the upper mechanical stops, the safety circuit breaks. On many Hobart Legacy models, an open bowl switch allows low-speed jogging or stir mode under specific software revisions but completely locks out higher gear shifting.
What are the signs that transmission gears are stripped rather than an electrical actuator failure?
Stripped transmission gears produce loud, metallic grinding, rhythmic rattling, or screeching sounds as the planetary agitator rotates. If you turn off power and rotate the planetary head by hand, a mixer with stripped helical gears will feel rough, catch on broken tooth fragments, or spin freely without resistance. Conversely, a failed shift actuator typically operates quietly, simply failing to engage the requested gear ratio.
How much does it cost to repair a Hobart Legacy shift actuator in Alpharetta, GA?
Professional on-site repair for a Hobart Legacy shift actuator in Alpharetta typically ranges from $450 to $980, depending on mixer frame size (HL200 vs. HL600 vs. HL1400) and whether the repair requires replacing the solenoid coil, installing a new micro-switch position assembly, or chemically cleaning and repacking the gummed shifter rail with food-grade grease.
How long does a Hobart Legacy shift actuator replacement take on-site?
A certified master commercial technician with an active truck inventory of OEM Hobart parts can typically complete diagnostic testing, transmission cover removal, actuator replacement, micro-switch calibration, and full-load dough run-in testing within 90 minutes to 2.5 hours.
Can I bypass the shift actuator to manually lock the mixer into Speed 2 for emergency production?
We strongly advise against attempting to mechanically lock or wedge the shifting fork into a specific gear. Because the Legacy mixer’s electronic control system continuously cross-references micro-switch feedback with the programmed VFD frequency curve, manually locking the gear collar will cause frequency mismatches, severe motor overheating, and permanent control board lockouts. Call our 45-minute priority dispatch instead.
What causes the shift solenoid coil to burn out in commercial bakery mixers?
The primary cause of solenoid coil burnout is mechanical binding on the shifting rail. The solenoid coil is engineered to pull the plunger in a quick 200-millisecond stroke. If hardened grease or flour dust prevents the plunger from seating fully into its electromagnetic core, the solenoid draws high inrush AC current continuously rather than dropping to low holding current. This rapid electrical over-saturation overheats the copper wire windings, melting the enamel insulation and shorting out the coil.
How does dough absorption ratio (AR) affect transmission and shifter lifespan?
The Absorption Ratio (water weight divided by flour weight) directly determines dough viscosity and mechanical drag on the planetary transmission. Low-hydration doughs (such as bagels or artisan pizza with an AR of 45% to 55%) place immense torsional stress on helical gear teeth and shift dog clutches. Overloading a mixer with low-AR dough in Speed 2 or 3 generates severe vibrational shockwaves that loosen shifter mounting fasteners and fatigue micro-switch brackets. Always follow Hobart’s maximum batch rating charts for specific dough hydration levels.
What warranty coverage is included with your commercial Hobart mixer repairs?
All commercial Hobart mixer transmission repairs, shift actuator replacements, and VFD diagnostic overhauls executed by our certified master technicians are backed by our comprehensive 90-day parts and labor commercial warranty. If the repaired subsystem experiences any operational defects within 90 days, our technicians return for priority zero-cost warranty resolution.
Do your technicians service all Hobart Legacy models from countertop to floor sizes?
Yes! Our commercial technicians are factory-trained on the complete Hobart Legacy planetary mixer lineup, including the countertop HL120 (12-qt) and HL200 (20-qt), mid-sized floor models HL300 (30-qt) and HL400 (40-qt), high-volume production HL600 (60-qt) and HL800 (80-qt), and industrial HL1400 (140-qt) planetary mixers.
What geographic areas in North Fulton County do your commercial technicians cover?
Our rapid commercial dispatch fleet serves commercial food businesses, wholesale bakeries, commissary kitchens, and restaurant corridors throughout Alpharetta, Milton, Roswell, and Johns Creek, maintaining rapid 45-to-90 minute emergency arrival times across the North Fulton region.
How do I schedule same-day emergency Hobart mixer service in Alpharetta?
To lock in a same-day commercial repair slot with our on-call master technicians, call our direct commercial service line at (770) 796-7742. Our commercial dispatcher will confirm your mixer model, reported symptoms, and dispatch a fully stocked service vehicle directly to your kitchen.
North Fulton Commercial & Residential Service Corridors
Alpharetta Commercial Hub
Haynes Bridge Rd, Old Milton Pkwy, Avalon Blvd, and Windward Pkwy bakeries & restaurants.
Milton Artisan District
Crabapple Market, Birmingham Crossroads, and culinary equestrian event kitchens.
Roswell Culinary Strip
Historic Canton Street, Alpharetta Highway, and Holcomb Bridge Road dining establishments.
Johns Creek Foodservice
Medlock Bridge Rd, State Bridge corridor, and country club hospitality kitchens.
Master Technician Executive Key Takeaways
For commercial restaurant general managers, executive pastry chefs, and bakery operations directors, these key points summarize critical knowledge regarding Hobart Legacy speed shifting and transmission reliability:
- Shift Solenoid Health is Binary: The electromechanical shift solenoid coil must read between 32.0Ω and 40.0Ω. An open circuit (∞Ω) prevents the actuator from shifting gears, locking the mixer in its base speed.
- Micro-Switches Form the Safety Loop: Even with a functional solenoid, an oxidized micro-switch with contact resistance above 2.0Ω will prevent the control board from receiving gear-engagement confirmation, triggering safety timeouts.
- VFD Electronics Require Balanced Power: The Variable Frequency Drive modulates motor output from 0 to 60 Hz. Power fluctuations or drying electrolytic capacitors can cripple the deceleration/acceleration ramp essential for Shift-on-the-Fly operation.
- Food-Grade Lubricant is Mandatory: Only NSF H1 registered food-grade synthetic grease (Lubriko #702) can be used. Non-approved automotive grease will seize the shifting rail and contaminate prep food bowls.
- Rapid Commercial ROI: Restoring an existing Hobart Legacy mixer with a new shift actuator ($450–$980) restores factory performance for a fraction of the $24,000 to $48,000 replacement cost of a new commercial floor unit.
- Same-Day North Fulton Coverage: Our factory-trained master technicians provide 45-to-90 minute emergency commercial dispatch backed by an ironclad 90-day parts and labor warranty.