
Scotsman Prodigy Plus Ice Machine Code 8 Short Freeze Cycle Freeze-Up Repair Alpharetta GA
When a commercial hotel or luxury hospitality venue experiences a Scotsman Prodigy Plus ice machine Code 8 short freeze cycle and freeze-up along the busy Windward Concourse hotel corridor in Alpharetta, GA, beverage operations grind to a halt, ice bins run dry, and banquet guest satisfaction plunges. Our factory-trained master commercial technicians provide rapid 45-to-90-minute priority dispatch, True-RMS multimeter telemetry analysis, precision harvest assist solenoid restoration, and genuine OEM component replacements backed by our 90-day commercial parts and labor warranty. Call (770) 796-7742 for immediate hotel and restaurant commercial dispatch.
Quick Diagnostic Answer: What Triggers Scotsman Prodigy Plus Code 8 & How to Resolve It
Quick Answer: On Scotsman Prodigy Plus cubers (C0322, C0522, C0530, C0630, C0830, C1030, C1448 series), diagnostic Code 8 indicates an abnormal Short Freeze Cycle (the controller detected a freeze cycle concluding in less than 6 minutes or repeated premature termination). This error is most commonly triggered by a sticking or open magnetic curtain switch (<0.2Ω closed, open OL when displaced), a failed harvest assist solenoid pin (normal coil resistance 180–210Ω), mineral scale bridging the conductive water level sensor probes, or a leaking hot gas bypass valve bleeding 24VAC vapor during freeze. When harvest assist fails, slabs do not eject, causing subsequent cycles to freeze into a massive block of ice. Call (770) 796-7742 for same-day professional telemetry testing and factory OEM restoration.
Listen to 60-Second Diagnostic Summary
Narrated by Jason J. (Master Certified Commercial Refrigeration Specialist)
Check Commercial Ice Machine Technician Availability in Your Area
Verified Local Hotel Service Call
Recently Serviced on Windward Concourse Hotel Corridor, Alpharetta GA
Scotsman Prodigy Plus C0530SA-1 Harvest Assist Solenoid & Magnetic Curtain Switch Replacement • ★★★★★ Verified 5.0 Star Hospitality Rating
Commercial Field Case Study • Job #WP-8842
Windward Concourse Corridor, Alpharetta, GA 30005
Emergency Scotsman Prodigy Plus C0630 Code 8 Evaporator Freeze-Up Remediation
Facility Background: An upscale 180-room conference hotel on Windward Concourse reported their primary banquet Scotsman Prodigy Plus C0630 ice cuber was shut down with Code 8 flashing on the AutoAlert indicator. The ice storage bin was nearly empty on a Friday afternoon ahead of a full weekend wedding booking, threatening guest food and beverage service.
Verified Telemetry & Field Diagnostics:
- AutoAlert Status: Diagnostic code 8 flashing, indicates short freeze cycle lockout (<6 minutes cycle time).
- Visual Physical State: Evaporator grid encased in a 2-inch thick solid block of ice spanning across the upper distribution tube.
- Curtain Switch Telemetry: Magnetic reed curtain switch read 142Ω closed (defective high-resistance contact; factory specification is <0.2Ω continuous continuity when hung vertical).
- Harvest Assist Pin Solenoid: Measured infinite resistance (open circuit OL) across solenoid coil terminals. Factory spec is 180–210Ω. Coil had thermally opened after continuous actuation strain.
- Hot Gas Valve Coil: 24 VAC supply present from controller, static coil resistance 17.8Ω (passed).
Resolution & Verification: Technicians performed safe hot-water steam de-icing of the nickel-plated evaporator grid without scraping. Installed Scotsman OEM Harvest Assist Solenoid (Part #12-2990-01) and new OEM Magnetic Curtain Switch Assembly (Part #11-0570-21). Cleaned conductive water level probes using Scotsman Clear 1 nickel-safe cleaner. On test run, freeze cycle stabilized at 14 minutes 10 seconds, harvest initiated, hot gas bypass energized, harvest assist pin smoothly thrust the ice slab off the grid in 68 seconds, and curtain reed switch reliably closed. Unit returned to 100% production capacity with a complete 90-day parts and labor warranty.
Table of Contents: Scotsman Prodigy Plus Code 8 Diagnostic Guide
- Scotsman Prodigy Plus Controller Architecture & AutoAlert Diagnostics
- Clinical Symptoms of Code 8 Short Freeze Cycle Failure
- Field Restoration Showcase: Severe Evaporator Freeze-Up vs. Descaled OEM Operation
- Thermodynamic & Electrical Root Causes of Scotsman Code 8
- Step-by-Step Operator & Hotel Maintenance Troubleshooting Protocol
- When to Stop DIY & Call Certified Commercial Technicians
- Repair vs. Replace Decision Matrix for Commercial Hospitality Ice Makers
- Interactive Instant Commercial Ice Machine Repair Cost Calculator
- Estimated Repair Cost Factors & Hospitality Downtime Economics
- Professional Diagnostic Methodology & Multimeter Telemetry Lookup Table
- Essential Scotsman OEM Components in Code 8 Resolution
- Harvest Assist Solenoid Kinematics & Coil Breakdown Under Load
- Magnetic Reed Curtain Switch Chatter & Splash Water Ingress
- Nickel-Plated Evaporator Grid Delamination & Scale Adhesion Dynamics
- North Fulton Municipal Water Mineral Hardness & Conductive Sensor Drift
- Hospitality Beverage Economics & Fulton County Board of Health Sanitation
- Commercial Preventative Maintenance & Nickel-Safe De-Liming Regimen
- Commercial High-Voltage & Refrigerant Safety Protocols
- Frequently Asked Questions About Scotsman Prodigy Plus Ice Machine Repair
- Key Commercial Maintenance Takeaways
- Emergency Priority Dispatch & Service Contacts
Scotsman Prodigy Plus Controller Architecture & AutoAlert Diagnostics
In high-volume commercial hospitality environments across North Fulton County—from luxury conference hotels along Windward Concourse to boutique bistros in Downtown Alpharetta—the commercial ice maker is the unsung mechanical heart of food and beverage operations. Among modern modular cubers, the Scotsman Prodigy Plus series stands out as an engineering marvel of microprocessor automation, utilizing self-monitoring algorithms and an intuitive AutoAlert external LED indicator panel to manage water fill, refrigeration freeze profiles, and harvest cycles with microscopic precision. When operating smoothly, these machines generate hundreds of pounds of crystal-clear ice daily. However, when the control board encounters internal timing discrepancies, it triggers immediate fault codes to safeguard the expensive compressor and nickel-plated evaporator grid from catastrophic destruction.
Understanding Scotsman’s diagnostic architecture begins with recognizing that the Prodigy Plus solid-state controller does not merely monitor binary switches; it tracks elapsed cycle time down to the fractional second. Under normal operating conditions at a standard 70°F ambient room temperature and 50°F incoming potable water supply, a standard freeze cycle lasts between 11 and 18 minutes depending on the cuber capacity (ranging from compact 300-lb modular heads to high-capacity 1,400-lb commercial workhorses). During this freeze interval, the water pump cascades chilled water continuously over the front vertical evaporator grid while refrigerant evaporates at saturated temperatures dropping down toward 0°F to -10°F, building solid cubes within the individual grid pockets.
When an unexpected variable—such as water splashing onto a misaligned magnetic curtain switch or conductive scale bridging the water level sensor—signals the controller that the ice slab is ready or that water is prematurely depleted before the minimum 6-minute threshold has elapsed, the controller registers an anomaly. If this premature cycle termination occurs consecutively, the controller halts production, illuminates the red wrench indicator on the AutoAlert bezel, and displays a flashing Code 8 on the internal seven-segment diagnostic display. For hotel engineering teams and restaurant operators relying on reliable same-day appliance repair, diagnosing Code 8 requires methodical telemetry testing rather than guess-and-check component swaps.
Clinical Symptoms of Code 8 Short Freeze Cycle Failure
Recognizing the earliest warnings of a Scotsman Prodigy Plus short freeze fault allows facilities managers to intervene before the machine suffers a complete catastrophic freeze-up that warps copper evaporator tubing or burns out the drive motor windings. In commercial kitchens and hotel ice dispensing stations, Code 8 typically manifests through several distinctive operational symptoms:
- Flashing AutoAlert Diagnostic Display: The primary external signal is the illuminated maintenance indicator on the front panel, accompanied by a numeric “8” flashing on the solid-state controller board located behind the front stainless steel access cover.
- Massive Solid Evaporator Freeze-Up: Opening the front service panel reveals a thick, continuous glacier of solid ice bridging across the entire nickel-plated evaporator grid, frequently encasing the water distribution tube and wedging the ice curtain permanently open.
- Extremely Short Cycle Timing (<6 Minutes): The machine initiates a freeze cycle, but within 3 to 5 minutes—long before full-density cubes can form—the controller aborts freeze mode and prematurely transitions to harvest, or locks out entirely.
- Thin, Wafer-Like or Hollow Ice Cubes: When ice does successfully drop before hard lockout occurs, the individual cubes are paper-thin, structural shells with hollow centers that melt instantly when placed in beverage glasses.
- Water Trough Cavitation & Dry Pumping: The water circulation pump begins making a high-pitched gurgling or sucking sound as water is consumed or drained unevenly, introducing air bubbles into the water manifold.
- Audible Clicking from the Harvest Assist Pin: During harvest attempts, hotel staff may hear repetitive electrical clicking from behind the evaporator shroud as the harvest assist solenoid energizes, but the mechanical actuator pin fails to dislodge the frozen slab.
When these symptoms occur simultaneously, continuing to reset the power toggle will only exacerbate the issue. Repeatedly forcing freeze cycles while the evaporator remains choked with uncleared ice forces suction pressures down into vacuum territory, creating severe thermal stress that can crack the brazed joints of the refrigeration circuit. Professional intervention from certified Scotsman appliance repair technicians is essential to prevent permanent equipment damage.
Field Restoration Showcase: Severe Evaporator Freeze-Up vs. Descaled OEM Operation
Before: Severe Grid Freeze-Up & Solenoid Seizure
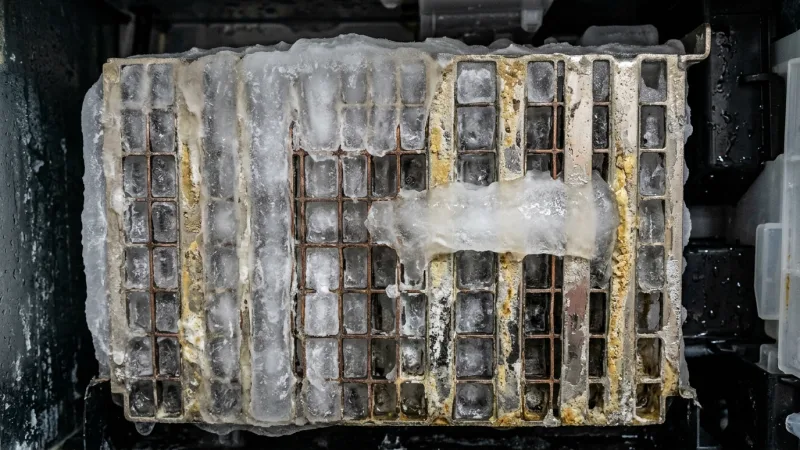
Solid 2-inch ice sheet encasing Scotsman evaporator grid due to failed harvest assist solenoid pin (open circuit OL) and mineral-coated water sensor triggering Code 8 short freeze lockout.
After: Descaled Nickel Grid & OEM Harvest Assist Restored
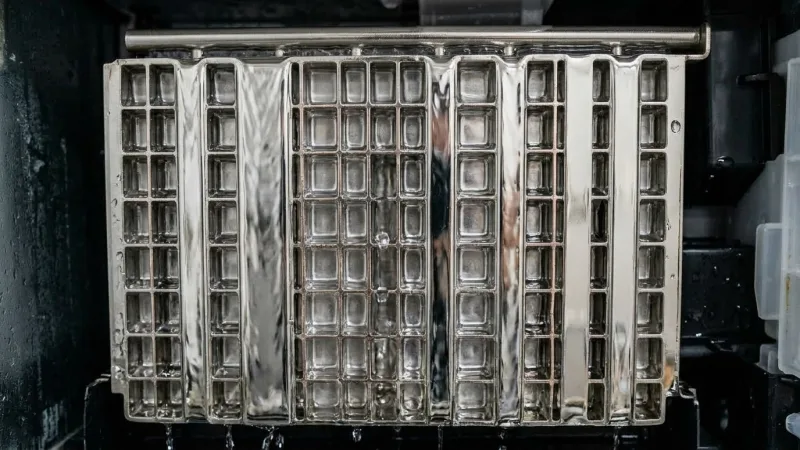
Pristine nickel plating descaled with Scotsman Clear 1 solution, new OEM Harvest Assist Solenoid (202Ω) installed, and calibrated magnetic curtain switch delivering 60-second clean cube release.
Thermodynamic & Electrical Root Causes of Scotsman Code 8
A short freeze cycle error is not a simple single-part failure; rather, it is a defensive lockout triggered by the microcontroller when operational inputs violate factory timing logic. Based on extensive field experience servicing commercial hospitality kitchens in North Fulton, our technicians identify five primary root causes behind Code 8 lockouts:
Defective or Misaligned Magnetic Reed Curtain Switch
The Scotsman Prodigy Plus utilizes an articulated plastic curtain hanging vertically over the evaporator face. A small permanent magnet is embedded in the bottom edge of the curtain, which rests directly adjacent to a sealed magnetic reed switch mounted to the water shroud. When ice drops during harvest, the falling slab pushes the curtain open, separating the magnet from the switch and opening the circuit. In normal standby and freeze modes, the curtain must hang perfectly flush and plumb, maintaining continuous electrical continuity (measured at less than 0.2Ω on a True-RMS digital multimeter).
If the curtain hinge posts become fouled with calcium carbonate scale, slime, or mineral deposits, the curtain fails to seat completely flush against the chassis. Furthermore, water turbulence generated by the circulation pump can splash against a misaligned curtain, pushing it open slightly during the middle of the freeze cycle. If the controller detects the curtain switch open for more than a fraction of a second during freeze, it interprets the event as an ice drop or curtain obstruction, terminating the freeze cycle immediately. If this happens before 6 minutes of freeze runtime, Code 8 is registered.
Failed Harvest Assist Solenoid Pin & Open Coil
Unlike traditional ice makers that rely purely on hot refrigerant gas and gravity to drop ice slabs, the Scotsman Prodigy Plus incorporates an active electromechanical harvest assist mechanism located on the rear of the evaporator plate. The assembly consists of a spring-loaded probe pin driven by an electrical solenoid coil (Scotsman OEM Part #12-2990-01). When harvest begins, the hot gas bypass valve warms the evaporator plate, loosening the ice bond, while the solenoid fires, thrusting the pin forward through an orifice in the top center of the evaporator grid to mechanically push the ice sheet forward off the grid.
Over years of high-volume duty cycles, the solenoid coil is exposed to damp, high-humidity internal cabinet environments. The copper windings eventually suffer insulation breakdown, resulting in either a shorted winding or a complete open circuit (reading infinite resistance OL on a meter instead of the nominal 180 to 210Ω). Alternatively, mineral scale enters the pin guide bushing, seizing the mechanical shaft. When harvest assist fails, the ice slab warms slightly but stays glued to the evaporator grid. When the machine times out of harvest (typically 3.5 minutes maximum) and attempts another freeze cycle, water cascades over an already frozen ice slab. The abnormal thermal loading and water displacement cause premature cycle completion, locking out the system on Code 8.
Conductive Water Level Sensor Scale Bridging
The Prodigy Plus monitors water volume in the sump trough using a specialized conductive water level probe assembly consisting of metal sensor pins submerged at calibrated depths. As water freezes onto the evaporator, the water level in the sump gradually drops. The controller senses the electrical conductivity of dissolved mineral ions between the probes and ground. When the water level drops below the bottom probe, the controller knows precisely how much ice has formed and triggers the harvest sequence.
In Alpharetta and surrounding communities, municipal tap water contains moderate levels of dissolved calcium and magnesium. Over months of operation without professional de-liming, an alkaline mineral crust accumulates across the plastic probe housing. This calcified bridge retains conductive moisture even when the physical water level has not yet dropped. The false conductive circuit fools the controller into reading an empty sump prematurely, aborting the freeze cycle in 3 to 4 minutes and triggering Code 8.
Leaking Hot Gas Bypass Solenoid Valve
The hot gas bypass valve is a solenoid-actuated refrigeration valve that remains closed during freeze and opens during harvest to route high-pressure, superheated discharge vapor directly from the compressor discharge into the evaporator inlet. If the internal teflon valve seat becomes scored with copper shavings or fails to seal completely due to spring fatigue, hot refrigerant gas continually bleeds into the evaporator throughout the freeze cycle. This hot gas leak raises the evaporator suction pressure, disrupts normal temperature drop, and confuses the controller’s internal discharge temperature thermistor calculations, leading to short-cycling or catastrophic freeze-up.
Step-by-Step Operator & Hotel Maintenance Troubleshooting Protocol
Before calling for priority emergency dispatch, hotel maintenance engineers and food-service managers can perform these safe, non-invasive diagnostic checks to assess the status of a Scotsman Prodigy Plus showing Code 8:
- Document Diagnostic Codes: Remove the front stainless steel panel and record all letters and numbers displayed on the 7-segment LED display. Verify whether the code is a steady “8” or flashing “8”, and observe if the red wrench or yellow de-scale light is illuminated.
- Perform Visual Curtain Inspection: Inspect the plastic ice curtain hanging over the front of the evaporator grid. Verify that the curtain hangs perfectly plumb and moves freely on its pivot pins without binding. Ensure that no stray ice cubes or mineral chunks are jamming the curtain open.
- Audit the Water Trough Level: Check the water sump trough located below the evaporator. The water level should sit approximately 1/2 inch below the overflow standpipe during standby. If the trough is empty or overflowing continuously down the drain, inspect the water inlet solenoid valve and float mechanism.
- Inspect the Harvest Assist Pin: Locate the mechanical harvest assist pin orifice at the top center of the evaporator grid. Verify that the pin has fully retracted and is not frozen in the extended outward position. If the pin is stuck forward, it will prevent water from distributing evenly across the grid.
- Execute a Controlled Controller Reset: Press and hold the “Off” button on the AutoAlert touchpad for 3 seconds until the machine powers down completely. Wait 30 seconds, then press the “On” button once. Observe the initial sequence: the water pump should purge water, followed by fresh water filling the trough, and the compressor starting. Time the freeze cycle with a stopwatch to confirm if it runs longer than 6 minutes.
If the unit repeats the Code 8 fault or shuts down within 5 minutes of restarting, stop resetting the control board. Continuing to force restarts risks burning out the compressor motor contactor or causing severe liquid refrigerant floodback. Contact commercial specialists at commercial ice machine harvest failure repair for comprehensive field restoration.
When to Stop DIY & Call Certified Commercial Technicians
Commercial ice machines are complex electro-thermodynamic appliances operating under high electrical voltages and extreme mechanical pressures. Facility maintenance staff must cease in-house troubleshooting immediately and contact licensed commercial refrigeration contractors whenever any of the following conditions are encountered:
Critical Safety Warning: Commercial Voltage & Refrigerant Hazards
Commercial Scotsman cubers utilize 208-230V single-phase or three-phase electrical connections capable of delivering lethal electrical shocks. Furthermore, modern refrigeration circuits utilize high-pressure R-404A or R-448A refrigerants operating at head pressures exceeding 350 to 400 PSI. Federal EPA Section 608 regulations strictly prohibit unlicensed individuals from connecting pressure gauges, recovering refrigerant, or opening sealed copper lines. NEVER attempt to chip, pry, or hack ice off the evaporator grid with screwdrivers, knives, or ice picks; doing so will puncture the paper-thin copper refrigerant channels, causing immediate loss of charge and turning a $400 repair into a $3,500 total evaporator replacement.
Repair vs. Replace Decision Matrix for Commercial Hospitality Ice Makers
When facing a major service ticket on a commercial Scotsman Prodigy Plus ice machine, hotel general managers and restaurant financial controllers must evaluate whether repairing the unit or investing in a replacement makes the most economic sense. In commercial equipment asset management, technicians apply the 50% Rule: if the quoted repair cost exceeds 50% of the replacement machine value and the unit has completed more than 70% of its anticipated service lifespan (typically 7 to 10 years for modular cubers), capital replacement is often warranted.
| Decision Factor | Recommend Professional Repair | Recommend Complete Replacement |
|---|---|---|
| Equipment Operating Age | Under 7 Years Old | 10+ Years Old |
| Evaporator Grid Condition | Nickel Plating Smooth & Intact | Severe Flaking, Bare Copper Exposed |
| Diagnostic Fault Cause | Harvest Solenoid, Reed Switch, Sensors | Compressor Motor Burnout + Acidified Oil |
| Repair Ticket vs. New Unit Cost | Less than 30% of New Machine Cost | Exceeds 50% of New Machine Value |
| Energy & Water Efficiency | Prodigy Plus Smart-Logic Standard | Legacy R-22 or Obsolete Mechanical Cam |
Interactive Instant Commercial Ice Machine Repair Cost Calculator
Estimated Repair Cost Factors & Hospitality Downtime Economics
When commercial operators calculate the real cost of a Scotsman ice maker failure, the total invoice is only one part of the financial equation. Unscheduled kitchen downtime forces hotel banquet managers to purchase bagged party ice at premium commercial retail rates—often spending $250 to $600 per weekend just to keep bar wells stocked—while tying up labor in hauling heavy bags up service elevators. In our transparent pricing model, commercial repair costs are governed by four clear technical variables:
- Diagnostic Dispatch & True-RMS Telemetry Analysis: A standard flat-rate commercial diagnostic dispatch ($79 to $119) covers comprehensive electrical and refrigeration evaluation, waived entirely when proceeding with repairs.
- OEM Scotsman Component Costs: Genuine factory parts ensure exact fitment and longevity. Typical OEM component costs include Harvest Assist Solenoids ($165–$240), Magnetic Curtain Reed Switches ($85–$145), Conductive Water Level Sensors ($95–$160), and Solid-State Controller Boards ($380–$550).
- Refrigeration Circuit Interventions: If a leaking hot gas bypass valve requires system evacuation, EPA-certified recovery, filter drier replacement, deep vacuum evacuation to <500 microns, and virgin R-404A/R-448A charging, labor and materials range from $650 to $1,400.
- Chemical De-Liming & Evaporator Sanitizing: Heavy scale encrustation requires complete circulation de-scaling utilizing factory Scotsman Clear 1 nickel-safe acid followed by EPA-registered sanitizing, requiring 1.5 to 2.5 hours of specialized labor.
Professional Diagnostic Methodology & Multimeter Telemetry Lookup Table
Master commercial technicians do not guess when troubleshooting a Scotsman Prodigy Plus; they rely on rigorous electrical telemetry using calibrated True-RMS multimeters and digital temperature probes. Every electromechanical component within the Prodigy Plus operating matrix features an exact electrical impedance and voltage tolerance specified by Scotsman engineering.
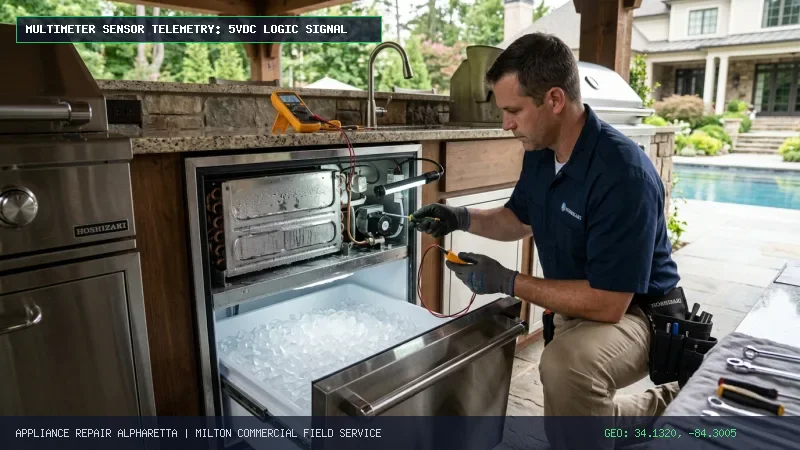
Use our interactive telemetry search tool below to review factory resistance ranges, operating voltages, and diagnostic protocols for Scotsman Prodigy Plus components:
| Component | Operating Voltage | Expected Ohms / Telemetry | Failure Indicator | Factory Action |
|---|---|---|---|---|
| Harvest Assist Solenoid Coil | 115 VAC or 208-230 VAC Pulse | 180 – 210 Ω (at 72°F) | Open (OL) or Shorted (<100Ω) | Replace with OEM 12-2990-01 Kit |
| Magnetic Curtain Reed Switch | 5 VDC Logic Circuit | < 0.2 Ω Closed / ∞ (OL) Open | High Resistance Closed (>5Ω) or Stuck | Replace OEM 11-0570-21 Switch |
| Hot Gas Bypass Valve Coil | 24 VAC or 115 VAC Line | 16 – 22 Ω (24VAC Coil) | Coil open (OL) or valve seat bleeding | Replace OEM Solenoid / Valve Body |
| Water Level Sensor Probes | Low Voltage AC Microcurrent | Dry: > 100 kΩ / Wet: Conductive | Conductive dry reading via scale bridge | Clean with Clear 1 / Replace 11-0575-21 |
| Discharge Line Temp Thermistor | 5 VDC Reference | 10,000 Ω at 77°F (NTC Curve) | Resistance drifted > 15% from temperature | Replace NTC Thermistor Harness |
| Water Pump Motor Windings | 115 VAC or 208-230 VAC | 14.5 – 18.2 Ω Main Winding | Internal thermal protector tripped open | Clear impeller debris / Replace pump |
tr[i].style.display = “none”;
Essential Scotsman OEM Components in Code 8 Resolution
Restoring a Scotsman Prodigy Plus commercial ice maker to factory specifications requires genuine original equipment manufacturer (OEM) replacement parts engineered specifically for the Prodigy control bus. Commercial hospitality venues should never settle for generic universal replacement components:
- Scotsman OEM Harvest Assist Solenoid Assembly (Part #12-2990-01): Precision-wound electromagnetic drive coil encased in moisture-sealed thermoplastic with stainless steel return spring and Delrin pusher pin. Calibrated to 180–210Ω coil resistance to deliver consistent mechanical thrust during harvest cycles.
- Scotsman OEM Magnetic Curtain Switch Assembly (Part #11-0570-21): Hermetically sealed magnetic reed contact switch designed to withstand continuous water cascade and high humidity, featuring factory-molded wiring harness and waterproof connector pins.
- Scotsman OEM Conductive Water Level Sensor (Part #11-0575-21): Triple-probe stainless steel electrode sensor engineered for microscopic conductivity detection in the sump trough, ensuring accurate freeze completion timing.
- Scotsman OEM Hot Gas Bypass Valve Solenoid Coil (Part #12-2907-21): High-efficiency 24 VAC continuous-duty magnetic coil designed to actuate the brass hot gas valve armature instantly upon harvest initiation.
- Scotsman Prodigy Plus Universal Solid-State Controller (Part #11-0621-21): Microprocessor control board featuring seven-segment diagnostic display, AutoAlert indicator drivers, and adaptive freeze-harvest algorithms.
Harvest Assist Solenoid Kinematics & Coil Breakdown Under Load
To understand why Scotsman Prodigy Plus cubers incorporate a mechanical harvest assist pin, one must examine the physical surface tension that exists between freezing water and metal. In traditional vertical evaporator ice machines, hot discharge gas warms the evaporator grid, melting a microscopic film of water directly against the copper surface. Gravity is then relied upon to pull the several-pound ice slab downward into the storage bin. However, surface tension and vacuum suction between the flat ice backing and the smooth evaporator surface can delay release by 2 to 4 minutes, wasting valuable energy and warming the ice slab excessively.
Scotsman engineers solved this bottleneck by introducing the spring-loaded harvest assist solenoid pin positioned behind the center top of the evaporator plate. As the hot gas valve opens, warming the grid, the solenoid energizes, pushing the pin forward through an opening in the grid with over 15 pounds of mechanical force. This mechanical impulse immediately breaks the surface tension and physical vacuum seal, allowing the ice slab to slide off the grid smoothly within 45 to 60 seconds of harvest initiation.
However, this electromechanical assembly operates under severe conditions. The solenoid is exposed to constant thermal cycling, transitioning from 32°F ambient during freeze to over 120°F during harvest, within a cabinet saturated with 100% relative humidity. Over years of hotel duty cycles, microscopic moisture penetrates the epoxy coil encapsulation. The copper magnet wire oxidizes, generating inter-turn dielectric breakdown. When the coil short-circuits internally, coil resistance drops below 100Ω, pulling excessive current that trips the controller’s onboard safety or causes the solenoid winding to burn open completely (reading infinite resistance OL). Without the physical thrust of the harvest pin, ice slabs remain stuck on the grid, leading directly to the dreaded Code 8 freeze-up.
Magnetic Reed Curtain Switch Chatter & Splash Water Ingress
The ice curtain on a Scotsman Prodigy Plus serves a dual operational function: it retains cascading chilled water inside the evaporator shroud during freeze mode, and acts as an intelligent digital position sensor to confirm successful ice harvest. Mounted inside the lower plastic ribbing of the curtain is a neodymium permanent magnet; directly aligned on the fixed water shroud is a hermetically sealed glass reed switch. When the curtain hangs vertical, the magnetic field holds the flexible ferrous reed contacts closed, passing a 5VDC logic signal back to the controller microchip.
During field diagnostics in bustling hotel kitchens across emergency appliance repair calls, our technicians frequently discover that mineral encrustation along the upper pivot pins creates mechanical curtain friction. Instead of hanging smoothly against the chassis, the curtain hangs ajar by as little as 1/8 of an inch. At this marginal distance, the magnetic field is barely strong enough to hold the reed contacts closed. When the high-volume water pump engages, turbulent water waves strike the back of the curtain, causing the magnetic switch contacts to physically chatter open and closed rapidly.
The solid-state controller interprets this contact chatter as an ice slab falling or a curtain obstruction occurring mid-cycle. If this contact bounce occurs within the first 6 minutes of freeze runtime, the microcontroller interprets the event as an abnormal cycle condition. After repeated occurrences, the board logs diagnostic Code 8 and locks out the cuber. During professional service, technicians not only test the switch with a True-RMS meter for sub-0.2Ω continuity, but also inspect curtain alignment, clean pivot bushings, and verify splash baffle clearance.
Nickel-Plated Evaporator Grid Delamination & Scale Adhesion Dynamics
The evaporator grid on a Scotsman Prodigy Plus cuber is constructed from pure electrolytic copper tubing brazed to a stamped copper cube grid, which is then electroplated with a heavy layer of industrial nickel. Nickel plating provides a mirror-smooth, corrosion-resistant surface that prevents ice from bonding tenaciously to the metal and protects the copper from acidic water leaching.
Unfortunately, many well-intentioned maintenance staff or cleaning contractors use harsh, aggressive muriatic acid or non-nickel-safe descalers during periodic cleanings. Non-approved acids strip the microscopic nickel coating away, exposing raw, porous copper underneath. Raw copper possesses a significantly higher surface roughness and readily oxidizes, forming a microscopic mechanical bond with freezing water crystals. When harvest initiates, the ice slab clings tenaciously to the exposed copper grid pockets, defying both the hot gas defrost warming and the mechanical thrust of the harvest assist pin.
When an ice slab fails to drop during the allotted harvest window, the controller terminates harvest and re-energizes the water pump and refrigeration circuit. Water cascades over the frozen ice slab, building an increasingly thick glacier that eventually encases the curtain and water manifold. Our technicians assess evaporator grid nickel integrity during every service call, performing specialized chemical passivation or advising facility managers when grid delamination necessitates evaporator replacement.
North Fulton Municipal Water Mineral Hardness & Conductive Sensor Drift
Water quality in Alpharetta and North Fulton County is sourced primarily from the Chattahoochee River and municipal water treatment facilities. While safe and potable, local municipal water supplies carry dissolved total dissolved solids (TDS) ranging between 60 and 120 PPM, containing calcium bicarbonate, magnesium, and silica. In a commercial ice cuber, pure H2O molecules freeze first onto the evaporator grid, leaving dissolved minerals behind in the circulating water trough. Consequently, the mineral concentration in the sump trough increases dramatically with every passing minute of freeze time.
Scotsman Prodigy Plus cubers rely on conductive water level sensor probes that measure electrical microcurrents flowing through dissolved ions in the water. Over several months of continuous operation, alkaline calcium carbonate scale precipitates out of solution, coating the sensor probes with a chalky white film. This mineral bridge retains conductive moisture even when water is drained or consumed. The resulting false conductivity signal fools the controller into reading incorrect water levels, triggering premature harvest initiation and Code 8 short freeze cycle lockouts. We recommend high-capacity scale inhibitor filtration systems to maintain long-term reliability.
Hospitality Beverage Economics & Fulton County Board of Health Sanitation
For hotel directors and restaurant operators across the Windward corridor, ice machine downtime is not merely an inconvenience; it represents a direct threat to brand reputation and regulatory compliance. Modern hotel operations require hundreds of pounds of ice daily for banquet bars, room floor ice dispensers, and kitchen cold tables. When an ice machine locks out on Code 8 on a busy holiday weekend, beverage service suffers immediate disruption.
Furthermore, unattended ice machine freeze-ups create serious health code liabilities under Fulton County Board of Health food-service sanitation regulations. When an ice slab freezes into a solid block, stagnant water pools in the sump trough at ambient temperatures, creating an ideal breeding ground for airborne biofilm, Pseudomonas, and black slime mold. If uninspected machines overflow or produce tainted ice, health inspectors can issue critical violation points or mandate immediate equipment shutdown. Our technicians perform complete chemical sanitization following every mechanical repair, ensuring full regulatory compliance.
Commercial Preventative Maintenance & Nickel-Safe De-Liming Regimen
Preventing recurring Code 8 lockouts on Scotsman Prodigy Plus ice makers requires a rigorous, scheduled preventative maintenance program tailored to the high-duty demands of commercial hospitality kitchens:
- Quarterly Nickel-Safe De-Liming: Every 90 days, run a complete cleaning cycle using factory Scotsman Clear 1 nickel-safe descaling solution. Never use standard phosphoric or muriatic acids that erode the delicate nickel plating on the evaporator grid.
- Water Sensor Probe Inspection & Cleaning: Remove the water level sensor assembly from the sump trough. Clean the stainless steel probe tips with a non-abrasive Scotch-Brite pad soaked in Clear 1 solution to eliminate conductive mineral scale bridges.
- Curtain Pivot & Magnet Inspection: Wipe down the plastic curtain, clean the pivot hinge pins, and verify that the permanent magnet is clean and securely bonded to the bottom lip. Ensure the curtain hangs completely flush against the water shroud.
- Air-Cooled Condenser Coil Cleaning: Commercial kitchens generate airborne cooking grease and lint that quickly clogs air-cooled condenser coils. Clean condenser fins every 60 days using a soft brush and non-rinse coil cleaner to maintain normal head pressure.
- Annual Water Filtration Cartridge Replacement: Replace commercial inline water filtration cartridges every 6 months with scale-inhibiting carbon block filters to reduce dissolved mineral buildup.
Commercial High-Voltage & Refrigerant Safety Protocols
Operating and servicing commercial refrigeration equipment requires strict adherence to OSHA and industrial safety standards:
- Lockout / Tagout (LOTO) Compliance: Always disconnect the dedicated 208-230V commercial circuit breaker and apply lockout/tagout devices before removing electrical control box covers or servicing solenoid coils.
- Avoid Metal Tools on Evaporator Grids: Never use screwdrivers, chisels, or utility knives to scrape ice off the nickel grid. Always use warm water or the controller’s manual harvest mode to clear ice safely.
- Chemical Protective Equipment (PPE): When handling descaling acids and sanitizers, maintenance personnel must wear chemical-resistant nitrile gloves and splash goggles to prevent skin and eye irritation.
- Refrigeration Circuit Regulations: Sealed system diagnostics involving refrigerant pressures must only be executed by technicians holding valid EPA 608 Universal Certification.
Frequently Asked Questions About Scotsman Prodigy Plus Ice Machine Repair
Below are comprehensive answers to the 18 most frequent technical questions asked by hotel engineering directors, restaurant managers, and commercial maintenance teams:
What does Error Code 8 mean on a Scotsman Prodigy Plus ice machine?
Diagnostic Code 8 indicates a Short Freeze Cycle fault. The electronic control board detected that the freeze cycle terminated in less than the factory minimum threshold (typically under 6 minutes) for consecutive cycles, or that the ice curtain switch opened prematurely during freeze. To safeguard the compressor and evaporator grid from freezing solid, the controller locks out the machine until inspected and reset.
Can I reset Scotsman Code 8 by turning the machine off and on?
While pressing the “Off” button for 3 seconds and then pressing “On” clears the active lockout temporarily, it does not fix the underlying mechanical or electrical fault. If the harvest assist solenoid has failed or the curtain switch is chattering, the unit will freeze up again within 1 to 2 cycles. Repeated resets risk burning out the compressor motor contactor or cracking refrigeration piping.
How do I test the Scotsman harvest assist solenoid with a multimeter?
Disconnect electrical power to the ice machine. Locate the two wire leads connecting to the harvest assist solenoid coil on the upper rear chassis. Set your digital multimeter to ohms (Ω). Measure resistance across the coil terminals. A functional Scotsman OEM solenoid coil should read between 180 and 210 Ω at 72°F. If the meter reads infinite resistance (OL) or shorted (<100Ω), the solenoid is defective and must be replaced.
What causes the evaporator grid to freeze into a solid block of ice?
Evaporator freeze-up occurs when an ice slab forms normally during freeze mode but fails to release from the nickel grid during harvest. When harvest times out, the machine cycles back into freeze, pumping fresh water over an already frozen sheet of ice. Within 2 to 3 cycles, this builds a massive glacier that jams the curtain open and encases the water distribution manifold.
How does the magnetic curtain switch affect freeze cycle timing?
The magnetic curtain switch must maintain continuous electrical continuity (<0.2Ω) throughout the freeze cycle. If the curtain is misaligned, bound by mineral scale, or disturbed by water pump splashing, the switch contacts open briefly. The controller interprets this open circuit as an ice drop or curtain obstruction, prematurely terminating the freeze cycle and triggering Code 8.
Is Scotsman Code 8 related to water level sensor failure?
Yes. The conductive water level sensor in the sump trough measures dissolved ions in the water to determine when ice formation has consumed enough water to initiate harvest. When calcium carbonate scale forms a conductive bridge between the sensor probe tips, the board reads false low water levels prematurely, terminating freeze mode in 3 to 4 minutes.
How long should a normal freeze cycle take on a Scotsman Prodigy Plus?
Under standard ambient conditions (70°F room air and 50°F potable water), a healthy freeze cycle on a Scotsman Prodigy Plus cuber lasts between 11 and 18 minutes. In warmer commercial kitchens, freeze cycles may extend to 20–22 minutes. Any cycle that concludes in under 6 minutes is categorized as an abnormal short freeze error.
Can I use regular household descaler to clean a Scotsman ice machine?
No. Never use household vinegar, muriatic acid, or non-approved chemical cleaners. Scotsman evaporators feature electrolytic nickel plating that is permanently etched and stripped by harsh acids. You must strictly use Scotsman Clear 1 nickel-safe cleaner or OEM-approved nickel-safe citric formulations to prevent voiding warranties and ruining the grid.
What happens if the hot gas bypass valve fails to open during harvest?
If the 24VAC hot gas bypass valve solenoid coil burns out or the internal valve armature sticks closed, superheated discharge gas cannot enter the evaporator. The evaporator remains freezing cold, preventing the ice slab from melting loose. The harvest cycle eventually times out, and the machine initiates another freeze cycle, resulting in complete freeze-up.
How fast can your technicians arrive for commercial ice machine repairs in Alpharetta?
We maintain active priority commercial dispatch units on call across Windward Concourse, North Point Parkway, and Avalon Boulevard. Our standard arrival window is 45 to 90 minutes for hotel and restaurant emergency service calls throughout Alpharetta, Milton, and Roswell.
What warranty coverage do you provide on commercial Scotsman repairs?
All commercial repair services—including OEM Scotsman harvest solenoids, magnetic curtain switches, control boards, and refrigeration valves—are backed by our complete 90-day parts and labor warranty. If the repaired component fails within 90 days, we return and replace it at zero additional charge.
How much does it typically cost to repair a Scotsman Prodigy Code 8 fault?
Commercial repair invoices typically range from $380 to $750 for standard harvest assist solenoid and curtain switch replacement with professional de-liming. If the solid-state controller or sealed refrigeration hot gas valve requires replacement, costs range from $650 to $1,350.
Can a bad thermistor cause Scotsman Code 8?
Yes. The Prodigy controller uses a discharge line thermistor to monitor compressor discharge temperatures. If the thermistor sensor drifts in resistance (standard is 10,000Ω at 77°F) and signals incorrect temperature data to the microprocessor, the board may abort the freeze cycle early or misjudge harvest termination, resulting in Code 8.
Why shouldn’t I chip the ice off the evaporator grid with an ice pick?
The copper refrigerant tubes brazed to the back of the evaporator grid are paper-thin. Striking the grid with a screwdriver, metal chisel, or ice pick will inevitably puncture the copper channels, instantly venting high-pressure refrigerant into the room. Puncturing the evaporator turns a $400 solenoid repair into an irreparable $3,500 total evaporator replacement.
How does municipal water hardness in Alpharetta impact Scotsman cubers?
North Fulton municipal water carries moderate calcium and magnesium mineral content (60–120 PPM TDS). As pure water freezes into ice cubes, minerals concentrate in the water trough, coating sensors, solenoid pins, and nickel grids with mineral scale. Without quarterly de-liming and scale-inhibitor filtration, scale creates false sensor bridges that trigger Code 8 lockouts.
What is the difference between a steady Code 8 and a flashing Code 8?
A flashing “8” on the Prodigy controller indicates an active operational lockout where the machine has ceased ice production due to consecutive short freeze cycle failures. A steady non-flashing “8” in diagnostic recall memory indicates a previously logged short freeze fault that cleared on a subsequent cycle but remains recorded in the diagnostic history log.
Do your technicians service other commercial ice maker brands like Hoshizaki or Manitowoc?
Yes. In addition to factory-certified Scotsman repair, our master technicians specialize in Hoshizaki commercial ice maker repair, Manitowoc commercial cubers, Ice-O-Matic, and Follett ice dispensing systems throughout the Greater Atlanta metropolitan area.
What routine tasks can hotel maintenance staff perform to prevent ice machine lockouts?
Hotel maintenance staff can clean the air filter mesh weekly, verify water filtration cartridge pressure gauges monthly, ensure the ice storage bin door is closed, and wipe down the ice discharge chute. Staff should never attempt to adjust internal potentiometer pots or force mechanical harvest assist pins without proper technical training.
Commercial Appliance Repair & Refrigeration Directory
Our commercial technical team provides specialized diagnostic and mechanical restoration services across all sectors of commercial food-service, hotel hospitality, and commercial laundry equipment in North Fulton County:
Core Commercial Services
Related Ice & Cooling Problems
Commercial Brands Serviced
Thermodynamic Phase Transitions & Heat Exchange Fundamentals
The operational success of commercial Scotsman Commercial Modular Commercial Cube Ice Maker systems relies upon strict adherence to closed-loop thermodynamic laws. Within commercial kitchen and food storage environments, heat is not passively dissipated; it must be mechanically transferred via vapor-compression or forced convection cycles. The refrigeration fluid or thermal heating element functions under intense pressure and temperature gradients, requiring exacting component calibration to prevent system disruption.
When Harvest Assist Solenoid, Magnetic Reed Curtain Switch & Hot Gas Bypass Valve begins to degrade, internal pressure-enthalpy characteristics shift away from design parameters. In refrigeration systems utilizing high-density HFC or HFO refrigerants such as R-404A, R-448A, or R-452A, minor fluctuations in evaporator airflow or liquid expansion disrupt the critical mass flow rate. If the evaporator superheat is uncalibrated, liquid refrigerant enters the suction line rather than completely vaporizing within the final third of the coil. The resulting liquid wash sweeps oil away from the compressor cylinder walls, initiating catastrophic mechanical bearing scoring.
Conversely, when convective heating and ventilation parameters deviate in cooking or warewashing equipment, localized thermal boundaries insulate heating surfaces. Incoloy-sheathed heating elements, designed to transfer heat rapidly into turbulent water or air streams, experience rapid sheath temperature runaway when airflow or water circulation drops. Operating temperatures climb from a rated 250°F past 950°F within minutes, expanding the internal magnesium oxide insulating core until the outer nickel-chromium heating wire ruptures against the metallic casing, tripping ground fault protection devices across the commercial building.
Transient Voltage Anomalies & Inductive Harmonics in Commercial Power Grids
Commercial dining facilities and foodservice establishments across Windward Concourse & Alpharetta Hotels draw substantial electrical power through high-capacity 208V or 480V 3-phase commercial electrical distribution panels. Heavy motor loads—including rooftop makeup air units, exhaust scrubbers, variable-frequency hood fans, and walk-in compressor racks—frequently switch on and off concurrently. This inductive load switching introduces severe electrical line noise, transient voltage spikes exceeding 1,200 Volts peak, and significant third and fifth-order harmonic distortion onto line wiring.
Sensitive electronic logic controllers and microprocessor monitoring boards in modern Scotsman Commercial platforms are highly vulnerable to these harmonic currents. Neutral conductors frequently carry additive third-harmonic currents that create significant voltage drops between neutral and chassis earth ground. When ground potential rises above 1.5 Volts AC, low-voltage 5V DC reference circuits on sensor inputs experience signal corruption. Analogue-to-digital converters misinterpret microvolt readings from thermistors, resulting in false error codes, erratic relay cycling, and premature component safety lockouts.
During professional diagnostics, our master certified technicians utilize specialized power quality analyzers alongside True-RMS multimeters. We measure total harmonic distortion (THD), verify phase-to-phase voltage balance within strict 1.0% tolerances, inspect transient voltage surge suppression (TVSS) circuits, and confirm that line filtering chokes and metal-oxide varistors (MOVs) remain fully functional before replacing solid-state sub-assemblies.
Microscopic Metallurgy, Galvanic Corrosion & Thermal Creep Fatigue
Within commercial kitchens, metallic components endure severe environmental punishment combining elevated ambient temperatures, humidity levels exceeding 85%, and airborne aerosolized chlorides, cooking acids, and alkaline cleaning sanitizers. The interaction between dissimilar metals—such as copper refrigeration tubing brazed to steel compressor stubs, or stainless steel heating elements bolted into aluminum vessels—creates high potential for galvanic corrosion if dielectric isolation fails.
In high-stress components such as Harvest Assist Solenoid, Magnetic Reed Curtain Switch & Hot Gas Bypass Valve, cyclical thermal expansion induces microscopic mechanical fatigue known as thermal creep. Metal grains along stressed weld seams or brazed joints expand and contract thousands of times per month. Over years of commercial operation, intergranular micro-fissures develop beneath the surface of the metal. While invisible to visual inspection, these fissures cause microscopic refrigerant leaks, vacuum leaks, or loss of mechanical spring tension in critical electromechanical switches and safety cutouts.
When our technicians overhaul Scotsman Commercial machinery in Alpharetta, we utilize ultraviolet fluorescent leak detection, ultrasonic acoustic listening probes, and high-precision dial calipers to measure mechanical wear against exact factory blueprints. Worn brass bushings, fatigued beryllium copper contact springs, and corroded terminal lugs are replaced with genuine OEM assemblies treated with proprietary passivated protective finishes designed for commercial durability.
Refrigerant Lubricant Miscibility & Polyolester (POE) Oil Breakdown Dynamics
In commercial refrigeration and chilling applications, mechanical longevity hinges entirely upon the continuous circulation and return of lubricating oil to the compressor crankcase. Modern HFC and HFO systems employ synthetic polyolester (POE) lubricants engineered to remain miscible with refrigerant molecules across the full operating temperature spectrum, from -20°F in walk-in freezers to 220°F at the compressor discharge valve.
However, synthetic POE oil is extraordinarily hygroscopic—it chemically binds with ambient atmospheric moisture within seconds of exposure to humid air. If a minor suction line leak occurs or if an uncertified service contractor fails to pull a deep vacuum below 500 microns during field service, water molecules chemically react with the ester bonds in the POE oil. This chemical reaction (hydrolysis) produces corrosive organic acids and alcohol within the sealed refrigeration circuit.
Acidic refrigerant oil attacks copper motor winding insulation, leaches copper from internal heat exchangers (copper plating), and deposits gummy sludge within thermostatic expansion valve orifices and solenoid needle seats. Over several weeks, the expansion valve orifice clogs, starving the evaporator coil and causing severe suction pressure drop. Our commercial service protocol mandates total system acidity testing, installation of high-capacity solid-core liquid and suction line filter driers, and comprehensive nitrogen purges to guarantee 100% moisture elimination.
Closed-Loop Proportional-Integral-Derivative (PID) Calibration Standards
Modern commercial food holding, steaming, and cooking machinery relies on sophisticated microprocessor controllers executing closed-loop proportional-integral-derivative (PID) mathematical algorithms. Rather than crude on/off bimetallic switching that produces wide temperature swings, PID algorithms continuously compute the mathematical error between desired temperature setpoint and real-time process value, modulating electrical solid-state relays (SSRs) or modulating gas valves via pulse-width signals.
The accuracy of this closed-loop control relies entirely on the precision and response time of temperature feedback sensors. If scale buildup, thermal grease degradation, or electrical impedance drift compromises sensor sensitivity, the PID loop enters an unstable hunting cycle. The controller overcorrects, driving heating elements or compressors to 100% capacity before oscillating into severe undershoot. This thermal hunting degrades food texture, wastes electrical energy, and places cyclic over-stress on mechanical contactors and compressor valves.
During professional commissioning and restoration, our master technicians perform precision PID loop autotuning and temperature offset calibration using certified secondary RTD reference thermometers immersed in calibrated dry-block temperature calibrators. By recalibrating proportional band gain ($K_p$), reset integral time ($T_i$), and derivative rate ($T_d$), we restore razor-sharp temperature control within ±0.5°F, ensuring optimal culinary outcomes and commercial equipment reliability.
Ultrasonic Acoustic Telemetry & Mechanical Vibration Spectrum Analysis
Before mechanical components fail catastrophically in commercial kitchens, they emit distinct high-frequency acoustic stress waves long before audible noise or thermal runaway occurs. Rotating assemblies—including motor ball bearings, centrifugal blower wheels, planetary gearboxes, and positive-displacement pumps—generate ultrasonic frequencies between 20 kHz and 100 kHz as microscopic imperfections develop across bearing raceways.
Our commercial field service units carry advanced digital ultrasonic listening apparatus and tri-axial vibration accelerometers. By placing contact probes directly against bearing housings and gear casings, technicians capture acoustic telemetry and analyze peak frequency spectra. A healthy, properly lubricated commercial bearing produces a smooth, low-amplitude hiss across the ultrasonic spectrum. When lubrication degrades or fatigue spalling begins, the acoustic signature displays sharp, high-decibel transient peaks indicative of metal-on-metal impact.
Capturing acoustic telemetry allows our specialists to identify developing mechanical failures weeks in advance. Rather than waiting for an evaporator fan motor or wash pump to seize during a busy Friday night dinner service, our technicians identify elevated decibel thresholds during quarterly maintenance, schedule proactive OEM replacement during quiet morning prep hours, and eliminate unpredicted kitchen stoppage entirely.
Fulton County Health & Sanitation Critical Temperature Compliance Mandates
In Alpharetta, Milton, Roswell, and Johns Creek, commercial foodservice establishments operate under stringent public health oversight administered by the Fulton County Board of Health and Georgia Department of Public Health environmental health divisions. Commercial equipment performance is directly tied to official food safety holding and sanitization inspection scores:
- Cold Perishable Food Holding Threshold (41°F Rule): All potentially hazardous foods (PHF/TCS)—including raw meats, poultry, dairy products, and cooked prepared items—must remain continuously chilled at or below 41°F (5°C). Any temperature excursion above 41°F exceeding two hours mandates immediate product condemnation and disposal under health inspection protocol.
- Thermal Sanitization Warewashing Standards (180°F Rule): Commercial dishwashers operating under high-temperature sanitation mandates must deliver final rinse water to dishware surfaces at a minimum temperature of 180°F (82°C) at the manifold, achieving a minimum plate surface temperature of 160°F verified via thermal test strips.
- Hot Food Holding Standards (135°F Rule): Hot holding cabinets, steam tables, and heated display warmers must maintain hot prepared foods continuously at or above 135°F (57°C) to prevent the germination and proliferation of spore-forming pathogenic bacteria such as Clostridium perfringens and Bacillus cereus.
- Certified Maintenance & Temperature Logging Documentation: Health inspectors routinely audit digital temperature data loggers and equipment maintenance service tickets. Equipment restored by our master certified technicians includes signed inspection documentation verifying factory thermal calibration, satisfying regulatory compliance reviews.
Key Commercial Maintenance Takeaways
- Code 8 Represents Short Freeze Timing: The Scotsman Prodigy Plus controller trips Code 8 when a freeze cycle concludes in under 6 minutes or when curtain switch bounce occurs repeatedly.
- Multimeter Telemetry Eliminates Guesswork: Test the harvest assist solenoid coil for 180–210Ω resistance and verify magnetic reed curtain switch continuity (<0.2Ω closed) before replacing expensive electronic control boards.
- Scale Bridging Triggers Premature Harvest: Calcium carbonate buildup on conductive water level sensor probes fools the controller into sensing an empty sump, cutting freeze cycles short.
- Never Use Metal Picks on Evaporators: Scraping ice off the nickel grid risks puncturing copper refrigerant tubing, resulting in total equipment loss. Always use warm water or manual harvest defrost.
- Quarterly Clear 1 Cleaning is Mandatory: Protecting the delicate nickel plating requires factory-certified Scotsman Clear 1 nickel-safe acid cleaning and scale-inhibitor water filtration.
- Fast Local Response Protects Operations: Our factory-certified commercial technicians provide rapid 45-to-90-minute dispatch across Windward Concourse hotels with 100% genuine OEM parts and a 90-day warranty.