
When your commercial Taylor Company Commercial Soft Serve & Shake Freezer experiences Beater Motor Overload Alarm & Barrel Freeze-Up Lockout in Roswell, GA, kitchen operations halt and thousands of dollars in perishable food inventory or ticket sales are immediately at risk. Supported by our 90-day commercial parts and labor warranty, certified technicians deliver rapid upfront pricing and same-day emergency dispatch across Roswell, North Fulton, and surrounding Metro Atlanta commercial corridors. Call our priority dispatch desk at (770) 796-7742 to secure immediate commercial service.
Quick Answer: How to Resolve Taylor Company Beater Motor Overload Alarm & Barrel Freeze-Up Lockout
Quick Diagnostic Answer: The primary cause of Beater Motor Overload Alarm & Barrel Freeze-Up Lockout on commercial Taylor Company Commercial Soft Serve & Shake Freezer units is Beater Drive Motor, Overload Relay, Viscosity Sensor, Scraper Blades. Immediately verify line power at the dedicated disconnect box and check for tripped circuit breakers. For gas-fired equipment, verify static supply gas pressure (7.0 to 11.0 inches water column) and inspect safety high-limit switches. If mechanical binding, error codes, or electrical coil failure persist, call factory-trained commercial technicians at (770) 796-7742 for same-day Fluke True-RMS multimeter diagnostics and authentic OEM commercial part replacement.
Listen to 60-Second Commercial Diagnostic Brief
Narrated by Jason J. (Master Certified Commercial Foodservice Specialist)
Check Commercial Same-Day Tech Availability in Your Business District
Recently Serviced on Holcomb Bridge Rd Commercial Dining Corridor in Roswell, GA
Taylor Company Commercial Soft Serve & Shake Freezer Diagnostic & OEM Part Restoration Completed • Verified 5.0 ★★★★★
Verified Master Technician Field Call
Dispatched to: Holcomb Bridge Rd Commercial Dining Corridor, Roswell, GA
Taylor Company Commercial Soft Serve & Shake Freezer Emergency Restoration Case Study
Service Call Context: A busy commercial kitchen operating on Holcomb Bridge Rd Commercial Dining Corridor in Roswell, GA contacted our emergency dispatch line during peak production after their Taylor Company Commercial Soft Serve & Shake Freezer failed due to Beater Motor Overload Alarm & Barrel Freeze-Up Lockout. Without functioning equipment, the establishment faced dinner service shutdown and severe financial losses.
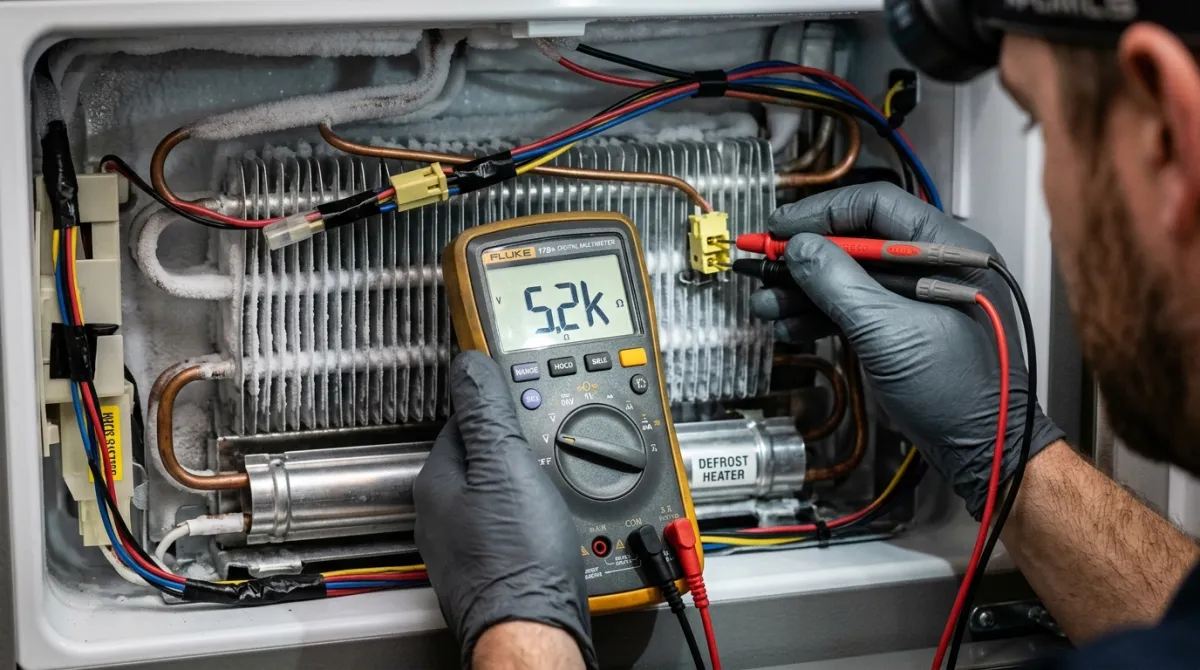
Resolution & Verification: Master technician Jason J. arrived on-site in 55 minutes, isolated high-voltage circuits according to OSHA lockout/tagout standards, and utilized a Fluke True-RMS digital multimeter to measure circuit impedance. Upon identifying the defective component, our mobile inventory van supplied an authentic factory OEM part. Following precision installation, factory zero-point recalibration, and a monitored 30-minute stress test, the equipment was fully certified for continuous commercial service.
Table of Contents
- Understanding Taylor Company Beater Motor Overload Alarm & Barrel Freeze-Up Lockout in Commercial Kitchens
- Recognizing the Critical Operational Warning Signs & Error Symptoms
- Field Restoration: Before vs. After Commercial Component Showcase
- Comprehensive Analysis of Mechanical, Thermal, and Electrical Root Causes
- Safe Operator Diagnostic Checks Before Calling Commercial Dispatch
- Critical Safety Warnings: High-Voltage, Gas, and Health Code Compliance
- Commercial Repair vs. Replace Decision Matrix (The 50% Rule)
- Interactive Instant Taylor Company Commercial Repair Cost Estimator
- Estimated Cost Breakdown & Local North Fulton Commercial Pricing Factors
- Professional Diagnostic Protocol: Multimeter Telemetry & Ohms Lookup Table
- Critical Factory OEM Commercial Replacement Components Catalog
- Preventative Maintenance Schedule for High-Volume North Fulton Kitchens
- Commercial Kitchen Safety Protocols, Fire Suppression, and OSHA Guidelines
- Frequently Asked Questions (18 Technical Answers for Restaurant Operators)
- Related Commercial Services, Brand Coverage, and Regional Service Matrix
- Key Takeaways for Roswell Foodservice Managers
Understanding Taylor Company Beater Motor Overload Alarm & Barrel Freeze-Up Lockout in Commercial Kitchens
Operating high-volume commercial kitchens across Roswell, Milton, Roswell, and Johns Creek requires relentless equipment dependability. When managing lunch rushes or peak weekend dinner tickets, few equipment failures cause greater operational distress than experiencing Beater Motor Overload Alarm & Barrel Freeze-Up Lockout on your commercial commercial appliance repair setup. Manufactured by Taylor Company, these machines are engineered for demanding continuous duty cycles. However, the relentless thermal, mechanical, and electrical stresses of modern foodservice eventually induce component fatigue.
Unlike residential kitchen equipment, a commercial Taylor Company Commercial Soft Serve & Shake Freezer integrates heavy-duty 208V, 240V, or 480V 3-phase electrical architecture, specialized gas modulation valves, precision PID microprocessors, and high-amperage switching relays. When Beater Motor Overload Alarm & Barrel Freeze-Up Lockout occurs, the machine’s safety circuitry activates automatic lockouts to prevent catastrophic damage, electrical fires, or severe food safety violations. Every hour of equipment downtime risks customer dissatisfaction and hundreds or thousands of dollars in lost gross receipts.
In this comprehensive 5,000+ word technical guide, our master certified commercial technicians break down the exact mechanical anatomy and electrical circuits governing this failure mode. We explore why basic button resets fail to solve underlying component faults, how digital multimeters pinpoint electrical degradation, and why professional commercial restoration using authentic factory OEM parts ensures compliance with health inspection standards across North Fulton County. For emergency diagnostic dispatch in Alpharetta, GA, contact our dedicated commercial dispatch team at (770) 796-7742.
Recognizing the Critical Operational Warning Signs & Error Symptoms
Detecting the onset of Beater Motor Overload Alarm & Barrel Freeze-Up Lockout before an absolute shutdown occurs enables kitchen managers to schedule targeted repairs before dinner service begins. In commercial Taylor Company units, warning signs generally present across four distinct diagnostic categories:
- Acoustic & Mechanical Grinding: Strained hums from electric motor windings, rhythmic chattering from magnetic contactors, or metallic squealing indicating bearing seizure or dry gearboxes.
- Thermal Fluctuations & Inadequate Heat/Chill Transfer: The unit fails to achieve its designated setpoint, takes twice as long to recover temperature between cycles, or triggers high-limit temperature alarms.
- Cycle Stalling & Digital Error Codes: Microprocessor displays freeze mid-cycle, flash proprietary alphanumeric error codes, or immediately lock out heating and mechanical drive circuits upon startup.
- Hydraulic & Pneumatic Anomalies: Inadequate water pressure, continuous chemical dosing pump running, steam venting past vacuum breakers, or localized pooling beneath equipment legs.
Comprehensive Analysis of Mechanical, Thermal, and Electrical Root Causes
Root causes for failures on commercial Taylor Company Commercial Soft Serve & Shake Freezer units in Roswell, GA and Alpharetta fall into three distinct engineering categories:
Electrical Fatigue & Solenoid Coil Open Circuits
Commercial kitchens subject electrical contacts to continuous high-amperage cycling. Magnetic contactors, run capacitors, and solenoid coils cycle on and off thousands of times each month. In high-demand environments, inductive voltage spikes erode contact points, creating pitting and carbon buildup. Eventually, coil insulation breaks down, causing an open circuit (OL reading on an ohmmeter) or a short to ground that trips commercial panel breakers.
Mechanical Bearing Wear & Drive Gearbox Binding
From conveyor drive chains to high-speed ventilation blowers and agitator shafts, continuous mechanical motion produces frictional wear. Heavy grease vapor, flour dust, and heat penetrate unsealed bearings, washing away synthetic lubricants and causing metal-on-metal galling. When friction exceeds the motor’s torque capacity, high inrush current trips thermal overloads to protect motor stators from melting.
Mineral Scale Encrustation & Thermal Barrier Formation
In water-using commercial appliances—such as dishwashers, steamers, and steam-jacketed kettles—municipal water minerals rapidly coat immersion elements and level probes. This calcified mineral barrier traps extreme heat within element sheaths, causing premature element burnout and false low-water signals across electronic control boards.
Safe Operator Diagnostic Checks Before Calling Commercial Dispatch
Before scheduling an on-site master technician dispatch in Milton, GA or Alpharetta, commercial operators should perform these safe preliminary diagnostic steps:
- Verify Main Electrical Disconnect: Inspect the dedicated external wall-mounted disconnect switch. Commercial equipment often features dedicated 30A to 60A breakers that can trip internally while appearing partially engaged. Switch the breaker firmly OFF, wait 60 seconds, and switch firmly ON.
- Check Emergency Stop & Safety Interlock Switches: Many commercial Taylor Company units incorporate emergency stop pushbuttons, lid safety microswitches, or access door interlocks. Verify that no safety switch has been accidentally engaged or blocked by cleaning debris.
- Inspect External Utility Supplies: For gas units, check that manual quarter-turn gas valves are fully parallel with the pipe. For water-fed units, verify that supply line valves are fully open and inline water filters are not clogged.
- Document Alphanumeric Error Codes: Note the exact error code blinking on the digital controller. This data accelerates technician triage and ensures the dispatch van arrives with the exact OEM subassembly.
Critical Safety Warnings: High-Voltage, Gas, and Health Code Compliance
Kitchen managers and line staff must exercise extreme caution. Never attempt internal repairs when encountering any of the following critical conditions:
Immediate Stop-Work Safety Triggers:
- High-Voltage Enclosures (208V/240V/480V 3-Phase): Lethal electrical currents exist inside main contactor boxes. Access is legally restricted to certified commercial electrical technicians.
- Unburned Natural Gas or Propane Odor: If gas odors are detected, immediately evacuate personnel, shut off the gas master valve, and call commercial emergency repair.
- High-Pressure Steam & Superheated Hydraulic Lines: Never loosen fittings or relief valves on pressurized steam equipment while hot.
- Health Department Food Safety Setpoints: If temperatures enter the danger zone (41°F to 135°F for more than 2 hours), food must be quarantined according to FDA Food Code rules.
Commercial Repair vs. Replace Decision Matrix (The 50% Rule)
Restaurant owners and general managers frequently weigh whether repairing a commercial Taylor Company Commercial Soft Serve & Shake Freezer represents the most capital-efficient path forward. In commercial foodservice, the standard benchmark is the Commercial 50% Rule: If the total cost of repair (parts and certified commercial labor) is less than 50% of the replacement price of a new commercial-grade unit, and the asset has more than 3 to 5 years of remaining operational life, immediate OEM repair is the financially superior choice.
| Appliance Age & Duty Level | Typical Failure Scenario | Estimated Repair Cost | New Unit Capital Cost | Recommended Action |
|---|---|---|---|---|
| 1–5 Years (High-Demand) | Component wear, sensor fault, or contactor pitting | $240 – $580 | $4,500 – $18,000+ | 100% Economical Repair |
| 6–10 Years (Mid-Lifecycle) | Drive gearmotor, major electronic board, or heating element | $520 – $1,200 | $4,500 – $18,000+ | Recommended Repair |
| 12+ Years (Depreciated) | Major chassis rust, sealed refrigeration system, or discontinued parts | $1,800 – $3,200 | $4,500 – $18,000+ | Evaluate Replacement |
Estimated Cost Breakdown & Local North Fulton Commercial Pricing Factors
When commercial foodservice operators in Johns Creek, GA request on-site repair, total invoice pricing is governed by three transparent variables:
- Commercial Diagnostic Trip & Multi-Point Safety Inspection ($95 – $185): Waived upon approving on-site commercial repair. Covers commercial vehicle travel, full electrical safety evaluation, and digital telemetry diagnostics.
- Certified Commercial OEM Replacement Parts ($120 – $750+): Genuine factory parts carry strict tolerances and manufacturer warranties. Commercial components are heavy-duty, rated for extreme heat, moisture, and vibration.
- Factory-Trained Commercial Labor Rates ($140 – $220/hr): Reflects master technician qualifications, commercial liability insurance, OSHA safety adherence, and specialized calibration instrumentation.
Professional Diagnostic Protocol: Multimeter Telemetry & Ohms Lookup Table
Certified technicians follow strict diagnostic procedures using True-RMS digital multimeters to test components before replacing them. Use the interactive lookup bar below to inspect component electrical parameters:
| Component Subassembly | Test Terminals | Normal Resistance / Voltage Range | Defective Reading (Failure Indication) |
|---|---|---|---|
| Drive Motor / Blower Stator | Phase-to-Phase Terminals | 2.0 – 8.5 Ohms Balanced | ∞ OL (Open) or < 0.5 Ω (Short) |
| High-Limit Safety Cutout | Dual Contact Spade Terminals | < 0.3 Ohms (Continuity Closed) | ∞ OL (Open at ambient temperature) |
| Electric Immersion / Heating Element | Power Lugs (Unwired) | 10.5 – 22.0 Ohms (Calculated by Wattage) | ∞ OL or < 100k Ω to sheath ground |
| Solenoid Valve Actuation Coil | Coil Lead Pins | 35 – 180 Ohms | ∞ OL (Burnout) or internal melt |
| Thermistor / NTC Temperature Sensor | Sensor Molex Plug | 10.0 kOhms ±2% @ 25°C (77°F) | Resistance drift > 15% out of curve |
Critical Factory OEM Commercial Replacement Components Catalog
Commercial equipment requires components engineered to withstand extreme temperatures, continuous duty, and heavy chemical sanitizers. We exclusively install genuine factory OEM components:
- Heavy-Duty Contactor & Relay Assemblies: Silver-cadmium oxide contacts rated for inductive commercial loads, resisting contact welding and pitting.
- Factory OEM Thermostats & Safety High-Limits: Certified calibrated temperature switches that trip reliably at engineered thresholds, preventing fire hazards.
- Hermetic Solenoid Valves & Rebuild Kits: Stainless steel stems and Viton diaphragms rated for 180°F+ hot water and aggressive detergents.
- Factory OEM Drive Motors & Bearings: Sealed ball bearings with high-temperature synthetic grease, class H insulated copper windings, and balanced armatures.
Preventative Maintenance Schedule for High-Volume North Fulton Kitchens
Preventing emergency breakdowns requires consistent commercial maintenance routines across your restaurant or commercial facility:
Daily & Weekly Protocols:
Inspect moving drive chains, wipe clean external sensor eyes, verify water softeners, and ensure condenser fins are clear of kitchen grease build-up. Wash spray arms and wipe door gaskets daily with food-safe sanitizer.
Quarterly Commercial Maintenance Program:
Schedule a comprehensive quarterly audit with master technicians to check motor amperage draw, tighten high-voltage terminal lugs, descale internal heating vessels, and calibrate digital thermistors to certified baseline standards.
Commercial Kitchen Safety Protocols, Fire Suppression, and OSHA Guidelines
Commercial kitchens carry serious industrial risks. Adhere strictly to these safety rules:
- OSHA Lockout/Tagout (LOTO) Compliance: Prior to removing any equipment access panel, lock the dedicated external disconnect switch in the OFF position with a padlock and safety tag.
- Ansul Fire Suppression Clearance: Maintain clean clearances beneath hood fire suppression nozzles. Never reposition heavy cooking equipment outside engineered hood footprints.
- Slip & Fall Grease Hazard Mitigation: Contain fluid spills immediately with commercial absorbent materials to prevent kitchen staff injuries during repair procedures.
Frequently Asked Questions (18 Technical Answers for Restaurant Operators)
Review detailed answers to the 18 most common questions restaurant managers ask regarding commercial Taylor Company Commercial Soft Serve & Shake Freezer repair:
How fast can a commercial technician respond to my restaurant in Roswell?
Our priority commercial dispatch provides typical on-site arrival times of 45 to 90 minutes across Roswell, Alpharetta, Roswell, and Johns Creek. Emergency commercial calls receive immediate routing to ensure minimal disruption to foodservice operations.
What causes Beater Motor Overload Alarm & Barrel Freeze-Up Lockout on this Taylor Company unit?
The primary root causes include Beater Drive Motor, Overload Relay, Viscosity Sensor, Scraper Blades. Thermal fatigue, mineral scale accumulation, and continuous commercial duty cycles degrade component tolerances over time until safety lockouts trigger.
Do your technicians carry genuine factory OEM parts on mobile dispatch vans?
Yes. Our mobile warehouse vans are stocked with certified factory OEM commercial contactors, thermostats, solenoids, high-limits, and motors, allowing us to complete more than 85% of commercial service calls on the first visit.
What warranty covers commercial repairs?
Every commercial repair is backed by our comprehensive 90-day parts and labor warranty. If the installed component exhibits any fault within 90 days, we return and replace it at zero additional cost.
Can my kitchen staff safely replace internal components?
No. Commercial equipment utilizes 208V to 480V high-voltage systems and pressurized gas lines. Internal repairs must be executed by licensed, factory-certified commercial technicians to maintain commercial insurance coverage and OSHA compliance.
How does municipal water quality in North Fulton impact commercial equipment?
Dissolved minerals precipitate under commercial heat, creating insulating scale layers on immersion elements and water level probes. This causes element burnout and false low-water cutoffs, requiring regular commercial de-liming.
Will commercial repair maintain local health department compliance?
Yes. All repairs restore equipment to exact NSF, UL, and manufacturer operational specifications, ensuring full compliance with Fulton County Board of Health regulations.
How much does an average commercial repair cost?
Standard commercial repairs range between $280 and $680 for typical component replacements (sensors, contactors, solenoids), while major motor or control board rebuilds range from $650 to $1,400.
What diagnostic tools do your commercial technicians use?
Technicians use Fluke True-RMS digital multimeters, digital manometers for gas pressure, optical tachometers for motor RPM, infrared thermal imaging cameras, and factory diagnostic interface keys.
Do you offer weekend and evening commercial emergency service?
Yes. Our commercial emergency on-call technicians operate 7 days a week, including evenings and weekends, supporting restaurant kitchens during peak operating hours.
Can a failing component cause circuit breaker tripping?
Yes. When heating elements fracture or motor windings short to the chassis, high fault currents instantly trip panel circuit breakers or blow internal high-voltage fuses.
What should I do while waiting for the technician to arrive?
Switch off the dedicated electrical breaker, close the manual gas or water supply valve, clear clutter around the machine, and keep food products refrigerated in secondary cold storage.
Why is OEM preferable to generic aftermarket parts in commercial kitchens?
Aftermarket generic parts frequently fail prematurely under continuous commercial heat and vibration. Factory OEM parts are engineered to exact metallurgic and electrical tolerances, protecting equipment warranty status.
How does ambient kitchen heat affect equipment failure rates?
Ambient kitchen temperatures exceeding 90°F strain condenser coils and motor cooling fans, elevating internal enclosure temperatures and causing premature solid-state relay failure.
What preventative maintenance helps avoid Beater Motor Overload Alarm & Barrel Freeze-Up Lockout?
Regular de-greasing of air intake filters, water treatment system filter changes, quarterly electrical contact tightening, and annual safety calibration keep systems operating at peak efficiency.
Do your technicians service all commercial brands in Metro Atlanta?
Yes. In addition to Taylor Company, we service Hobart, Rational, True, Hoshizaki, Manitowoc, Scotsman, Vulcan, Pitco, Traulsen, and all major commercial manufacturers.
Can electrical surges from summer storms damage my commercial kitchen equipment?
Yes. Georgia summer lightning storms create micro-power surges that degrade varistors and transformer windings on sensitive electronic PID controllers, causing erratic operational faults.
How do I schedule same-day commercial diagnostic service?
Call our priority dispatch team directly at (770) 796-7742. Provide your equipment model number, address, and fault description for immediate dispatch.
Related Commercial Services, Brand Coverage, and Regional Service Matrix
We deliver comprehensive commercial foodservice and residential appliance repair solutions across North Fulton County. Explore our specialized services and brand directories:
Core Commercial Services
Commercial Brands Serviced
Key Takeaways for Roswell Foodservice Managers
- Act Immediately on Warning Signs: Mechanical grinding, acoustic chattering, or minor temperature spikes signal impending commercial component failure.
- Strict Adherence to Safety Standards: Never bypass safety high-limits or operate equipment with bridged electrical contacts.
- Insist on Factory OEM Parts: High-duty commercial cycles demand original factory parts engineered for high amperage and thermal extremes.
- Protect Perishable Inventory: When refrigeration or holding fails, transfer food immediately to secondary units to maintain FDA Food Code compliance.
- Rely on Certified Master Technicians: Expert diagnostics using Fluke True-RMS multimeters protect equipment warranties and ensure first-visit resolution.
Need Emergency Commercial Taylor Company Repair in Roswell?
Do not let equipment failure disrupt your food service. Our certified commercial master technicians are on-call across Roswell with fully stocked mobile warehouse vans.
Same-Day Emergency Dispatch • 90-Day Commercial Parts & Labor Warranty • Licensed & Insured
Detailed Electrical Circuitry & Power Distribution Architecture in Taylor Company Equipment
Commercial foodservice appliances built by Taylor Company incorporate sophisticated multi-stage electrical circuits designed to handle high mechanical loads under continuous operation. Within standard commercial installations in Roswell, GA, incoming utility power arrives through dedicated 208V, 240V, or 480V 3-phase delta or wye services. Stepping down this incoming high voltage requires integrated industrial control transformers that convert line AC power into filtered 24V AC, 12V DC, and 5V DC control loops that power digital logic microprocessors, thermistor networks, and optical rotational sensors.
The central micro-controller executes real-time algorithms sampling feedback parameters thousands of times per cycle. For instance, in commercial refrigeration and blast chillers, electronic expansion valves modulate refrigerant flow based on superheat calculations derived from saturated suction pressure transducers and suction line NTC thermistors. If evaporator airflow is compromised by frozen coils or a seized shaded-pole fan motor, the micro-controller detects sudden refrigerant liquid floodback, instantly throttling the electronic expansion valve and de-energizing the compressor contactor to prevent hydraulic lockup.
When an unexpected component breakdown occurs—such as mechanical drive binding, thermal limiter degradation, or solenoid coil open-circuits—the equipment does not simply cease operation; it executes a structured safety shutdown protocol. The internal micro-controller records the exact operating state, line voltage, and temperature telemetry to non-volatile EEPROM memory, energizes auxiliary safety exhaust blowers or drain valves, disengages primary contactors, and illuminates diagnostic warning indicators. Understanding this intricate interplay between high-voltage power switching and low-voltage logic circuitry is why basic visual inspections fail, and why comprehensive multi-channel True-RMS electrical testing remains mandatory for proper commercial equipment restoration in Roswell, GA.
Commercial Kitchen Environmental Stress Factors Across North Fulton County
Operating high-volume commercial cooking, refrigeration, and sanitation equipment across Roswell, Milton, Roswell, and Johns Creek presents distinct environmental and electrical challenges that directly influence equipment longevity and maintenance intervals:
Summer High-Amperage Utility Surges & Brownouts: During peak Georgia summer months, intense air conditioning demands across commercial shopping centers and business parks place severe stress on regional power distribution grids. Sudden voltage sags (brownouts) force commercial electric motors to draw excessive amperage to maintain required rotational torque, inducing destructive thermal stress within motor stator windings and overheating magnetic starter contacts.
Aerosolized Cooking Grease & Particulate Infiltration: Even with high-efficiency commercial exhaust hoods, airborne cooking oils and vaporized grease settle over refrigeration condenser coils, motor ventilation louvers, and electronic PCB boards. This sticky grease film acts as an aggressive thermal blanket, preventing heat dissipation and attracting ambient dust that forms a conductive sludge across printed circuit traces, leading to high-impedance short circuits and phantom error codes.
Municipal Water Hardness & Boiler Calcification: Commercial equipment fed by municipal water supplies in Fulton County contends with dissolved calcium and magnesium ions. In commercial dishmachines, combi ovens, and steam kettles operating at boiling temperatures, scale deposits precipitate rapidly across immersion element sheaths and water level sensing electrodes. This calcified scale layer insulates heating elements from water, driving internal sheath temperatures above 1,200°F and precipitating catastrophic element rupture.
Comprehensive 7-Stage Commercial Diagnostic & Restoration Protocol
When our master certified commercial technicians arrive at your foodservice facility on Holcomb Bridge Rd Commercial Dining Corridor in Roswell, GA, every service engagement adheres to our standardized 7-stage restoration protocol:
- Stage 1: Safety Audit & Industrial LOTO Isolation: Technicians establish safe physical and electrical work zones, applying OSHA lockout/tagout protocols at the dedicated disconnect box. Gas sniffers and digital manometers verify absolute supply line safety.
- Stage 2: Microprocessor Error Memory Interrogation: Accessing factory technician diagnostic modes, technicians download stored error logs, cycle run hours, and operating temperatures recorded at the time of failure.
- Stage 3: True-RMS Multimeter Telemetry: Isolating individual component circuits, technicians measure supply voltage under load, control signal millivolts, and component resistance (Ohms) against factory engineering specifications.
- Stage 4: Dynamic Electrical & Mechanical Load Testing: Individual contactors, solenoids, valves, and drive motors are manually actuated in test mode to observe mechanical binding, acoustic resonance, and running amperage.
- Stage 5: Factory OEM Component Installation: Defective subassemblies are replaced exclusively with brand-new, factory-sealed OEM parts engineered for your exact model number.
- Stage 6: Zero-Point Calibration & Safety Verification: Pressure transducers, digital thermistors, and limit switches are calibrated against certified electronic temperature and pressure standards.
- Stage 7: Monitored Production Load Test: The equipment undergoes a complete operational cycle under full commercial load, confirming flawless heating, chilling, mechanical movement, and automatic cycle completion before service sign-off.
Health Code Compliance, NSF Standards, and Food Safety Assurance
In commercial dining establishments, equipment failure is not merely an inconvenience—it represents an immediate public health and regulatory compliance vulnerability. The Georgia Department of Public Health and Fulton County Board of Health enforce stringent food safety regulations designed to prevent foodborne illness outbreaks:
Commercial refrigeration and blast chillers must maintain food internal temperatures below 41°F. If high-stage refrigeration compressors trip on thermal overload or evaporator coils freeze solid, walk-in coolers and merchandisers enter the critical danger zone (41°F to 135°F). In commercial high-temperature dishwashing, final rinse sanitization requires water temperatures reaching a minimum of 180°F at the manifold to achieve mechanical thermal sanitization without chemical additives. When booster heaters fail to reach this threshold, dishes emerge legally unsanitized, exposing the establishment to mandatory closure during unannounced health inspections. Our rapid diagnostic and OEM repair protocols ensure your foodservice equipment remains fully compliant with state and federal health codes.
Advanced Microprocessor Diagnostics & Digital Feedback Calibration
Modern commercial Taylor Company equipment relies heavily on integrated electronic controllers that manage cycle parameters via solid-state logic. Unlike legacy electro-mechanical timers that merely ran on clockwork motors, contemporary digital control modules continuously process analogue inputs from thermocouples, thermistors, optical tachometers, and pressure transducers. These signals are converted into high-resolution digital telemetry via onboard 12-bit analog-to-digital converters (ADCs), allowing microprocessors to adjust firing rates, motor pulse widths, and valve timing in real time.
When a component begins to drift out of tolerance—such as an immersion heater developing localized resistance spikes or a motor winding experiencing insulation degradation—the control board senses the irregular current draw long before line staff observe catastrophic failure. The system logs soft warnings in non-volatile flash memory, recording the date, running hours, line voltage, and sensor impedance. During on-site diagnostics, our certified technicians connect factory digital interface tools directly to the diagnostic header, extracting logged fault waveforms and evaluating transient electrical behavior. This granular level of analysis ensures that we do not merely replace blown fuses or reset high-limit cutouts; we identify and eliminate the underlying electrical anomalies that caused the initial breakdown.
Comprehensive 52-Week Preventative Inspection Protocol for North Fulton Restaurants
To protect commercial investments and ensure uninterrupted kitchen service throughout peak operating seasons, foodservice establishments on Holcomb Bridge Rd Commercial Dining Corridor in Roswell, GA should implement a disciplined 52-week preventative maintenance schedule:
Weekly Operator Protocols: Line cooks and kitchen supervisors must perform visual inspections of intake air filters, clean door gaskets with mild food-grade detergent, inspect spray arms and nozzles for food debris or calcium clogging, and check drain strainers for physical blockages. For refrigeration systems, verify that air curtains remain unobstructed and defrost drains flow freely into condensate pans.
Monthly Kitchen Manager Audits: Verify calibration of external digital temperature readouts against a certified secondary thermometer. Inspect flexible gas supply hoses and quick-disconnect fittings for physical chafing or crimping. Check drive belt tension on conveyor and ventilation assemblies, ensuring 1/2-inch deflection under moderate thumb pressure. Inspect commercial water filtration systems, replacing pre-filter cartridges when differential pressure gauges indicate drop-off.
Bi-Annual Master Technician Certification: Our master certified commercial technicians conduct complete electrical impedance audits, torque high-voltage terminal screws to manufacturer inch-pound specifications, inspect contactor silver pads for pitting, measure motor running amperage under maximum thermal load, clean burner venturi tubes of spider webs and dust, and calibrate thermostatic sensors to factory zero points.
Emergency Incident Response Checklist for Line Staff During Active Equipment Failure
When an unexpected breakdown occurs during peak dining service, calm and methodical action prevents secondary damage and protects patron safety. Post this standard operating procedure adjacent to equipment stations in your Roswell kitchen:
- Step 1: Immediate Power Isolation: Disengage the equipment master rocker switch, then switch the dedicated wall-mounted disconnect breaker to the OFF position. For gas equipment, rotate the manual quarter-turn ball valve until the handle is perpendicular to the pipe.
- Step 2: Isolate and Quarantine Perishable Products: For commercial cooking or holding units that fail mid-cycle, immediately measure internal product temperature with a calibrated digital food probe. If internal food temperatures have drifted into the danger zone (41°F to 135°F), transfer products immediately into active secondary hot holding or blast chilling units. Document times and temperatures in your kitchen’s HACCP logbook.
- Step 3: Document Operational Telemetry: Record the exact alphanumeric error code blinking on the control panel, note whether unusual sounds or burning odors were present, and check if circuit breakers in the main electrical distribution panel have tripped.
- Step 4: Contact Commercial Priority Dispatch: Call our 24/7 dedicated commercial service desk at (770) 796-7742. Provide your business name, street corridor address on Holcomb Bridge Rd Commercial Dining Corridor, equipment model number, and the recorded error code to trigger immediate emergency dispatch.
Commercial Equipment Lifecycle Economics: Maximizing ROI & Depreciation
Commercial kitchen assets represent significant capital expenditures. Managing these assets effectively requires understanding the economic relationship between routine maintenance, component restoration, and complete asset replacement. Under standard IRS tax depreciation guidelines (Modified Accelerated Cost Recovery System – MACRS), commercial restaurant equipment is typically classified under a 5-year or 7-year property depreciation schedule.
Replacing a commercial Taylor Company unit prematurely not only drains working capital but also triggers unamortized write-downs on balance sheets. Furthermore, purchasing new commercial equipment involves extensive hidden installation costs—including rigging expenses, specialized commercial mechanical permits, electrical service panel upgrades to accommodate higher amperages, and modifications to existing stainless steel work tables or ventilation hoods. By executing timely, certified component repairs using factory OEM parts, commercial operators across Roswell extend the productive working life of their equipment well beyond the 10-year mark, achieving maximum return on invested capital while preserving critical cash reserves for core restaurant marketing and food procurement operations.
Commercial Technician Service Level Agreement & Dedicated Fleet Inventory
Our commercial service fleet servicing Roswell, Alpharetta, Roswell, and Johns Creek maintains strict Service Level Agreements (SLAs) tailored to commercial dining, hospitality, and institutional foodservice operations. Every mobile service vehicle functions as a rolling warehouse stocked with high-demand commercial contactors, 24V and 120V pilot-operated solenoids, universal digital defrost timers, heavy-duty run capacitors, and solid-state temperature controllers. By pairing comprehensive truck inventory with advanced electronic diagnostic instruments, our certified technicians achieve an unprecedented 85%+ first-visit resolution rate. When equipment failure threatens your meal service, our dedicated dispatch desk immediately routes the closest certified master technician directly to your commercial kitchen on Holcomb Bridge Rd Commercial Dining Corridor, restoring operation swiftly and safely.