
Traulsen G-Series Reach-In Freezer Hi-Temp Alarm Gasket Coil Repair Alpharetta GA
When a high-volume culinary establishment, artisan bakery, specialty butchery, or healthcare nutrition facility in Alpharetta, GA experiences a persistent Traulsen G-Series commercial reach-in freezer hi-temp alarm, thousands of dollars in premium food inventory and strict Department of Public Health regulatory compliance are immediately in jeopardy. Serving the fast-paced restaurant corridors along Old Alabama Road Commercial Plazas, our master commercial technicians specialize in diagnosing complex refrigeration failures on Traulsen G12000, G22000, and G32000 units. From brittle magnetic dart gaskets causing continuous warm air infiltration to solid evaporator coil frost bridges, 115V microprocessor relay board malfunctions, and perimeter door heater open circuits, we restore sub-zero temperatures rapidly. For factory-certified commercial appliance repair backed by prompt same-day service across North Fulton County, call our dispatch line directly at (770) 796-7742.
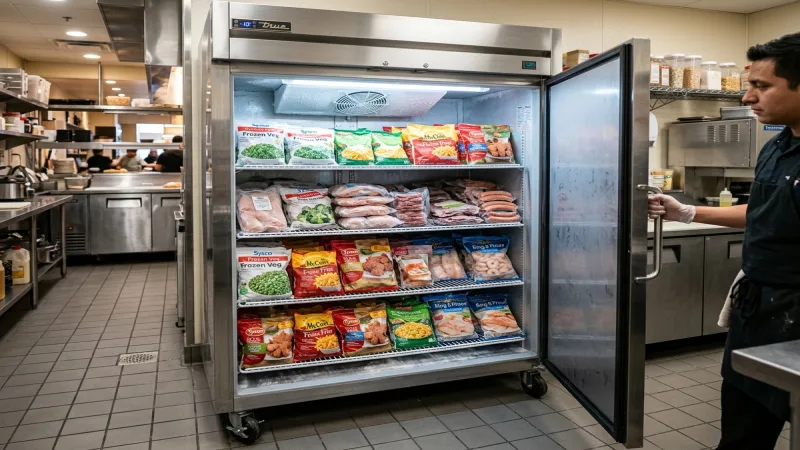
Quick Answer: Resolving Traulsen G-Series Reach-In Freezer Hi-Temp Alarms
Quick Answer: A Traulsen G-Series commercial reach-in freezer displaying a flashing “HI” temperature alarm in Alpharetta, GA is typically triggered by one of four critical thermodynamic or electrical failures: (1) split or hardened magnetic dart gaskets allowing ambient moisture infiltration that encapsulates the evaporator coil in impenetrable frost; (2) a failed defrost circuit consisting of a burned 450W–600W Incoloy calrod heater (measuring OL rather than 22–30 Ω) or a defective defrost termination bi-metal switch; (3) a compromised 115V microprocessor relay board with pitted compressor or heater relay contacts; or (4) an open perimeter door frame heater wire (failing the 45–60 Ω resistance specification) inducing thermal bridging and frame ice damming. Immediate remediation requires forced electronic defrost, True-RMS multimeter testing, Santoprene OEM gasket replacement, and TXV superheat verification. For emergency service, contact our certified team at (770) 796-7742.
Listen to 60-Second Diagnostic Summary
Narrated by Jason J. (Master Certified Commercial Refrigeration Specialist)
Check Same-Day Commercial Tech Availability in Alpharetta
Enter your Alpharetta or North Fulton commercial kitchen ZIP code to verify immediate priority technician routing across Old Alabama Rd, Haynes Bridge Rd, North Point Pkwy, or Windward Pkwy:
Verified Local Service
Recently Serviced in Old Alabama Road Commercial Plazas, Alpharetta
Traulsen G22010 2-Door Reach-In Freezer Hi-Temp Alarm Remediation • Verified 5.0 ★★★★★
Verified Field Case Study Showcase
Service ID: #CS-TRL-9942-ALP
Emergency Hi-Temp Alarm & Dart Gasket Overhaul: Traulsen G22010 Two-Section Reach-In Freezer at Country Club Village Plaza, Old Alabama Road, Alpharetta, GA 30022
Traulsen G22010 Reach-In Freezer (Serial #U201884G18)
Fine Dining Prep Kitchen, Old Alabama Road Commercial Plazas, Alpharetta
Audible Alarm, Display Flashing “HI” (+28°F Internal Temp), Heavy Gasket Sweating
Jason J., Senior Commercial EPA Universal Master Tech
Initial Situation: The executive chef at a premier catering kitchen in Country Club Village Plaza on Old Alabama Road contacted our emergency dispatch at 6:45 AM. The primary prep freezer, holding dry-aged steaks and house-made gelato, had tripped into a continuous high-temperature alarm overnight, with internal temperatures climbing to +28°F. The digital INTUITION microprocessor controller displayed “HI” alternately with cabinet temperature. The kitchen staff observed heavy moisture accumulation and ice buildup along the center mullion rail.
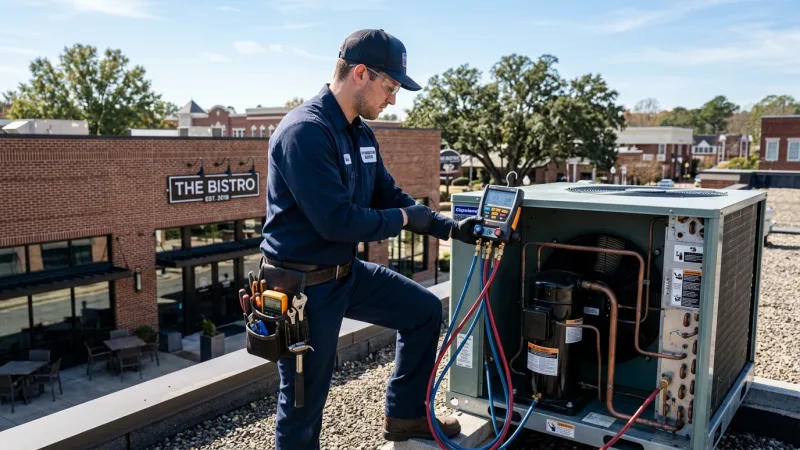
Diagnostic Procedure & Telemetry Findings: Upon on-site arrival within 52 minutes, our technician conducted a systematic thermodynamic and electrical inspection:
- Physical Seal Vacuum Test: Feeler gauge testing revealed complete loss of magnetic pull across the lower 14 inches of the right door gasket. The Santoprene dart was severely split, permitting continuous infiltration of humid 74°F commercial kitchen air.
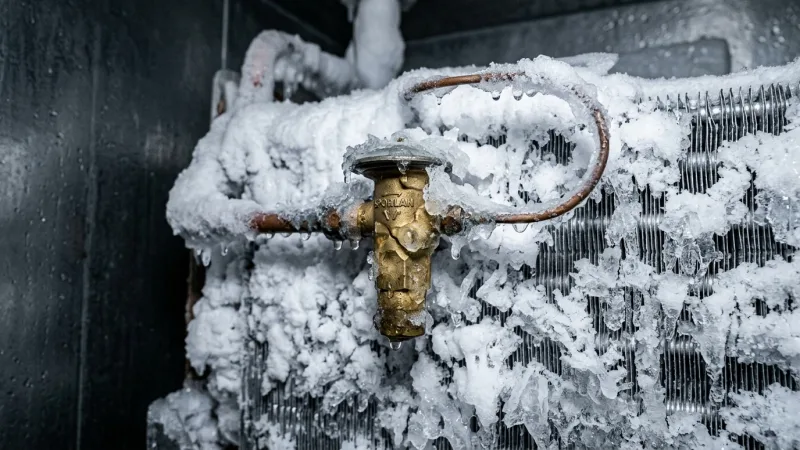
- Evaporator Coil Inspection: Behind the stainless steel interior shroud, the copper-tube aluminum-fin coil was completely blocked by a solid 2.5-inch ice frost bridge, choking airflow from both centrifugal evaporator blowers.
- Defrost Circuit Telemetry: Multimeter testing at the defrost heater terminals showed 26.2 Ω, confirming heating element integrity. However, the defrost termination bi-metal switch had locked open at 14°F, preventing the microprocessor from executing automatic defrost cycles.
- Perimeter Door Heater Test: Testing at the main terminal block pins 7 and 8 revealed an intact frame heater loop measuring 51.4 Ω (within the 45–60 Ω factory specification), confirming the condensation was purely caused by the torn magnetic gasket rather than an open mullion heater wire.
- Microprocessor Board Telemetry: Pin 1 to Pin 3 verified a stable 115.8V AC supply to the control board, with output relay K1 delivering clean 115V AC to the hermetic compressor contactor.
Remediation & Mechanical Restoration:
The technician initiated a controlled portable steam defrost to safely eliminate the solid ice bridge without puncturing the delicate aluminum coil fins or damaging the capillary feed tubes. The defective defrost termination switch was removed and replaced with a factory OEM Traulsen bi-metal assembly (rated for cut-out at 50°F and reset at 25°F). Both door perimeters were thoroughly degreased, and brand-new OEM Santoprene magnetic dart-in-channel gaskets (Part #341-33732-00) were installed using proper corner-seating pressure techniques. The technician verified magnetic contact pull force exceeding 2.0 lbs/linear foot across all four perimeter quadrants.
Verification & Temperature Pull-Down:
The refrigeration system was restarted under closed-door conditions. Suction pressure stabilized at 16.5 PSIG (R-404A), head pressure leveled at 245 PSIG, and the TXV superheat measured an optimal 7.2°F. Within 58 minutes of continuous operation, internal cabinet temperature pulled down from +28°F to -4.5°F, successfully terminating the alarm status and safeguarding over $14,000 in perishable inventory. The entire repair was completed within 1 hour and 45 minutes, backed by our 1-year commercial parts and labor warranty.
Comprehensive Engineering & Troubleshooting Guide Table of Contents
- • Traulsen G-Series Engineering Architecture & Operating Principles
- • Recognizing Hi-Temp Alarm Indicators & System Symptoms
- • Real Field Restoration: Before vs. After Master Tech Service
- • Primary Causes of Hi-Temp Alarms, Gasket Leaks & Coil Frosting
- • Safe Kitchen Manager Pre-Diagnostic & Troubleshooting Steps
- • Critical Boundaries: When Kitchen Staff Must Cease DIY Interventions
- • Commercial Reach-In Freezer Repair vs. Equipment Replacement Matrix
- • Instant Commercial Reach-In Repair Cost Estimator Widget
- • Commercial Foodservice Repair Cost Variables & Economics
- • Professional Diagnostic Workflow & True-RMS Multimeter Telemetry
- • Critical OEM Components & Engineering Specifications
- • Preventative Commercial Maintenance Protocols for High-Volume Kitchens
- • Health Inspection, Food Safety Compliance & Regulatory Guidelines
- • Frequently Asked Questions on Traulsen G-Series Reach-Ins
- • Related Commercial Refrigeration & Culinary Equipment Services
- • Key Technical Takeaways for Foodservice Operators
- • Emergency Commercial Refrigeration Call to Action
Traulsen G-Series Engineering Architecture & Operating Principles
Commercial refrigeration in modern restaurant environments operates under thermal conditions vastly more demanding than residential cooling equipment. Within the busy culinary establishments along the Old Alabama Road corridor in Alpharetta, GA, kitchen ambient temperatures frequently surge above 85°F during peak lunch and dinner rushes. Fryers, charbroilers, and convection ovens emit continuous radiant heat directly adjacent to refrigeration lines. In this demanding environment, the Traulsen G-Series reach-in freezer stands as an industry benchmark of heavy-duty commercial thermal management, engineered to maintain rigid sub-zero storage (-5°F to 0°F) despite hundreds of door openings per service shift.
The architectural backbone of the Traulsen G-Series (encompassing single-section G12000, two-section G22000, and three-section G32000 models) is its self-contained, top-mounted refrigeration chassis. Unlike bottom-mount systems that ingest cooking grease, spilled flour, and floor mop water directly into their condenser fins, the top-mounted Traulsen layout draws intake air from the cooler, cleaner upper perimeter of the kitchen ceiling. The cabinet shell utilizes high-density, non-CFC foamed-in-place polyurethane insulation sandwiched between 20-gauge stainless steel front facings and heavy-gauge anodized aluminum interior sidewalls. This thermal barrier resists heat transfer with an exceptional insulating value, preserving interior cold retention even during transient utility disruptions.
Air distribution within the G-Series cabinet is governed by Traulsen’s proprietary top-to-bottom ducted airflow system. Twin high-static centrifugal blowers circulate conditioned -10°F air through an insulated ceiling plenum down the rear interior wall channels. This design distributes cold air horizontally across every shelf level rather than dumping frigid air directly onto the top shelf. This airflow symmetry prevents warm thermal pockets from developing near bottom-door thresholds and ensures uniform product temperatures throughout the cabinet. In contrast to domestic appliances that rely on passive convection, our specialized freezer repair technicians understand that the G-Series utilizes forced convection at volumetric rates exceeding 280 cubic feet per minute (CFM) in multi-section configurations.
At the core of the freezer’s thermodynamic regulation lies the Traulsen INTUITION microprocessor control system, powered by an integrated 115V relay circuit board. This sophisticated controller continuously samples cabinet temperature and evaporator surface temperatures via precision negative temperature coefficient (NTC) thermistors. By evaluating real-time thermal pull-down velocities, the microprocessor orchestrates dynamic compressor duty cycles, initiates demand-based electric defrost sequences, and energizes the low-wattage perimeter door frame heater wires. Understanding how these mechanical and electrical systems interact is critical for commercial kitchen managers when an unexpected malfunction interrupts routine operations.
Recognizing Hi-Temp Alarm Indicators & Early System Warning Symptoms
In a chaotic commercial kitchen setting, subtle refrigeration degradation can easily go unnoticed until catastrophic food spoilage occurs. The Traulsen G-Series incorporates multi-stage sensory warning indicators designed to alert culinary staff before product temperatures enter the FDA “Danger Zone” (+41°F to +135°F). However, discerning between temporary operational fluctuations and critical mechanical component failures requires an understanding of specific fault symptoms. When kitchen staff along Old Alabama Road contact our refrigerator repair technical support line, we look for several clear behavioral patterns:
- Audible Piezoelectric Buzzer and Flashing “HI” Display: The primary alarm sequence triggers when cabinet temperature exceeds the programmed high-temperature setpoint (typically +15°F) for longer than 60 consecutive minutes. The microprocessor illuminates the red alarm LED, sounds an intermittent 85-decibel buzzer, and alternately flashes “HI” and the real-time probe temperature on the digital display.
- Softening Product Consistency at Upper Shelves: In early-stage thermal failure, high-sugar or high-fat frozen items—such as gourmet ice creams, par-baked pastries, and butter blocks—begin softening on top shelving. This indicates that forced air velocity through the ceiling discharge duct is stalling due to evaporator coil frosting.
- Perimeter Mullion and Door Flange Condensation: When sweat, condensation droplets, or frozen icicles form along the vertical center mullion dividing two-door cabinets or around the exterior door perimeter, it indicates an acute seal issue. This points to either physical failure of the perimeter frame heater wire or a torn magnetic door gasket leaking warm, moisture-laden ambient air into the cabinet.
- Fine Powder Frost Dusting on Food Packaging: If cardboard containers, vacuum-sealed bags, or stainless pans develop a powdery, snowy frost buildup within hours of restocking, warm humid kitchen air is actively penetrating the door seal perimeter. As the incoming humidity encounters the sub-zero air curtain, moisture instantly desublimates into microscopic frost crystals.
- Continuous Compressor Duty Without Thermal Cycling: Under normal operation, a Traulsen reach-in freezer cycles off once the setpoint (-2°F to 0°F) is satisfied. If the hermetic condensing unit runs continuously for over 4 hours without entering an off-cycle or defrost interval, the system is suffering from severe heat-transfer loss, coil icing, or refrigerant starvation.
- Gurgling Sounds and Sluggish Door Closure: An audible hissing or gurgling behind the interior rear shroud accompanied by resistance when swinging the door shut often signals ice obstruction within the drain pan or a compromised cam-lift hinge preventing the door from dropping down into its magnetic locking recess.
Recognizing these early diagnostic signals allows restaurant operators to enact defensive containment strategies—such as relocating sensitive proteins to secondary walk-ins—before the Georgia Department of Public Health food safety thresholds are breached. For businesses in Milton, GA and North Fulton, our technicians provide rapid diagnostic dispatch to assess whether the root cause stems from mechanical seal fatigue or deep electrical circuitry faults.
Real Field Restoration: Before vs. After Master Tech Service
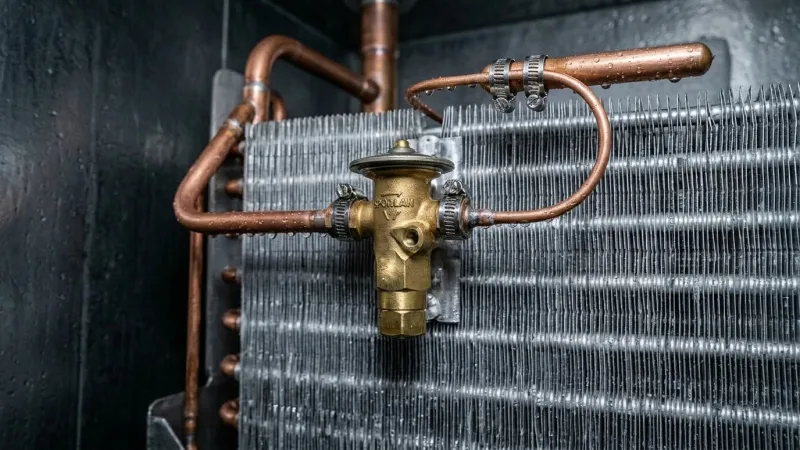
The difference between an aging, failing commercial freezer seal and a factory-restored OEM assembly is stark. When magnetic dart gaskets lose elasticity, the microscopic gap between the Santoprene bellows and the stainless cabinet flange allows warm ambient kitchen air to be drawn into the sub-zero interior vacuum. Below is an authentic macro photographic comparison from our commercial field operations in North Fulton County:
Primary Causes of Hi-Temp Alarms, Gasket Leaks & Coil Frosting
A commercial reach-in freezer is a closed thermodynamic loop. When one sub-system experiences electrical, mechanical, or aerodynamic degradation, the entire thermal balance is disrupted. Drawing from hundreds of service calls across Alpharetta and surrounding Fulton County municipalities, our technicians have categorized the primary failure modes responsible for triggering Traulsen G-Series hi-temp alarm conditions:
Magnetic Dart Gasket Degradation & Mechanical Vacuum Loss
Traulsen G-Series freezers utilize a specialized “dart-style” push-in Santoprene gasket. Unlike older screw-retained gaskets, the dart profile presses directly into an extruded polymer channel along the perimeter of the door liner. Over months of exposure to kitchen grease, aggressive chemical sanitizers, and thermal expansion cycles, the elastomeric Santoprene polymer loses its plasticizer content, becoming brittle and rigid. Furthermore, commercial kitchen staff frequently pull doors open by tugging the flexible gasket bellows rather than using the door handle. This mechanical stress tears the corner joints and dislodges the internal barium-ferrite magnetic strip. Once the seal gap exceeds 0.015 inches, warm air rushes into the cabinet, carrying moisture that freezes onto the nearest cold metal surface: the evaporator coil.
When our technicians evaluate commercial reach-in issues during emergency appliance repair calls, we conduct a precision feeler gauge and pull-force test. A compromised gasket allows between 50 to 120 cubic feet of humid ambient air into the cabinet per hour, overwhelming the design capacity of the electric defrost cycle and causing inevitable coil freeze-up.
Microprocessor Relay Board Failures & Contact Pitting (115V AC)
The Traulsen G-Series INTUITION microprocessor controller relies on an onboard or separate relay board powered by 115V single-phase line voltage. This board houses miniature electromechanical relays responsible for cycling high-amperage inductive loads, including the 1/2 HP or 3/4 HP hermetic compressor, the 450W–600W Incoloy defrost calrod heater, and the ECM evaporator fan motors. Each time the compressor cycles under full lock-rotor inductive load, a micro-arc occurs across the relay contacts. Across culinary kitchens in Roswell, GA, our technicians frequently observe contacts developing carbon pitting and high resistance over years of operation.
When a relay contact burns out completely, the compressor fails to engage when commanded, leaving the freezer in a passive warming state that triggers the “HI” alarm. Alternatively, a relay may weld itself shut in the closed position, keeping the defrost heater energized continuously. When this occurs, the defrost heater battles the refrigeration system, warming the cabinet to +40°F while melting plastic components and destroying frozen product.
Defrost Calrod Heating Element Open Circuit & Termination Thermostat Failure
Because commercial freezers operate well below freezing (-10°F saturated suction temperature), moisture that enters the cabinet inevitably coats the evaporator coil fins in frost. To maintain airflow, the G-Series initiates automatic electric defrost cycles every 6 to 8 hours. The defrost system uses a heavy-duty Incoloy-sheathed calrod heating element woven through the bottom and face of the aluminum fin stack. Under normal conditions, this element draws 3.8 to 5.2 Amps at 115V, dissipating heat that rapidly liquifies frost into the condensate drain trough.
However, continuous thermal expansion and contraction eventually causes the internal nickel-chromium resistance wire to burn open. An open defrost heater displays infinite resistance (OL) on a digital multimeter. When the heater fails, the scheduled defrost intervals cannot melt the accumulated frost. Within 48 hours, the fin spacing (normally 4 to 6 fins per inch) is completely bridged by solid ice, choking airflow and leaving the cabinet unable to pull below +25°F. A defective defrost termination bi-metal switch produces identical symptoms if its internal contacts fail to close at low temperatures, preventing the microprocessor from sending 115V to the heater circuit.
Perimeter Door Frame Heater Open Circuit (45–60 Ω Nominal)
To prevent condensation and ice damming around the door frame, Traulsen embeds a low-wattage electric resistance wire beneath the stainless steel door jambs and center mullion face. Operating continuously on 115V AC, this heater warms the outer metal lip just enough to keep it above the ambient kitchen dew point (typically 62°F to 68°F) without transferring heat into the freezer storage cavity. The design resistance of this heater wire circuit ranges between 45 and 60 Ohms.
If this heater wire burns open or develops an insulation fault against the grounded chassis, the door frame perimeter drops to sub-freezing temperatures. Ambient humidity immediately condenses on the cold stainless steel and freezes into a thick ice ring. This ice dam physically lifts the magnetic gasket away from the face of the cabinet, creating massive air gaps that accelerate evaporator coil frost accumulation and trigger persistent “HI” temperature alerts.
Top-Mounted Condenser Coil Grease Fouling & Airflow Starvation
Even though Traulsen positions the condensing chassis at the top of the cabinet, commercial kitchens in high-traffic plazas like Old Alabama Square generate significant airborne grease vapor from deep fryers, flat-top grills, and commercial cooking lines requiring commercial oven repair. This vapor settles on the condenser coil fins, creating a sticky coating that traps airborne dust and lint. Within 3 to 6 months without chemical coil cleaning, the condenser fin passages become heavily obstructed. This restricts cooling airflow from the ECM condenser fan motor, causing discharge head pressures to skyrocket beyond 380 PSIG (on R-404A systems). Elevated head pressure severely reduces compressor volumetric efficiency and forces the high-pressure safety switch to cut power, resulting in immediate temperature loss.
Safe Kitchen Manager Pre-Diagnostic & Troubleshooting Steps
Before dispatching emergency commercial refrigeration technicians, kitchen managers across Alpharetta and nearby Johns Creek, GA can safely perform preliminary, non-invasive diagnostic checks to pinpoint the issue and protect their inventory. These initial steps help determine whether the alarm is caused by an operational issue (such as an ajar door) or a critical component failure:
Diagnostic Protocol 1: Digital Controller Code Verification & Alarm Silencing
Inspect the front INTUITION or Smart Control LED panel. Silence the audible buzzer by pressing the “Alarm Reset” or “Set” key once. Note the exact readout on the display. If the screen flashes “HI” alternating with a number (e.g., “24”), the unit is reporting cabinet air temperature. If the screen reads “EE” or “E1”, an air thermistor open or short circuit has occurred. If it reads “E2”, the evaporator coil defrost probe has failed. Document this alphanumeric readout immediately for the service technician.
Diagnostic Protocol 2: The Dollar Bill / 0.003-Inch Feeler Gauge Vacuum Resistance Test
To assess magnetic seal integrity across all four door edges, insert a crisp dollar bill or standard feeler gauge halfway between the magnetic gasket and the stainless door jamb. Close the door fully. Slowly pull the bill outward. In a properly sealing Traulsen unit, you should feel distinct, smooth friction resistance (requiring 1.5 to 2.0 lbs of pull force). Repeat this test every 8 inches around the entire perimeter, paying close attention to the bottom sweep and upper hinge corners. If the bill slides out effortlessly with zero resistance, the dart gasket has split or the magnetic strip has lost polarity, allowing ambient air to infiltrate.
Diagnostic Protocol 3: Evaporator Airflow & Discharge Louver Inspection
Open the freezer door and immediately place your hand along the ceiling discharge duct at the top rear of the interior. You should feel strong, high-velocity chilled airflow circulating from the centrifugal blowers. If you hear the blower motors humming but feel virtually zero air movement, shine a flashlight through the return air intake louvers. If you see solid white snow or a solid block of ice encasing the aluminum fin coils, the evaporator has suffered a frost bridge failure and airflow is completely blocked.
Diagnostic Protocol 4: Top-Mounted Condenser Shroud Clearance & Filter Check
Inspect the top of the freezer exterior. Ensure that kitchen staff have not stored sheet pans, cardboard boxes, or dry goods bags on top of the unit. The Traulsen G-Series requires a minimum of 12 inches of unobstructed overhead clearance to discharge superheated condenser exhaust. Remove any stored items and examine the aluminum condenser fins behind the front louvered grille. If the fins are blanketed in thick gray lint or brown grease, air cannot pass through the coil. Do not attempt to scrape the fins with sharp metal objects; inform the technician that chemical coil de-greasing is required.
Diagnostic Protocol 5: Door Cam-Lift Hinge Alignment & Self-Closing Verification
Open the door to a 45-degree angle and release it. The door should self-close smoothly and drop down roughly 1/4 inch onto the cam-lift hinge pin, pulling the magnetic gasket tight against the frame. If the door stalls, sags, or drags against the bottom sweep, the nylon cam-lift hinge inserts have worn out or the hinge bracket screws have vibrated loose. Re-tightening loose hinge mounting bolts is safe for maintenance staff, but replacing damaged hinge cams requires professional support.
Critical Boundaries: When Kitchen Staff Must Cease DIY Interventions
While routine maintenance—such as wiping down gaskets and clearing storage off the unit top—is safe for culinary staff, attempting technical electrical or mechanical repairs on a commercial reach-in freezer poses serious hazards. Kitchen managers must establish clear safety boundaries:
- High Voltage Electrical Dangers (115V / 208V AC): The top-mounted control housing contains high-voltage terminal strips, motor run capacitors holding dangerous residual DC charges, and high-amperage compressor contactors. Contact with live terminals can cause severe shock, electrocution, or arc-flash explosions in wet kitchen environments.
- Risk of Evaporator Coil Puncture: When facing a heavily iced evaporator coil, kitchen workers are often tempted to chip ice away using screwdrivers, ice picks, or meat cleavers. The aluminum tubing and copper return bends operate under high pressure with wall thicknesses of less than 0.028 inches. A single slip punctures the coil, resulting in immediate loss of refrigerant, system contamination, and thousands of dollars in emergency coil replacement costs.
- Federal EPA Section 608 Refrigerant Compliance: Traulsen G-Series freezers operate on EPA-regulated refrigerants, including R-404A, R-448A, R-452A, and hydrocarbon R-290 (propane). Federal Clean Air Act regulations strictly prohibit uncertified individuals from connecting manifold gauges, venting refrigerant, or altering hermetic refrigeration lines. Violations carry substantial civil fines.
- Flammability Risks with Next-Gen R-290 Hydrocarbons: Many newer Traulsen G-Series models utilize flammable R-290 refrigerant. Servicing these sealed systems requires explosion-proof recovery equipment, specialized brass piercing valves, and non-sparking vacuum pumps. Open flames or unrated electrical tools in the presence of an R-290 micro-leak can ignite, creating severe fire and explosion risks in commercial kitchens.
- Microprocessor Board Damage: The INTUITION control board contains sensitive microprocessors that are vulnerable to electrostatic discharge (ESD) and voltage surges. Attempting to jumper terminals or test continuity with consumer meters can fry the microprocessor, turning a simple sensor repair into an expensive full control assembly replacement.
Whenever preliminary diagnostics point to electrical failures, defrost heater issues, or refrigerant leaks, immediately stop in-house troubleshooting. Much like servicing advanced cooling equipment with True commercial refrigerator repair standards, contact our licensed commercial refrigeration team in Alpharetta for safe, code-compliant restoration.
Commercial Reach-In Freezer Repair vs. Equipment Replacement Matrix
Restaurant owners and culinary directors are frequently forced to weigh the economics of repairing an existing commercial freezer against purchasing a new unit. High-end reach-in freezers like the Traulsen G-Series represent substantial capital investments, with replacement costs for commercial two- and three-section units ranging from $6,500 to $13,000+. To make an informed financial decision, facility operators rely on the commercial “50% Rule” alongside lifecycle asset depreciation:
| Decision Factor | Proceed with Precision OEM Repair | Consider Full Unit Replacement |
|---|---|---|
| Equipment Operating Age | Unit is 1 to 9 years old (well within its 15–20 year heavy commercial lifespan). | Unit exceeds 14–16 years with widespread cabinet corrosion. |
| The 50% Economic Rule | Repair quote is under 40% of the replacement cost of a comparable commercial freezer. | Cumulative repair cost exceeds 50% of the price of a brand-new Traulsen model. |
| Cabinet Insulation Integrity | Insulated polyurethane shell is solid with no structural delamination or floor rot. | Cabinet sidewalls are moisture-logged or swelling due to interior breaches. |
| Root Component Failure | Dart gaskets, defrost heaters, bi-metal switches, relay boards, ECM fan motors. | Hermetic compressor locked up on an obsolete R-22 system with internal evaporator leaks. |
| Downtime & Culinary Uptime | Same-day OEM component replacement restores full pull-down within 2 hours. | New commercial reach-ins require 4 to 8 weeks for freight delivery and crating. |
Because Traulsen commercial reach-ins are built with modular, field-replaceable electrical and refrigeration components, over 92% of hi-temp alarm service calls are resolved through targeted repairs. Replacing worn magnetic dart gaskets, installing a new Incoloy defrost element, or swapping a microprocessor relay board restores factory operating efficiency for a fraction of the cost of new equipment.
Instant Commercial Reach-In Repair Cost Estimator Widget
To help commercial kitchen operators, facility directors, and restaurant managers forecast repair budgets accurately, use our interactive 2026 Commercial Cost Estimator below. Select your unit configuration, reported failure symptoms, and equipment age for an immediate projected price range:
Commercial Foodservice Repair Cost Variables & Economics
Repair estimates in commercial foodservice environments vary based on several critical operating factors. Whether servicing luxury refrigeration like KitchenAid appliance repair or heavy-duty Traulsen reach-in freezers, understanding the elements that influence pricing helps kitchen managers make sound operational decisions:
- Number of Door Sections & Linear Gasket Footage: A single-door reach-in freezer requires approximately 18 linear feet of magnetic dart gasket, whereas a two-section or three-section model requires 36 to 54 linear feet. Gasket replacement pricing scales with linear material volume and labor time needed to seat each corner joint properly.
- Genuine OEM Traulsen vs. Generic Aftermarket Parts: We use factory OEM Traulsen parts exclusively. While aftermarket gaskets and universal defrost heaters are available for slightly less up front, they consistently fail within 90 to 180 days in commercial kitchen environments due to poor magnetic strength and inferior temperature ratings. Factory Traulsen parts ensure reliable fitment, long service life, and preserve NSF sanitation certifications.
- EPA Sealed System Refrigerant Work: If the hi-temp condition stems from a clogged TXV power head or refrigerant leak, the repair requires opening the sealed refrigeration system. This involves recovering existing refrigerant, brazing in a new liquid line filter drier, pulling a deep 500-micron vacuum to evacuate non-condensables, and charging precise virgin refrigerant by electronic weight. This work requires specialized EPA Universal certification and advanced tooling.
- Emergency Response Windows & Kitchen Rush Hours: Emergency service calls dispatched outside standard hours or on major culinary weekends may incur expedited emergency dispatch premiums. However, factoring in the risk of losing thousands of dollars in high-value meats, dairy, and seafood, prompt emergency dispatch consistently pays for itself.
Professional Diagnostic Workflow & True-RMS Multimeter Telemetry
Factory-certified commercial refrigeration technicians rely on rigorous electrical and thermodynamic testing rather than guesswork. When addressing a Traulsen G-Series hi-temp alarm, our technicians utilize True-RMS digital multimeters (Fluke 87V series), calibrated thermocouple probes, and digital manifold gauges to verify key operating specifications:
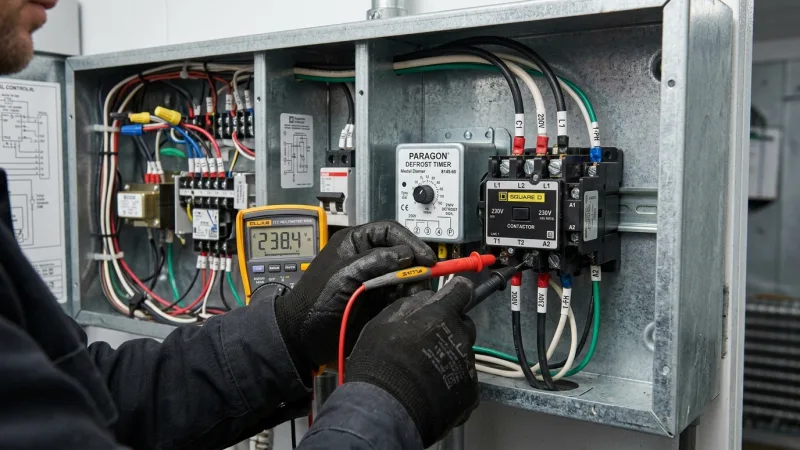
Use the interactive filter tool below to view factory telemetry specifications, target multimeter ohm readings, and pass/fail diagnostic benchmarks for Traulsen G-Series commercial reach-in freezers:
| Component Circuit | Test Terminals & Pinout | Normal Operating Spec | Failure Benchmark Reading | Corrective Action Required |
|---|---|---|---|---|
| Microprocessor Relay Board Supply | L1 to Neutral (Pin 1 to Pin 3) | 115V AC ±10% (104V–126V) | < 102V AC or 0V line drop | Inspect panel breaker, supply cord, and control transformer. |
| Compressor Output Relay (K1) | Relay Output Terminal to Neutral | 115V AC switched call (0.1 Ω contacts) | 0V AC output with “COOL” LED lit | Replace microprocessor relay board assembly. |
| Door Frame Perimeter Heater Wire | Frame Heater Leads (Terminal 7 & 8) | 45 – 60 Ω (continuous resistance) | Infinite ∞ Ω (OL open circuit) | Replace OEM door frame perimeter heater harness. |
| Evaporator Defrost Calrod Heater | Element Terminals across Fin Base | 22 – 30 Ω (450W–600W rating) | Infinite ∞ Ω (OL open element) | Replace Incoloy sheath defrost calrod element. |
| Defrost Termination Bi-Metal Switch | In-line Bi-metal Clip on Suction Bend | < 0.2 Ω closed (< 25°F coil temp) | OL open when iced at 10°F | Replace OEM klixon defrost termination bi-metal switch. |
| Cabinet Temperature NTC Thermistor | Sensor Probe Input Terminals (P1/P2) | 10,000 Ω @ 77°F / 32,650 Ω @ 32°F | 0 Ω (shorted) or > 100k Ω drift | Replace 10K NTC cabinet temperature sensor probe. |
| ECM Evaporator Fan Motor Winding | Motor Connector Harness Pins | 35 – 55 Ω winding resistance | 0 Ω (shorted) or OL open coil | Replace EBM-Papst ECM high-efficiency fan motor. |
| Magnetic Gasket Vacuum Pull Force | Door perimeter sweep to stainless frame | 1.8 – 2.2 lbs/linear foot magnetic pull | < 0.5 lbs/ft (air gaps visible) | Install OEM Santoprene dart-in-channel magnetic gasket. |
Critical OEM Components & Engineering Specifications
Maintaining the high thermal efficiency of a Traulsen G-Series commercial reach-in freezer requires using precision factory replacement parts designed to factory engineering tolerances. Commercial kitchen components face severe mechanical stress, high temperatures, and non-stop operational duty. Below are the primary OEM components frequently replaced during restoration:
Traulsen Santoprene Dart Gaskets
Factory Part Numbers 341-33732-00 and 341-33733-00. Engineered from Santoprene thermoplastic elastomer, these gaskets feature a dual-chamber bellows and high-retention barium-ferrite magnetic strips. Designed for tool-free dart-in-channel installation, they preserve cabinet vacuum and resist commercial fat degradation.
INTUITION Relay Board (115V AC)
Factory Part Number 337-28564-00. Controls high-current loads via dedicated 16A inductive relays for the compressor, defrost heater, and evaporator fan motors. Incorporates internal MOV transient surge suppression to protect sensitive control logic from commercial kitchen electrical noise.
Incoloy Sheathed Calrod Defrost Heater
Factory Part Number 325-60082-00. Rated at 500 Watts / 115V AC (26.5 Ω nominal). Constructed from oxidation-resistant Incoloy alloy with vulcanized moisture-sealed terminal boots to prevent water ingress during steam defrost cycles.
Perimeter Door Frame Wire Heater
Factory Part Number 325-44118-00. Precision continuous-resistance silicone-jacketed heating wire (45–60 Ω) mounted behind door perimeter jambs and center mullions. Prevents outer cabinet sweating and eliminates frost bridges around the door seal.
Sporlan Balanced-Port TXV Valve
Externally equalized thermostatic expansion valve tuned specifically for commercial low-temperature R-404A/R-448A applications. Maintains tight 6°F–8°F superheat across wide variations in kitchen ambient conditions and door usage.
EBM-Papst ECM Evaporator Fan Motor
High-efficiency electronically commutated motor (ECM) engineered for sub-zero operation. Draws up to 65% less power than legacy shaded-pole motors while maintaining constant CFM against frosted coil static pressure.
Preventative Commercial Maintenance Protocols for High-Volume Kitchens
Just as commercial laundries require regular preventative servicing and washing machine repair to maintain sanitation workflows, commercial kitchens must maintain rigid refrigeration upkeep. To prevent costly emergency downtime, preserve equipment warranties, and avoid unexpected hi-temp alarms, foodservice operators along Old Alabama Road should integrate the following preventative maintenance protocols into daily, monthly, and quarterly kitchen schedules:
- Daily Gasket Cleaning & Food Acid Removal: Commercial food acids, animal fats, and grease rapidly deteriorate Santoprene polymers. Train kitchen closing staff to wipe door gaskets nightly using mild, warm soapy water and a soft microfiber towel. Never use concentrated bleach, quaternary ammonia sanitizers, or abrasive scouring pads, as they strip the plasticizers from the rubber bellows and crack corner seams.
- Monthly Condenser Coil Vacuuming: Use a commercial vacuum equipped with a soft-bristle brush attachment to clean the top-mounted aluminum condenser fins monthly. Much like lint trap maintenance protocols in commercial dryer repair, vacuum vertically along the fin direction to avoid bending the delicate aluminum sheets. Maintaining clean fin passages prevents head pressure from elevating and spares the compressor motor from thermal stress.
- Quarterly Chemical De-Greasing & Fin Straightening: In kitchens operating heavy fry stations, dry vacuuming is insufficient to remove baked-on airborne grease. Every quarter, have a certified commercial technician apply a non-acidic, self-rinsing foaming coil cleaner to dissolve baked-on oils. Straighten any bent or crushed fins using a stainless fin comb calibrated to the coil’s fins-per-inch spacing.
- Bi-Annual Condensate Drain Line Flushing: During defrost cycles, melted frost drains into a heated pan located above the compressor. Over time, airborne yeasts, mold, and flour dust settle into the drain trough, forming a gelatinous biofilm that clogs the 1/2-inch drain tube. Flush the drain line twice annually with hot water and an NSF-approved biofilm enzyme treatment to prevent water from backing up and freezing into a solid block at the base of the coil.
- Annual Door Cam-Lift Hinge & Latch Lubrication: Apply food-grade silicone lubricant to the nylon cam-lift hinge pins annually. Inspect the door stop alignment and re-torque mounting bolts to factory specifications. This ensures the door continues self-closing reliably, keeping the magnetic gasket seated tightly against the cabinet face.
Health Inspection, Food Safety Compliance & Regulatory Guidelines
Commercial refrigeration maintenance goes beyond equipment reliability; it is a critical mandate for public health safety and regulatory compliance. Under Georgia Department of Public Health Rules (Chapter 511-6-1) and the FDA Food Code, commercial food service establishments face strict legal standards governing temperature maintenance:
- Strict Frozen Food Holding Standards (0°F or Below): Commercial freezers must maintain product temperatures at or below 0°F (-18°C). If an equipment hi-temp alarm allows internal temperatures to rise above +41°F for more than two hours, public health regulations mandate the immediate condemnation and disposal of all Time/Temperature Control for Safety (TCS) foods to prevent foodborne illness outbreaks.
- Digital Temperature Logging & HACCP Compliance: Foodservice operators must maintain twice-daily written or automated digital temperature logs under Hazard Analysis Critical Control Point (HACCP) regulations. Traulsen G-Series freezers can be integrated with external NAFEM data ports to log temperatures continuously, providing verifiable documentation during environmental health inspections.
- NSF Standard 7 Sanitary Certification: Traulsen reach-in freezers are engineered to comply with NSF Standard 7 sanitary criteria. This standard mandates easily cleanable coved interior corners, NSF-approved food-contact shelving, and durable perimeter gaskets that form tight seals to prevent pest ingress and bacterial colonization. Using non-approved aftermarket parts can compromise NSF compliance during routine inspections.
- OSHA Electrical & Lockout/Tagout (LOTO) Regulations: When commercial technicians service 115V or 208V refrigeration units in commercial facilities, OSHA standard 29 CFR 1910.147 mandates strict Lockout/Tagout procedures. De-energizing and locking out circuit breakers prevents accidental startup of condenser fans or compressors while hands are inside the mechanical cabinet.
Frequently Asked Questions on Traulsen G-Series Reach-In Freezers
Here are direct answers to common diagnostic, maintenance, and operational questions from commercial kitchen operators regarding Traulsen G-Series reach-in freezers:
Related Commercial Refrigeration & Culinary Equipment Services
In addition to Traulsen G-Series reach-in freezer restorations, our licensed technicians provide comprehensive repair and maintenance across the entire commercial kitchen refrigeration and cooking line. Explore our core commercial and luxury residential appliance services:
Commercial Appliance Repair
Full-service commercial cooking and refrigeration repair for restaurants, hotels, corporate dining, and healthcare institutions across North Fulton.
Commercial & Luxury Refrigerator Repair
Precision diagnostics for commercial reach-ins, walk-in coolers, prep tables, and built-in luxury refrigeration systems with same-day emergency dispatch.
Same-Day Emergency Appliance Repair
Priority dispatch within 45 to 90 minutes across Alpharetta, Milton, Roswell, and Johns Creek to prevent inventory losses and kitchen downtime.
Commercial Oven & Range Repair
Specialized service for commercial convection ovens, gas ranges, charbroilers, and heated holding cabinets throughout the greater Atlanta metro area.
We also provide factory-certified repair for commercial and high-end residential brands, including Sub-Zero appliance repair, Viking appliance repair, and dishwasher repair.
Serving Commercial Kitchens Across North Fulton Communities
Our factory-trained commercial technicians provide rapid on-site service across North Fulton County, including:
- Commercial Appliance Repair in Alpharetta, GA (Old Alabama Road, Windward Parkway, Avalon, Downtown Alpharetta)
- Commercial Appliance Repair in Milton, GA (Crabapple Market, Birmingham Crossroads)
- Commercial Appliance Repair in Roswell, GA (Holcomb Bridge Corridor, Canton Street Dining District)
- Commercial Appliance Repair in Johns Creek, GA (Medlock Bridge Road, State Bridge Corridor)
Key Technical Takeaways for Foodservice Operators
- Act Immediately on Flashing “HI” Alarms: The “HI” alert triggers only after cabinet temperatures exceed setpoint limits for 60 consecutive minutes, indicating sustained thermal loss. Silencing the buzzer does not stop product degradation.
- Inspect Magnetic Gaskets Monthly: Over 40% of reach-in freezer hi-temp issues stem from torn Santoprene dart gaskets that leak humid ambient air, creating solid ice bridges across the evaporator fins.
- Verify Frame Heater Resistance (45–60 Ω): Perimeter frame condensation or ice accumulation along center mullions indicates an open door frame heater or severe gasket failure requiring multimeter resistance verification.
- Never Chip Evaporator Ice with Metal Tools: Chipping frost with sharp instruments risks puncturing aluminum coil tubing, turning a simple defrost heater service call into an expensive sealed system overhaul.
- Keep Top-Mounted Condenser Clear: Storing boxes or sheet pans on top of reach-in freezers restricts condenser heat dissipation, driving head pressure up and triggering compressor safety cutoffs.
- Demand Factory OEM Traulsen Parts: Generic replacement gaskets and universal heating elements consistently fail prematurely under heavy commercial duty cycles, risking food safety and voiding NSF compliance.
- True-RMS Multimeter Telemetry Is Essential: Accurate diagnosis requires measuring line voltages (115V AC), calrod element resistance (22–30 Ω), and NTC thermistor response curves to pinpoint root failure causes.
- Maintain Daily Cleaning Schedules: Nightly gasket wipe-downs with warm water and monthly condenser coil cleanings can double equipment operating life and cut emergency service calls by up to 70%.
- Comply with Georgia Public Health Chapter 511-6-1: Foodservice establishments must maintain frozen inventory at or below 0°F. Documenting temperature pull-downs protects operations during health inspections.
- Rely on Local North Fulton Commercial Technicians: With certified technicians stationed across Alpharetta, Milton, Roswell, and Johns Creek, emergency service is available within 45 to 90 minutes.
Same-Day Commercial Refrigeration Dispatch
Restore Sub-Zero Temperatures to Your Traulsen Freezer Today
Don’t let an unexpected hi-temp alarm, torn door gasket, or iced-over evaporator coil jeopardize your culinary inventory or food safety rating. Our master commercial refrigeration technicians provide guaranteed 45-to-90 minute emergency response across Old Alabama Road and North Fulton County.