
When a high-volume artisan pizzeria, brewpub, or Italian trattoria in the bustling Crabapple Market district or along Highway 9 in Milton faces a catastrophic lunch or dinner rush failure, few emergencies cause immediate panic like a dead conveyor deck on a commercial pizza oven. Lincoln Impinger conveyor ovens—including the legendary 1000, 1100, 1400, 1600, and double-stack 3240 series—are engineered to bake hundreds of pies per hour with surgical precision by combining pressurized impingement air columns with a steadily moving wire mesh conveyor. When kitchen staff suddenly notice pizzas burning inside the bake cavity or piling up at the entry point because the drive belt has completely seized, finding fast and precise lincoln impinger conveyor pizza oven belt stopped repair is the only way to avoid thousands of dollars in lost ticket sales. Trust our experienced team for expert commercial appliance repair across North Fulton commercial corridors. When your production line halts, contact our master commercial dispatch team immediately at (770) 796-7742 for prompt, same-day field diagnostics.
Quick Answer: Why Did My Lincoln Impinger Conveyor Belt Stop Moving?
A Lincoln Impinger conveyor belt stops moving due to five primary mechanical and electrical failures: a seized 90VDC permanent magnet gearmotor (armature open circuit or worn carbon brushes), a blown Silicon-Controlled Rectifier (SCR) speed control board, a sheared drive shaft roll pin, an overtensioned or jammed #35 roller chain, or a disconnected Hall-effect optical pulse tachometer. Checking motor armature resistance (normal 45–65 ohms) and DC output voltage isolates the failure rapidly.
Listen to 60-Second Lincoln Oven Conveyor Diagnostic Summary
Narrated by Jason J. (Master Certified Foodservice Cooking Equipment Technician)
Check Same-Day Commercial Pizza Oven Tech Availability in Milton
Verified Local Service
Recently Serviced in Crabapple Market / Milton Corridor
Lincoln Impinger 1450 Double Deck 90VDC Gearmotor & SCR Drive Controller Replacement • Verified 5.0 ★★★★★
Verified Field Service Case Study #LN-8422
Location: Heritage Walk near Crabapple Rd, Milton, GA 30004
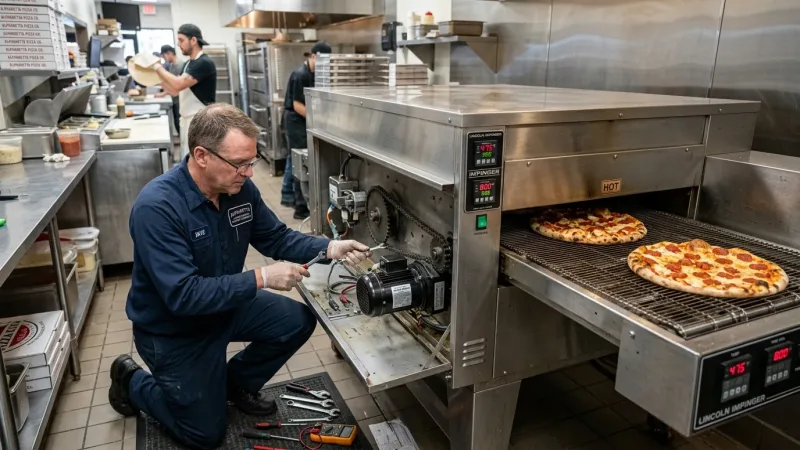
Emergency Conveyor Belt Stoppage & Drive Gearbox Seizure on Lincoln Impinger 1600 Advantage Series
Commercial Facility: High-volume wood-fired and deck hybrid pizzeria operating twin Lincoln Impinger 1600 gas-fired conveyor ovens during Friday evening service.
Reported Symptom: The lower bake deck conveyor belt completely stopped moving at 5:15 PM with 45 tickets on the rail. The digital display blinked intermittently with a drive speed error, and a faint electrical burning odor emanated from the motor control enclosure on the right-hand cabinet. The kitchen staff had attempted to hand-push pizzas through the 28-inch tunnel before calling for immediate emergency support.
Master Technician Multimeter & Mechanical Diagnostic Telemetry:
- Line Voltage Input: 120.4 VAC verified across terminals L1 and Neutral on main terminal strip.
- SCR Speed Controller DC Output: 89.6 VDC present across A+ and A- terminals at maximum speed dial setting, confirming the solid-state speed control board was commanding drive rotation.
- DC Gearmotor Armature Resistance: Measured Infinite Resistance (∞ Open Circuit) across the motor lead disconnect plug (Factory spec: 45.0 to 65.0 Ω).
- Brush Inspection: Removal of the motor carbon brush inspection caps revealed the commutator bars were heavily pitted, and one spring-loaded carbon brush had shattered from thermal stress and severe mechanical chatter.
- Drive Gearbox Resistance: Disengaging the #35 drive roller chain demonstrated that the conveyor shaft spun freely by hand on its flanged ball bearings, ruling out a warped conveyor deck or finger blockage.
Resolution & Verification: The technician installed a genuine Lincoln factory OEM Permanent Magnet DC Gearmotor Assembly (Part #369524), realigned the drive sprockets with laser precision, tensioned the nickel-plated drive chain to 3/8-inch deflection, and calibrated the digital Hall-effect speed pickup. Within 65 minutes of arrival, the oven completed four consecutive test passes at a calibrated 5:30 bake time, restoring full weekend production capacity with a 90-day parts and labor commercial warranty.
Diagnostic Table of Contents
- Understanding Lincoln Impinger Conveyor Drive Architecture
- Symptoms of Impinger Conveyor Belt Stoppage & Drive Failure
- Visual Before & After Gearmotor Restoration Showcase
- Common Causes of Lincoln Conveyor Belt Failure
- Safe Operator Troubleshooting for Pizza Kitchen Managers
- High-Voltage Hazards: When to Cease Kitchen Diagnostics
- Repair vs. Replace Matrix: Drive Gearmotor vs. Conveyor Deck Overhaul
- Instant Lincoln Pizza Oven Repair Cost Estimator
- Commercial Conveyor Repair Cost Factors & Labor Dynamics
- Master Technician Multimeter Diagnostics & Ohms Telemetry
- Critical Lincoln Impinger Conveyor Components
- High-Volume Pizzeria Preventative Maintenance Protocols
- Electrical Lockout, Thermal & Mechanical Safety Protocols
- Frequently Asked Questions: Conveyor Pizza Oven Drive Systems
- Commercial Cooking Service Network & Related Solutions
- Key Technical Takeaways for Commercial Kitchen Operators
- Emergency Commercial Dispatch & Schedule Service
Understanding Lincoln Impinger Conveyor Drive Architecture
In commercial high-capacity baking, the Lincoln Impinger oven stands as an indisputable industry benchmark. Operating throughout Milton pizza kitchens, sports bars, and corporate dining facilities, Lincoln Impingers utilize patented air impingement technology. High-velocity jets of heated air blast through precision-perforated upper and lower finger ducts directly onto dough, cheese, and toppings. This turbulent boundary-layer penetration removes the natural thermal barrier surrounding the food, producing blistering crust caramelization and rapid cheese melt in roughly half the bake time of a traditional deck oven. However, the fundamental mechanical cornerstone of this rapid baking cycle is constant, unwavering conveyor velocity. The entire baking algorithm depends on an unvarying transit speed through the tunnel—typically between 4 minutes and 30 seconds to 7 minutes flat.
To achieve smooth and repeatable conveyor movement across extreme 500°F baking environments, Lincoln incorporates a sophisticated electro-mechanical drivetrain. The core prime mover is a heavy-duty Permanent Magnet Direct Current (PMDC) gearmotor, typically manufactured by Bodine Electric or Bison Gear. Operating on variable rectified DC voltage (ranging from 0 to 90 volts DC), this motor delivers exceptional low-speed torque without cogging. Connected directly to an internal worm-gear or helical reduction gearbox, the motor turns an external drive sprocket. This sprocket engages an ANSI #35 precision roller chain, which in turn rotates the main conveyor drive shaft via a driven sprocket secured with hardened steel roll pins or keyed set screws. When an operator in Milton, GA commercial appliance repair corridors encounters a seized belt, the root cause lies within this delicate chain of electrical rectification, pulse feedback, and mechanical power transmission.
The electronic speed control is regulated by an SCR (Silicon Controlled Rectifier) drive board or a micro-controller board equipped with an optical or Hall-effect pulse tachometer pickup. The tachometer monitors the rotational velocity of the motor armature shaft, sending rapid frequency pulses back to the main control logic. If grease splatter, thermal expansion, worn motor brushes, or a foreign object in the conveyor tunnel creates excessive mechanical drag, the controller detects an RPM drop. When the system can no longer compensate by increasing armature voltage, or when an open circuit prevents electrical current from flowing entirely, the belt stops dead in its tracks. Our certified commercial oven repair technicians specialize in dissecting these complex interactions rapidly, preventing hours of operational downtime.
Symptoms of Impinger Conveyor Belt Stoppage & Drive Failure
Conveyor drive system failures rarely manifest out of absolute silence; they often provide progressive mechanical and electrical warnings before full operational collapse. In high-output Milton pizza kitchens, kitchen supervisors and prep staff should recognize early indicators to halt equipment damage before a complete gearcase seizure or motor burnout ruins an evening rush. If you identify any of the following symptoms on your Lincoln Impinger 1000, 1100, 1400, or 1600 series oven, immediate professional intervention is imperative.
- Sudden and Absolute Belt Arrest: The conveyor belt ceases all linear travel while the main heating blowers and burners continue firing at 475°F. The motor compartment may emit an audible 60Hz or 120Hz electrical hum without rotational output, indicating locked rotor conditions.
- Jerky, Cogging, or Surging Belt Movement: The wire mesh conveyor stutters, pulses, or moves intermittently in micro-bursts. This uneven transport causes severely inconsistent pizza bakes, with pies exiting doughy on one edge and charred on the opposite side due to erratic dwell times.
- Digital Display Error Codes: Modern Lincoln Impinger series equipped with digital displays will throw diagnostic error messages such as “BELT STALLED”, “BELT ERROR”, “SPD ERR”, or flashing bake times. These codes trigger when the Hall-effect tachometer sensor fails to detect pulse feedback within a pre-programmed threshold (usually 10 to 30 seconds).
- Pungent Electrical or Ozone Odor: A sharp, unmistakable scent of burning varnish, melting wire insulation, or ozone emanates from the motor control cabinet. This is a telltale sign of carbon brush arcing, shorted commutator bars, or an overloaded SCR motor speed controller heatsink.
- Drive Chain Slack Slapping & Sprocket Rattling: Metallic clinking, rhythmic snapping, or slapping sounds against the interior of the chain guard indicate excessive chain elongation, severe tooth wear on the drive sprockets, or sheared shaft retention roll pins.
- Motor Free-Wheeling Without Belt Motion: The electric motor can be heard spinning at high RPM inside the cabinet, yet the conveyor belt remains stationary. This symptom conclusively points to a sheared roll pin, a stripped reduction gear set, or a loosened sprocket set screw on the output shaft.
Ignoring these early operational symptoms often leads to catastrophic collateral failure. An overheated, locked DC gearmotor drawing locked-rotor current through the circuit board will quickly destroy delicate trace circuits and triacs on the main control assembly. When you observe even subtle belt hesitation in your commercial kitchen, engaging our same-day commercial appliance repair specialists ensures small component adjustments do not spiral into multi-thousand-dollar kitchen overhauls.
Visual Before & After Gearmotor Restoration Showcase
Extreme commercial kitchen environments place extraordinary demands on conveyor drive components. Fluoropolymer bearing surfaces, high-temperature drive chains, internal motor commutators, and hardened gear assemblies are constantly exposed to airborne cooking oils, cornmeal dust, ambient radiant heat exceeding 140°F inside the control cabinet, and non-stop rotational stress. Review this real-world restoration completed by our commercial field service division in a Milton culinary facility:
Before: Carbonized Commutator & Stripped Reduction Gears
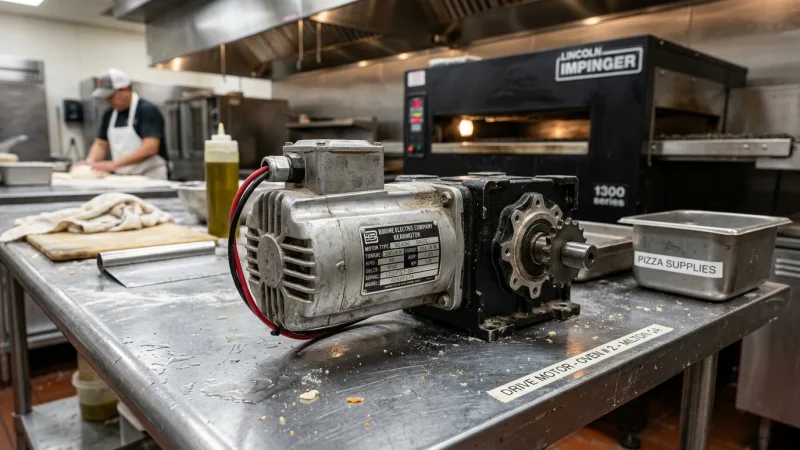
Diagnostic Finding: Severe carbon soot bridging commutator segments, burnt armature winding showing open circuit (∞ Ω), cracked carbon brush housing, and internal gear tooth pitting from heavy flour dust ingestion.
After: Brand-New Factory OEM 90VDC Gearmotor Assembly
Restoration Spec: Factory OEM Lincoln 90VDC PMDC motor installed, calibrated Hall-effect pulse wheel aligned to 0.040-inch air gap, new #35 nickel-plated drive chain tensioned to 3/8-inch play, armature resistance 54.2 Ω.
Common Causes of Lincoln Conveyor Belt Failure
Pinpointing the root engineering cause behind a stopped Lincoln Impinger conveyor belt requires systematically analyzing each electrical, electronic, and mechanical node in the drive assembly. Over decades of commercial foodservice servicing in Milton, our master technicians have isolated the most frequent mechanical and electrical culprits responsible for conveyor shutdowns.
Permanent Magnet DC Motor Armature Burnout & Carbon Brush Wear
The heart of the Lincoln conveyor system is the 90-volt permanent magnet DC motor. Unlike brushless or three-phase AC induction motors, PMDC motors utilize physical spring-loaded carbon brushes to transfer rectified DC electrical energy across a rotating copper commutator. Over tens of thousands of operating hours in a 500°F commercial environment, these carbon blocks naturally wear down. Once the brush length diminishes to less than 1/4 inch, spring tension drops precipitously, inducing severe electrical arcing across the commutator segments. This arcing carbonizes the copper bars, generates immense local heat, and eventually melts the micro-thin lacquer insulation on the copper armature windings. When the windings short to ground or burn open, the motor experiences a total loss of electromagnetic flux, halting rotation instantly. A healthy Lincoln PMDC motor armature should exhibit 45 to 65 ohms of continuous resistance; a burnt motor displays infinite resistance (open) or near-zero resistance (short circuit).
Silicon-Controlled Rectifier (SCR) Speed Control Board Failure
Lincoln Impinger ovens convert standard 120VAC or 208/240VAC single-phase power into variable 0–90VDC output through an electronic speed control board (such as OEM Part #369393 or integrated digital main boards). This board relies upon high-current Silicon-Controlled Rectifiers (SCRs) or field-effect transistors to chop the incoming AC sine wave into variable-width DC voltage pulses. The control board is located inside the side electrical compartment, adjacent to high-temperature cooling blowers. Over years of operation, flour dust, aerosolized oils, and electrical spikes from nearby compressors or refrigeration equipment contaminate the circuit board traces. When an SCR triac breaks down internally, it either fails shorted—causing the conveyor belt to spin uncontrollably at maximum velocity—or fails open, providing 0.0 VDC to the motor terminals despite a call for movement on the front control panel.
Sheared Drive Sprocket Roll Pins & Set Screw Slippage
Mechanical torque transfer from the gearmotor output shaft to the conveyor drive roller relies on drive sprockets fastened via hardened steel roll pins (spring pins) or keyed set screws. As pizza pans, heavy cast iron skillets, or oversized deep-dish screens travel across the wire mesh belt, they generate dynamic rotational friction. If a pizza screen jams against an impingement finger box inside the baking chamber, the motor continues attempting to deliver rotational torque. To protect the expensive gear reducer from total catastrophic shattering, Lincoln engineers incorporate roll pins that act as sacrificial shear points under extreme overload. Once this pin shears cleanly through the shaft diameter, the gearmotor shaft spins freely inside the drive sprocket bore while the conveyor belt remains entirely stationary.
Drive Chain Binding, Stretching & Sprocket Misalignment
The ANSI #35 roller chain connecting the gearmotor to the conveyor shaft operates under high thermal stress and cyclic shock loads. In busy Milton pizzerias, routine chain lubrication is frequently overlooked. Without regular application of high-temperature, food-grade synthetic graphite or non-silicone chain lubricant, the chain links experience metal-to-metal galling. Carbonized cornmeal and grease dust penetrate the roller bushings, causing links to bind rigidly. As the chain elongates (“stretches”) from bushing wear, it begins riding up on the sprocket tooth tips rather than seating deep in the root diameter. Eventually, the chain either jumps off the sprockets entirely or bunches up against the protective sheet metal housing, jamming the entire drivetrain.
Hall-Effect Tachometer & Optical Pulse Pickup Sensor Failure
On modern digital Lincoln Impinger ovens, the control board requires real-time rotational feedback to confirm the conveyor is traveling at the exact bake time set by the chef. This feedback is supplied by a Hall-effect magnetic pickup or an optical interrupter wheel mounted directly on the tail shaft of the drive motor. As the motor turns, the sensor generates a 0 to 5-volt square wave pulse train. If cornmeal dust coats the optical receiver, if the sensor air gap shifts beyond 0.050 inches due to vibration, or if the sensor’s silicon chip degrades from thermal soaking, pulse transmission halts. The microprocessor interprets this loss of signal as a stalled conveyor and initiates an emergency safety shutdown of the drive circuit to prevent unattended pizzas from catching fire within the radiant bake chamber.
Safe Operator Troubleshooting for Pizza Kitchen Managers
When a conveyor belt stops moving during active food service, kitchen managers in Milton can perform a series of safe, non-invasive diagnostic checks before calling for professional field dispatch. Performing these immediate checks helps isolate whether the issue is a simple external mechanical jam or a complex internal electrical breakdown.
Operator Step 1: Immediate Safety Isolation & Visual Tunnel Inspection
Immediately switch off the conveyor speed switch on the front control panel to stop feeding voltage into an overloaded motor. Put on high-temperature thermal oven mitts (rated to 500°F) and illuminate the entire interior of the baking tunnel using a high-lumen flashlight. Inspect every inch of the wire conveyor belt where it passes above and below the impingement air fingers. Check for dropped pizza pans, warped baking screens, stray spatulas, or accumulated food debris wedged tightly between the wire belt and the air finger nozzles. If an obstruction is found, allow the oven to cool down before attempting extraction to avoid severe second-degree burns.
Operator Step 2: Conveyor Belt Free-Travel Manual Pull Test
With the oven main power switch turned OFF, attempt to manually grasp the wire conveyor belt at the exit end using heavy leather work gloves and pull it gently in the direction of normal travel. In a healthy system with a reduction gearbox, you should feel firm, uniform mechanical resistance, but the belt should yield slightly without harsh binding. If the belt feels completely locked like a solid steel wall, the obstruction is mechanical—either a seized drive shaft bearing, a foreign object in the tunnel, or locked reduction gears. Conversely, if the belt moves effortlessly with zero resistance while the drive motor does not turn, a roll pin has sheared or the drive chain has dislodged.
Operator Step 3: Drive Chain & Guard Inspection
Locate the removable drive chain guard on the side or rear of the conveyor frame. Without opening electrical enclosures, inspect the external chain drive. Check whether the ANSI #35 roller chain is intact, properly seated on both the motor sprocket and the conveyor shaft sprocket, and free of foreign debris. If the chain is dangling loose or has derailed, do not attempt to force it back onto the sprockets while hot; misalignment or broken teeth will cause immediate recurrence.
Operator Step 4: Speed Potentiometer & Digital Display Audit
If your Lincoln oven utilizes an analog dial speed controller, gently rotate the speed control knob from its minimum setting (e.g., 1 minute) to its maximum setting (e.g., 30 minutes) several times with the power on. Listen closely for changes in motor pitch or relay clicks. In many commercial kitchens, flour dust invades the internal carbon wiper of the 10kΩ potentiometer, creating dead spots where electrical continuity is lost. If the digital display blinks an error code or displays “–:–“, note the exact display readout for our service technician.
High-Voltage Hazards: When to Cease Kitchen Diagnostics
Commercial conveyor pizza ovens are high-voltage industrial machines engineered with complex, interconnected circuits. While checking for external conveyor jams is well within the scope of restaurant management, removing electrical access panels introduces severe, life-threatening hazards. Kitchen personnel must immediately cease all troubleshooting and contact an authorized commercial service agency under the following conditions:
- 208V / 240V / 480V Three-Phase Supply Exposure: Lincoln Impingers are powered by high-amperage dedicated electrical circuits. Even with the front control switch turned off, line voltage remains continuously energized across the primary contactors, transformers, and terminal strips inside the control cabinet. Contact with live bus bars can cause fatal electrical shock or severe arc flash injuries.
- High-Voltage DC Motor Bus Capacitors: The solid-state SCR motor controller utilizes large electrolytic filtering capacitors that store high-voltage direct current (up to 130VDC) long after the oven has been unplugged or disconnected at the wall breaker. Touching capacitor terminals can discharge hazardous energy instantaneously through testing tools or human tissue.
- Internal Gearbox Teardown & Spring Tensions: Attempting to disassemble the sealed Bodine or Bison gearcase on the kitchen prep table risks releasing high-pressure synthetic grease, stripping internal bronze worm gears, and misaligning internal needle thrust bearings. Factory gearmotors must be bench-serviced or replaced as matched assemblies.
- Severe Radiant Heat & Thermal Burns: The stainless steel inner chassis, finger assemblies, and conveyor framework retain heat upwards of 400°F for over two hours after shutdown. Unskilled disassembly of conveyor rails while hot invariably results in severe contact burns.
If non-invasive checks do not immediately free the conveyor, do not risk employee safety or compromise manufacturer warranties. Contact our emergency appliance repair team for fast, OSHA-compliant commercial service throughout the Milton area.
Repair vs. Replace Matrix: Drive Gearmotor vs. Conveyor Deck Overhaul
A brand-new commercial Lincoln Impinger single-deck conveyor oven costs between $14,000 and $28,000, while double and triple-stacked configurations easily exceed $45,000 installed. When faced with a conveyor belt failure, restaurant owners must make financially sound decisions balancing capital expenditure against projected operational life. The industry-standard 50% Rule dictates that if the total estimated repair cost is less than 50% of the cost of a replacement unit and the oven has not exceeded its useful mechanical lifespan (typically 12 to 15 years with proper maintenance), repairing the sub-assembly is overwhelmingly the most profitable choice.
| Diagnostic Condition | Recommended Action | Estimated Investment | Operational Lifespan Added | Strategic ROI Assessment |
|---|---|---|---|---|
| Failed 90VDC Gearmotor (Burnt Armature / Brushes) | Replace with Factory OEM Motor Assembly | $650 – $1,250 | 5 to 8 Years | Exceptional ROI. Restores factory conveyor torque and speed regulation at ~5% of new oven replacement cost. |
| Blown SCR Speed Control Board / Potentiometer | Replace Solid-State Board & Calibrate Tachometer | $450 – $850 | 6 to 10 Years | Immediate payback. Eliminates jerky speeds and restores exact culinary bake times without modifying chassis. |
| Worn #35 Drive Chain, Sprockets & Shaft Roll Pins | Mechanical Drivetrain Overhaul & Alignment | $280 – $550 | 3 to 5 Years | Essential routine mechanical rebuild. Prevents sudden tooth slipping and protects the motor reduction gearbox. |
| Warped Conveyor Frame, Cracked Cavity & Rusted Chassis | Evaluate Total Oven Replacement | $14,000 – $28,000+ | 15+ Years (New Unit) | Advised only when the heat exchanger has cracked, the blower motor is shorted, or the chassis has lost structural integrity. |
Commercial Conveyor Repair Cost Factors & Labor Dynamics
Commercial kitchen managers budgeting for equipment maintenance need transparency regarding what factors influence the final invoice for Lincoln conveyor oven servicing. Unlike residential appliance repairs, commercial foodservice equipment demands specialized master certifications, industrial-grade electrical testing, and severe environment-rated components. Several critical variables dictate the overall cost:
- OEM Part Sourcing vs. Substandard Aftermarket Units: Lincoln Impinger gearmotors operate at specialized reduction gear ratios (typically between 40:1 and 60:1) with specialized high-temperature windings. Installing cheap aftermarket universal motors inevitably leads to premature winding failure, tachometer pulse mismatches, and inaccurate baking speeds. Genuine Lincoln OEM parts carry higher wholesale costs but deliver multi-year industrial reliability.
- Single Deck vs. Double / Triple Stack Access: Servicing a single-deck Lincoln oven at waist height is straightforward. In stacked multi-deck configurations, servicing the upper deck or tight middle cavity often requires partial dismounting of heat shielding, specialized compact angle drivers, and two-man technician teams to safely manipulate heavy conveyor frames.
- Emergency Rush Dispatch vs. Scheduled Maintenance: A catastrophic belt seizure occurring at 6:30 PM on a Friday during Crabapple Market peak dining demands immediate emergency dispatch. After-hours, weekend, and holiday emergency dispatches carry premium labor rates compared to pre-scheduled weekday morning maintenance windows.
- Collateral Drive Component Wear: When a gearmotor locks up, it rarely fails in isolation. Often, the drive chain has elongated, the sprocket teeth have hooked, and the nylon drive belt idler bushings have worn oval. Replacing the complete wear set alongside the motor adds modest parts expense but completely prevents repeat breakdowns.
For an exhaustive breakdown of commercial service rates and preventative maintenance plans across North Fulton County, consult our comprehensive commercial appliance repair cost guide.
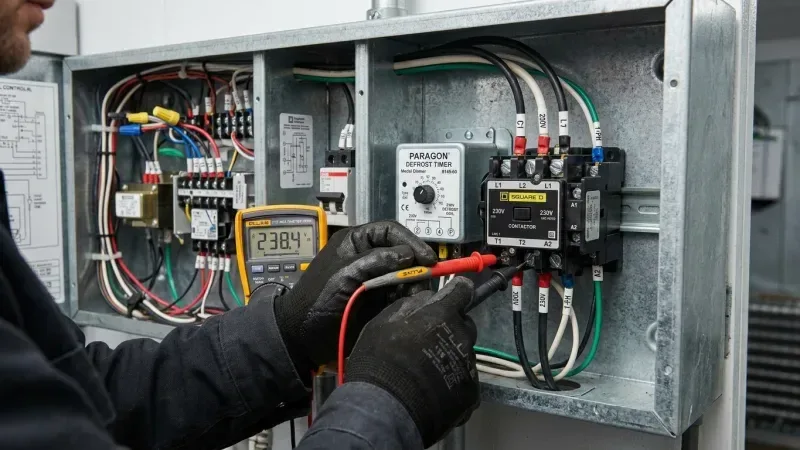
Master Technician Multimeter Diagnostics & Ohms Telemetry
Commercial foodservice technicians do not guess or swap parts blindly; we execute systematic electrical telemetry measurements using calibrated True-RMS digital multimeters (Fluke 87V or equivalent). By measuring DC armature resistance, incoming AC line voltages, rectified DC speed outputs, and pulse frequency waves, our master technicians pinpoint the exact defective component in minutes.
| Component / Test Point | Multimeter Setting | Expected Factory Reading | Failure Telemetry Reading | Diagnostic Conclusion |
|---|---|---|---|---|
| PMDC Motor Armature Winding | Resistance (Ω) | 45.0 – 65.0 Ω | ∞ (OL) or < 5.0 Ω | Open circuit winding, carbonized brushes, or shorted commutator bars. Motor must be replaced. |
| SCR Controller DC Output (A+ / A-) | DC Volts (VDC) | 0 – 90.0 VDC (Smooth ramp) | 0.0 VDC steady or 120+ VDC raw | Blown SCR triac, burnt gate circuit, or shorted rectifier diode on speed control board. |
| Speed Control Potentiometer | Resistance (Ω) | 0 – 10,000 Ω (Linear sweep) | Erratic jumps, ∞ at midpoint | Worn or contaminated carbon track causing speed signal dropouts. Replace 10kΩ potentiometer. |
| Hall-Effect Tachometer Output | DC Volts / Frequency (Hz) | 0 to 5.0 VDC Square Pulse Train | Flat 0.0 VDC or Flat 5.0 VDC | Failed pickup sensor, dirty optical disc, or excessive air gap. Triggers “BELT STALLED” error. |
| Step-Down Control Transformer Secondary | AC Volts (VAC) | 24.0 ± 2.0 VAC | 0.0 VAC or < 18.0 VAC | Blown secondary fuse or open primary winding. Low voltage causes microprocessor reboot lockouts. |
| Conveyor Frame Ground Continuity | Continuity / Ohms (Ω) | < 0.5 Ω to Earth Ground | > 2.0 Ω or Open | Poor ground bond introduces EMI noise into tachometer circuit, causing erratic conveyor speed hunting. |
Critical Lincoln Impinger Conveyor Components
Understanding the exact factory components that comprise the Lincoln conveyor drive train helps kitchen owners comprehend the scope of professional repairs. Our commercial mobile response vans carry genuine Lincoln OEM parts to ensure immediate, single-visit restoration:
- Lincoln OEM Permanent Magnet DC Gearmotor Assembly (Part #369524 / #370165): A rugged, sealed 90VDC motor featuring heavy copper commutator bars, replaceable spring-loaded carbon brushes, and an integrated high-torque reduction gearbox lubricated with synthetic extreme-pressure grease.
- SCR Motor Speed Control Board (Part #369393 / #370397): The solid-state power electronic board that converts 120VAC line power into precision-modulated 0–90VDC armature voltage, maintaining tight speed regulation even under variable conveyor loading.
- Optical / Hall-Effect Pulse Tachometer Assembly (Part #369395): A digital pickup sensor that reads slotted chopper wheels or magnetic rings on the motor shaft to provide closed-loop RPM feedback to the central processing display.
- ANSI #35 Nickel-Plated Heavy-Duty Roller Chain: High-tensile, heat-treated roller chain engineered specifically to resist corrosion from cooking grease and survive high-temperature baking environments without premature pitch elongation.
- Hardened Steel Drive & Driven Sprockets: Precision-machined, induction-hardened sprockets with keyed hubs and roll-pin bores that transfer rotary power to the 1-inch stainless steel conveyor drive shaft.
- Flanged Conveyor Shaft Bearings & Fluoropolymer Bushings: Food-grade, high-temperature composite bushings that support the conveyor drive and idler shafts, eliminating friction and preventing shaft galling.
High-Volume Pizzeria Preventative Maintenance Protocols
Pizzeria kitchens in Milton operating during intense high-volume shifts can dramatically reduce unexpected conveyor failures by enforcing disciplined, scheduled preventative maintenance routines. Adopting these factory-recommended practices protects vital gearcase bearings and extends drive motor life by several years:
Daily Protocol: Crumb Tray Evacuation & Belt Inspection
At the conclusion of every evening shift once the oven has cooled below 120°F, slide out the lower crumb trays and thoroughly empty all charred flour, cornmeal, and cheese remnants. Inspect the wire conveyor belt links for snagged wire tines or foreign objects. Never allow baked cheese or carbonized crust to harden on the conveyor drive rollers, as buildup introduces eccentric runout and increases radial bearing loads.
Weekly Protocol: High-Temperature Drive Chain Lubrication
Remove the drive chain inspection cover and apply a light coating of NSF-certified high-temperature synthetic food-grade chain lubricant (or colloidal dry graphite spray) across the roller links. Never use standard petroleum oils, WD-40, or cooking spray, as these attract abrasive flour dust, gummy residues, and carbonize into hard varnish at oven temperatures. Check that chain deflection remains between 1/4 inch and 3/8 inch at mid-span.
Monthly Protocol: Control Compartment Air Filter De-Greasing
The side electrical control compartment relies upon cooling intake fans to evacuate heat generated by the SCR board, transformers, and drive motor. Remove the metal mesh grease filters from the cooling fan intakes, soak them in hot commercial degreaser, rinse thoroughly, dry completely, and reinstall. Clogged cooling filters cause cabinet temperatures to soar past 150°F, causing SCR triacs to de-rate and motor brushes to soften and pit.
Quarterly Protocol: Professional Carbon Brush & Tachometer Audit
Have a certified commercial technician remove the screw-in brush caps on the Bodine gearmotor to measure remaining carbon brush length. If brushes are worn past 50% of original length, replace them proactively. Clean commutator bars with non-conductive electrical contact cleaner, blow away accumulated carbon soot with dry filtered air, and verify tachometer optical sensor alignment.
Electrical Lockout, Thermal & Mechanical Safety Protocols
Commercial food-service kitchen environments present overlapping physical, thermal, and electrical hazards. Adhering to strict safety protocols protects restaurant employees, service technicians, and the physical premises from catastrophic injuries or structural fires during conveyor oven maintenance:
- OSHA Lockout / Tagout (LOTO) Compliance: Prior to opening any mechanical chain guard or electrical access panel, the oven’s electrical supply must be isolated. Turn off the dedicated wall breaker or disconnect switch and apply a physical lockout padlock with an informational tag. Never rely on the unit’s front control switch to de-energize the cabinet.
- Conveyor In-Running Nip Point Hazards: Where the wire conveyor belt passes over the drive and idler sprockets, powerful mechanical pinch points exist. Never attempt to adjust chain tension, spray lubricant, or wipe crumbs while the conveyor belt is in motion. Loose aprons, chef coats, jewelry, or long hair can be drawn into the drive sprockets within a fraction of a second, causing severe crushing injuries.
- Radiant Burn Mitigation & Cooldown Periods: Impingement finger assemblies and conveyor framework operate at 450°F to 550°F. Allow the oven to undergo a full 90-minute cooldown cycle with cooling blowers running before servicing interior conveyor deck rails. Technicians must wear Kevlar heat-resistant sleeves and insulated safety gloves when inspecting recently operated units.
- Gas Line Isolation for Gas-Fired Impingers: When servicing gas-fired Lincoln Impingers (Natural Gas or Propane), close the manual gas shutoff valve upstream of the flexible quick-disconnect line before rolling the oven away from the wall to access rear motor compartments. Always test flexible gas joints with an electronic combustible gas sniffer after repositioning.
Frequently Asked Questions: Conveyor Pizza Oven Drive Systems
Browse answers to the most common questions raised by Milton pizzeria managers, executive chefs, and restaurant operators regarding Lincoln Impinger conveyor drive systems:
Why did my Lincoln Impinger conveyor belt stop moving during service?
The conveyor belt stops moving primarily due to a burnt permanent magnet DC gearmotor (armature open circuit or worn carbon brushes), a failed SCR motor speed control board, a sheared drive sprocket roll pin, an overtensioned or seized #35 drive roller chain, or a disconnected Hall-effect pulse tachometer pickup. Internal finger box obstructions in the tunnel can also mechanically jam the wire belt.
What does the “BELT STALLED” or “SPD ERR” error code mean on a Lincoln oven?
The “BELT STALLED” or speed error code indicates that the main micro-controller board is commanding the conveyor motor to run but is not receiving pulse feedback from the Hall-effect or optical tachometer sensor on the motor shaft. This occurs when the motor armature has failed, the drive chain is jammed, the tachometer sensor is dirty or misaligned, or the conveyor belt is physically blocked inside the tunnel.
Can I push pizzas through the conveyor tunnel manually if the motor stops?
We strongly advise against manually pushing pizzas through the baking tunnel. Doing so produces severely uneven, ruined bakes, creates extreme risks of 500°F contact burns for kitchen staff, and can buckle the wire conveyor belt mesh against the impingement air fingers, multiplying repair costs substantially.
What electrical resistance should a healthy Lincoln Impinger gearmotor show?
A healthy Lincoln 90VDC permanent magnet DC gearmotor armature winding should exhibit between 45.0 and 65.0 ohms of resistance across the motor leads with carbon brushes properly seated. A reading of infinite resistance (∞ or OL) indicates an open circuit winding or worn-out brushes, while a reading below 5.0 ohms indicates a dead short circuit.
Why is my conveyor belt jerky and stuttering rather than moving smoothly?
Jerky, stuttering belt movement is commonly caused by an overtightened or unlubricated #35 drive chain, severely worn motor carbon brushes causing intermittent arcing, a dirty 10kΩ speed potentiometer with dropouts, or heavily worn composite conveyor shaft bushings causing mechanical binding.
How much does it cost to replace a Lincoln Impinger gearmotor in Milton, GA?
Replacing a genuine factory OEM Lincoln 90VDC gearmotor typically ranges from $650 to $1,250 depending on the oven series (1100 countertop vs. 1400/1600/3240 floor models), whether after-hours emergency dispatch is required, and whether related drive sprockets and chains require concurrent replacement.
What type of lubricant should be used on the Lincoln oven drive chain?
Only use NSF-certified high-temperature synthetic food-grade chain lubricant or colloidal dry graphite lubricant rated to at least 500°F. Never use standard motor oils, petroleum grease, or cooking sprays, as they vaporize, smoke, attract cornmeal, and bake into abrasive carbon varnish.
Why does the motor spin inside the cabinet but the belt doesn’t move?
When the motor spins freely without belt motion, the mechanical connection has severed. This is caused by a sheared drive sprocket roll pin (sacrificial shear pin), a loosened set screw on the output shaft keyway, a derailed or broken #35 drive chain, or stripped internal reduction gears inside the gearbox.
Can worn motor carbon brushes be replaced without replacing the entire gearmotor?
Yes, if caught early before the commutator bars are grooved, pitted, or melted. If the armature windings test healthy (45–65 ohms) and the commutator is clean, installing genuine OEM carbon brush sets and tension springs can restore reliable operation at a fraction of motor replacement cost.
How fast can a technician arrive for emergency pizza oven repair in Milton?
Our priority commercial dispatch guarantees rapid response for active commercial kitchens in Milton, with certified commercial technicians arriving on-site within 45 to 90 minutes. Our service vehicles carry genuine Lincoln OEM replacement parts for same-day resolution.
What causes the SCR motor speed control board to fail?
SCR boards fail primarily from excessive heat buildup inside the control compartment caused by clogged cooling fan filters, airborne grease and flour dust accumulation creating electrical shorts, voltage transients from power grid surges, or sustained locked-rotor motor conditions drawing excessive current.
How is Lincoln conveyor bake time calibrated after motor replacement?
After replacing the gearmotor, technicians place a test target on the conveyor wire and use a digital stopwatch to measure transit time from the entry tunnel lip to the exit lip. Technicians adjust the board’s MIN and MAX calibration trimpots or program the microprocessor digital speed parameters until physical bake time matches the digital display to within ±2 seconds.
Can a Lincoln Impinger oven be converted from 120V to 208V/240V conveyor drive?
Lincoln Impinger conveyor drive systems operate on DC voltage supplied by an internal step-down transformer or SCR rectifier board. Regardless of whether the incoming building supply is 120V single-phase or 208V/240V three-phase, the internal drive motor operates on regulated 90VDC. Any voltage re-tapping must strictly follow factory wiring schematics.
How often should Lincoln conveyor drive roller chains be replaced?
In high-volume commercial kitchens, the ANSI #35 nickel-plated roller chain should be replaced every 18 to 24 months, or immediately if pitch elongation exceeds 3% or if roller links exhibit tight binding that cannot be relieved with high-temperature lubricant.
What warranty coverage is provided on Lincoln Impinger commercial repairs?
All commercial pizza oven repairs performed by Appliance Repair Alpharetta include a comprehensive 90-day warranty covering both genuine Lincoln OEM factory parts and professional labor. If any installed component fails within the warranty window, warranty service is dispatched immediately at zero additional charge.
Do you service other commercial conveyor and pizza oven brands in Milton?
Yes. In addition to Lincoln Impinger series, our certified commercial technicians service Middleby Marshall, Blodgett, Bakers Pride, Vulcan, Hobart, and TurboChef commercial baking equipment throughout Milton, Alpharetta, Roswell, and Johns Creek.
How do I schedule same-day commercial pizza oven service in Milton, GA?
You can schedule immediate same-day commercial service by calling our dedicated commercial dispatch line directly at (770) 796-7742. Our service coordinators will record your oven model, serial number, and reported symptoms to dispatch a fully equipped commercial repair vehicle immediately.
Commercial Cooking Service Network & Related Solutions
Appliance Repair Alpharetta provides complete commercial kitchen maintenance support across North Fulton County. Explore our specialized commercial service divisions and related diagnostic guides:
Commercial Cooking Services
Emergency diagnostics and factory OEM part replacements for restaurant cooking lines across North Atlanta.
Explore our specialized commercial cooking equipment service solutions across North Fulton.
Commercial Refrigeration
Certified EPA Universal technicians servicing prep tables, walk-in coolers, blast chillers, and commercial ice makers.
Commercial Refrigerator Repair •
Reach-In Freezer Repair •
Commercial Ice Maker Service
Local Service Corridors
Dedicated mobile commercial repair units stationed across North Fulton municipalities for sub-90-minute arrival.
Milton, GA Service •
Alpharetta, GA Service •
Roswell, GA Service •
Johns Creek, GA Service
Diagnostic Problem Guides
Explore in-depth technical walkthroughs for common commercial restaurant equipment failures and error codes.
Walk-In Cooler High Temp Alarm •
Traulsen High Pressure Alarm •
Scotsman Ice Machine Sensor Fault
Our technicians also provide comprehensive culinary support for kitchen dishwashing lines via our specialized commercial dishwasher repair team, as well as high-temperature convection units through our commercial convection oven igniter repair specialists.
Key Technical Takeaways for Commercial Kitchen Operators
- Conveyor Belt Velocity Governs Baking Precision: Lincoln Impinger air impingement technology relies upon strictly uniform transit times; when the belt hesitates or arrests, pizza burning and immediate kitchen disruption occur.
- The 90VDC PMDC Motor is the Primary Prime Mover: Healthy motor armature resistance measures between 45.0 and 65.0 ohms; an open circuit (∞ Ω) indicates burnt copper windings or worn-out carbon brushes.
- SCR Speed Boards Modulate Direct Current: A blown SCR board either delivers 0.0VDC (dead conveyor) or full raw voltage (uncontrollable runaway speed), necessitating board replacement.
- Roll Pins Act as Sacrificial Shear Fuses: When the drive motor spins loudly but the conveyor belt remains stationary, a sheared sprocket roll pin has successfully protected the reduction gearbox from catastrophic destruction.
- Only Use High-Temperature Food-Grade Chain Lubricant: Standard oils, WD-40, and cooking sprays carbonize at 500°F, accelerating chain wear and causing catastrophic sprocket binding.
- Never Attempt Live Electrical Diagnostics: 208V/240V lines and high-voltage DC bus capacitors inside the electrical enclosure present severe electrical shock and arc flash hazards.
- Fast Priority Commercial Dispatch is Accessible: Appliance Repair Alpharetta provides same-day emergency dispatch throughout Milton commercial districts with a 90-day parts and labor warranty.
Emergency Commercial Dispatch & Schedule Service
Priority Commercial Pizzeria Service • Milton & North Fulton
Restore Your Lincoln Conveyor Pizza Oven to Peak Production Today
Do not let a seized conveyor gearmotor, severed drive pin, or erratic SCR speed control board shut down your pizza production line. Our factory-trained master commercial technicians arrive equipped with genuine Lincoln OEM parts to restore your deck on the spot.
Serving Milton, Crabapple, Alpharetta, Roswell, Johns Creek • Certified EPA & Master Commercial Electricians • 90-Day Comprehensive Warranty