
Scotsman Commercial Nugget Ice Machine Bin Sensor Stuck Full Troubleshooting in Milton, GA
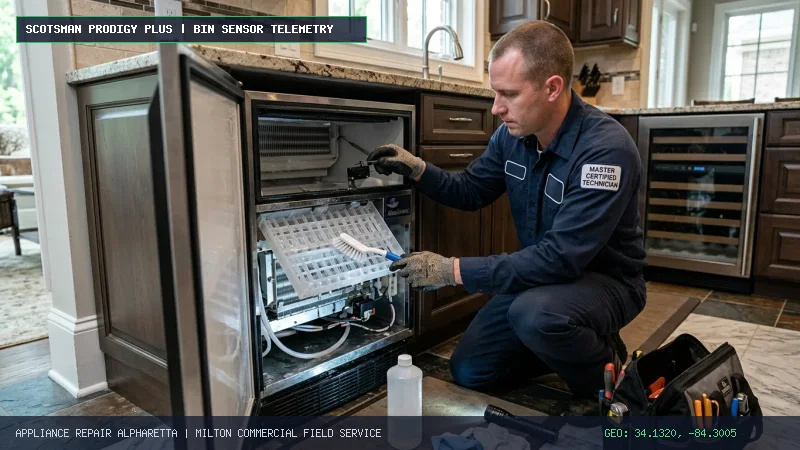
When a commercial Scotsman Prodigy Plus, Meridian, or modular nugget ice machine in Milton, GA displays an illuminated bin full indicator or diagnostic code “b” despite an entirely empty storage bin, the refrigeration and extrusion harvest systems immediately shut down. In high-demand equestrian clubhouse kitchens, Crabapple taverns, medical therapy facilities, and fast-casual beverage bars throughout North Fulton County, an unexpected nugget ice shortage creates critical operational bottlenecks and food service disruptions. Our factory-trained refrigeration specialists provide same-day emergency diagnostic testing, optical infrared sensor descaling, mechanical curtain switch realignment, and OEM controller board restoration to keep your ice supply operating at peak capacity. For priority commercial dispatch, call our master technical team directly at (770) 796-7742.
Quick Answer: Why Is Your Scotsman Nugget Ice Machine Bin Sensor Stuck Full?
A Scotsman commercial nugget ice machine indicates a stuck “Bin Full” status when its electronic controller continuously senses an obstructed ice drop zone. In Prodigy Plus modular units, this fault is primarily caused by calcium carbonate mineral scale or airborne yeast biofilm occluding the dual infrared photoelectric eyes, an ice-bridged discharge chute, a physically misaligned magnetic curtain switch, or a deteriorated 5VDC sensor wiring harness that mimics constant beam interruption.
Listen: Scotsman Nugget Ice Machine Bin Sensor Field Diagnostic
Key commercial troubleshooting takeaways for Milton kitchen managers & facilities engineers (3 min audio briefing)
Play Audio
Check Milton Commercial Refrigeration Service Availability
Enter your facility zip code to verify immediate commercial ice machine technician dispatch windows:
Live Dispatch Activity in Milton & Surrounding Fulton County
- Yesterday, 2:15 PM: Scotsman Prodigy Plus N0622 nugget ice machine optical sensor descaling & harness reset — Equestrian Clubhouse dining room, Birmingham Hwy, Milton, GA 30004.
- Thursday, 10:40 AM: Replaced defective infrared bin level sensor kit (OEM Part A39030-021) on Scotsman NS0422 nugget maker — Specialty bistro, Crabapple Rd, Milton, GA 30004.
- Wednesday, 4:55 PM: Diagnostic troubleshooting of code “b” false bin full lockout & auger gearbox inspection — Private athletic training center, Hopewell Rd, Milton, GA.
- Tuesday, 11:20 AM: Complete Scotsman water system sanitation, curtain switch alignment & descaling — Farm-to-table grill, Arnold Mill Rd, Milton, GA.
Table of Contents — Scotsman Bin Sensor Diagnostic Guide
- Introduction: The Critical Nature of Commercial Ice Production & Sanitation Compliance
- Operational Symptoms & Scotsman AutoAlert Diagnostic Status Codes
- Visual Before & After Macro Pair: Calcified Sensor Aperture vs. Descaled Optical Assembly
- Six Primary Causes of False Bin Full Lockouts in Scotsman Nugget Makers
- Step-by-Step Safe Facility Troubleshooting Protocols for Kitchen Staff
- When to Halt In-House Troubleshooting: High Voltage, Mechanical, and EPA Regulations
- Commercial Financial Decision Matrix: Repairing vs. Replacing Your Ice Machine
- Interactive Instant Repair Cost Estimator for Scotsman Ice Machines
- Estimated Commercial Repair Cost Factors Breakdown in North Fulton County
- How Certified Technicians Diagnose: Multimeter, DC Voltage & Optical Telemetry
- Critical Genuine OEM Scotsman Replacement Parts Involved in Sensor Repairs
- Facility Preventative Maintenance Schedules to Prevent Future Lockouts
- Commercial Facility Health, Electrical, and Chemical Safety Guidelines
- Frequently Asked Questions Regarding Scotsman Ice Machine Bin Controls
- Commercial Technical Resources, Regional Coverage & Brand Silos
Introduction: The Critical Nature of Commercial Ice Production & Sanitation Compliance
In the commercial food and beverage sector of Milton, Georgia, edible ice is not merely an optional drink garnish; under United States Food and Drug Administration (FDA) Food Code Section 3-501.16 and Georgia Department of Public Health environmental standards, ice is formally regulated as a perishable food commodity. Maintaining strict food temperatures below the critical 41°F (5°C) threshold requires an uninterrupted, clean supply of ice for seafood display beds, cold salad holding tables, wine presentation buckets, and customer beverage hydration wells. When an automated Scotsman nugget ice machine abruptly halts production because of a false bin sensor lockout, hospitality establishments face immediate compliance violations, catastrophic food spoilage risks, and thousands of dollars in lost dining revenue during busy Friday evening services. Utilizing professional commercial appliance repair services ensures your refrigeration infrastructure satisfies stringent local health department inspection criteria while preventing revenue loss.
Commercial ice machine technology diverges dramatically between batch-type cubers and continuous-harvest nugget or flake makers. Traditional cubers freeze water across a vertical grid plate before initiating an energy-intensive hot-gas defrost cycle that drops a sheet of ice onto a mechanical curtain. In contrast, commercial Scotsman nugget ice machines (commonly producing popular chewable “Sonic-style” nugget ice) operate on an unbroken, continuous refrigeration thermodynamic cycle. Water enters a constant-level float reservoir and feeds by gravity into the bottom of a heavily insulated vertical cylindrical evaporator barrel. The outer perimeter of this stainless steel evaporator barrel is tightly wrapped with copper refrigeration tubing carrying low-temperature R-404A or hydrocarbon R-290 refrigerant boiling at approximately 28 to 32 psig, generating a continuous internal surface temperature between 0°F and 5°F.
Inside this freezing cylinder, an precision-machined, spiral stainless steel auger rotates continuously at approximately 9.5 to 11.5 revolutions per minute, driven by a heavy-duty permanent split capacitor gearmotor. As water contacts the frozen cylindrical wall, microscopic ice crystals instantly freeze. The rotating auger’s sharp flights scrape these crystals from the barrel wall and continuously propel the freezing slush upward. At the top of the cylinder, the slush enters a conical brass or stainless steel extrusion head. Under tremendous radial pressure—frequently exceeding 400 inch-pounds of mechanical torque—the slush is compressed through tapered extrusion passages, squeezing out excess liquid water before emerging as dense, compressed ice columns. A rotating breaker blade mounted atop the auger shaft fractures these extruded columns into uniform, bite-sized cylindrical nuggets that tumble by gravity down a plastic harvest discharge chute and into the insulated storage bin. Facility managers experiencing sudden mechanical binding or temperature fluctuations frequently turn to commercial refrigeration service specialists who understand the complex electromechanical relationship between the evaporator refrigeration loop and electronic bin monitoring telemetry.
Because nugget ice production is a continuous, perpetual extrusion process rather than a timed batch harvest, the electronic bin level control system functions as the primary safety gatekeeper for the entire mechanical assembly. In Scotsman Prodigy Plus platforms, this monitoring is achieved using dual infrared optical sensors positioned across the throat of the ice discharge chute. When the storage bin fills to maximum capacity, falling nuggets back up inside the chute, physically breaking the line-of-sight infrared beam between the photoelectric transmitter and phototransistor receiver. When this beam remains interrupted for 20 to 30 continuous seconds, the AutoAlert controller registers that the bin is full, shuts off the liquid line solenoid, stops the auger gearmotor, and puts the compressor into a controlled pump-down shutdown.
The operational catastrophe occurs when this optical sensor array falsely detects an obstruction when the ice storage bin is completely empty. Whether due to calcium carbonate calcification, airborne biological yeast biofilm, or electrical harness corrosion, the controller board believes the machine is full of ice. The front status panel illuminates the yellow “Bin Full” light, the diagnostic display shows code b, and the entire ice-making assembly remains locked in standby. For busy commercial facilities in Milton, GA—from equestrian clubhouses along Birmingham Highway to Crabapple eateries and Hopewell Road sports clinics—this silent lockout leads to immediate ice starvation. Resolving the fault requires deep diagnostic analysis of the optical beam voltage drops, control logic relays, and harvest chute mechanics.
Operational Symptoms & Scotsman AutoAlert Diagnostic Status Codes
Accurately interpreting the diagnostic indicators on modern Scotsman commercial ice makers is the first step toward effective troubleshooting. Scotsman Prodigy Plus modular nugget and flaker units (including models N0422, N0622, N0922, and NS0422) feature two distinct communication interfaces: the external AutoAlert indicator light panel visible on the front composite panel, and an internal 7-segment digital diagnostic LED display mounted directly to the central microprocessor printed circuit board. When kitchen managers observe erratic behavior, engaging emergency commercial appliance repair technicians provides immediate relief before inventory spoils.
The most telling symptom of a stuck bin sensor is the solid illumination of the amber or yellow “Bin Full” indicator lamp while the interior bin chamber is noticeably devoid of ice. Under ordinary operational circumstances, as ice is scooped out of the bin and the discharge chute clears, the AutoAlert controller senses light re-transmission across the photoelectric receiver. After an internal debounce verification delay of 20 to 30 seconds, the bin full lamp extinguishes, the water inlet valve opens, and the auger drive gearmotor immediately spins up, followed shortly by the refrigeration compressor contactor closing. In a stuck sensor scenario, this transition never occurs. The bin full light remains statically lit 24 hours a day.
Removing the front maintenance panel reveals the internal electronic brain of the Scotsman Prodigy Plus machine. On the control module, a bright green alphanumeric LED communicates real-time machine status. Under a stuck bin sensor failure mode, this screen continuously displays a lowercase letter b. It is vital to note that code b is technically classified as an operational state code rather than a permanent error lockout. Consequently, pressing the manual “ON/OFF” or “RESET” buttons on the panel will not clear the display; as long as the electronic logic circuits detect zero infrared light reaching the receiver phototransistor (or open continuity across curtain switch pins), the microprocessor immediately re-asserts code b within milliseconds of rebooting.
Another common symptom observed in commercial field diagnostics is rapid, erratic short-cycling accompanied by a blinking bin full indicator, as detailed in our Scotsman bin sensor blinking indicator guide. This condition typically occurs when mineral scale or translucent yeast slime has partially coated the sensor lenses. As water droplets splash down the chute or condensation beads form, the refracted infrared beam flickers between acceptable and blocked thresholds. The machine may run for 45 seconds, extrude a small handful of soft nuggets, suddenly shut down into code b for three minutes, and then attempt to restart. This rapid short-cycling causes extreme electrical stress on the compressor start capacitor and potential relay, eventually leading to compressor thermal overload tripping.
In older Scotsman or undercounter units—such as the Scotsman CU50, UN1520, or residential-commercial crossover models covered in our Scotsman residential and undercounter models guide—bin control relies on a vapor-charged capillary bulb thermostat positioned near the top of the ice bin. Symptoms of a failed bin thermostat include a completely dead refrigeration circuit, despite normal water reservoir levels and active circulation pump hum. If the mechanical contacts inside this thermostat corrode or the capillary charge leaks out, the internal switch remains permanently open, perfectly mimicking a perpetually full bin.
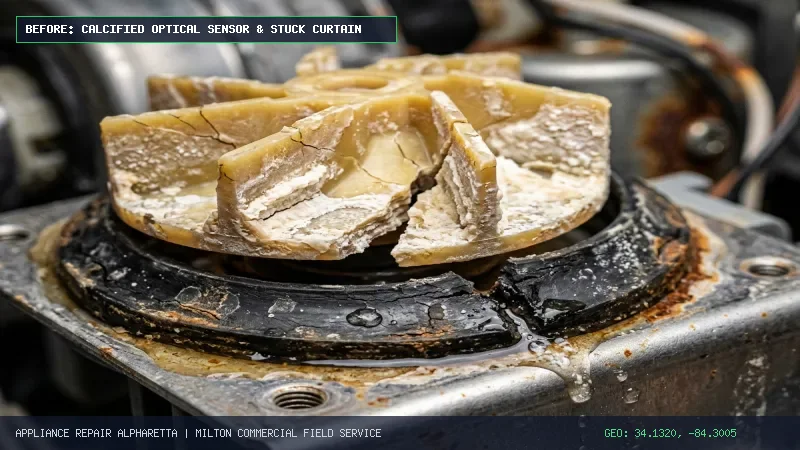
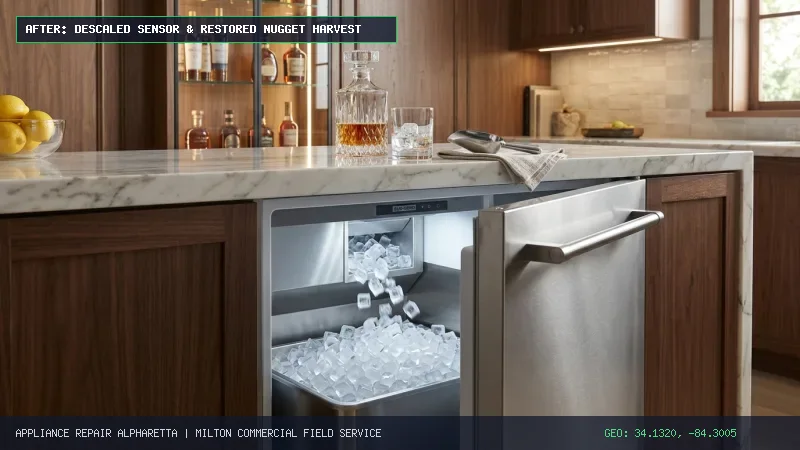
Visual Before & After Macro Pair: Calcified Sensor Aperture vs. Descaled Optical Assembly
The optical infrared bin sensing array on Scotsman Prodigy Plus machines operates on precision photoelectric physics. An infrared light-emitting diode (LED) transmits an invisible beam of light across an air gap of approximately 3.5 to 5.0 inches directly toward a silicon NPN phototransistor receiver. When this optical path is uninterrupted, photons saturate the base of the phototransistor, allowing current to flow to ground and maintaining a high logic voltage signal (4.2VDC to 4.9VDC) across the controller’s input terminals. However, operating within the saturated, 100% relative humidity environment of an ice harvest chute leaves these delicate lenses exposed to heavy airborne and waterborne contamination.
Macro Inspection: Scotsman Prodigy Plus Optical Sensor Decontamination
Six Primary Causes of False Bin Full Lockouts in Scotsman Nugget Makers
In the commercial kitchens of Milton, GA, a stuck Scotsman bin sensor rarely stems from a random software glitch. It is almost invariably caused by specific environmental, physical, or electrochemical failure modes that disrupt the sensing loop. When unexpected ice maker shutoffs halt facility operations, contacting a technician for same-day commercial repair prevents unnecessary downtime and preserves business continuity. Below are the six most common causes discovered during field service calls across Milton, GA:
1. Calcium Carbonate & Mineral Scale Occlusion on Photoelectric Emitter / Receiver Prisms
Municipal water supplies in North Fulton County, sourced from local water treatment plants and supplemented by deep private groundwater wells across rural Milton estates, carry moderate levels of dissolved calcium and magnesium carbonates. In nugget ice machines, water continuously freezes along the evaporator barrel while minerals remain concentrated in the residual water film. As ice nuggets are sheared by the breaker head and extruded into the discharge chute, fine microscopic droplets of mineral-saturated water atomize into the air. These droplets strike the heated surfaces of the infrared emitter and receiver lenses. As the water evaporates, microscopic crystals of calcite and aragonite form hard, opaque mineral rings. Over weeks of operation, this mineral crust thickens until infrared light can no longer penetrate the prism face. The phototransistor receiver starves of light, its signal return voltage plunges to ground, and the controller locks into a continuous code b shutdown.
2. Slime, Biofilm & Airborne Yeast Bio-Accumulation
Commercial kitchens operating pizza proofing cabinets, bread ovens, craft beer tap towers, or kombucha dispensers maintain high concentrations of airborne yeast cells and carbohydrate aerosols. The high-volume air-cooled condenser fan on a Scotsman ice machine pulls thousands of cubic feet of kitchen air through the chassis every hour. These fungal spores readily colonize the warm, perpetually damp surfaces of the ice discharge chute. Fungi and slime-producing bacteria secrete an extracellular polysaccharide matrix (biofilm) that creates a dense, gelatinous pink or brownish coating over the optical sensor eyes. Because this biofilm possesses high optical density and light-scattering properties, it completely attenuates the infrared wavelength, tricking the controller into registering a permanently blocked ice chute even when the storage bin is bone dry.
3. Mechanical Bin Curtain Switch Misalignment & Magnetic Reed Switch Failure
On select Scotsman commercial platforms, including cubers and hybrid modular units, bin level monitoring is governed by a physical plastic curtain suspended on molded pivot hinges directly across the evaporator face. As ice drops during harvest, it pushes the curtain open. A neodymium permanent magnet sealed inside the lower corner of the plastic curtain moves away from a hermetically sealed magnetic reed switch mounted inside the side chassis wall, opening the electrical circuit. Once the ice clears, gravity swings the curtain shut, closing the reed switch contacts (0.0Ω continuity). If mineral deposits cake the hinge pins, if physical ice chunks wedge the baffle open 1/8th of an inch, or if thousands of mechanical cycles cause the internal glass reed switch contacts to fatigue or weld open, the controller senses the curtain as permanently tilted, triggering continuous code b standby.
4. Infrared Optical Bin Sensor Harness Degradation & DC Signal Voltage Loss
The low-voltage wiring harness that connects the optical sensor bracket to the main Prodigy Plus controller operates on a sensitive 5VDC logic reference circuit. In harsh restaurant environments, high humidity combined with chlorine sanitizing vapors corrodes the female molex pin terminals at connector J6. Furthermore, the intense mechanical vibration generated by the auger drive transmission over years of operation can cause copper strand fatigue inside the wiring sheath. A resistance increase of just 15 ohms across the ground return circuit produces a substantial voltage drop, pulling the phototransistor’s sensing output below the digital comparator’s switching threshold. To the microprocessor, this electrical signal degradation is indistinguishable from a physical mass of ice blocking the chute.
5. Ice Bridging, Chute Splay & Nugget Compaction Obstructing the Sensor Aperture
Chewable nugget ice contains significantly more liquid water within its porous structure than dense, sub-cooled cube ice (typically 15% to 25% liquid moisture by mass). Consequently, nugget ice has a high thermodynamic propensity to fuse together if bin temperatures rise slightly or bin drainage is impeded. If kitchen staff leave an ice scoop propped upright beneath the discharge opening, or if a worn bin door magnetic gasket allows ambient 78°F kitchen air to infiltrate the storage cavity, the bottom layers of descending nuggets melt slightly and refreeze into a hard, cohesive ice bridge. This ice arch sits directly within the optical beam path across the chute collar. Even though the lower storage bin may be completely empty, the physical presence of jammed ice in the chute creates an authentic optical interruption that prevents harvest resumption.
6. Defective Scotsman Prodigy Plus Main Electronic Controller Board
The central printed circuit board on Scotsman Prodigy Plus ice machines (OEM Part No. 12-3124-01) utilizes surface-mount optical comparator integrated circuits to interpret low-voltage sensor telemetry. Electrical power transients, lightning strikes common during Georgia summer thunderstorms, or phase voltage unbalances can degrade these sensitive semiconductors. If an on-board comparator chip shorts to ground or a logic pull-up resistor burns open, the microprocessor permanently registers a blocked sensor input regardless of field conditions. Even disconnecting the sensor harness entirely will not clear the fault; the damaged board remains frozen in code b. Facility managers require specialized advanced diagnostic service to isolate electronic board component failures from field sensor wiring faults.
Step-by-Step Safe Facility Troubleshooting Protocols for Kitchen Staff
Before dispatching an emergency technician, kitchen managers and facilities maintenance staff can perform seven non-invasive, safe troubleshooting steps derived from our Scotsman ice machine diagnostics protocols. Executing a regular preventive maintenance routine ensures commercial kitchen equipment operates efficiently:
- Step 1: Inspect Exterior AutoAlert Status Lights: Examine the front diagnostic display on the machine casing. Note whether the “Bin Full” indicator lamp is glowing steady amber/yellow or blinking intermittently. A steady light indicates an uninterrupted blocked-beam condition, whereas a blinking lamp points toward electrical noise, harness contact fluttering, or translucent biological slime allowing partial light transmission.
-
Step 2: Remove the Front Maintenance Panel & Verify Controller Code: Loosen the two front captive screws and lift the front stainless steel or composite maintenance panel off the chassis. Locate the 7-segment green LED display on the main control module. Confirm whether it displays lowercase code
b, code0(standby), or an alternating error code such as1(long freeze cycle) or2(long harvest). - Step 3: Perform Safe High-Voltage Electrical Isolation: Locate the dedicated electrical breaker serving the ice maker in your facility’s power distribution panel (typically a 20A or 30A 115V or 208/230V breaker) and switch it off. Confirm high-voltage power is de-energized before reaching near the harvest chute or auger housing to eliminate electrical shock or accidental motor startup hazards.
- Step 4: Clear Physical Ice Compaction in the Harvest Chute: Open the ice storage bin door and look upward into the ice drop chute throat. Using a sanitized plastic spatula or non-scratch implement, inspect for compacted nugget ice, fused ice bridges, or slush clumps hanging directly across the sensor collar. Carefully dislodge any compacted ice, allowing it to drop freely into the storage bin. Never use ice picks, knives, or metal scrapers that can puncture plastic chute walls or gouge optical lenses.
- Step 5: Perform Optical Sensor Lens Decontamination: Locate the circular optical lenses mounted on opposite sides of the black plastic chute collar. Dip a clean, lint-free microfiber cloth or medical cotton swab in a warm solution of Scotsman Clear 1 Nickel-Safe Cleaner (or food-grade white vinegar). Gently rub both optical prism faces in a circular motion to dissolve calcium carbonate scale and pink yeast film. Follow with a clean water-dampened swab to remove chemical residue, and dry thoroughly with a dry swab to eliminate light-refracting water beads.
- Step 6: Verify Mechanical Curtain Swing Freedom (If Equipped): On units utilizing a physical ice deflector curtain, gently push the curtain inward by hand. Confirm that it pivots freely on its top molded hinge pins without binding or dragging against the side walls. Release the curtain; it must fall shut completely by gravity, seating flush against the chassis stops. Descale any mineral crust accumulation around the hinge pivot sockets.
-
Step 7: Re-Energize Power & Monitor Controller Debounce Cycle: Re-install the front maintenance panel and switch the electrical breaker back on. Press the manual “ON/OFF” button once. Observe the 7-segment digital display. The controller will initiate a 20-to-30-second debounce verification cycle. If the optical beam is clear, code
bwill clear, the display will switch toF(freezing) orr(ready), and the auger drive motor will hum into operation. If codebre-appears immediately with an empty chute, a deeper electrical harness or electronic board component failure exists.
When to Halt In-House Troubleshooting: High Voltage, Mechanical, and EPA Regulations
While basic visual inspection and exterior lens cleaning are safe for kitchen employees, deeper operational faults affecting cooling cycles—such as those explored in our refrigeration cooling system failures handbook—carry severe life-safety, mechanical, and regulatory legal hazards. In-house troubleshooting must halt immediately when the following professional boundaries are reached:
- OSHA & NFPA 70E High Voltage Arc Flash Hazards: Commercial Scotsman modular ice makers in Milton operate on dedicated 208/230V single-phase or 3-phase high-voltage power feeds. Testing live electrical terminal blocks, compressor contactor coils, dual capacitor start relays, and control transformer primaries presents life-threatening shock and electrical arc flash risks. Only licensed technicians equipped with NFPA 70E compliant personal protective equipment (PPE) and CAT-III 600V rated multimeters should access open electrical junction boxes.
- Auger Gearmotor High-Torque Mechanical Crush Hazard: The internal transmission gearbox in a commercial nugget machine produces extreme rotational torque (often exceeding 400 inch-pounds) to force dense ice through the stainless extrusion dies. Inserting fingers, screwdrivers, or wire brushes near the extrusion head while the machine is energized can result in catastrophic crushing or amputation injuries.
- EPA Section 608 Clean Air Act Compliance: Commercial ice machines utilize closed refrigeration circuits pressurized with fluorocarbon or hydrocarbon refrigerants (such as R-404A, R-448A, R-449A, or flammable R-290). Piercing process tubes, connecting refrigeration service manifold gauges, or servicing expansion valves requires Universal EPA Section 608 Certification. Unlicensed venting of refrigerants is a direct violation of federal law carrying penalties exceeding $44,000 per day per violation.
Commercial Financial Decision Matrix: Repairing vs. Replacing Your Ice Machine
When facing a major Scotsman ice machine malfunction, Milton business owners must weigh the cost of repairs against the capital investment of a full equipment replacement, keeping in mind standard commercial refrigeration maintenance benchmarks. Commercial Scotsman modular nugget machines have an anticipated operational lifespan of 7 to 10 years depending on water filtration quality and preventative maintenance frequency. Use the following financial decision matrix to guide your facility planning:
| Diagnostic Condition | Equipment Age | Est. Repair Cost | Est. Replacement | Recommended Action |
|---|---|---|---|---|
| Optical Bin Sensor Descale & Recalibration | Any Age (1–10 Yrs) | $165 – $285 | $5,800 – $9,500 | 100% Immediate Repair (Fast ROI) |
| OEM Optical Sensor Kit Replacement (A39030-021) | 1 – 7 Years | $320 – $485 | $5,800 – $9,500 | Immediate Repair Recommended |
| Prodigy Plus Main Controller Board Replacement | 1 – 6 Years | $680 – $995 | $5,800 – $9,500 | Repair if Gearmotor & Barrel Sound |
| Auger Gearmotor Overhaul & Water Seal Rebuild | 6 – 8 Years | $1,450 – $2,200 | $5,800 – $9,500 | Evaluate Overall Barrel Wear |
| Scored Evaporator Barrel + Hermetic Compressor Burnout | 8+ Years | $3,600 – $4,800 | $5,800 – $9,500 | Full Replacement Recommended |
Interactive Instant Repair Cost Estimator for Scotsman Ice Machines
Use our dynamic pricing widget below to generate an immediate cost estimate for your commercial Scotsman ice machine repair based on your equipment architecture and diagnostic scope:
Estimated Commercial Repair Cost Factors Breakdown in North Fulton County
Commercial refrigeration repairs represent a significant operational expense for Milton hospitality venues. Discovering why an ice machine stops making ice requires transparent pricing so facility managers can budget accurately. Repair quotes are influenced by four principal cost elements:
- Factory OEM Replacement Component Costs: Scotsman genuine factory parts are precision-engineered to meet stringent tolerances. OEM bin level optical sensor kits (A39030-021) typically range from $140 to $220. Electronic AutoAlert Prodigy Plus microprocessor control boards (12-3124-01) cost between $420 and $680. Mechanical magnetic curtain reed switch assemblies average $85 to $150.
- Specialized Commercial Labor Rates: Commercial refrigeration labor across Milton, Alpharetta, and Roswell reflects specialized trade expertise. Certified refrigeration technicians carry EPA Section 608 Universal licenses and NFPA 70E electrical certifications. Standard commercial field rates range between $135 and $195 per hour, with diagnostic service fees ($95 to $145) generally credited toward approved repairs.
- Deep Sanitation & Chemical Descaling Procedures: If a false bin full error is caused by severe calcium carbonate calcification or bio-slime buildup, clearing the optical lenses is only a temporary fix. Complete system decontamination requires circulating Scotsman Clear 1 nickel-safe acid cleaner through the water distributor and evaporator barrel, flushing the reservoir, and sanitizing with EPA-registered food contact sanitizer, adding $120 to $220 to service totals.
- Emergency Dispatch Windows: During high-volume weekend dining shifts, evening bar rushes, or holiday catering events, facilities require immediate response. Emergency same-day red-alert dispatches (under 60 minutes) or weekend calls include an emergency surcharge ($75 to $120) to guarantee immediate commercial van routing.
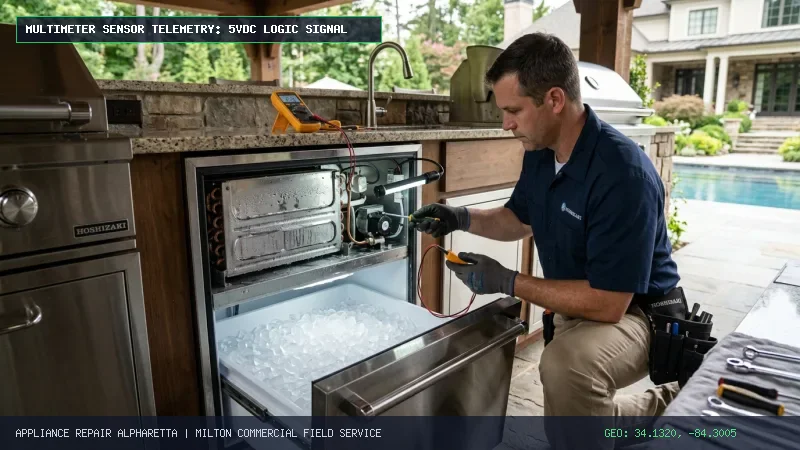
How Professionals Diagnose: Multimeter, DC Voltage & Optical Telemetry Lookup Table
Certified technicians follow strict diagnostic protocols when analyzing a Scotsman machine locked in code b or suffering from nugget ice auger squeaking and mechanical binding. Instead of guessing or replacing parts unnecessarily, technicians take precise multimeter measurements of the low-voltage DC logic circuit, sensor phototransistor resistance, and mechanical switch continuity. Refer to the interactive telemetry lookup table below to verify electrical values:
| Test Point / Terminal | Component Tested | Expected Normal Reading | Failure / Out-of-Spec Reading | Diagnostic Conclusion |
|---|---|---|---|---|
| J6 Connector Pin 1 to 2 | Optical Emitter Supply Voltage | 4.80 – 5.15 VDC | 0 VDC or < 4.2 VDC | Controller board 5V logic rail failure or harness short |
| J6 Connector Pin 3 to 4 | Phototransistor Receiver (Beam Clear) | 4.20 – 4.90 VDC | < 0.8 VDC (With Chute Empty) | Severe calcification on lenses or failed receiver eye |
| J6 Connector Pin 3 to 4 | Phototransistor Receiver (Beam Blocked) | < 0.70 VDC (Beam Obstructed) | > 2.5 VDC (With Chute Blocked) | Optical receiver eye shorted internally; won’t sense ice |
| Curtain Switch Terminals | Magnetic Reed Switch (Curtain Closed) | 0.00 – 0.20 Ω (Continuity) | Infinite (O.L.) with curtain shut | Defective reed switch, demagnetized curtain, or stuck hinge |
| Curtain Switch Terminals | Magnetic Reed Switch (Curtain Tilted) | Infinite Resistance (O.L.) | 0.00 Ω (Stuck Closed) | Welded reed contacts; failure to sense full bin overflow |
| Auger Motor Winding Lead 1-2 | Gearmotor Stator Winding Resistance | 6.8 – 8.5 Ω (At 77°F) | 0.0 Ω (Short) or O.L. (Open) | Burned motor winding or tripped internal thermal protector |
| Water Level Probe Pins | Acoustic / Conductivity Water Sensor | 2.4 – 3.1 VDC (Submerged) | 0 VDC or constant 5.0 VDC | Calcified water level probe causing dry-run lockout |
tr[i].style.display = “none”;
Critical Genuine OEM Scotsman Replacement Parts Involved in Sensor Repairs
When repairing commercial Scotsman ice systems or comparing them against other leading brands such as our Hoshizaki commercial repair services, installing genuine original equipment manufacturer (OEM) replacement components is non-negotiable. Generic aftermarket sensors frequently exhibit improper optical focal lengths, inadequate moisture sealing, or incorrect resistor tolerances that cause false-positive error codes. Certified technicians stock the following genuine Scotsman parts:
- Scotsman A39030-021 Bin Level Optical Sensor Kit: Contains matching matched-pair infrared photoelectric transmitter and receiver eye assemblies, moisture-sealed wiring pigtail, molded silicone mounting grommets, and snap-lock harness connectors. Engineered specifically for Scotsman Prodigy Plus nugget, flaker, and cuber chassis.
- Scotsman 11-0619-21 Magnetic Curtain Switch Assembly: Includes the sealed magnetic reed switch sensor and weather-pack electrical leads designed to mount inside the evaporator side panel. Replaces damaged or heat-fatigued curtain sensors on cuber models.
- Scotsman 02-4299-01 Ice Deflector & Drop Chute Curtain: Molded from heavy-duty NSF-certified food-grade polypropylene with encapsulated permanent rare-earth magnets. Eliminates curtain binding, hinge cracking, and mineral warp.
- Scotsman 12-3124-01 Prodigy Plus Master Electronic Controller Board: The central logic module featuring the integrated AutoAlert status engine, dual 7-segment LED diagnostic display, 5VDC regulated logic power supply, and multi-pin sensor headers.
- Scotsman 11-0540-21 Bin Thermostat Control: Adjustable mechanical capillary bulb thermostat utilized in undercounter nugget units (such as the Scotsman CU50 and Brilliance models) to cycle refrigeration based on direct ice contact temperature.
- Scotsman 02-3866-02 Water Level Sensor Probe: Triple-pin conductivity and temperature probe mounted within the float reservoir to monitor supply water continuity and prevent dry freeze cycles.
Facility Preventative Maintenance Schedules to Prevent Future Lockouts
Commercial ice machine breakdowns can be prevented with structured preventative maintenance protocols similar to standard Manitowoc commercial harvest care. Establishing disciplined maintenance cycles protects mechanical assemblies and preserves hygiene compliance across your facility:
Recommended Commercial Maintenance Intervals
- Daily Facility Protocols: Visually confirm ice is actively dropping from the chute. Sanitize the exterior bin door handle and ice scoop. Ensure ice scoop is stored in a dedicated sanitized wall holster, never left resting inside the bin.
- Bi-Weekly Inspection: Inspect the air-cooled condenser filter on the front panel. Vacuum away accumulated lint, dust, and kitchen grease. Restricted condenser airflow elevates head pressures, accelerating mineral deposition inside the ice chute.
- Monthly Optical Swab: Power down the machine. Using a cotton swab saturated with diluted nickel-safe descaler, wipe the optical bin sensor lenses to eliminate embryonic mineral rings and yeast film before beam obstruction occurs.
- Quarterly Water Filter Replacement: Replace primary and secondary sediment and activated carbon filter cartridges. In Milton facilities with heavy water mineral hardness, install a phosphate scale inhibitor feeder to chemically sequester calcium ions.
- Semi-Annual Professional Overhaul: Schedule a comprehensive commercial field service visit. Certified technicians disassemble the ice chute, perform complete descaling and sanitation cycles, test auger gearbox amp draw, verify gearmotor bearing play, measure refrigeration suction and discharge pressures, and inspect electrical terminal torques.
Commercial Facility Health, Electrical, and Chemical Safety Guidelines
Handling commercial ice machines involves high voltage, mechanical torque, acidic descaling chemicals, and food safety standards across our local appliance repair in Milton, GA service territory. Adhere strictly to the following safety protocols:
- OSHA Lockout / Tagout (LOTO) Compliance: Prior to opening any internal service cabinet panels, technicians and maintenance engineers must lock and tag out the electrical breaker or disconnect switch. Never rely on the front panel “OFF” switch, as high voltage remains present across the line side of the contactor and control board transformer.
- Chemical Handling PPE: Scotsman Clear 1 and commercial phosphoric acid descalers cause severe chemical burns to skin and eyes. Technicians and kitchen staff must wear chemical splash goggles, nitrile gloves, and an apron during mixing and flushing. Never mix acid descalers with chlorine bleach sanitizers, as this reaction releases toxic chloramine gas.
- Food Contact Sanitation Standards: All brushes, cloths, and solutions introduced into the ice storage bin or harvest chute must be certified food-grade and thoroughly rinsed. Discard the first three full harvests of ice following any chemical descaling or repair service to ensure zero chemical carryover into customer beverages.
- Physical Drain Air Gap Integrity: Federal and state plumbing codes mandate that ice machine bin drain lines terminate with a minimum 1-inch physical air gap above the rim of the floor sink. Never connect an ice bin drain directly into a sanitary sewer line, as a sewer backup would siphon sewage directly into the edible ice storage chamber.
Frequently Asked Questions Regarding Scotsman Ice Machine Bin Controls
Browse our technical archive of the sixteen most common questions regarding commercial Scotsman nugget ice machine bin sensors, error codes, and maintenance protocols developed by our appliance repair in Alpharetta, GA commercial response division:
What does diagnostic code “b” mean on a Scotsman Prodigy Plus ice machine?
How do I clean the optical bin level sensors on my Scotsman nugget ice maker?
Why does my Scotsman ice machine keep shutting off when the bin is only half full?
Can I bypass the bin sensor on my Scotsman ice maker temporarily to make ice?
What is the difference between Scotsman optical bin sensors and curtain switches?
How does a technician test a Scotsman optical bin sensor with a multimeter?
What causes nugget ice to back up and freeze inside the discharge chute?
How often should a commercial Scotsman ice machine be descaled in Milton, GA?
What is the part number for the Scotsman Prodigy Plus optical bin sensor kit?
Why does my Scotsman ice maker show a blinking bin full light instead of solid?
Can hard water mineral scale permanently damage Scotsman optical sensors?
How long does a Scotsman commercial ice machine take to restart after cleaning the bin sensor?
What chemical cleaner is approved for cleaning Scotsman ice machine water circuits?
How does ambient kitchen temperature affect Scotsman nugget ice machine harvest?
Can a failed water level float switch mimic a stuck bin sensor?
b. A water supply failure or failed float sensor displays code 0 or 1 on the controller and illuminates the “Water” indicator light amber or red on the front panel. However, if a water level float probe calcifies and shorts to ground while the bin sensor has an unstable harness connection, multiple alternating codes can confuse kitchen staff.
How do I schedule same-day emergency commercial ice machine service in Milton?
Commercial Technical Resources, Regional Coverage & Brand Silos
Explore our network of certified commercial appliance repair resources across North Fulton County:
Specialized Services
Related Ice Machine Guides
Commercial Brand Hubs
Key Technical Takeaways for Milton Facility Engineers
- Diagnostic Code “b” Meaning: Indicates the electronic controller senses an interrupted infrared beam or open curtain switch, halting the drive auger and compressor to prevent mechanical jamming.
- Mineral Scale Vulnerability: North Fulton County water hardness causes calcium carbonate deposition across optical prisms, dropping signal voltage below the 0.8VDC threshold.
- Airborne Yeast Hazards: Kitchens near pizza ovens or draft beer taps experience rapid biological biofilm formation over optical lenses, requiring regular antimicrobial cleansing.
- DC Telemetry Testing: Technicians verify 4.8–5.15VDC supply on J6 Pins 1-2 and 4.2–4.9VDC unblocked signal return on Pins 3-4 to confirm sensor circuit integrity.
- Bypass Hazards: Never jumper or bypass a nugget ice machine bin sensor; ice extrusion back-up will bend auger shafts and destroy transmission gearboxes.
- Approved Chemicals Only: Descale exclusively using Scotsman Clear 1 or nickel-safe citric acid; harsh mineral acids destroy stainless steel and nickel evaporator plating.
- Genuine OEM Assemblies: Replace deteriorated optical arrays exclusively with genuine Scotsman A39030-021 sensor kits to preserve precise optical focal geometries.
- High Voltage Safety: Halting in-house troubleshooting is mandatory when testing 208/230V live circuits or opening refrigerant sealed loops governed by EPA Section 608 regulations.
Need Certified Appliance Repair Today?
Skip the phone line — book direct local priority dispatch across Alpharetta, Milton, Roswell & Johns Creek.