
When a heavy-duty Traulsen commercial reach-in freezer suffers a stuck hot gas defrost solenoid valve within the high-volume culinary operations of Milton equestrian estates, private golf clubhouses, and upscale banquet venues, the kitchen faces an immediate thermal and operational crisis. Prestigious country club kitchens along Birmingham Highway, Hopewell Road, Freemanville Road, and the Crabapple historic corridor rely on Traulsen G-Series, R-Series, and Centerline commercial refrigeration to preserve thousands of pounds of prime wagyu beef, delicate seafood shipments, house-made pastry foundations, and catered banquet inventory at sub-zero temperatures. Unlike conventional commercial freezers that utilize slower electric resistance calrod elements, high-performance Traulsen reach-in freezers employ an engineered hot gas bypass defrost circuit to clear evaporator ice rapidly using high-pressure discharge refrigerant. When the electromagnetic hot gas defrost solenoid valve seizes mechanically in an open or closed position, or its magnetic coil suffers electrical breakdown, the refrigeration cycle collapses. The freezer either blows blazing 180°F discharge gas continuously into the cabinet or allows frost to accumulate into an impenetrable glacial block across the evaporator fin pack. Our EPA Universal-certified, factory-trained master technicians provide dedicated same-day commercial emergency repair throughout Milton and North Fulton County, equipped with genuine OEM Traulsen parts, true-RMS digital multimeters, digital manifold gauges, and mobile nitrogen recovery apparatus. For immediate technical dispatch to your Milton country club or commercial kitchen, call our priority service line directly at (770) 796-7742.
Quick Answer: Diagnosing a Stuck Traulsen Hot Gas Defrost Solenoid Valve
Quick Answer: A Traulsen commercial reach-in freezer hot gas defrost solenoid valve fails in two primary modes: stuck OPEN or stuck CLOSED. A valve stuck open constantly dumps 180°F–200°F compressor discharge gas into the evaporator, preventing refrigeration, driving suction pressure up to 60–75 PSI, and heating the cabinet to 40°F–70°F. A valve stuck closed blocks hot gas during defrost, causing the evaporator coil to choke in solid ice while cabinet airflow ceases. Diagnosis requires verifying 24VAC across the solenoid coil (normal coil resistance: 22–30 Ω), inspecting the electronic controller relay (115VAC output), confirming a 65 PSI suction pressure differential, and testing the 10kΩ NTC defrost termination thermistor. Contact our Milton master commercial refrigeration technicians at (770) 796-7742 for immediate OEM valve rebuilding and sealed system restoration.
Listen to 60-Second Commercial Refrigeration Diagnostic Brief
Narrated by Jason J. (Master Certified Commercial Refrigeration Specialist)
Check Same-Day Commercial Tech Availability in Milton & North Fulton
Verified Local Service • Milton GA
Traulsen G-Series G22010 Two-Section Commercial Reach-In Freezer Hot Gas Solenoid Rebuild
Location: Private Country Club Clubhouse on Hopewell Road, Milton, GA • Replaced Seized Pilot Plunger & Burnt 24VAC Solenoid Coil • ★★★★★ Verified Executive Chef Client
Verified Commercial Field Case Study • Milton Equestrian Corridor
Corridor: Birmingham Hwy & Hopewell Rd • Completed in 2.2 Hours
Case Study: Restoring a Stuck Hot Gas Bypass Defrost Solenoid on a Traulsen G-Series Reach-In Freezer in an Elite Milton Clubhouse
Prestigious equestrian estate country club on Birmingham Highway, Milton, GA. Two-section Traulsen G22010 reach-in freezer holding $28,000 of aged prime steaks, wagyu loins, and imported pastry inventory for weekend tournament dinner.
Traulsen Smart Control flashing HI TEMP alarm at +48°F. Compressor running continuously without cycling. Suction line warm to the touch. Kitchen staff suspected complete compressor death or catastrophic refrigerant leak.
True-RMS digital multimeter measured 0V across solenoid coil, yet hot gas line measured 188°F entering evaporator inlet. Digital manifold gauges revealed suction pressure stuck at 68 PSI (design: 4 PSI). Solenoid valve mechanically stuck 40% open due to carbonized oil debris.
Recovered R-404A charge into DOT cylinder. Disassembled solenoid brass valve body, cleared sludge, installed genuine Traulsen OEM valve rebuild kit (Part #325-60098-00) with new stainless plunger and PTFE seat, replaced 24VAC magnetic coil (26.4 Ω), deep evacuated to 240 microns, recharged factory charge (21 oz). Cabinet pulled down to -5°F within 48 minutes.
Book Emergency Commercial Service →
Table of Contents: Traulsen Commercial Freezer Hot Gas Defrost Solenoid Guide
- Commercial Refrigeration Dynamics in Milton Country Club Kitchens
- Warning Signs of a Stuck Traulsen Hot Gas Defrost Solenoid Valve
- Visual Field Restoration: Before vs. After Hot Gas Defrost Solenoid Repair
- Mechanical and Electrical Causes Behind Hot Gas Defrost Solenoid Failure
- Step-by-Step Operator Diagnostics and Initial Inspection Protocol
- Critical Safety Boundaries: When Commercial Operators Must Stop DIY Action
- Repair vs. Replace Evaluation: Solenoid Rebuild vs. Complete Condensing Unit
- Instant Dynamic Commercial Freezer Repair Cost Estimator
- Commercial Freezer Defrost Repair Cost Drivers and Budget Factors
- How Certified Technicians Diagnose Traulsen Hot Gas Defrost Solenoids: Multimeter & Pressure Telemetry
- Essential Traulsen Commercial Freezer Defrost & Refrigeration Components
- Preventative Maintenance Protocols for Milton Commercial Kitchen Freezers
- Commercial High-Voltage and High-Pressure Refrigerant Safety Standards
- Frequently Asked Questions About Traulsen Hot Gas Defrost Solenoid Repairs
- Related Commercial & Residential Services
- Related Commercial Refrigeration Diagnostic Guides
- Commercial Brand Solutions We Support
- North Fulton Local Service Coverage Areas
- Summary & Key Takeaways for Commercial Kitchen Managers
- Emergency Commercial Freezer Repair Call-to-Action
Commercial Refrigeration Dynamics in Milton Country Club Kitchens
Throughout the pastoral landscapes and equestrian preserves of Milton, Georgia, private country club dining rooms, championship golf clubhouse bistros, and luxury equestrian estate kitchens maintain culinary standards comparable to Michelin-starred establishments. From the prestigious clubhouse kitchens surrounding Birmingham Highway, Freemanville Road, and Hopewell Road to historic dining venues in Crabapple, executive chefs manage rigorous banquet timelines, private gala catering, and daily fine-dining services. At the core of these high-volume culinary operations stands commercial refrigeration equipment engineered for unyielding reliability. Traulsen, a division of ITW Food Equipment Group, has reigned for nearly a century as the gold standard of commercial foodservice refrigeration, renowned for its indestructible stainless steel construction, ducted top-mounted airflow systems, and rapid-recovery refrigeration circuits. When executive chefs experience sudden equipment failure, our certified technicians deliver immediate commercial appliance repair across North Fulton County.
Unlike light-duty residential freezers or economy commercial cabinets that rely on simple electric resistance Calrod heaters embedded beneath aluminum evaporator fins, Traulsen premium reach-in freezers utilize an advanced hot gas defrost system. The thermodynamic physics of hot gas defrosting represent an engineering marvel. When an electric resistance defrost cycle initiates in a standard freezer, heating elements require 30 to 45 minutes to heat up, melt coil frost from the outside inward, and radiate heat outward throughout the cabinet. This sluggish cycle elevates cabinet air temperatures by 15°F to 25°F, subjecting stored frozen meats, seafood, and delicate par-baked pastries to destructive thermal micro-thawing. In contrast, Traulsen hot gas bypass technology routes high-temperature, superheated discharge refrigerant (typically exiting the compressor discharge port at 180°F to 215°F) directly into the interior passages of the evaporator tubing. By heating the coil from the inside out, the hot gas melts frost in just 5 to 10 minutes, minimizing internal cabinet temperature spikes, preserving food moisture, and slashing kitchen energy consumption. When walk-in or reach-in cooling fails, culinary directors trust our emergency emergency appliance repair team to preserve valuable inventory.
However, the remarkable efficiency of this thermodynamic bypass introduces mechanical complexity: the hot gas defrost solenoid valve. This electro-mechanical brass valve serves as the vital gatekeeper between the high-pressure discharge line and the low-pressure evaporator coil. During normal cooling mode, the valve must maintain a bubble-tight hermetic seal against 250 to 320 PSI of condensing discharge pressure. When the microprocessor initiates defrost, an electronic relay energizes a low-voltage magnetic coil, lifting a stainless steel internal plunger off its precision orifice to route scorching gas into the cooling coil. If mechanical wear, particulate contamination, burnt electrical windings, or coil plunger seizure occurs, this delicate balance collapses. Milton kitchen operators finding their commercial reach-in freezer blowing warm air or blanketed in ice can explore our specialized Milton, GA refrigeration support services.
Understanding the intricate electrical and refrigeration mechanics of Traulsen hot gas defrost solenoid valves is essential for commercial facility directors, executive chefs, and equipment maintenance managers. In this comprehensive technical guide, our EPA Universal-certified master technicians dissect every phase of hot gas bypass operation. We analyze the dual failure modes of stuck open and stuck closed solenoid valves, examine True-RMS multimeter testing procedures, break down refrigerant telemetry differentials, contrast OEM valve rebuilding versus condensing unit replacement, and provide preventative maintenance protocols tailored to the demanding country club kitchens of Milton, Georgia. For comprehensive estate kitchen refrigeration solutions, we also maintain dedicated Sub-Zero appliance repair diagnostic capabilities.
Warning Signs of a Stuck Traulsen Hot Gas Defrost Solenoid Valve
When a Traulsen commercial freezer hot gas defrost solenoid valve fails, the symptoms manifest distinctly depending on whether the valve has seized in the OPEN or CLOSED position. Because both failure modes compromise cabinet temperature regulation, kitchen staff must recognize the early physical and auditory indicators before thousands of dollars in frozen inventory perish. In high-traffic country club kitchens, these warning signs require immediate investigation and professional same-day appliance repair intervention:
Cabinet Warms to 40°F–60°F with Compressor Running (Stuck OPEN)
The most dramatic symptom of a valve stuck open is that the freezer acts as an oven. The compressor runs non-stop, but superheated 190°F discharge gas dumps continuously into the evaporator coil. The cabinet temperature climbs into the 40°F to 60°F range, melting ice cream and thawing meats while the condensing unit runs hot to the touch.
Evaporator Coil Encased in Solid Block Ice (Stuck CLOSED)
When the solenoid valve fails to open during scheduled defrost cycles, natural moisture introduced from frequent door openings cannot melt away. Frost accumulates into an impenetrable glacial block across the evaporator coil fins. Airflow from the evaporator fans halts completely, causing internal temperatures to creep above statutory storage limits.
Abnormally Elevated Suction Pressure (55 to 75 PSI)
During normal low-temperature operation on R-404A or R-448A refrigerant, suction pressure hovers between 2 and 6 PSI (-20°F to -15°F evaporating temperature). When the hot gas solenoid valve is stuck open or weeping internally, high-pressure gas bypasses the expansion valve, flooding the suction manifold and driving low-side pressure to 55–75 PSI.
Compressor Thermal Overload Tripping & HI TEMP Alarms
When superheated gas continuously floods back to the compressor housing without the liquid evaporative cooling effect of properly metering refrigerant, compressor motor winding temperatures skyrocket past 225°F. The compressor internal Klixon thermal protector trips open on overload, producing an ominous clicking sound every 3 to 5 minutes while the Traulsen microprocessor emits loud HI TEMP alarm beeps.
When commercial kitchen operators detect any of these critical symptoms, rapid isolation of the sealed system is essential. Allowing a compressor to cycle continuously on thermal overload with a stuck hot gas bypass valve will break down polyolester (POE) lubricant, generate acid sludge, and culminate in catastrophic motor burnout. Kitchens experiencing similar failures in commercial cold storage should consult our expert refrigerator repair technical team.
Visual Field Restoration: Before vs. After Hot Gas Defrost Solenoid Repair
Restoring a commercial Traulsen reach-in freezer afflicted by a defective hot gas bypass solenoid requires surgical sealed-system craftsmanship. In the field comparison below, inspect the severe mechanical and thermal degradation of an iced-up evaporator coil resulting from a seized solenoid valve, juxtaposed with the pristine factory restoration following precision valve rebuilding, nitrogen brazing, deep micron evacuation, and calibrated refrigerant charging:
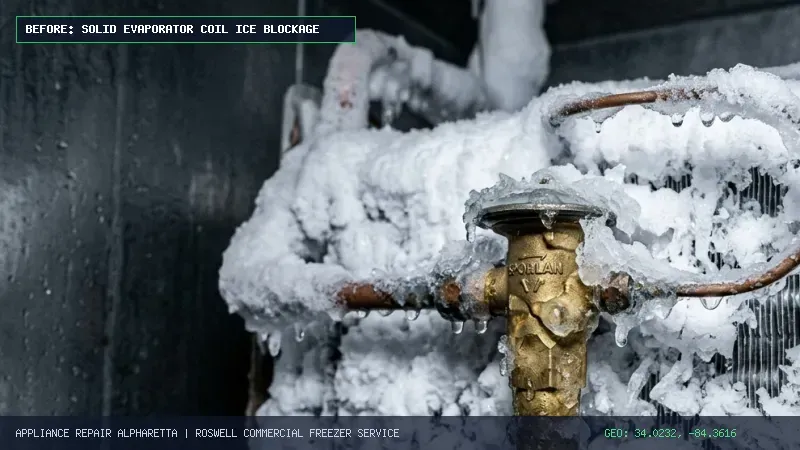
Before: Evaporator coil frozen into a solid glacial block on a Traulsen reach-in freezer. The hot gas solenoid valve plunger was mechanically seized shut with burnt coil windings, preventing thermal defrost cycles and choking cabinet airflow.
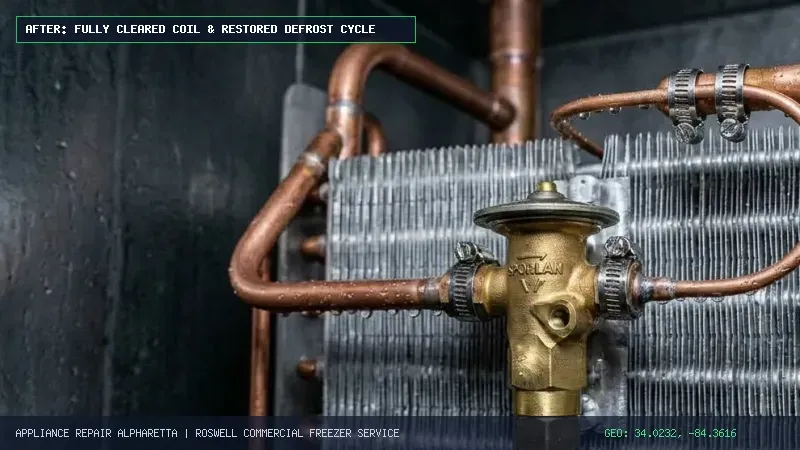
After: Fully restored evaporator coil assembly following OEM Traulsen solenoid valve rebuild, new 24VAC magnetic coil installation (26.4 Ω), deep 250-micron vacuum, and precise refrigerant charge. Cabinet maintains steady -5°F with unrestricted convective airflow.
Notice how the restored assembly exhibits zero ice bridging, immaculate fin spacing, and clean thermal distribution across all refrigerant circuits. Our commercial service trucks carry complete factory rebuild kits and high-capacity recovery machines to execute these comprehensive repairs on-site in a single service visit. For facilities operating commercial warewashing equipment, we also provide expert dishwasher repair and booster heater diagnostics.
Mechanical and Electrical Causes Behind Hot Gas Defrost Solenoid Failure
A commercial Traulsen hot gas defrost solenoid valve operates in an exceptionally demanding physical environment. It bridges two extreme thermodynamic zones: the scorching high-pressure discharge gas line exiting the hermetic compressor and the freezing low-pressure evaporator manifold. Multiple interrelated electrical, chemical, and mechanical failure mechanisms can compromise the valve:
Particulate Contamination and Carbonized Lubricant Sludge
In commercial kitchen environments where ambient condenser temperatures regularly exceed 90°F to 105°F due to cooking line radiant heat, compressor discharge temperatures can exceed 220°F. At these extreme thermal levels, polyolester (POE) synthetic refrigeration oils begin to thermally degrade, polymerizing into microscopic carbonized sludge and varnish. Furthermore, residual copper oxides from original field brazing or wear debris from compressor scroll or reciprocating bearings circulate throughout the closed refrigeration loop. Because the pilot port of a Traulsen hot gas solenoid valve possesses an orifice diameter of less than 0.040 inches (1 millimeter), minute debris easily jams the pilot needle or wedges beneath the main Teflon (PTFE) seating disk. This foreign matter prevents the spring-loaded plunger from seating firmly, locking the valve partially or fully open.
Electrical Breakdown and Thermal Burnout of the 24VAC Solenoid Coil
The electromagnetic coil encapsulated in epoxy atop the brass valve stem is responsible for creating the intense magnetic field required to lift the stainless steel internal plunger against 200+ PSI of differential pressure. Traulsen commercial freezers typically employ 24VAC step-down coils (drawing approximately 10 to 15 volt-amperes) or 115VAC line-voltage coils. Over years of operation, ambient heat radiated from the top-mounted compressor housing bakes the magnetic wire insulation. Voltage fluctuations, brownouts, or rapid cycling can cause inter-turn insulation breakdown. If the coil winding shorts internally, resistance drops from the nominal 22–30 ohms down to near 0 ohms, blowing the control circuit fuse. If the copper winding burns open, resistance reads infinite (OL), leaving the coil completely dead and unable to actuate the valve during defrost.
Internal Plunger Spring Fatigue and Mechanical Galling
Traulsen commercial reach-in freezers initiate hot gas defrost cycles three to four times every 24 hours. Over a five-to-ten-year commercial operational lifespan, the solenoid valve plunger cycles thousands of times. The internal return spring, manufactured from passivated stainless steel, is subjected to continuous thermal cycling between -10°F and 200°F. Over time, metal fatigue weakens the spring tension, reducing its closing force. Simultaneously, the stainless steel plunger sliding inside the non-magnetic enclosing tube can suffer surface galling or mineral erosion, causing it to bind physically against the tube sleeve. When the coil de-energizes, the weakened spring cannot overcome the mechanical friction, leaving the valve stuck wide open in cooling mode. For commercial baking and roasting lines, we also service oven and range repair equipment.
Microprocessor Defrost Relay Contact Welding or Failure
Modern Traulsen G-Series and R-Series reach-in freezers are controlled by the Traulsen Smart Control or INTUITION electronic microprocessor. The electronic board utilizes an onboard electromechanical relay to switch voltage to the defrost solenoid coil or the 24VAC step-down transformer. When an inductive load such as a solenoid coil is de-energized, an inductive voltage spike (flyback voltage) arcs across the miniature relay contacts. Over hundreds of defrost cycles, electrical arcing can physically weld the silver-alloy relay contacts together. When relay welding occurs, 115VAC or 24VAC continues flowing to the solenoid coil 24 hours a day, keeping the hot gas valve locked open even though the controller display indicates normal cooling mode.
Defective Defrost Temperature Termination Sensor (10kΩ NTC Thermistor)
To prevent commercial freezers from overheating their evaporator chambers, Traulsen engineers install an evaporator coil temperature sensor—a precision 10k-ohm negative temperature coefficient (NTC) thermistor. During defrost, when the coil reaches 45°F to 50°F, the sensor signals the microprocessor to terminate the cycle and close the solenoid. If moisture penetrates the thermistor epoxy bulb, the sensor drifts out of calibration, reading falsely cold. The control board assumes the coil is still packed in ice, keeping the defrost relay energized until the emergency fail-safe timer (typically 30 to 45 minutes) finally forces a timeout, causing severe cabinet temperature rise.
Step-by-Step Operator Diagnostics and Initial Inspection Protocol
Before calling for emergency sealed-system refrigeration dispatch, executive chefs, kitchen managers, and commercial facility engineers can conduct safe, non-invasive diagnostic checks to pinpoint the failure and prepare accurate technical details for the incoming repair crew. Follow this structured protocol:
Step 1: Check Traulsen Smart Control Display Status and Error Codes
Inspect the digital display located on the top front louvered panel. Check whether the display reads DEF (actively in defrost mode) or displays a temperature value. Note any blinking alarm codes such as HI TEMP, EP1 (evaporator probe 1 error), or CP1 (cabinet probe error). If the display indicates normal cooling yet the internal temperature is rising steadily, the solenoid may be stuck open.
Step 2: Inspect Evaporator Airflow and Internal Fan Motor Rotation
Open the reach-in freezer door and depress the mechanical door switch plunger manually. Verify whether the internal evaporator blower fans spin immediately. If the fans run but almost zero cold air exhausts from the top distribution duct, shine a flashlight through the louvers to inspect the evaporator coil. If the coil is encased in solid frost, the unit has missed multiple defrost cycles, indicating the hot gas valve is stuck closed or the coil is burnt out.
Step 3: Conduct the External Touch Test on the Solenoid Bypass Tube
With the freezer operating in standard cooling mode (display NOT reading DEF), carefully access the top-mounted mechanical compartment. Locate the 3/8-inch copper line extending from the compressor discharge tee down to the brass hot gas solenoid valve body. Use extreme caution: discharge pipes can exceed 200°F. Feel the copper line exiting the downstream side of the solenoid valve leading to the evaporator. During cooling mode, this line should feel cool or ambient. If the pipe downstream of the valve feels blisteringly hot, the solenoid valve is weeping or stuck wide open, dumping hot discharge gas into the cooling coil.
Step 4: Execute a Manual Defrost Cycle Test
Press and hold the manual defrost key (the snowflake/water droplet icon) on the Traulsen controller for 5 to 7 seconds. Listen intently near the top compressor compartment for an audible mechanical “click” or “thunk” as the solenoid coil energizes. If a distinct metallic click occurs and the bypass pipe instantly warms up, the valve is actuating electrically. If the controller enters DEF mode but no click sounds and the pipe remains cold, the electrical circuit or coil has failed open.
Step 5: Inspect Condenser Coil Cleanliness
Inspect the top-mounted wire-fin condenser coil for heavy deposits of airborne grease, lint, and dust. A clogged condenser coil causes head pressure to escalate past 350 PSI, accelerating thermal breakdown of compressor oil and forcing debris directly into the delicate pilot ports of the hot gas solenoid valve. If heavy lint covers the coil, gently brush it with a soft vacuum attachment.
If these preliminary checks reveal an unyielding warm bypass line, a coil completely encased in solid ice, or a continuously cycling compressor, kitchen staff must cease operation and engage professional commercial service immediately. Commercial kitchens requiring rapid assistance across nearby Alpharetta corridors can also leverage our dedicated Alpharetta, GA technical dispatch team.
Critical Safety Boundaries: When Commercial Operators Must Stop DIY Action
While basic visual checks and manual controller keypad prompts are well within the scope of kitchen management, repairing a commercial Traulsen hot gas defrost system crosses into high-voltage electrical, extreme thermal, and pressurized refrigerant domains. Commercial kitchen operators must cease internal troubleshooting and contact EPA-certified professionals immediately upon encountering the following conditions:
- Never Attempt to Disassemble the Brass Solenoid Valve Under Pressure: The hot gas defrost solenoid is hermetically brazed into the active refrigeration loop containing 18 to 28 ounces of high-pressure R-404A, R-448A, or flammable R-290 propane refrigerant under up to 300 PSI. Unbolting the enclosing tube or loosening the spanner nut without recovering refrigerant will cause explosive gas release, catastrophic cryogenic freeze burns, and severe toxic oil atomization.
- Never Use Torches or Heat Guns on Iced Evaporator Coils: Using an open propane torch or high-powered heat gun inside the cabinet to melt ice risks puncturing thin-walled aluminum refrigeration fins, melting polystyrene insulation liners, or igniting combustible materials in proximity.
- Never Tap or Hammer on the Brass Solenoid Valve Body: Striking the brass valve body with a hammer or wrench in an attempt to “free” a stuck plunger can deform the internal stainless sleeve, permanently ruining the valve seat and potentially fracturing brazed copper joints, venting all refrigerant into the kitchen.
- Never Bypass or Jumper Safety Thermostats or Overloads: Bypassing compressor thermal overloads or jumping defrost termination circuits can cause runaway heating, boiling compressor oil, and electrical short-circuits that risk total facility electrical fires.
- Federal Clean Air Act Violations: Under EPA Section 608 regulations, only certified refrigeration technicians possessing EPA Universal credentials may connect manifold gauges, vent, recover, or charge commercial refrigerants. Uncertified handling incurs federal penalties exceeding $44,000 per violation day.
Protecting your kitchen staff, honoring health department standards, and preserving factory warranties requires professional certified intervention. When high-voltage or refrigeration faults arise, contact our licensed commercial team immediately.
Repair vs. Replace Evaluation: Solenoid Rebuild vs. Complete Condensing Unit
Commercial Traulsen reach-in freezers represent substantial capital investments, with new two- and three-section stainless units commanding replacement costs between $8,500 and $16,000 installed. When faced with a major defrost failure, country club general managers and culinary directors must determine whether rebuilding the solenoid assembly, replacing the condensing unit module, or replacing the entire freezer represents the most economically prudent path. We apply the industry-standard 50% Rule: if the total cost of repair exceeds 50% of the replacement value of a comparable new unit, or if the cabinet has exceeded its expected commercial lifespan, unit replacement is recommended.
| Assessment Factor | Option A: Solenoid Valve Rebuild / Coil | Option B: Complete Condensing Unit Replacement | Option C: Complete Freezer Cabinet Replacement |
|---|---|---|---|
| Estimated Cost Range | $480 – $950 | $2,400 – $3,800 | $8,500 – $16,000 |
| Equipment Age Profile | 1 to 10 Years Old | 8 to 14 Years Old | 15+ Years Old / Corroded Cabinet |
| Compressor Health | Clean POE oil, low acid, strong pump compression | Oil burnt, damaged valve plates, bearing wear | Complete system burnout, obsolete refrigerant |
| Cabinet Structural State | Immaculate stainless steel, tight magnetic gaskets | Sound cabinet shell, minor hinge or door wear | Punctured liner, waterlogged urethane insulation |
| Turnaround / Downtime | 2 to 4 Hours (Same Day) | 1 to 2 Business Days | 1 to 3 Weeks Freight Lead Time |
In over 85% of field calls involving Traulsen reach-in freezers under 10 years of age, rebuilding the hot gas defrost solenoid valve and installing a new 24VAC magnetic coil restores 100% factory efficiency at a fraction of the cost of new equipment. Because Traulsen cabinets feature unyielding 300-series stainless steel liners that last 20+ years, surgical component replacement delivers phenomenal return on investment. For commercial facilities in surrounding Fulton County suburbs, we also provide specialized Roswell, GA refrigeration and cooking repair services.
Commercial Freezer Defrost Repair Cost Drivers and Budget Factors
Commercial kitchen operators budget carefully for maintenance and capital repairs. When addressing a stuck hot gas defrost solenoid valve on a Traulsen commercial freezer, several distinct mechanical and logistical variables influence the total investment:
- Extent of Valve Damage (Coil vs. Sealed System Rebuild): If the failure is restricted purely to an open or shorted 24VAC magnetic coil, the technician can slip off the old coil and slide on a genuine OEM coil without breaching the sealed refrigeration system. This repair falls on the economical end ($280–$440). However, if the internal stainless plunger or brass seat is scored, damaged, or seized with carbon sludge, the sealed system must be recovered, brazed, evacuated to deep micron levels, and recharged with pure refrigerant ($580–$980).
- Refrigerant Type and System Charge Weight: Older Traulsen G-Series freezers utilize HFC blends like R-404A or R-507A, whereas modern units employ lower-GWP alternatives such as R-448A, R-452A, or hydrocarbon R-290. The cost of certified recovery, filter-drier replacement, and factory weight-matched virgin refrigerant scales with the volume of the charge (typically 18 to 32 ounces on dual-section reach-ins).
- Compressor Lubricant Acid Contamination: If a hot gas solenoid has been stuck open for several days, the compressor has likely operated at discharge temperatures exceeding 230°F. The technician must perform a total acid test on the POE oil. If high acidity is detected, the technician must install a high-capacity suction line acid-scavenging filter-drier alongside the new solenoid to protect the compressor against imminent motor burnout.
- Microprocessor Control Board Condition: In instances where electrical coil failure was precipitated by or resulted in a welded defrost relay contact on the Traulsen Smart Control board, the main control board must be replaced simultaneously to prevent immediate destruction of the new replacement solenoid.
- Service Urgency and Weekend Dispatch: When country clubs host major weekend weddings or tournaments, emergency evening or holiday dispatch ensures valuable culinary assets remain protected without kitchen work stoppages.
Our commercial service team provides 100% upfront pricing before touching a wrench, ensuring executive chefs and club general managers understand every line item with zero surprises. For luxury estate kitchens equipped with premium cooking equipment, explore our dedicated Viking appliance repair options.
How Certified Technicians Diagnose Traulsen Hot Gas Defrost Solenoids: Multimeter & Pressure Telemetry
Master commercial refrigeration technicians rely on scientific testing methodologies rather than guesswork. When evaluating a Traulsen commercial reach-in freezer with suspected defrost failure in a Milton kitchen, our technicians execute a comprehensive 4-stage electrical and thermodynamic telemetry audit:
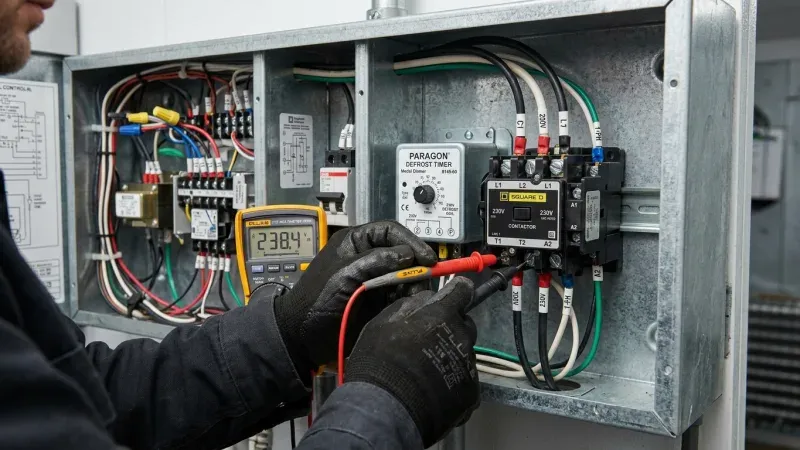
Phase 1: Voltage and Resistance Telemetry Testing
Using a True-RMS digital multimeter calibrated for low-resistance accuracy, the technician disconnects power and disconnects the quick-connect leads feeding the solenoid coil. Measuring across the coil terminals, the technician verifies DC resistance. A factory-spec Traulsen 24VAC solenoid coil must read between 22 and 30 ohms (Ω) at 70°F room temperature. A reading of 0.0 Ω indicates an internal short circuit that will immediately pop the control transformer secondary fuse. A reading of infinite resistance (OL) proves the fine magnet wire has parted due to thermal stress, leaving the coil completely incapable of generating magnetic flux.
Phase 2: Controller Relay Output and Step-Down Transformer Verification
With power restored and the Traulsen Smart Control manually advanced into DEF mode, the technician measures voltage across the defrost relay contacts on the electronic board. The relay must deliver steady 115VAC to the primary side of the control transformer, and the transformer secondary must output a steady 24VAC (±10%) under load to the solenoid leads. If 115VAC is missing during active defrost mode, the board relay is burnt open. Conversely, if 24VAC remains present across the solenoid during standard cooling mode, the relay contacts have welded closed.
Phase 3: Suction Pressure Differential Telemetry
Connecting low-loss digital manifold gauges to the compressor suction and discharge service ports reveals the true thermodynamic state of the valve. In standard cooling mode, a properly functioning R-404A freezer operates at 2 to 6 PSI suction and 220 to 260 PSI discharge. When defrost is initiated, the hot gas solenoid opens, creating a direct bypass from the discharge line into the evaporator. Within 30 seconds, suction pressure must surge to 65 to 75 PSI—reflecting a 60 to 65 PSI suction pressure differential. If the solenoid is energized electrically yet suction pressure remains flat at 4 PSI, the internal plunger is mechanically stuck in the closed position. If suction pressure is 65 PSI during normal cooling mode, the valve is jammed open.
Phase 4: Defrost Temperature Termination Sensor Calibration
The technician inspects the evaporator coil temperature sensor—a 10kΩ NTC thermistor. At 77°F (25°C), the sensor must read exactly 10,000 Ω. At freezing (32°F / 0°C), resistance rises to 32,600 Ω. If the thermistor reads out of spec by more than 10%, the microprocessor will misjudge evaporator temperature, terminating defrost prematurely or failing to terminate, burning out components.
| Component / Test Point | Nominal Specification | Tolerance / Normal Range | Failure Indicator |
|---|---|---|---|
| Hot Gas Bypass Solenoid Coil | 24VAC Electromagnetic Coil | 22 – 30 Ω at 70°F | 0 Ω (shorted) or OL ∞ (open circuit) |
| Electronic Controller Relay Output | Traulsen Smart Control Defrost Pin | 115VAC ± 10% during Defrost | 0V during DEF mode or 115V during cooling |
| Suction Pressure Differential | Low-Side Manifold Gauge Port | 65 PSI Delta (2 PSI to 67 PSI) | <10 PSI change on defrost or 65 PSI constant |
| Defrost Termination Sensor (NTC) | 10kΩ Thermistor Bulb on Coil Return | 10,000 Ω at 77°F / 32,600 Ω at 32°F | >15% resistance drift or open/short circuit |
| 24V Step-Down Transformer | Class 2 Power Supply 40VA | 24.0 – 26.5 VAC Secondary Output | 0 VAC output with 115VAC primary input |
| Compressor Winding Resistance | Copeland Low-Temp Hermetic Pump | Start: 3.5–5.5 Ω / Run: 0.8–1.6 Ω | Open windings or <50 MΩ to ground on megohmmeter |
These precise specifications enable our certified technicians to isolate whether the failure is an isolated electrical coil drop, a stuck mechanical valve body, or an electronic control logic error in minutes. For commercial dishwashing systems, we also provide specialized CMA commercial dishwasher fill valve solenoid repair throughout North Fulton.
Essential Traulsen Commercial Freezer Defrost & Refrigeration Components
A seamless Traulsen commercial reach-in freezer defrost cycle depends on synchronized operation between specialized electro-mechanical and sealed refrigeration components. When servicing Traulsen units, our mobile technical units carry authentic factory-certified OEM replacement parts:
Traulsen Hot Gas Solenoid Valve Body (Part #325-60098-00)
Heavy-duty forged brass 2-way normally closed solenoid valve body with 3/8-inch ODF extended copper solder connections, PTFE synthetic seating disc, and high-temperature Viton internal seals rated for 400 PSI working pressure.
Traulsen 24VAC Magnetic Solenoid Coil (Part #334-60124-00)
Molded waterproof Class H epoxy-encapsulated magnetic coil with quick-connect spade terminals, rated for continuous commercial duty at 24VAC / 60Hz with 22–30 ohms nominal internal resistance.
Traulsen Smart Control Electronic Board (Part #337-60341-00)
Microprocessor command board managing temperature regulation, smart adaptive defrost initiation, 115VAC defrost relay switching, alarm logging, and LED display communications.
10k NTC Evaporator Defrost Termination Sensor (Part #337-60284-00)
Hermetically sealed, moisture-proof thermistor mounted directly to the evaporator coil return bend to monitor real-time coil temperature and terminate defrost at precisely 48°F.
Using genuine Traulsen OEM parts ensures exact electrical impedance matching, correct pipe diameter flow characteristics, and factory safety compliance. For commercial kitchen steam equipment, we also support Rational iCombi Pro steam generator diagnostics across North Fulton County.
Preventative Maintenance Protocols for Milton Commercial Kitchen Freezers
Preventing catastrophic hot gas bypass solenoid lockups requires consistent, disciplined commercial kitchen maintenance. High-volume country club kitchens and banquet facilities can extend equipment life and maintain freezing stability by executing these preventative protocols:
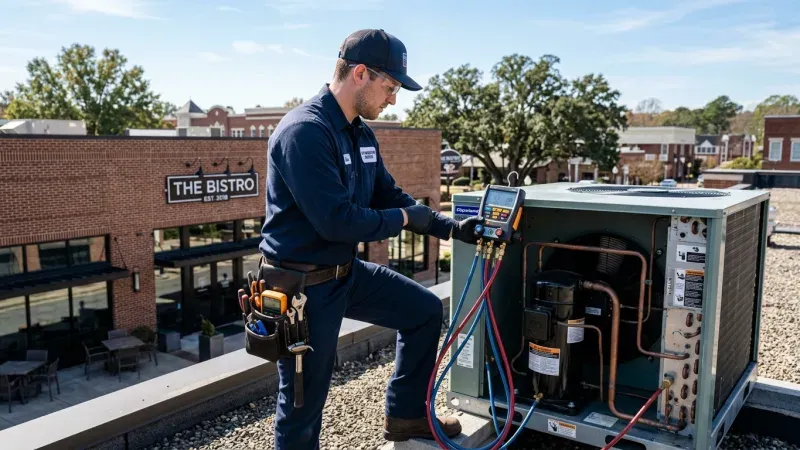
- Monthly Condenser Coil Degreasing and Vacuuming: Airborne cooking oil aerosols and flour dust coat top-mounted condenser fins, restricting airflow and forcing compressor head temperatures above 230°F. Cleaning condenser coils monthly with non-corrosive chemical foaming wash preserves oil integrity and prevents carbon sludge from jamming solenoid orifices.
- Bi-Weekly Magnetic Door Gasket Inspection & Cleaning: A cracked or loose dart-mount magnetic door gasket admits humid kitchen air continuously into the sub-zero cabinet. This massive moisture infiltration overwhelms defrost capabilities and forces excessive defrost cycles that wear out the solenoid plunger. Clean gaskets with warm mild detergent and replace split gaskets immediately.
- Quarterly Electrical Terminal Tightening and Amp Draw Testing: Thermal expansion and contraction loosen screw terminal blocks on the electronic control board, step-down transformer, and contactors. Technicians should tighten all connections and verify compressor running amps against the cabinet serial nameplate.
- Annual Sealed System Acid Testing and Filter-Drier Renewal: Commercial refrigeration systems running continuously in hot kitchens should undergo annual refrigerant oil acid checks. Replacing the liquid line bi-flow filter-drier captures moisture and particulate contamination before it reaches the hot gas valve.
- Defrost Drain Pan and Trace Heater Inspection: Ensure the internal condensate drain line and electric drain pan trace heater are clear and functional to prevent melted defrost water from freezing in the bottom of the cabinet.
Implementing these preventative measures ensures compliance with Fulton County Board of Health regulations, prevents costly inventory write-offs, and ensures peak performance for your commercial refrigeration assets. For residential laundry appliances in country club clubhouses, we also provide expert dryer repair and washing machine repair services.
Commercial High-Voltage and High-Pressure Refrigerant Safety Standards
Commercial refrigeration repair involves substantial physical hazards. Kitchen managers, executive chefs, and internal maintenance personnel must respect rigorous safety guidelines when operating near commercial cooling systems:
- Lockout/Tagout (LOTO) Compliance: Always disconnect and lock out the main commercial branch circuit breaker at the distribution electrical panel before removing protective top louvers or side access panels. Traulsen reach-in freezers utilize 115VAC or 208-230VAC power with high-capacity electrolytic capacitors capable of delivering lethal electrical shocks.
- Severe Thermal Burn Protection: Hot gas discharge lines, compressor cylinder heads, and the brass solenoid body operate at temperatures between 180°F and 220°F. Never handle refrigerant piping with bare hands; always wear heat-resistant leather mechanic gloves.
- Cryogenic Frostbite Hazards: Liquid refrigerant flashing into ambient air instantly drops to -40°F (-40°C), causing irreversible eye damage and instantaneous cryogenic frostbite to exposed skin. Always wear ANSI Z87.1-approved safety goggles and cryogenic work gloves when inspecting sealed service ports.
- Flammable Hydrocarbon Refrigerant Protocols (R-290 Propane): Newer Centerline and G-Series Traulsen models utilize R-290 (A3 refrigerant classification). Absolutely zero open flames, non-explosion-proof electrical switches, or ungrounded recovery machines are permitted in proximity. Use spark-free recovery units and nitrogen purging during all service operations.
- Heavy Equipment Ergonomics: Traulsen reach-in freezers weigh between 350 and 700 pounds. Never attempt to tilt or move cabinets without heavy-duty appliance dollies, locking caster chocks, and adequate mechanical support to prevent tip-over injuries.
Adhering strictly to these professional commercial safety protocols prevents personal injury, protects physical premises, and guarantees high-grade commercial code compliance.
Frequently Asked Questions About Traulsen Hot Gas Defrost Solenoid Repairs
Review comprehensive answers to common technical, operational, and financial questions regarding Traulsen commercial freezer hot gas defrost systems in Milton and North Fulton County:
What is the difference between hot gas defrost and electric defrost on a Traulsen commercial freezer?
Electric defrost systems use electric resistance Calrod heaters positioned below the evaporator fins, requiring 30 to 45 minutes to heat the coil and raising cabinet temperatures by 20°F or more. Traulsen hot gas bypass systems redirect superheated 190°F discharge gas directly into the interior passages of the evaporator tubing, melting coil frost in just 5 to 10 minutes from the inside outward. This drastically minimizes cabinet temperature rise and protects perishable frozen inventory.
Why is my Traulsen commercial freezer blowing warm air while the compressor runs?
When a Traulsen freezer runs continuously while the interior blows warm air (temperatures climbing from 40°F to 60°F), the hot gas defrost solenoid valve is almost certainly stuck in the open position. Superheated discharge vapor is constantly bypassing the expansion valve and flooding the evaporator coil with heat, transforming the cooling coil into an unintended heating element.
What resistance reading should a Traulsen 24VAC hot gas solenoid coil measure on a multimeter?
A healthy factory-spec Traulsen 24VAC solenoid coil measures between 22 and 30 ohms (Ω) at 70°F room temperature. A reading of 0 ohms indicates a shorted coil winding that will trip the secondary transformer fuse, while a reading of OL (open loop) indicates a broken internal wire that prevents the valve from energizing.
Can I replace just the magnetic solenoid coil without recovering refrigerant?
Yes. If the valve body is undamaged and the failure is isolated to an electrically open or shorted coil, the coil slips off the sealed enclosing tube without opening the refrigerant loop. However, if the internal stainless plunger is mechanically jammed or the brass seat is eroded, the refrigerant must be recovered to rebuild or replace the valve body.
What happens to suction pressure when a hot gas solenoid valve is stuck open?
Suction pressure spikes dramatically from its normal operating range of 2 to 6 PSI up to 55 to 75 PSI. Because high-pressure discharge vapor bypasses directly into the low-pressure suction side, the compressor cannot establish the pressure differential required for refrigeration evaporation.
How does a stuck closed hot gas defrost solenoid affect the evaporator coil?
When stuck closed, no hot refrigerant enters the evaporator during defrost mode. Ambient humidity introduced during door openings accumulates across the coil fins, freezing into an impenetrable block of glacial ice within 24 to 48 hours. Airflow halts completely and cabinet temperatures climb past 32°F.
Can a stuck hot gas solenoid valve ruin the commercial compressor?
Yes. A valve stuck open returns superheated gas to the compressor without liquid cooling effect, driving motor temperatures past 230°F. This thermal stress breaks down POE oil into acid sludge, trips internal overloads, and culminates in mechanical compressor bearing seizure or electrical winding burnout.
What role does the defrost termination sensor play in Traulsen freezers?
The defrost termination sensor is a 10k-ohm NTC thermistor attached to the evaporator coil. When the coil reaches approximately 45°F to 48°F during hot gas bypass, the sensor signals the microprocessor to terminate the cycle, closing the solenoid and restoring cooling. A defective sensor can cause defrost cycle timeouts or prevent defrost entirely.
Why is the Traulsen Smart Control flashing a HI TEMP alarm code?
The HI TEMP alarm activates when internal cabinet temperatures exceed the programmed alarm setpoint (typically +20°F or +25°F) for longer than the alarm delay parameter. When a solenoid valve is stuck open or an evaporator is completely choked in ice, temperatures rise into the danger zone, triggering audible and visual alerts.
How long does a Traulsen hot gas defrost cycle normally take?
A normal Traulsen hot gas defrost cycle takes only 5 to 10 minutes to completely clear coil frost. After termination, the system enters a 2 to 3-minute drip time before the compressor restarts and evaporator fans re-engage.
How quickly can a certified technician repair a Traulsen commercial freezer in Milton, GA?
We maintain dedicated mobile technical units stationed near Milton and North Fulton County, providing arrival windows of 40 to 75 minutes for critical commercial refrigeration emergencies. Most solenoid valve rebuilds and sealed system repairs are completed in 2 to 3 hours on-site.
Can carbonized compressor oil cause the hot gas solenoid valve to stick?
Yes. Operating with dirty condenser coils causes discharge temperatures to exceed 220°F, thermally decomposing synthetic POE oil into carbonized varnish and particulate sludge. This debris circulates into the solenoid pilot port, jamming the plunger off its seat.
Is it necessary to replace the filter-drier when replacing the hot gas solenoid?
Yes. Any time a commercial refrigeration system is opened to atmosphere for brazing or component replacement, best practice requires installing a fresh liquid-line filter-drier to absorb atmospheric moisture and capture residual particulate matter.
What warranty covers Traulsen commercial freezer solenoid repairs?
All commercial Traulsen repair work performed by our certified technicians is backed by a 90-day comprehensive parts and labor warranty, with select OEM component rebuild assemblies covered for up to one full year.
Do you service other commercial cooking and refrigeration brands in Milton country club kitchens?
Yes. In addition to Traulsen, our commercial refrigeration and kitchen technicians service True Manufacturing, Hoshizaki, Scotsman, Turbo Air, Hobart, Blodgett, Rational, Cleveland Range, Vulcan, and Frymaster commercial culinary systems.
How can I schedule emergency same-day Traulsen commercial freezer service in Milton?
Call our dedicated commercial technical dispatch center directly at (770) 796-7742. Our dispatcher will confirm technician availability in Milton, collect your Traulsen model and serial data, and dispatch a fully stocked service vehicle immediately.
Related Commercial & Residential Services
Our factory-trained technicians provide comprehensive refrigeration, cooking, and warewashing equipment support across North Fulton County:
- Commercial Appliance Repair Solutions: Full-spectrum maintenance for commercial reach-in freezers, walk-in coolers, convection ovens, fryers, and warewashers.
- Commercial & Residential Refrigerator Repair: Advanced diagnostic troubleshooting for reach-in cooling systems, electronic defrost boards, and compressor failures.
- Same-Day Emergency Service Dispatch: Priority commercial dispatch across Milton, Alpharetta, and Roswell for critical foodservice temperature excursions.
- 24/7 Priority Emergency Kitchen Repair: Urgent evening and weekend service restoring cold storage systems before valuable food inventory spoils.
- Commercial Oven & Range Repair: Diagnostics and restoration for commercial combi ovens, convection ovens, and heavy-duty gas cooking ranges.
Related Commercial Refrigeration Diagnostic Guides
Review technical diagnostic breakdowns covering commercial refrigeration and culinary equipment failures:
- True commercial refrigerator defrost timer stuck and coil iced up: Troubleshooting electromechanical Paragon timers and iced evaporator coils in North Point Parkway venues.
- TurboChef Bullet commercial oven magnetron cooling fan repair in Milton: Resolving magnetron over-temperature alarms, hall-effect sensor errors, and high-speed blower stalls.
- Cleveland commercial convection steamer water level probe repair: Addressing lime scaling, false low-water lockouts, and generator water overflows in Alpharetta.
- Rational iCombi Pro steam generator error code 20 diagnostics: Fixing calcified level sensors and boiler lockouts in Johns Creek commercial kitchens.
Commercial Brand Solutions We Support
In addition to Traulsen commercial refrigeration systems, our technicians maintain factory diagnostic proficiency across industry-leading foodservice and estate kitchen brands:
- Sub-Zero Refrigeration Systems: Dual-refrigeration systems, wine preservation, and microprocessor diagnostics for luxury residential estates.
- Viking Professional Cooking Appliances: Heavy-duty commercial ranges, dual-fuel ovens, and sealed burner maintenance in North Fulton kitchens.
- Thermador Masterpiece & Professional Series: Column refrigeration, induction cooktops, and star burner systems.
- Bosch Benchmark & 800 Series Appliances: Precision warewashing, convection ovens, and quiet refrigeration platforms.
North Fulton Local Service Coverage Areas
We maintain dedicated mobile technical units across North Fulton County, guaranteeing rapid response times for commercial kitchen and residential emergencies:
- Milton, GA Commercial & Estate Service: Serving Crabapple, Birmingham Crossroads, Hopewell Road, and rural equestrian estates.
- Alpharetta, GA Commercial Kitchen Service: Supporting Downtown Alpharetta, Avalon, Windward Parkway, and North Point dining districts.
- Roswell, GA Restaurant Equipment Repair: Supporting Canton Street culinary corridor, Historic Roswell, and Holcomb Bridge dining centers.
- Johns Creek, GA Commercial Culinary Service: Serving Medlock Bridge, Technology Park, and State Bridge commercial dining districts.
Summary & Key Takeaways for Commercial Kitchen Managers
- Hot Gas Defrost Delivers Rapid Ice Removal: Traulsen commercial freezers route superheated 190°F discharge gas through the inside of the evaporator coil, melting frost in 5 to 10 minutes vs. 30 to 45 minutes for electric resistance heaters.
- Valve Stuck Open Causes Severe Warming: A solenoid jammed open continuously dumps 190°F gas into the evaporator, driving suction pressure up to 65–75 PSI and heating cabinet temperatures to 40°F–60°F while the compressor overheats.
- Valve Stuck Closed Causes Glacial Coil Choke: A solenoid failing to open blocks hot gas bypass, allowing airborne moisture to freeze into a solid block across the coil fins, halting airflow and warming the food cabinet.
- 24VAC Coil Nominal Resistance is 22–30 Ohms: Measure coil resistance with a True-RMS digital multimeter. A reading of 0 ohms indicates a shorted winding, while infinite resistance (OL) confirms a burnt open coil wire.
- Pressure Differential Confirms Mechanical Actuation: During hot gas defrost, low-side suction pressure must exhibit an immediate 60 to 65 PSI differential jump (from ~4 PSI to ~68 PSI) confirming the valve orifice has unseated.
- Always Install Genuine OEM Rebuild Kits: Genuine Traulsen replacement parts guarantee precision orifice tolerances, Class H waterproof coil encapsulation, and pressure ratings certified to 400 PSI.
- Monthly Condenser Cleaning Prevents Oil Sludge: Maintaining clean condenser coils keeps compressor discharge temperatures below 200°F, preventing synthetic POE oil carbonization that jams delicate solenoid pilot ports.