
Commercial kitchens operating along the Crabapple Market commercial corridors depend on Vulcan Hart heavy-duty gas ranges to sustain punishing lunch and dinner services without interruption. When open top burners begin clicking incessantly or output a weak, lazy blue flame that cannot boil water or maintain sauté pan sear temperatures, production grinds to a halt. In this master technical guide, our commercial master gas specialists dissect the combustion physics of Vulcan Hart range burner assemblies, analyzing fuel-air Venturi ratios, brass spud orifice fouling, gas manifold pressure calibration, and flame rectification microamp circuitry to restore full 28,000 to 35,000 BTU thermal performance.
Quick Diagnostic Answer for Commercial Kitchen Operators
Continuous burner clicking accompanied by a weak blue flame on Vulcan Hart commercial ranges stems from two primary thermodynamic and electrical failure modes: partially obstructed brass spud orifices reducing natural gas manifold pressure below 3.5″ W.C. (limiting thermal mass flow rate), or a fouled flame rectification electrode failing to conduct the requisite 1.5 to 3.5 microamps (µA DC) back to the spark relight module. Clearing carbonized grease from the precision orifice drill opening (#41 drill size for natural gas) and resetting the spark electrode air gap to 1/8″ restores instantaneous ignition and robust flame retention.
Listen to 60-Second Diagnostic Summary
Narrated by Jason J. (Master Certified Commercial Foodservice Specialist)
Check Same-Day Tech Availability in Your Corridor
Recently Serviced in Crabapple Market Commercial District, Milton GA
Vulcan Hart V Series 36″ Range Burner Orifice De-Liming & Flame Rectification Restored • Verified 5.0 ★★★★★
Vulcan Hart Endurance Range Burner Clicking & Flame Starvation Restoration
Crabapple Road & Heritage Walk Commercial Dining District, Milton, GA 30004
90-Day Commercial Parts & Labor Warranty Active
Boutique Italian Bistro Kitchen Line
Vulcan Hart 36″ Endurance Heavy-Duty 6-Burner Range
Front center and left rear burners clicking continuously, flame lifting and lazy 1/2″ weak blue pattern
Jason J. (EPA / Master Commercial Gas Specialist)
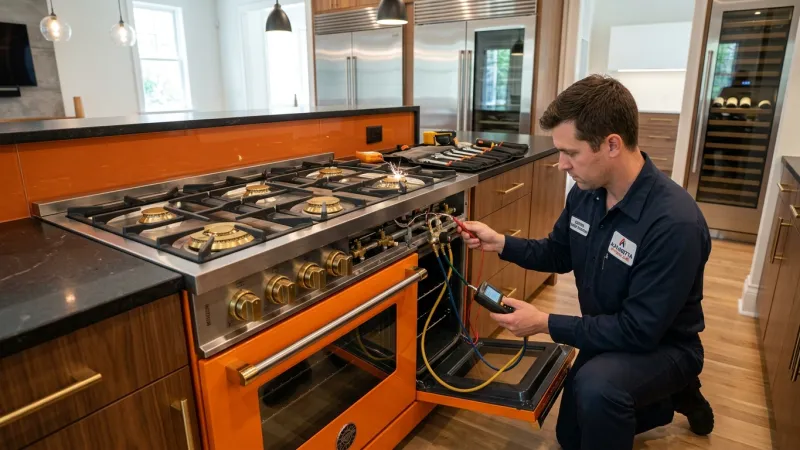
Diagnostic Multimeter & Manometry Telemetry
- Gas Manifold Pressure Under Load: Measured 1.8″ W.C. at burner spud (Factory Specification: 3.5″ W.C. for Natural Gas). Extreme pressure drop induced by heavy cooking oil polymerization inside the brass orifice.
- Flame Rectification Sensor Current: Measured fluctuating 0.4 µA to 0.7 µA DC at the spark electrode (Factory Specification: 1.5 µA to 3.5 µA DC). Microamp drop prevented the relight module from acknowledging flame presence.
- Spark Relight Ignition Module Input: 120 VAC stable, transformer secondary producing 14 kV spark output at 60 Hz cycle rate.
- Orifice Bore Verification: #41 drill bit gauge bound tightly on carbon deposits, indicating a 45% reduction in cross-sectional gas flow area.
Corrective Actions & OEM Part Restoration
Master technician isolated range gas isolation shutoff valve, extracted fouled brass spuds, and performed ultrasonic solvent reaming using precision carbon-cutting compound. Installed genuine Vulcan Hart OEM brass burner orifice spuds (Part #00-411500-00041) bored to exact factory #41 wire gauge diameter. Cleared oxidized carbon glaze from spark electrode ceramic insulators using non-abrasive glass bead dressing and recalibrated spark electrode ground clearance to exactly 0.125″ (1/8″). Reassembled cast iron burner heads, leveled aerator rings, and fine-tuned Venturi air shutters to eliminate yellow tipping.
Post-Repair Verification: Steady 3.5″ W.C. dynamic manifold pressure restored; flame rectification locked at 2.9 µA DC; burner clicking silenced within 0.8 seconds of ignition; deep blue 28,000 BTU inner flame cones holding steady across all firing rates.
Table of Contents
- Commercial Burner Aerodynamics & Vulcan Hart Range Engineering
- Combustion Flame Symptoms & Spark Module Clicking Patterns
- Visual Before & After Restoration Showcase
- Root Causes of Burner Clicking & Weak Flame Output
- Commercial Line Safe Troubleshooting Protocols
- Commercial Gas Safety & NFPA Code Compliance Thresholds
- Heavy-Duty Range Repair vs. Replace Decision Matrix
- Instant Commercial Range Repair Cost Estimator
- Cost Determining Factors for Commercial Range Restorations
- Professional Multimeter Telemetry & Component Diagnostics
- Vulcan Hart Combustion Component Anatomy
- Commercial Kitchen Line Preventative Maintenance & Degreasing
- Gas Isolation & High-Temperature Safety Standards
- Thermodynamic Combustion Kinetics & Stoichiometric Fuel Ratios
- Transient Electrical Noise & Flame Rectification Interference
- Microscopic Metallurgy, Brass Orifice Erosion & Thermal Creep
- Gas Manifold Fluid Dynamics & Pressure Drop Calculations
- Fulton County Commercial Kitchen Fire Codes & NFPA 96 Standards
- Frequently Asked Questions
- Commercial Foodservice Equipment Navigation Silos
- Key Engineering & Operational Takeaways
- Priority Commercial Gas Range Technician Dispatch
Commercial Burner Aerodynamics & Vulcan Hart Range Engineering
Heavy-duty restaurant cooking equipment operates under severe mechanical and thermal environments entirely distinct from residential stoves. When commercial culinary operations along the Crabapple Market dining district prepare hundreds of covers during a Friday dinner rush, open top burners on a Vulcan Hart V Series or Endurance commercial range run at peak thermal output for hours without pause. Vulcan Hart gas burners utilize an atmospheric cast iron Venturi injection configuration capable of delivering between 28,000 and 35,000 BTU/hr per open top section. Gas flows under controlled manifold pressure through an exchangeable brass spud orifice, discharging at high velocity into the throat of the Venturi tube.
According to Bernoulli’s principle of fluid dynamics, the high-velocity stream of fuel gas exiting the orifice creates a localized low-pressure zone at the throat of the Venturi. This pressure depression pulls in ambient air through the adjustable air shutter—designated as primary air. This primary air mixes turbulently with natural gas or liquid propane inside the cast iron mixing tube before distributing across dozens of precision-machined flame ports on the burner head. For comprehensive line servicing beyond cooking units, our technicians also provide dedicated commercial appliance repair throughout Fulton County commercial kitchens.
When the burner is operating properly, the air-to-fuel ratio closely mirrors ideal stoichiometric proportions (approximately 10 cubic feet of air to 1 cubic foot of natural gas). Upon reaching the burner port tips, the fuel mixture contacts secondary air drawn from the surrounding cooktop environment, forming a razor-sharp, stable, deep blue inner flame cone anchored securely to each port with zero flame lifting, zero yellow soot deposition, and zero audible clicking from the electronic ignition sub-assembly.
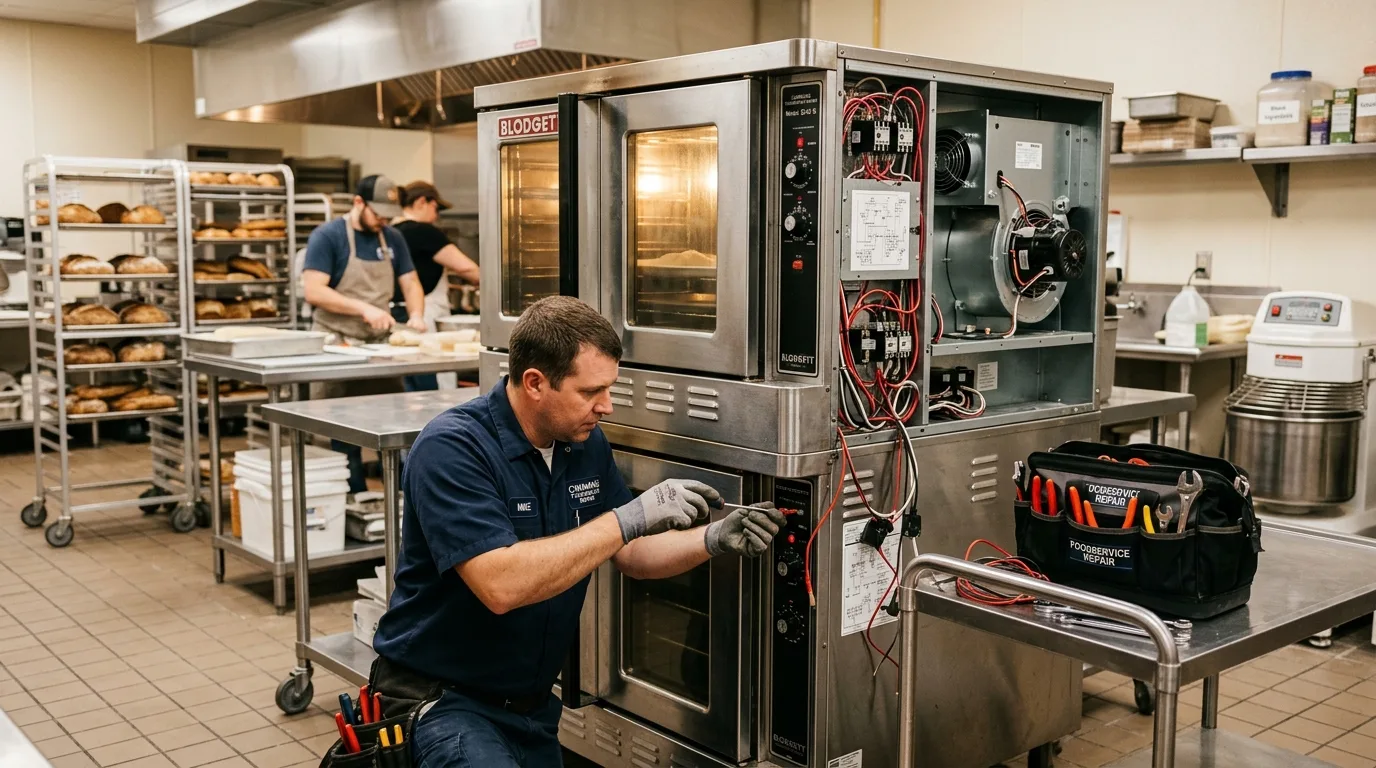
Combustion Flame Symptoms & Spark Module Clicking Patterns
In high-tempo kitchen environments, chefs often overlook gradual burner degradation until an open top section fails completely during service. Recognizing early symptom patterns allows kitchen managers to schedule proactive service before tickets back up. On Vulcan Hart commercial ranges equipped with electric spark ignition or pilot-less spark relight modules, several distinct symptoms indicate combustion boundary disruption.
The most prominent operational failure is rhythmic, continuous clicking from the high-voltage spark electrode long after the gas valve has been rotated to the high flame position. Under normal operation, the spark module fires at 2 to 4 Hz until the burner ignites, at which point the microamp flame rectification sensor registers an ionized flame path and immediately interrupts the spark circuit. If the spark continues clicking while a small flame burns, the flame sensor is failing to detect sufficient electrical conductivity through the flame envelope. In facilities with extensive cooking suites, addressing these issues promptly through specialized commercial oven and range repair prevents complete ignition lockout.
Simultaneously, kitchen personnel will observe that the flame pattern is visually compromised. Instead of a vibrant, 1.5-inch to 2-inch crisp blue cone with a distinct light blue inner core, the burner produces a stunted, lazy, translucent 1/2-inch flame that flickers timidly around only half of the burner perimeter. Sauté pans take upwards of ten minutes to reach high heat, and heavy stockpots fail to achieve a rolling boil. In severe cases, the flame lifts completely off the burner ports with an audible hissing sound, or exhibits yellow tipping that rapidly coats the undersides of cookware with black carbon soot.
Visual Before & After Restoration Showcase
Field restorations executed by our master technicians resolve both mechanical gas delivery restrictions and electronic signal degradation. Below is an authentic macro photographic comparison from a recent field dispatch along the Crabapple Market commercial strip, documenting the severe internal contamination responsible for burner clicking and weak flame velocity.
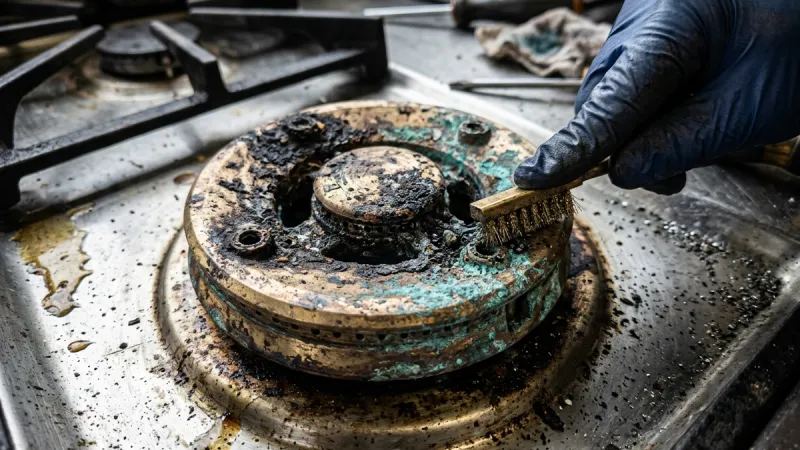
Extreme carbon encrustation and polymerized cooking grease blocking the #41 brass spud orifice opening. Manifold fuel delivery dropped from 3.5″ to 1.8″ W.C., starving the Venturi tube and dropping flame rectification current below 0.6 µA DC, locking the spark module into continuous clicking.
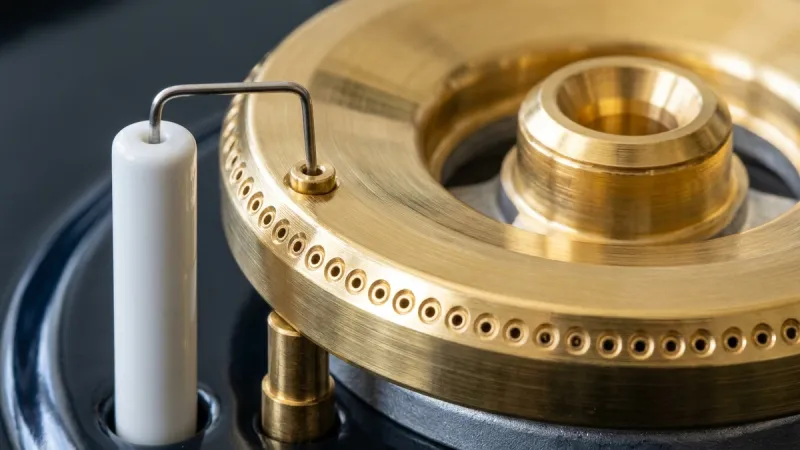
Pristine factory OEM Vulcan Hart brass orifice installed and calibrated to 3.5″ W.C. with re-aligned cast iron burner head. Stable 2.9 µA DC flame rectification achieved, silencing the spark module within 0.8 seconds and releasing 28,000 BTU thermal capacity.
Root Causes of Burner Clicking & Weak Flame Output
Diagnosing combustion failures on commercial gas cooking equipment requires understanding the interdependency between gas fluid dynamics and electrical sensing circuits. When a Vulcan Hart range displays both continuous spark clicking and low thermal velocity, multiple compounding root causes are typically present simultaneously across the cooktop manifold.
Brass Spud Orifice Fouling from Cooking Grease Boil-Overs
The brass orifice spud threaded into the front manifold valve controls the precise volume of gas entering the burner Venturi. In active commercial kitchens, high-volume sautéing, sauce reductions, and stockpot boiling inevitably produce boil-overs. Liquid fats, marinades, and starches cascade down around the burner ring and drip directly onto the orifice assembly. As temperatures fluctuate, these organic fats bake onto the brass orifice face, creating an impervious carbon glaze. Because natural gas orifice diameters are extraordinarily small—typically #41 wire drill size (0.0960 inches) for 28,000 BTU—even a microscopic layer of carbon reduces cross-sectional orifice area by 30% to 50%, starving the burner of combustible fuel.
Flame Rectification Microamp Circuit Breakdown
Modern electronic ignition systems utilized on commercial kitchen ranges utilize flame rectification rather than simple bimetal thermocouples to prove flame presence. The spark module applies a 120 VAC potential between the spark electrode probe and the grounded burner chassis. Burning gas molecules are naturally ionized; this plasma envelope acts as a diode, conducting electricity more easily in one direction than the other and converting alternating current (AC) into a direct current (DC) microamp signal. If grease glaze coats the ceramic insulator, or if the flame is too weak and starved to physically envelope the electrode tip, the rectified current drops below 1.5 µA DC. The module assumes flame failure and energizes the spark generator continuously. When urgent repairs arise during morning prep, our kitchen partners book same-day commercial repair service to prevent dining room closures.
Manifold Gas Pressure Loss from Contaminated Regulators
Commercial gas ranges require a constant, stable manifold pressure: 3.5″ to 4.0″ Water Column (W.C.) for Natural Gas, or 10.0″ W.C. for Liquid Propane. If the commercial appliance gas pressure regulator behind the range is fouled by pipe dope, iron oxide mill scale, or water vapor from incoming utility lines, downstream pressure drops precipitously when multiple burners are ignited simultaneously. A manifold operating at only 2.0″ W.C. cannot provide sufficient gas velocity to draw primary air through the Venturi, resulting in a weak, drooping flame that cannot maintain cooking temperatures.
Venturi Primary Air Shutter Misalignment & Lint Clogging
Behind the front control panel, each Vulcan Hart burner features an adjustable air shutter secured with a locking screw. Commercial kitchen exhaust hoods move thousands of cubic feet of air per minute, drawing flour dust, lint, and aerosolized grease beneath the cooktop chassis. This debris accumulates inside the Venturi throat, choking primary air intake. If the shutter is knocked out of calibration during cleaning, the fuel mixture becomes excessively fuel-rich (causing yellow tipping and carbon buildup) or excessively lean (causing flame lifting, where the flame detaches from the burner ports and fails to bathe the rectification sensor).
Warped Cast Iron Burner Head Caps & Port Oxidation
Vulcan Hart open top burners utilize heavy-duty cast iron heads engineered to distribute fuel evenly across concentric rings of flame ports. Years of exposure to 1,500°F combustion temperatures combined with aggressive end-of-night water quenching during kitchen sanitation causes cast iron thermal shock. Burner caps warp, creating microscopic air gaps between the base and cap through which raw gas escapes before reaching the ports. Furthermore, rust scale and boiled-over grease clog individual port openings, forcing gas out unevenly and preventing the flame from propagating across to the spark sensor.
Commercial Line Safe Troubleshooting Protocols
Before calling for professional equipment restoration, kitchen managers and executive chefs can conduct safe preliminary visual checks to identify obvious mechanical misalignments without opening pressurized gas lines. Kitchen managers should always ensure the range is completely cool and gas supplies are isolated before attempting hands-on inspections.
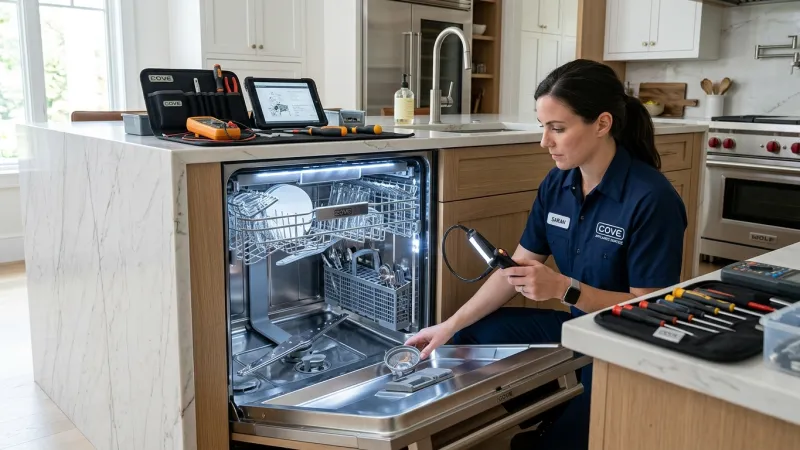
- Step 1 — Verify Burner Head Seating: Remove the heavy cast iron grates and inspect the burner head assembly. Ensure the cast iron cap sits completely flush against the mixing bowl. If cleaning staff knocked the cap off its locating pins, gas will escape laterally rather than through the ports, causing erratic ignition and clicking.
- Step 2 — Inspect Ceramic Spark Electrode Cleanliness: Examine the white porcelain insulator surrounding the spark electrode tip. Check for cracks in the ceramic or thick coatings of grease. If grease or carbon is present, clean gently using isopropyl alcohol and a lint-free cloth. Do NOT use abrasive wire brushes that scratch the glaze and create conductive carbon tracking paths.
- Step 3 — Inspect Flame Port Openings: Inspect each individual port hole along the perimeter of the cast iron burner ring. Use a stiff wooden toothpick or brass bristle brush to clear debris from blocked holes. Never drive hardened steel drill bits or sewing needles into ports, which can enlarge or deform critical combustion orifices.
- Step 4 — Perform Full-Bank Burner Firing Test: Turn on all open top burners, the griddle plate, and the lower convection oven simultaneously. Observe whether flame height drops significantly on the clicking burner when neighboring appliances engage. A noticeable flame drop indicates a line-wide gas supply or regulator delivery issue rather than an isolated burner malfunction. When emergency kitchen issues arise on the hot line, kitchens rely on emergency commercial appliance repair to restore cooking capacity.
- Step 5 — Inspect Venturi Throat for Obstructions: Lift the burner casting from the manifold support pin and peer down the mixing throat using a flashlight. Check for cobwebs, grease balls, or fallen food scraps resting inside the Venturi tube. Clear any obstruction before reseating the burner.
Commercial Gas Safety & NFPA Code Compliance Thresholds
While basic visual inspections and surface cleaning can be handled safely by in-house kitchen personnel, touching pressurized gas manifolds, disassembling control valves, or drilling burner orifices is strictly forbidden by commercial insurance policies, Fulton County building codes, and National Fire Protection Association (NFPA) standards.
If you detect the distinctive rotten-egg sulfur odor of mercaptan (natural gas odorant), hear loud hissing from behind the kick plate, or witness large yellow rolling flames that produce acrid black smoke, HALT DIY TROUBLESHOOTING IMMEDIATELY. Commercial ranges operate at enormous gas flow volumes; an unmetered leak inside an enclosed cook line creates an acute flashover explosion hazard that threatens the safety of kitchen staff and dining patrons. For operators situated in neighboring Milton communities, our team coordinates priority appliance repair in Milton, GA with rapid local response times.
Under NFPA 54 (National Fuel Gas Code) and NFPA 96 (Standard for Ventilation Control and Fire Protection of Commercial Cooking Operations), any repair involving gas manifold pressure adjustment, pilot safety shutoff valves, or gas orifice modification must be performed by a licensed, certified gas appliance technician equipped with calibrated electronic combustible gas sniffers and electronic digital manometers. Attempting DIY repairs with improper tools risks damaging brass threads, causing gas leaks that void commercial property insurance coverage in the event of a kitchen fire.
Heavy-Duty Range Repair vs. Replace Decision Matrix
Restaurant operators face substantial capital expenditure choices when hot line cooking equipment falters. A new heavy-duty Vulcan Hart 6-burner commercial range costs between $4,500 and $9,500, not including freight delivery, mechanical rigging, gas line hookup, and municipal building inspection fees. Applying the foodservice industry standard 50% Rule helps operators make financially sound repair-versus-replacement decisions.
| Evaluation Factor | Pro-Repair Recommendation (>85% of Cases) | Pro-Replacement Recommendation |
|---|---|---|
| Equipment Age & Duty Life | Range is under 12–15 years old; chassis and structural frame are solid and square. | Range exceeds 18–20 years; severe chassis rust-through or structural sagging. |
| Total Restoration Cost | Repair ticket ($380–$890) is well under 30% of new equipment replacement cost. | Cumulative repair estimate exceeds 50% of replacement value including installation. |
| Failure Mode Severity | Isolated orifice clogging, spark relight failure, or manifold pressure drift. | Cracked cast iron manifold header pipe or catastrophic oven cavity collapse. |
| Downtime Impact | Same-day field restoration in 1–2 hours; zero missed dinner service shifts. | Lead time of 2–4 weeks for commercial equipment freight shipping and rigging. |
| Energy & Combustion Efficiency | Restoring factory Venturi calibration yields 100% stoichiometric thermal efficiency. | Obsolescent non-insulated range body wasting significant kitchen HVAC energy. |
Instant Commercial Range Repair Cost Estimator
Use our interactive dynamic repair calculator below to generate a real-time diagnostic and repair estimate based on your Vulcan Hart equipment profile, reported symptoms, and unit service history. For neighboring dining destinations along Canton Street, our technicians handle Roswell commercial cooking repairs with factory tooling.
Cost Determining Factors for Commercial Range Restorations
Understanding what drives repair expenses enables restaurateurs to allocate maintenance budgets effectively. Several critical variables dictate the final scope and investment required to restore a malfunctioning Vulcan Hart range:
- Number of Compromised Burner Sections: If only a single burner has suffered grease boil-over contamination, a targeted orifice extraction and electrode adjustment is rapid and economical. However, in busy sauté stations where multiple burners have degraded simultaneously, overhauling the full manifold bank provides substantial labor savings compared to multiple emergency service calls.
- Ignition Architecture (Standing Pilot vs. Electronic Spark Relight): Basic standing pilot ranges utilize mechanical brass pilot tips and bimetal safety valves, which are inexpensive to rebuild. Heavy-duty ranges featuring multi-point electronic spark relight modules, pulse generators, and high-temperature flame sensors require precision electronic diagnostics and specialized OEM solid-state components.
- Gas Manifold Integrity & Pressure Regulation: If pressure diagnostics reveal that the appliance line regulator is stuck shut or leaking internally, replacing the master 3/4″ or 1″ NPT commercial gas regulator adds component cost but restores full thermal capacity to the entire cooking line.
- Replacement Part Availability & OEM Sourcing: Genuine Vulcan Hart OEM combustion components—including factory-bored brass spuds, Inconel electrode pins, and Baso gas safety valves—guarantee long-term durability and safety, whereas low-grade aftermarket copies fail rapidly under commercial kitchen temperatures. In corporate dining kitchens, we also service Southbend commercial range pilot repairs with identical technical rigour.
Professional Multimeter Telemetry & Component Diagnostics
Master certified foodservice technicians do not guess or swap parts blindly. We deploy precision electrical and manometric diagnostic instrumentation to capture quantitative component telemetry directly from the range assembly. Below is our filterable field diagnostic telemetry table detailing factory electrical tolerances, manifold pressures, and orifice specifications.
| Component Test Target | Test Meter Setting | Factory Operating Tolerance | Failure / Fault Threshold | Diagnostic Diagnostic Action |
|---|---|---|---|---|
| Flame Rectification Current | DC Microamps (µA DC) In-Series | 1.5 µA – 3.5 µA DC Stable | < 0.8 µA DC (Causes Clicking) | Clean electrode ceramic; de-scale burner head port ground plane. |
| Natural Gas Manifold Pressure | Digital Manometer (Inches W.C.) | 3.5″ to 4.0″ W.C. Dynamic | < 2.8″ W.C. Under High Fire | Adjust appliance regulator spring; inspect upstream line isolation valve. |
| Liquid Propane (LP) Pressure | Digital Manometer (Inches W.C.) | 10.0″ W.C. Dynamic Under Load | < 8.5″ W.C. Under High Fire | Calibrate LP second-stage regulator; check tank supply vaporization rate. |
| Natural Gas Orifice Bore Size | Precision Wire Gauge Pin Gauge | #41 Drill Size (0.0960 in / ~28k BTU) | Bore reduced > 15% or over-reamed | Replace with factory Vulcan OEM spud #00-411500-00041. |
| LP Gas Orifice Bore Size | Precision Wire Gauge Pin Gauge | #52 Drill Size (0.0635 in / ~28k BTU) | Carbon glaze or incorrect NG spud | Install dedicated LP brass spud; adjust air shutter to prevent soot. |
| Spark Module Supply Voltage | True-RMS AC Volts | 115 – 125 VAC Line Voltage | < 102 VAC or > 132 VAC | Check breaker panel neutral bus; inspect control harness wiring. |
| Electrode Ceramic Insulation | Megohmmeter @ 500V DC | > 50 MΩ to Chassis Ground | < 5 MΩ (Dielectric Leakage) | Replace cracked porcelain spark igniter electrode probe. |
Vulcan Hart Combustion Component Anatomy
Every Vulcan Hart range engineered by ITW Food Equipment Group is built upon proven, modular commercial combustion components designed to withstand intense mechanical vibration and thermal cycling. Understanding these individual assemblies is key to executing rapid, precise repairs. For operations utilizing commercial convection ovens in nearby Forsyth County, we offer comprehensive Blodgett commercial convection oven service.
- Precision Machined Brass Spud Orifices: Factory calibrated threaded brass fittings that discharge fuel gas directly into the Venturi entrance. Vulcan Hart manufactures orifices to tight tolerances (AMS-4640 naval brass) to resist sulfur erosion from utility fuel streams.
- One-Piece Aerated Cast Iron Venturi Burners: The aerodynamically shaped cast iron body incorporates a progressive Venturi bell, mixing neck, and radial port distribution head that balances gas velocity across all ports without creating localized hot spots.
- Electronic Spark Relight Pulse Modules: Solid-state ignition controllers manufactured by Fenwal or Honeywell that generate 14,000 to 20,000 Volt pulsed sparks across the electrode gap. The module incorporates sensitive comparator operational amplifiers that continuously monitor flame rectification microamps.
- Alumina Ceramic Spark & Sensor Probes: High-purity 99% alumina porcelain insulator bodies supporting heat-resistant nickel-chromium or Inconel wire probes positioned precisely 1/8″ above burner port crowns.
- Commercial Gas Pressure Regulators: Heavy-duty spring-loaded diaphragm regulators that throttle utility inlet pressures (typically 7.0″ to 14.0″ W.C. natural gas) down to a stable 3.5″ to 4.0″ W.C. manifold operating standard regardless of upstream pressure surges.
Commercial Kitchen Line Preventative Maintenance & Degreasing
Preventing unexpected burner failures requires institutionalizing rigorous end-of-day cleaning procedures that protect sensitive combustion orifices rather than damaging them. Kitchen staff often inadvertently trigger burner clicking by spraying liquid degreasers directly over assembled burner heads.
The Soak-and-Scrub Protocol: At the close of each shift, kitchen porters should lift off heavy grates and removable burner head caps. Soak cast iron caps in a hot, non-corrosive carbon-cutting bath for 30 minutes. Use a stiff brass wire brush to clean port slots. Crucially, allow cast iron components to dry completely before reassembling—never reinstall wet burner caps, as moisture trapped inside burner ports immediately shorts out the spark electrode, causing continuous clicking until heat evaporates the water. To ensure comprehensive kitchen reliability, commercial operators regularly pair range servicing with Frymaster commercial fryer troubleshooting for maximum hot-line uptime.
Orifice Shielding During Deep Cleaning: When deep-cleaning the range chassis with foam degreasers or pressure sprayers, always cover the brass spud orifices located along the front manifold with clean dry rag plugs or magnetic orifice shields. Liquid caustic degreasers seeping into orifice openings crystallize upon drying, forming rock-hard chemical obstructions that severely choke gas delivery.
Gas Isolation & High-Temperature Safety Standards
Working around high-capacity commercial gas ranges demands strict adherence to life safety protocols. A single Vulcan Hart 60-inch commercial range can consume in excess of 250,000 BTU/hr across its open tops, griddle, and double ovens—an enormous volume of volatile energy.
Always locate the designated yellow-handled emergency gas shutoff valve installed upstream of the quick-disconnect flex hose. In the event of an uncontrolled gas smell or flare-up, rotate this valve 90 degrees perpendicular to the pipe run immediately. When ranges are rolled away from the exhaust canopy for sanitation or service, verify that the mechanical restraint cable is firmly attached; this steel cable prevents accidental overextension and shearing of the flexible stainless steel gas connector. When sanitation lines require warewashing support, our master technicians also perform expert Hobart commercial dishwasher repairs across Fulton County.
Thermodynamic Combustion Kinetics & Stoichiometric Fuel Ratios
The combustion of natural gas (predominantly methane, $CH_4$) is a rapid exothermic chemical reaction yielding carbon dioxide, water vapor, and intense heat energy according to the stoichiometric equation:
CH4 + 2 O2 → CO2 + 2 H2O + ΔH (891 kJ/mol)
To achieve complete combustion and generate the signature crisp blue inner cone, exactly two molar equivalents of oxygen are required for every mole of methane. Because atmospheric air contains approximately 21% oxygen by volume, approximately 9.52 volumes of air must mix with each volume of methane gas. In a Vulcan Hart commercial burner, this air volume is delivered in two distinct phases: 40% to 50% as primary air introduced through the Venturi throat, and the remaining 50% to 60% as secondary air drawn from the surrounding open atmosphere around the burner crown.
When an orifice is partially clogged with carbon, the gas discharge velocity drops significantly. According to the conservation of momentum and Venturi fluid dynamics, lower gas mass velocity produces a much weaker localized vacuum at the throat. Consequently, primary air intake falls precipitously. The fuel mixture arriving at the burner ports becomes starved and fuel-rich relative to the reduced flow velocity, destroying flame stiffness. The flame cannot anchor firmly to port crowns, lifting upward and dropping flame envelope temperature from an optimal 2,800°F down to less than 1,700°F.
Transient Electrical Noise & Flame Rectification Interference
In high-density commercial kitchens, hundreds of horsepower of electric inductive loads operate in close proximity to the cooking line. Rooftop exhaust blowers, refrigeration compressor racks, commercial dishwashers, and food processors cycle constantly across the building electrical grid. These inductive motor loads produce substantial electrical line harmonics, high-frequency voltage spikes, and ground potential fluctuations.
Because flame rectification signals operate in the fragile direct-current microamp range (1.5 to 3.5 µA DC), electrical noise on the building chassis ground can easily corrupt the sensor circuit. If the range chassis does not maintain a solid, low-impedance earth ground connection (< 0.2 Ohms resistance to building ground), AC ground loop currents bleed across the burner casting. The electronic spark relight module’s differential amplifier cannot distinguish the true rectified microamp DC signal from ambient AC electrical hash. As a result, the controller fails to verify flame presence, causing the spark module to click continuously despite the presence of a visible flame. High-output culinary operations frequently combine cooking line overhauls with Cleveland commercial steamer restoration to maintain flawless preparation workflows.
Microscopic Metallurgy, Brass Orifice Erosion & Thermal Creep
Commercial gas spud orifices endure severe metallurgical degradation over thousands of operating hours. While brass is chosen for its machinability and non-sparking properties, it has a relatively low thermal softening point compared to stainless steel or cast iron. Positioned inches away from 28,000 BTU burner heads, brass spuds routinely experience continuous ambient temperatures exceeding 350°F to 500°F.
Under sustained high-temperature exposure, brass undergoes microscopic grain boundary expansion and zinc leaching (dezincification) when exposed to sulfur compounds in commercial gas lines and chlorine compounds in kitchen sanitizers. Furthermore, well-meaning kitchen cleaners often attempt to clear clogged orifices using steel welding tip cleaners or hard steel wire. Steel has a Rockwell hardness far exceeding brass; jamming steel reamers into an orifice inevitably cuts microscopic grooves, flares the discharge throat, or distorts the precision circular bore. An orifice bore enlarged by merely a few thousandths of an inch increases gas flow by over 25%, producing excessive fuel velocity, noisy combustion roar, and lethal carbon monoxide production.
Gas Manifold Fluid Dynamics & Pressure Drop Calculations
Calculating the gas flow rate through an orifice spud is governed by the standard compressible fluid discharge formula:
Q = 1658.5 • Cd • A • √(ΔP / G)
Where $Q$ represents gas flow rate in cubic feet per hour, $C_d$ is the discharge coefficient (typically 0.82 for precision chamfered orifices), $A$ is cross-sectional orifice area in square inches, $Delta P$ is gas manifold differential pressure in inches Water Column, and $G$ is the specific gravity of the fuel gas (approximately 0.60 for natural gas relative to air).
Notice that fuel flow rate is directly proportional to both orifice area $A$ and the square root of differential pressure $Delta P$. When carbon deposits reduce effective bore area from a #41 drill diameter ($0.007238text{ in}^2$) down to a #50 diameter ($0.003848text{ in}^2$), gas delivery drops by nearly 47%. If line manifold pressure simultaneously droops from 3.5″ to 2.2″ W.C. due to regulator restriction, the compounding reduction leaves the burner operating at barely 35% of rated thermal capacity—rendering it incapable of supporting commercial cooking speeds. For back-of-house storage facilities, our refrigeration teams also maintain Nor-Lake commercial walk-in cooler maintenance to protect raw perishable inventory.
Fulton County Commercial Kitchen Fire Codes & NFPA 96 Standards
Foodservice operators across Milton, Alpharetta, Roswell, and Johns Creek are subject to rigorous commercial fire safety regulations enforced by the Fulton County Fire Marshal’s Office and local municipal building departments. Commercial gas ranges must comply with strict physical clearance mandates, Type I commercial hood ventilation requirements, and semi-annual Ansul fire suppression system testing:
- Exhaust Canopy Airflow Velocity: Commercial cooking lines utilizing solid-fuel or heavy-duty gas open burners must maintain a minimum capture velocity of 100 feet per minute (FPM) measured at the lip of the Type I kitchen exhaust hood to ensure complete extraction of combustion byproducts and grease vapors.
- Combustible Clearance & Stainless Backsplashes: Ranges installed against building walls require 6 inches of clearance to combustible materials or must be shielded with an approved non-combustible ceramic tile or heavy-gauge stainless steel riser assembly.
- Emergency Gas Solenoid Interlocks: In modern commercial kitchen builds, the primary gas supply to the cooking line must be equipped with an automated mechanical or electrical gas shutoff valve interlocked directly to the kitchen exhaust hood proving switch and the fire suppression release system. If the hood is turned off or fire suppression discharges, gas delivery to the range must cut out within 2 seconds.
- Documented Certified Maintenance: Annual gas safety audits and combustion analysis records must be logged and maintained on-site for review during municipal fire safety inspections. Certified service records from our technicians satisfy municipal inspection mandates. To safeguard cold prep lines simultaneously, explore our specialized commercial walk-in freezer defrost repairs.
Frequently Asked Questions
Why does my Vulcan Hart commercial range burner click continuously while the flame is burning?
Continuous clicking occurs because the electronic spark relight module is not detecting a sufficient flame rectification microamp current (1.5 to 3.5 µA DC). Even though a small flame is visible, carbon or grease coating the ceramic electrode or a weak, starved flame pattern prevents the current from conducting to ground through the flame envelope. The module assumes ignition failure and keeps pulsing the high-voltage spark.
What causes a weak, lazy blue flame on a commercial gas burner?
A weak blue flame indicates severe fuel starvation. The primary culprit is a brass spud orifice partially clogged with baked-on boil-over cooking grease, reducing gas flow area. Additional causes include a drop in line manifold pressure below 3.5″ W.C., a clogged Venturi mixing tube, or an obstructed internal appliance gas regulator.
Can I clean a commercial gas burner orifice with a sewing needle or paper clip?
No, absolutely not. Brass is a relatively soft metal, and natural gas orifices are precision-drilled to exact thousandths of an inch (#41 wire gauge diameter). Hard steel needles or paper clips can gouge, scratch, or ream out the brass hole, causing oversized gas delivery, unstable combustion roaring, and dangerous carbon monoxide formation. Use only ultrasonic solvent baths or factory-sized carbon reaming broaches.
What is the correct natural gas manifold pressure for a Vulcan Hart range?
Standard natural gas Vulcan Hart commercial restaurant ranges require 3.5″ to 4.0″ Water Column (W.C.) manifold operating pressure measured at the range manifold tap under full firing load. Liquid Propane (LP) configurations require 10.0″ W.C. operating pressure.
What microamp reading should a commercial range flame sensor produce?
A healthy flame rectification circuit on a Vulcan Hart commercial range should produce between 1.5 and 3.5 microamps direct current (µA DC) with the burner firing at high flame. Any reading consistently below 0.8 to 1.0 µA DC triggers the spark controller’s flame lockout or relight cycling sequence.
How do I know if my burner clicking issue is electrical or gas-related?
If the burner will not light at all and no gas odor or hissing is present, the issue is likely a clogged orifice or closed valve. If gas flows and ignites with a robust, vigorous 2-inch blue flame but the electrode continues clicking, the failure is purely electrical (fouled ceramic, loose wire, or defective spark module). If the flame is tiny and weak while clicking, both gas starvation and sensor failure are occurring simultaneously.
How often should commercial gas range orifices be cleaned or replaced?
In high-volume commercial dining kitchens, brass orifices should undergo professional inspection and ultrasonic cleaning every 6 months during routine preventative maintenance. If heavy boil-overs occur or if metal tip cleaners have flared the bore, brass spud orifices should be replaced immediately with factory OEM parts.
Can a faulty exhaust hood cause commercial range burners to burn poorly?
Yes. If the makeup air unit (MAU) is malfunctioning or the kitchen operates under severe negative atmospheric pressure, downdrafts or inadequate fresh oxygen supply starve the burners of secondary air. This causes floating, lazy flames, yellow tipping, and poor flame rectification stability.
What drill size is used for Vulcan Hart natural gas open top burners?
For standard 28,000 BTU open top burners operating on Natural Gas at 3.5″ W.C. manifold pressure, a #41 wire gauge drill size (0.0960 inch diameter) is standard. For high-output 35,000 BTU burners, a #39 or #38 drill size is utilized.
Why is my commercial range flame lifting completely off the burner ring?
Flame lifting occurs when gas discharge velocity exceeds flame propagation speed. This is typically caused by excessive primary air opening at the Venturi shutter, high gas manifold pressure exceeding factory limits, or severe blockage of outer port rings forcing all gas through center ports.
How do technicians test for gas leaks around the burner manifold?
Technicians utilize calibrated electronic combustible gas sniffers capable of detecting methane concentrations down to 10 PPM, alongside non-corrosive bubbling leak detection solutions applied directly to valve stems and manifold threaded joints.
What happens if an uncertified contractor converts my Vulcan range from NG to LP?
Propane contains over 2.5 times the BTU energy content of natural gas per cubic foot and operates at much higher manifold pressure (10.0″ W.C. vs 3.5″ W.C.). If natural gas orifices (#41) are left in place on propane, the burner will over-fire violently by more than 200%, producing towering yellow flames, massive carbon monoxide emissions, melted grates, and extreme fire hazards.
Why does the spark electrode continue clicking after the range is turned completely off?
Clicking when turned off indicates that water, cleaning degreaser, or liquid boil-over has entered the microswitches mounted behind the front control burner valves. The conductive moisture bridges switch contacts, sending continuous 120V power to the spark module. The range should be disconnected from power until switches are dried or replaced.
What is the typical lifespan of a Vulcan Hart commercial restaurant range?
With proper daily degreasing and semi-annual preventative maintenance, a heavy-duty Vulcan Hart commercial range lasts between 15 and 25 years. Cast iron bodies and stainless steel chassis rarely wear out; periodic replacement of consumable brass orifices, valves, and spark modules keeps the unit in peak operating condition indefinitely.
How fast can a certified commercial technician arrive at my Crabapple Market restaurant?
Our commercial response fleet maintains dedicated service trucks staged throughout North Fulton County, specifically covering Milton, Alpharetta, Roswell, and Johns Creek. For urgent commercial hot-line breakdowns, average arrival times range from 45 to 90 minutes.
Do your commercial gas range repairs include a parts and labor warranty?
Yes. Every commercial cooking equipment repair performed by our EPA-certified master technicians is backed by our comprehensive 90-Day Commercial Parts and Labor Warranty. We install 100% genuine factory OEM parts sourced directly from Vulcan Hart / ITW Food Equipment Group.
Commercial Foodservice Equipment Navigation Silos
Explore our complete network of specialized commercial food service repair hubs, related cooking line challenges, brand directories, and North Fulton service territories below. For specialized commercial walk-in refrigeration coverage, review our certified True commercial refrigeration repairs across metro corridors.
Primary Commercial Service Hubs
Related Commercial Line Problems
Commercial Brand Specialists
North Fulton Commercial Service Areas
When kitchen equipment issues threaten dinner service, partnering with an experienced service company providing full-scope commercial cooking and refrigeration repair solutions ensures zero disruption to guest hospitality.
To verify our extensive commercial credentials and master technician track record, view our authenticated client reviews and commercial testimonials from restaurant operators across North Fulton County.
Key Engineering & Operational Takeaways
- Continuous spark electrode clicking on Vulcan Hart commercial ranges is directly triggered by flame rectification signals dropping below the critical 1.5 µA DC threshold.
- Weak, stunted blue flames result from carbonized grease boil-overs obstructing the precision #41 wire drill size brass spud orifice, starving the Venturi tube of fuel mass flow.
- Dynamic gas manifold pressure must test strictly at 3.5″ to 4.0″ W.C. for Natural Gas (10.0″ W.C. for LP) under full burner bank firing conditions.
- Never attempt DIY reaming of brass orifices with hard steel drill bits, needles, or paper clips, which flare openings and create dangerous carbon monoxide hazards.
- Ceramic electrode insulators must be cleaned with non-conductive solvent and set to a precise 1/8″ spark gap clearance above the burner port crown.
- Certified commercial restorations restore 100% stoichiometric combustion efficiency, silencing clicking, delivering 28,000 BTU thermal output, and ensuring full compliance with NFPA 54 and NFPA 96 kitchen fire codes.
Restore Your Vulcan Hart Cooking Line Today
Don’t let malfunctioning burners or continuous clicking cripple your commercial kitchen’s output during peak service hours. Connect with our Crabapple Market & North Fulton master certified gas technicians for immediate, same-day diagnostic service backed by factory OEM parts and a 90-day commercial warranty.
Call (770) 796-7742 for Priority Commercial Dispatch
Licensed • Insured • EPA Certified • 90-Day Commercial Parts & Labor Warranty